


Leave Your Message
Engineered for extreme thermal shocks, volatile hydrocarbon streams, and corrosive offshore environments, our critical-service valves guarantee flawless process isolation.
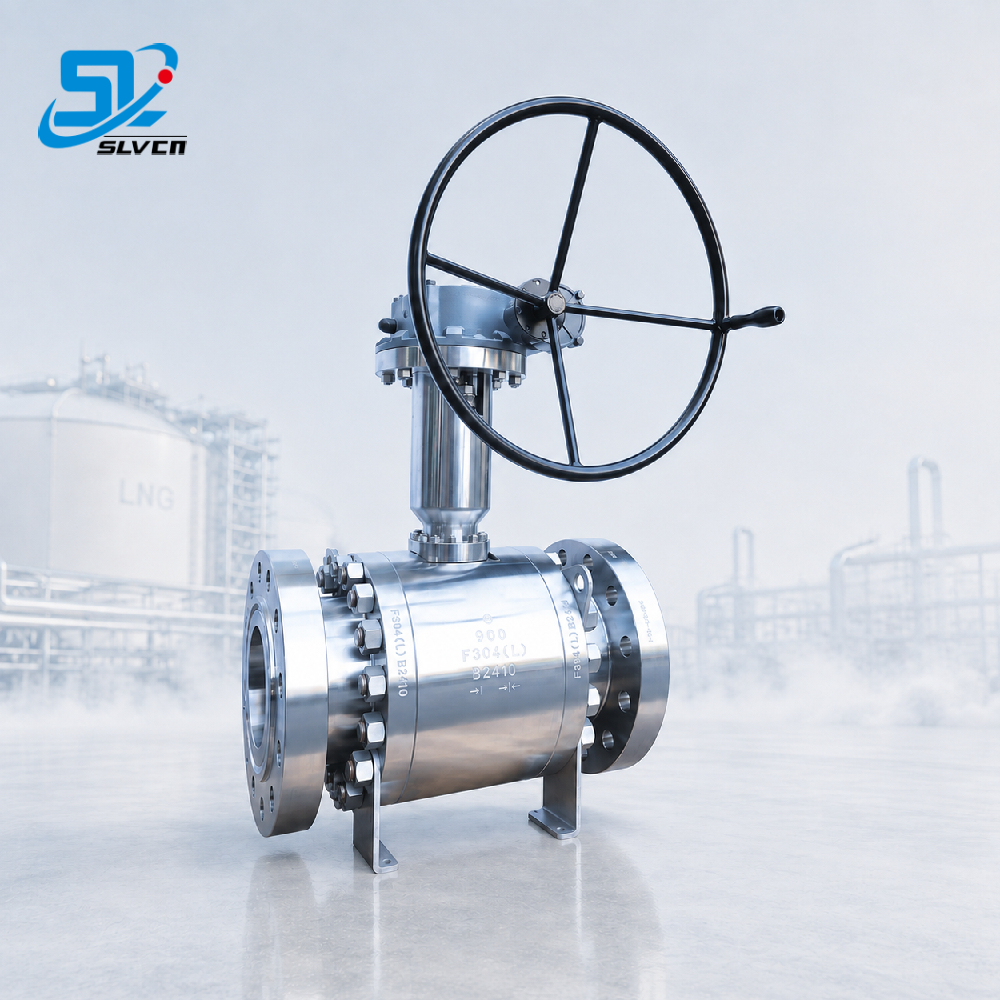
Rugged forged steel double block and bleed valve for topside LNG regasification and thermal cycling systems requiring high structural safety.
Explore Technical Specs →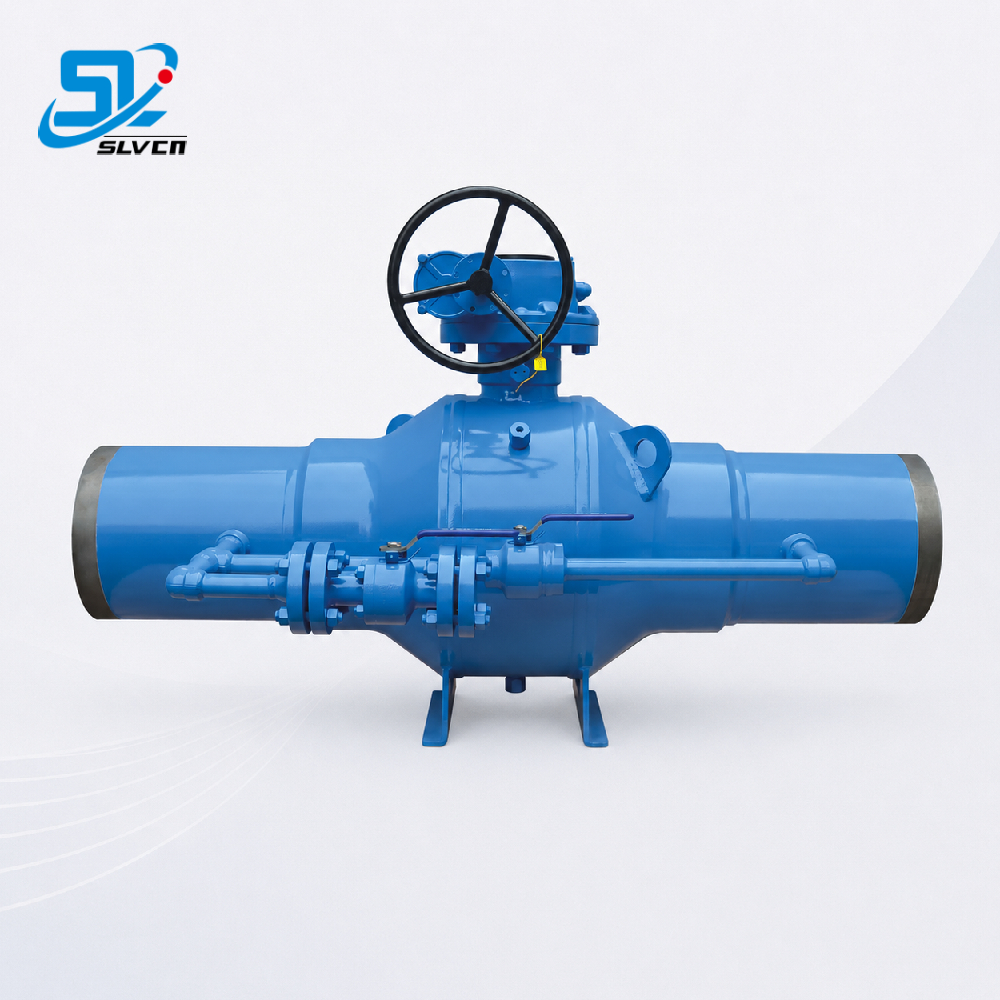
Hermetically sealed welded body eliminating fugitive flange emissions in offshore high-temperature transmission and separator manifolds.
Explore Technical Specs →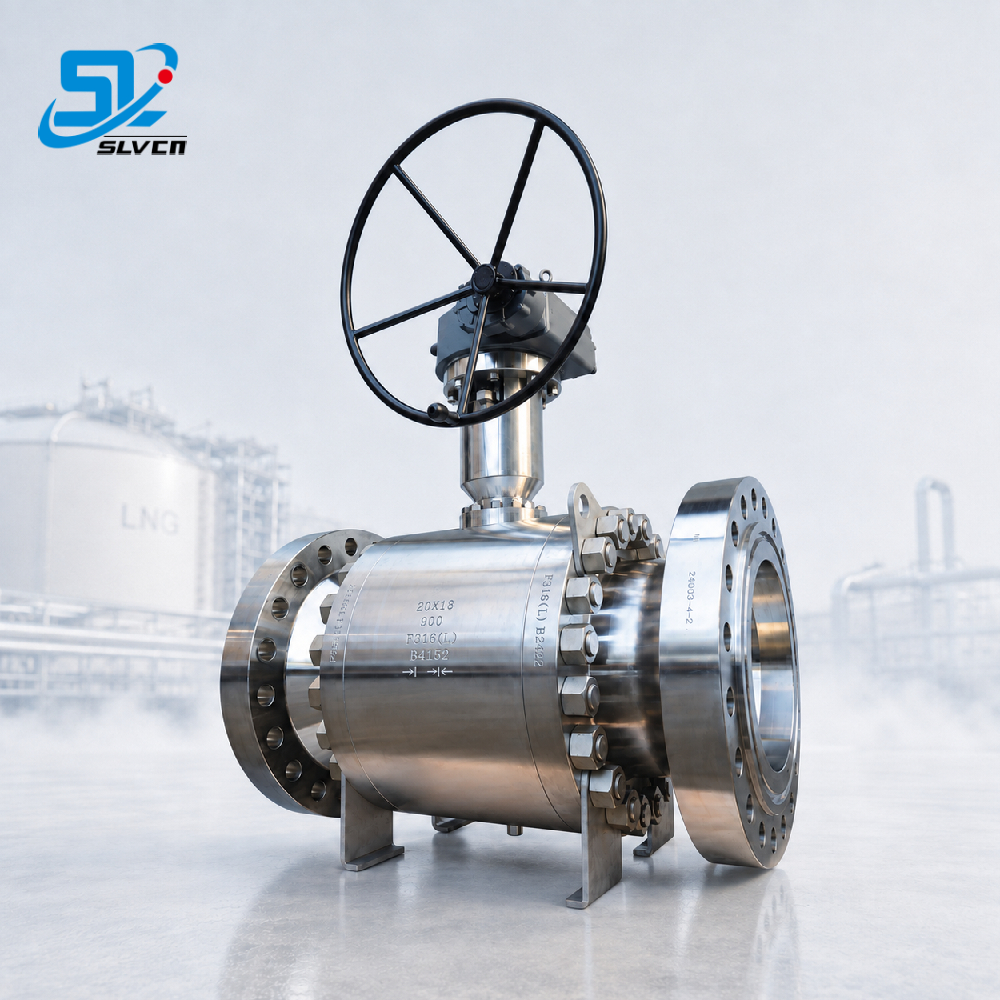
Compact design engineered to reduce weight on platform decks while providing bi-directional positive shutoff under high pressure differentials.
Explore Technical Specs →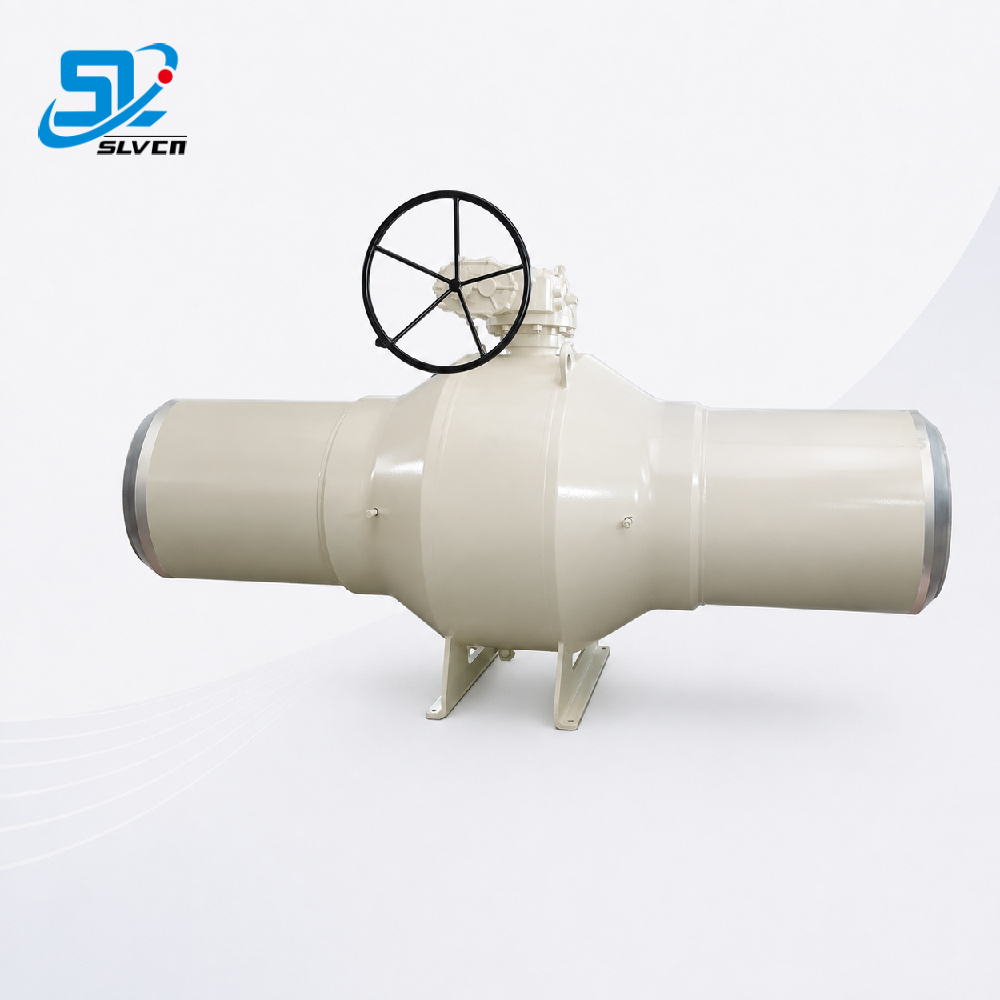
Equipped with extended pup pieces for seamless field welding, heavy-duty worm gear actuation, and deep-sea anti-corrosive coating systems.
Explore Technical Specs →Offshore oil and gas production has entered a new frontier characterized by deeper waters, higher reservoir pressures, and elevated bottom-hole temperatures. Modern production facilities, including Floating Production Storage and Offloading (FPSO) units, tension leg platforms (TLP), and fixed deepwater jackets, routinely manage reservoir fluids exceeding temperatures of 200°C (392°F) to well above 450°C (842°F) during thermal recovery and secondary refining processes.
Under these severe thermo-mechanical stresses, conventional resilient-seated ball valves suffer from rapid seat polymer degradation, blistering, and thermal binding. Unplanned downtime on an offshore installation costs operators millions of dollars per day, transforming valve reliability from a simple procurement metric into an essential asset integrity imperative.
Commercial Drivers: Global offshore CAPEX investments demand maintenance-free operation across 25 to 30-year design lifespans. High Temperature Ball Valves for Offshore Oil and Gas Platforms must mitigate thermal fatigue, resist chloride-induced stress corrosion cracking (SCC), and comply with stringent zero-fugitive emission targets under ISO 15848-1.


Years of Valve Manufacturing Excellence
 Jiangsu Shoulong Valve Co., Ltd. (SLVCN)
With over 30 years of manufacturing experience, SLVCN is a professional designer and manufacturer of high-performance forged steel ball valves for critical industrial applications. We specialize in extreme working conditions including high pressure, high temperature, and cryogenic environments, providing safe and reliable flow control solutions for global industrial projects where operational reliability is non-negotiable.
Our core product range covers forged trunnion-mounted and floating ball valves, top-entry and side-entry ball valves, fully welded ball valves, metal seated ball valves, cryogenic ball valves, high-pressure ball valves up to Class 2500 (PN420) and customized higher pressure ratings, as well as high-temperature service valves. Compared with conventional cast valves, SLVCN forged valves feature higher material density, superior mechanical strength, improved resistance to pressure fluctuations and thermal shock, and significantly longer service life under severe service conditions.
Today, SLVCN serves customers in more than 100 countries and regions, supplying valves to EPC contractors, engineering companies, and end users across Europe, the Middle East, Southeast Asia, and the Americas. Backed by strong engineering expertise, advanced manufacturing, and rigorous quality control, SLVCN is committed to delivering safe, durable, and truly engineered valve solutions for the world’s most demanding industrial projects.
Contact Offshore Engineering Team →On offshore platforms where space is constrained and safety thresholds are critical, high temperature ball valves must function reliably across diverse, harsh process nodes.
Raw unprocessed crude extracted from deep HPHT formations reaches platform topsides at severe thermal levels combined with entrained sand, sour H2S, and CO2. SLVCN metal-seated forged trunnion ball valves resist high fluid velocities and erosion while delivering bubble-tight Double Block and Bleed isolation.
For offshore heavy crude recovery employing Steam Assisted Gravity Drainage (SAGD) or cyclic steam stimulation, platform piping systems handle superheated steam up to 400°C to 500°C. Our high temperature ball valves utilize specialized Belleville spring-energized metal seats that dynamically compensate for dramatic thermal expansion.
Offshore gas processing plants rely on Triethylene Glycol (TEG) dehydration units to prevent pipeline hydrate formation. TEG regeneration boilers operate at elevated temperatures with corrosive organic acids. SLVCN valves in duplex or nickel alloy metallurgy ensure non-galling shutoff during continuous boiling operations.
Topside shell-and-tube or printed circuit heat exchangers transfer thermal energy between raw crude and refined products. Sudden process fluctuations cause thermal shock. The rugged forged body structure of SLVCN ball valves prevents body-joint distortion and gasket displacement under cyclic thermal stress.
During platform emergency depressuring (HIPPS / ESDV), valves must open or close instantaneously against full system differential pressures while enduring cryogenic blowdown chill followed by high thermal radiation from flaring systems, demanding API 607 / 6FA certified fire-safe integrity.
Re-injecting high-temperature produced water contaminated with chlorides, sulfates, and scale inhibitors downhole causes accelerated pitting and galvanic corrosion. SLVCN utilizes Super Duplex 2507 and Inconel cladding to guarantee decades of erosion-corrosion resistance.
Safety and reliability are embedded in every design. Our forged ball valves are equipped with Double Block and Bleed (DBB) structures, anti-blowout stems, fire-safe designs in accordance with API 607 / API 6FA, anti-static devices, emergency sealing systems, and pressure-balanced seating structures suitable for high differential pressure operation. Valves can be designed with SPE or DPE seat configurations based on application requirements. For sour service environments, materials and sealing systems comply with NACE MR0175 / ISO 15156 requirements.
Designed for High Pressure, High Temperature, and Cryogenic Applications, SLVCN valves are widely used in long-distance oil & gas transmission pipelines, LNG storage and regasification terminals, offshore platforms and deepwater projects, power plants, refineries, compressor stations, and high-pressure chemical processing units. Whether handling flammable media, corrosive fluids, sour service media (H₂S), ultra-low temperatures, or extreme differential pressures, our valves ensure stable operation, bubble-tight shut-off, and maximum system safety in accordance with international sealing and performance standards.


Adhering to rigorous international standards, our testing infrastructure ensures every valve operates safely under catastrophic conditions.
To ensure consistent quality, each valve undergoes a complete series of inspections and performance tests in accordance with API 6D, API 598, and ISO 5208, including shell test, seat leakage test (Rate A / zero visible leakage), fire-safe test, cryogenic test, operational torque test, dimensional inspection, and PMI material verification. SLVCN operates dedicated cryogenic testing facilities to validate valve performance at ultra-low temperatures down to −196°C.
SLVCN is certified to ISO 9001, CE, and API standards, and our products comply with API 6D, ASME B16.34, DIN, ANSI, and JIS specifications. We provide extensive customization capabilities covering sizes from 1/2” to 36”, full bore or reduced bore, special materials including A105, LF2, F11, F22, F51, Inconel, various soft and metal seat designs, and intelligent actuation with pneumatic, electric, and gear operators.
The offshore sector is evolving toward unmanned platforms and intelligent topside assets. SLVCN integrates smart diagnostic partial-stroke testing (PST) digital positioners, acoustic emission sensors for micro-leak detection, and predictive thermal wear modeling, empowering offshore operators with real-time health diagnostics and predictive condition monitoring.
Engineered for extreme offshore conditions, our full spectrum of forged ball valves offers unmatched performance in high temperature, high pressure, and cryogenic service.
Designed for severe thermal swings, cryogenic containment, and high-pressure platform storage utilities.
View Product Specifications →
Integral forged body with zero external leak paths, ideal for high temperature platform export risers.
View Product Specifications →
Space-saving reduced bore configuration engineered to lower deck payload without sacrificing flow isolation.
View Product Specifications →
Equipped with extended pup pieces for seamless direct welding onto subsea or platform high-pressure lines.
View Product Specifications →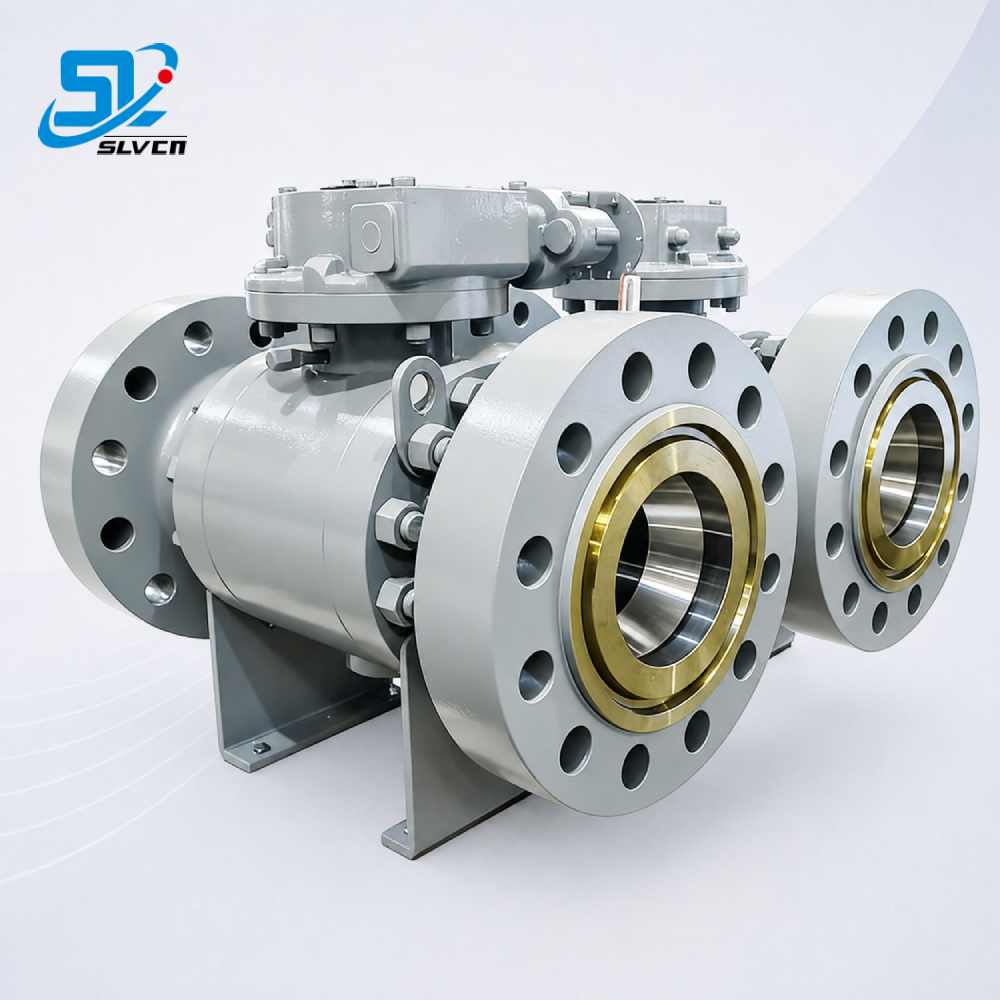
Heavy-duty metal-to-metal sealing utilizing tungsten carbide coatings to endure abrasive, high-temperature crude.
View Product Specifications →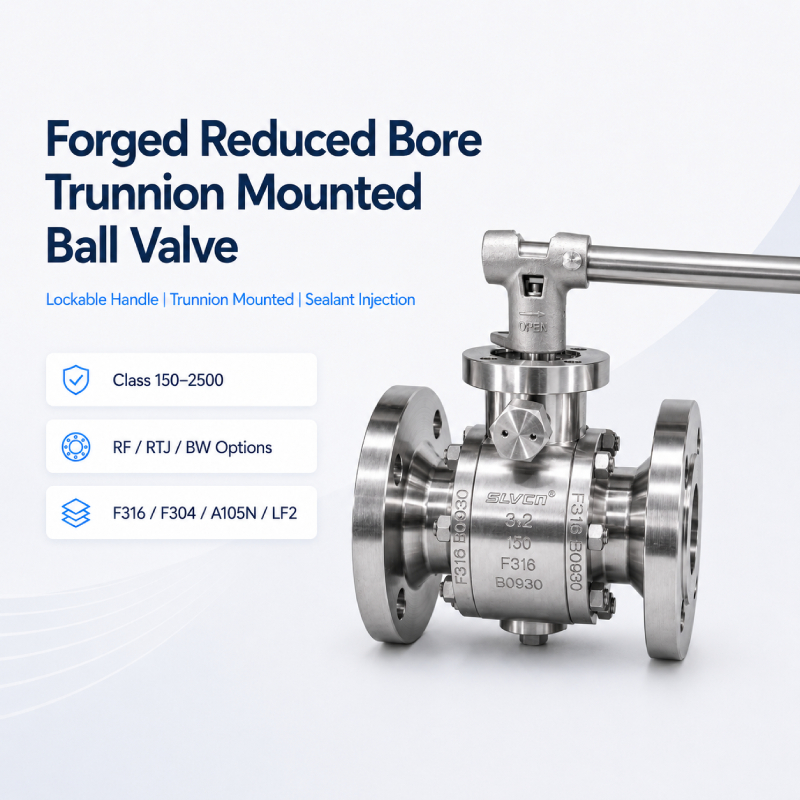
Manual lockable mechanism preventing accidental platform operation, built with anti-blowout stem integrity.
View Product Specifications →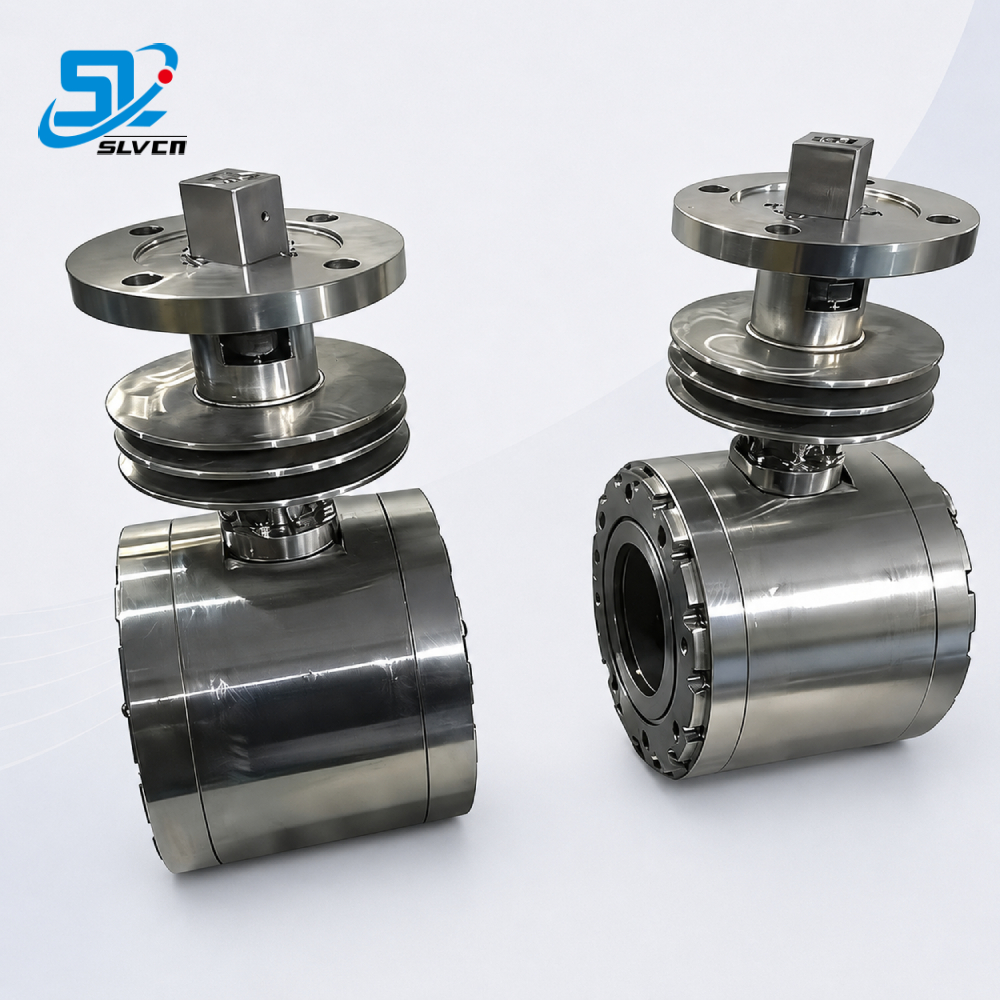
Specialized high-temperature seat compounds and graphitic packing engineered for extreme offshore thermal recovery.
View Product Specifications →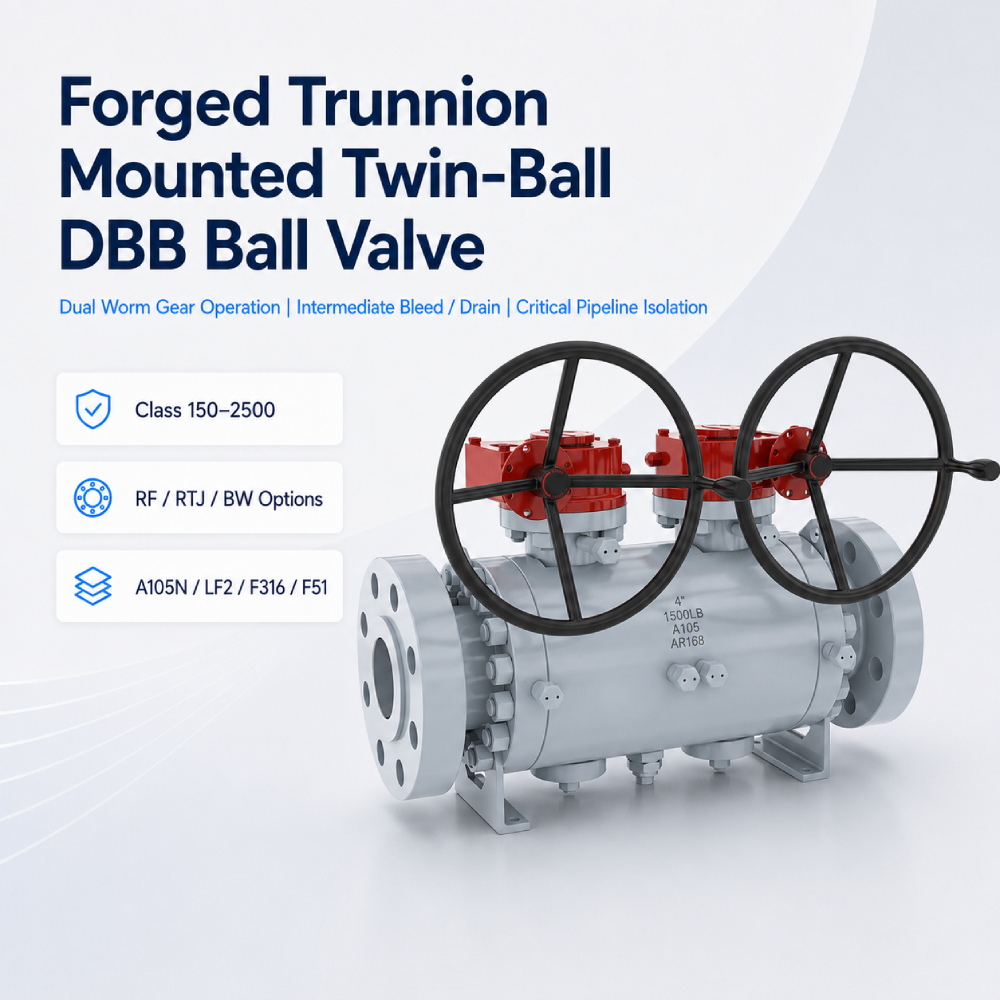
Twin-ball architecture delivering dual mechanical barriers in a single forged valve body, saving deck space and maximizing safety.
View Product Specifications →From custom alloy selection (Inconel, Monel, Super Duplex) to extreme temperature testing down to -196°C and up to +500°C, SLVCN delivers API 6D certified flow control systems engineered specifically for offshore oil and gas platforms.
Request Technical Data Sheets & Quotation →


 18061659285

