


Leave Your Message
Heavy-duty forged metal-seated architectures built specifically for severe scouring, high pressure differentials, and extreme thermal cycling.
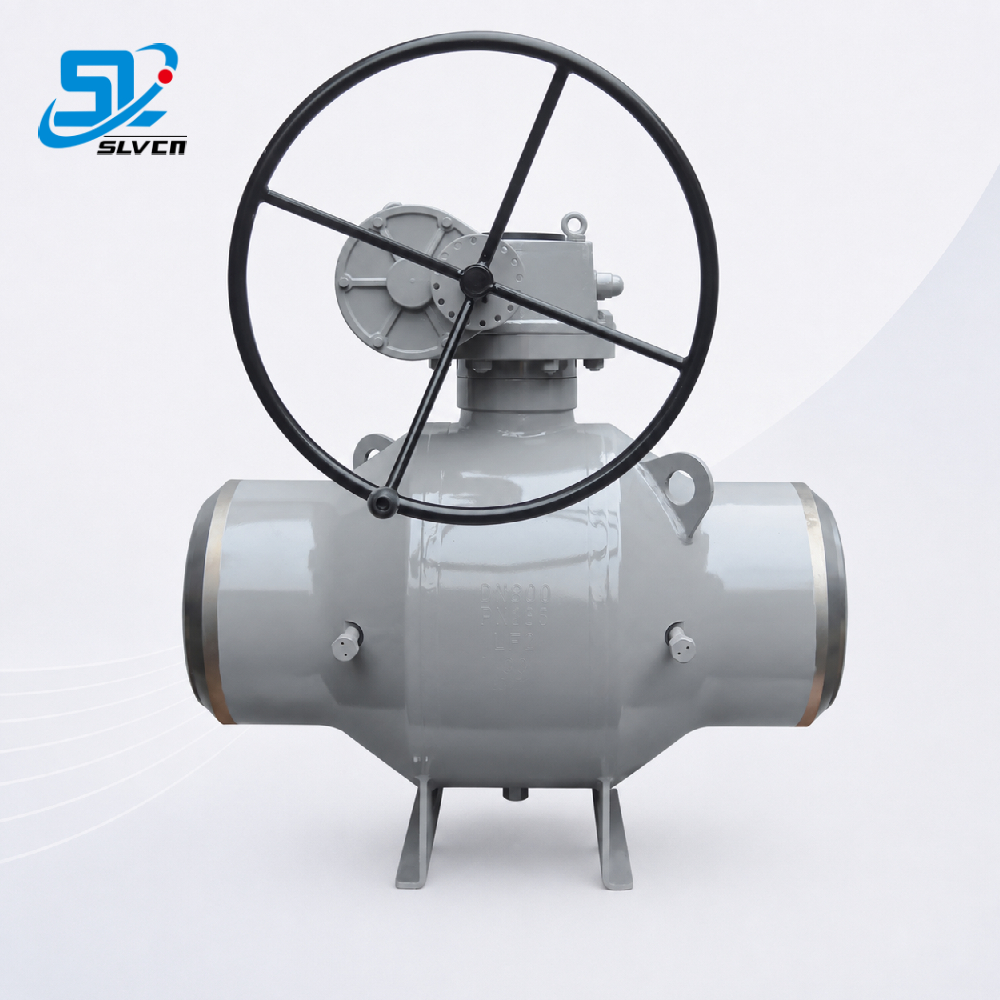
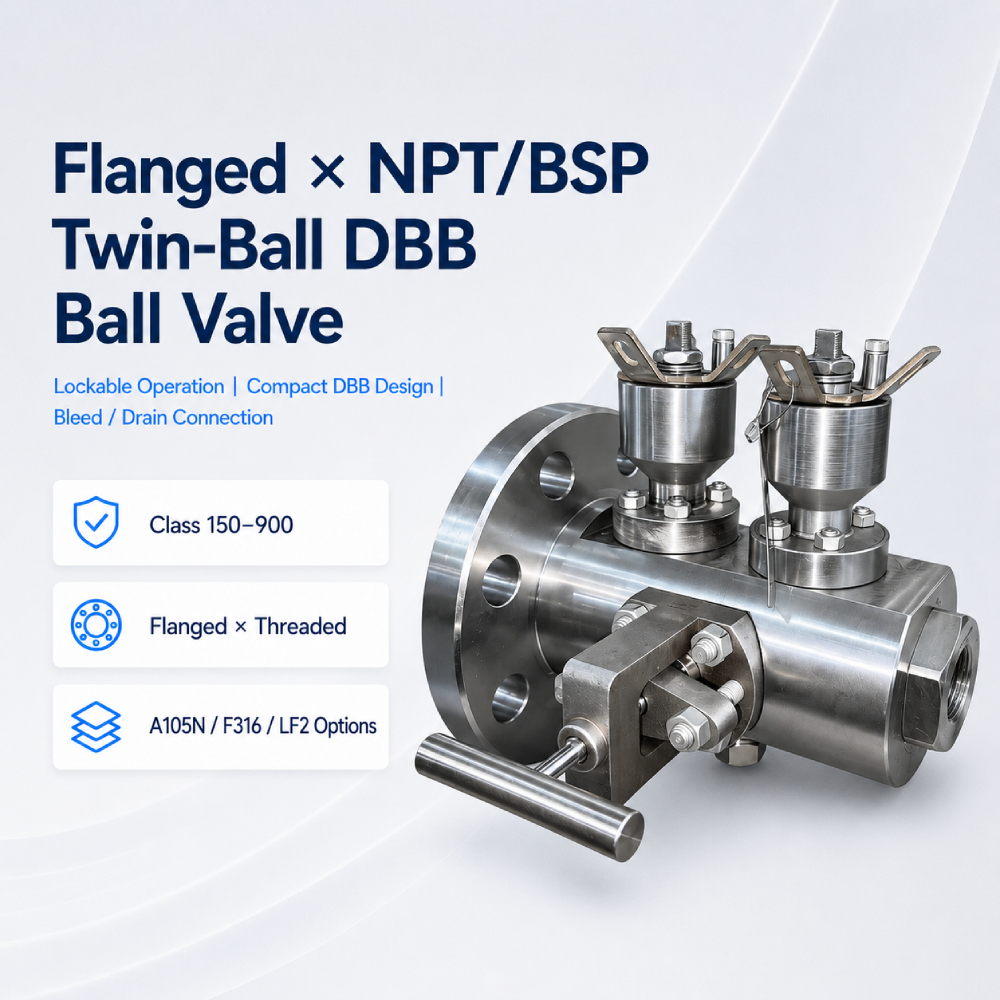
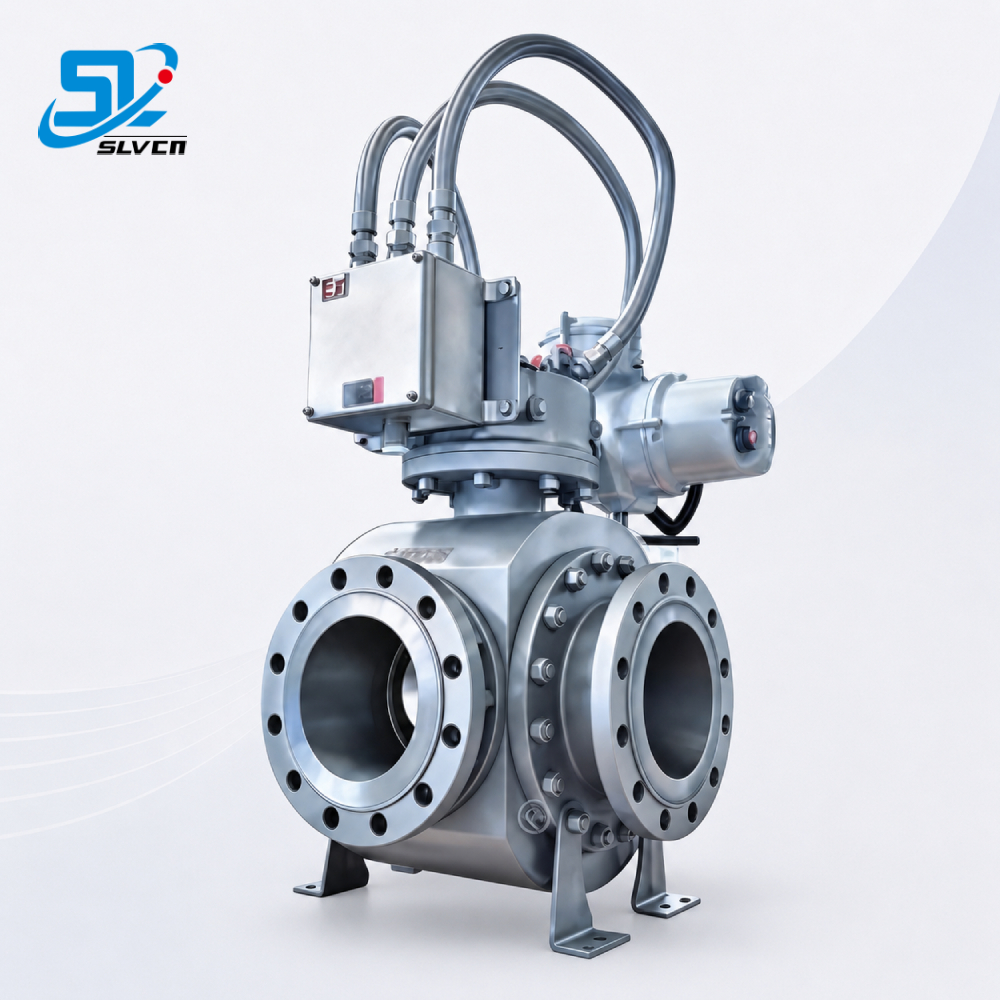
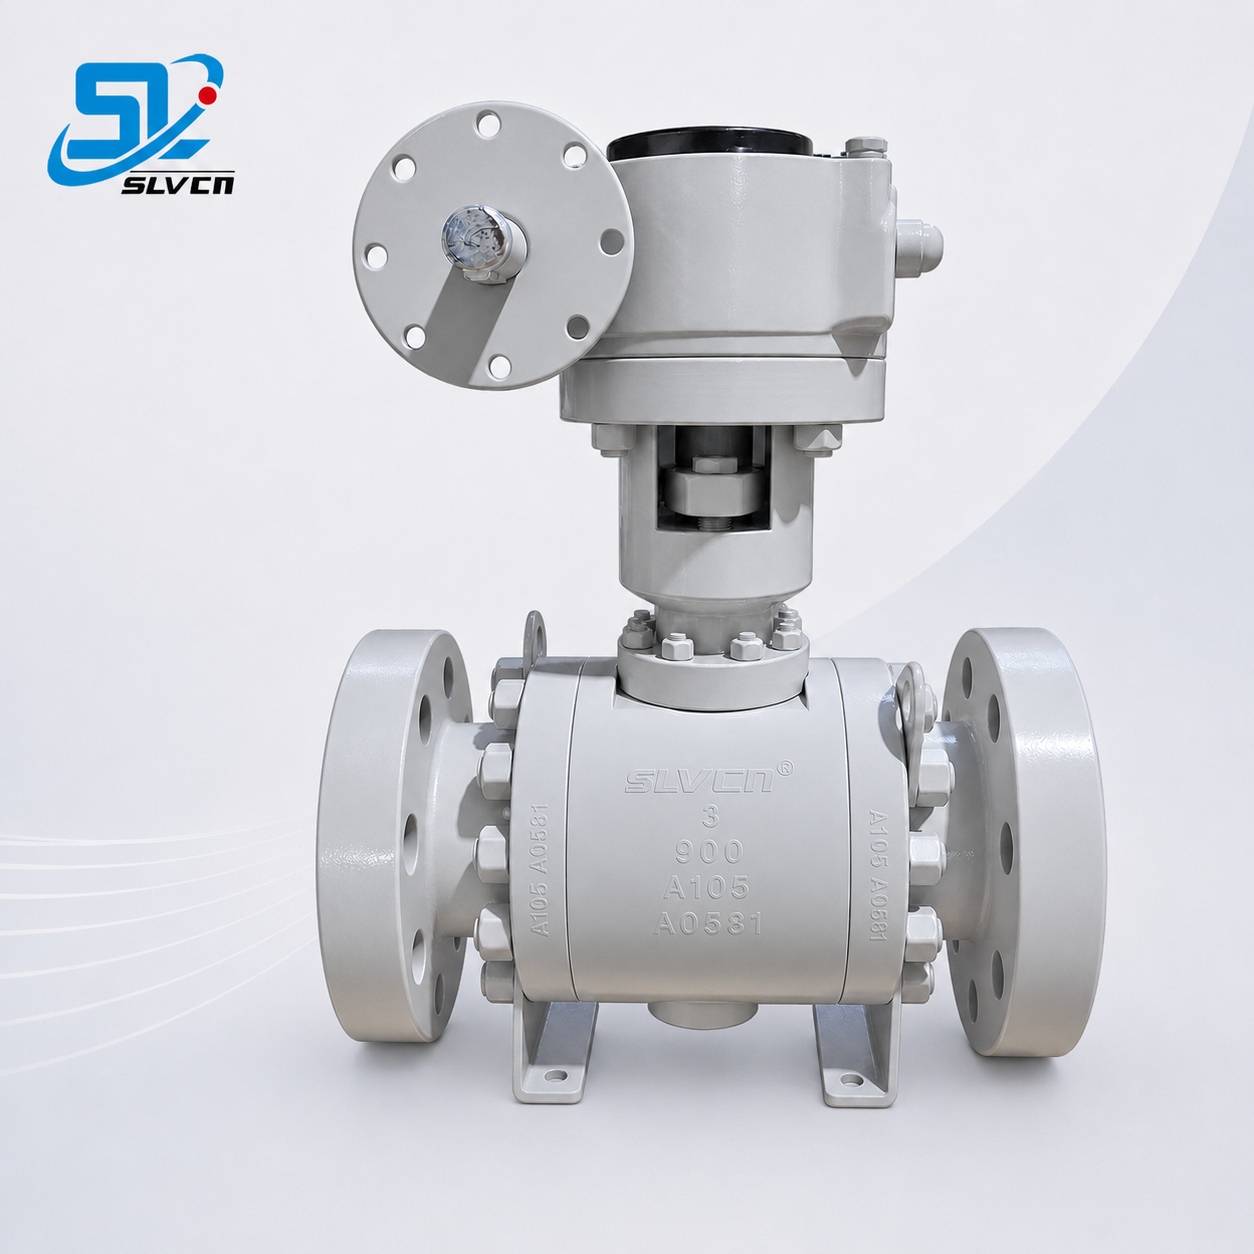
In modern heavy industrial operations—ranging from High-Pressure Acid Leaching (HPAL) in nickel/cobalt hydrometallurgy to coal gasification black water recycling and oil sands hydro-transport—slurry pipeline systems operate under some of the most destructive operating parameters in the processing sector. High operating temperatures (ranging from 180°C to well over 450°C) coupled with high solid particle concentrations (up to 60 wt%) create an aggressive combination of solid-particle erosion, high-temperature cavitation, and chemical micro-galvanic corrosion.
Standard soft-seated valves fail catastrophically within days in such environments due to polymer decomposition, particulate embedding, and explosive decompression. A purpose-engineered High Temp Valve For Abrasive Slurry Pipeline Systems requires an integrated design framework: advanced high-density forged metallurgy, thermal expansion compensation, specialized scraper sealing faces, and zero-cavity entrapment geometry.

Overcoming particle erosion and severe thermal shocks with state-of-the-art materials science and mechanical valve architecture.
Sealing faces and spherical balls are coated with High-Velocity Oxygen-Fuel (HVOF) Tungsten Carbide (WC-Co-Cr) or Chromium Carbide (Cr3C2-NiCr), achieving a microhardness above 68–72 HRC to resist continuous slurry impingement.
Specially contoured seat rings act as mechanical scrapers during ball rotation, shearing through sticky cakes, scale buildup, and packed slurry fines to preserve clean metal-to-metal sealing surfaces.
High-temperature Belleville Inconel 718 disc spring energizers maintain continuous, uniform seat loading across wide thermal swings (from ambient start-up up to 550°C), compensating for differential expansion.
Where standard industrial valves fail in minutes, our specialized abrasive slurry valves ensure continuous multi-year operational uptime.
Nickel and cobalt extraction relies on autoclave leaching at 250°C–280°C and pressures above 50 bar with high sulfuric acid and mineral slurry concentrations. SLVCN titanium-stabilized and alloy-clad forged valves prevent both extreme erosive grooving and acidic corrosion while sustaining absolute zero seat leakage.
Gasifier quench loops subject letdown valves to high differential pressure letdowns with entrained abrasive fine slag and soot. The high velocity causes severe throttling erosion. Our tungsten carbide hard-faced trunnion valves provide prolonged throttling resistance and dependable emergency shut-off.
Transporting coarse silica sand, heavy bitumen residue, and hot diluent at temperatures up to 350°C leads to rapid erosion-corrosion. Fully welded forged valve bodies eliminate fugitive flange emissions while internal hardfaced flow paths ensure smooth slurry passage without cavity clogging.
In the Bayer process, caustic bauxite slurries at elevated temperatures cause heavy scaling and abrasive wear on valve internals. Our self-scraping metal seat technology slices through hardened scale formations on every cycle, preventing valve seizure and unseated leakage.
With over 30 years of manufacturing experience, SLVCN is a professional designer and manufacturer of high-performance forged steel ball valves for critical industrial applications. We specialize in extreme working conditions including high pressure, high temperature, and cryogenic environments, providing safe and reliable flow control solutions for global industrial projects where operational reliability is non-negotiable.
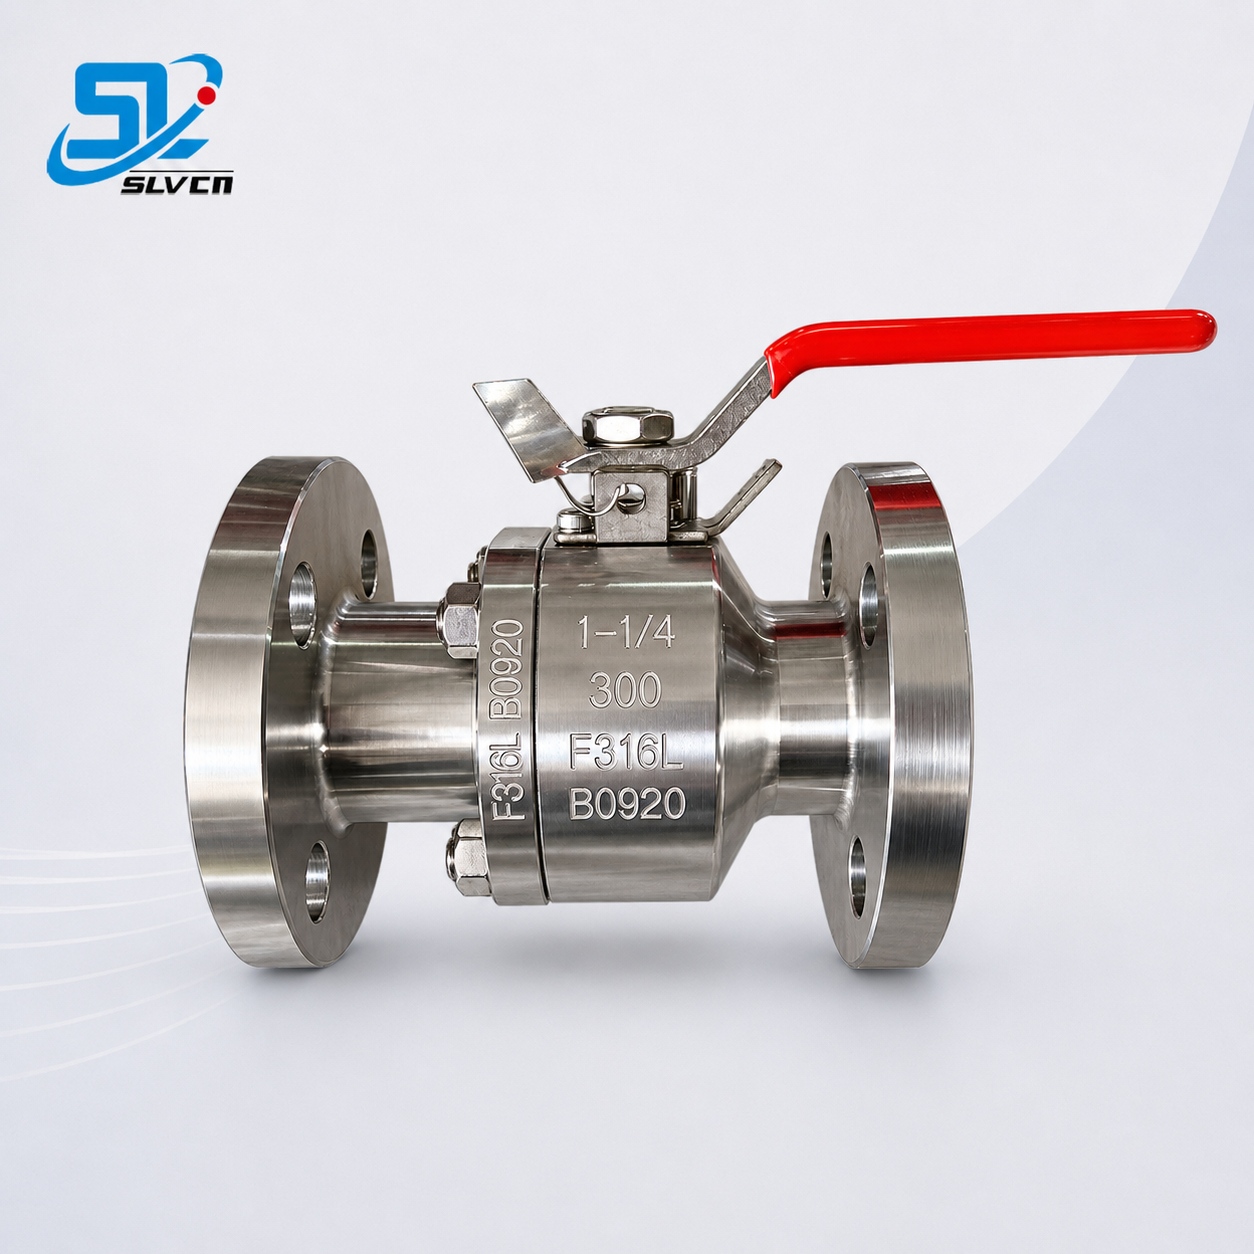
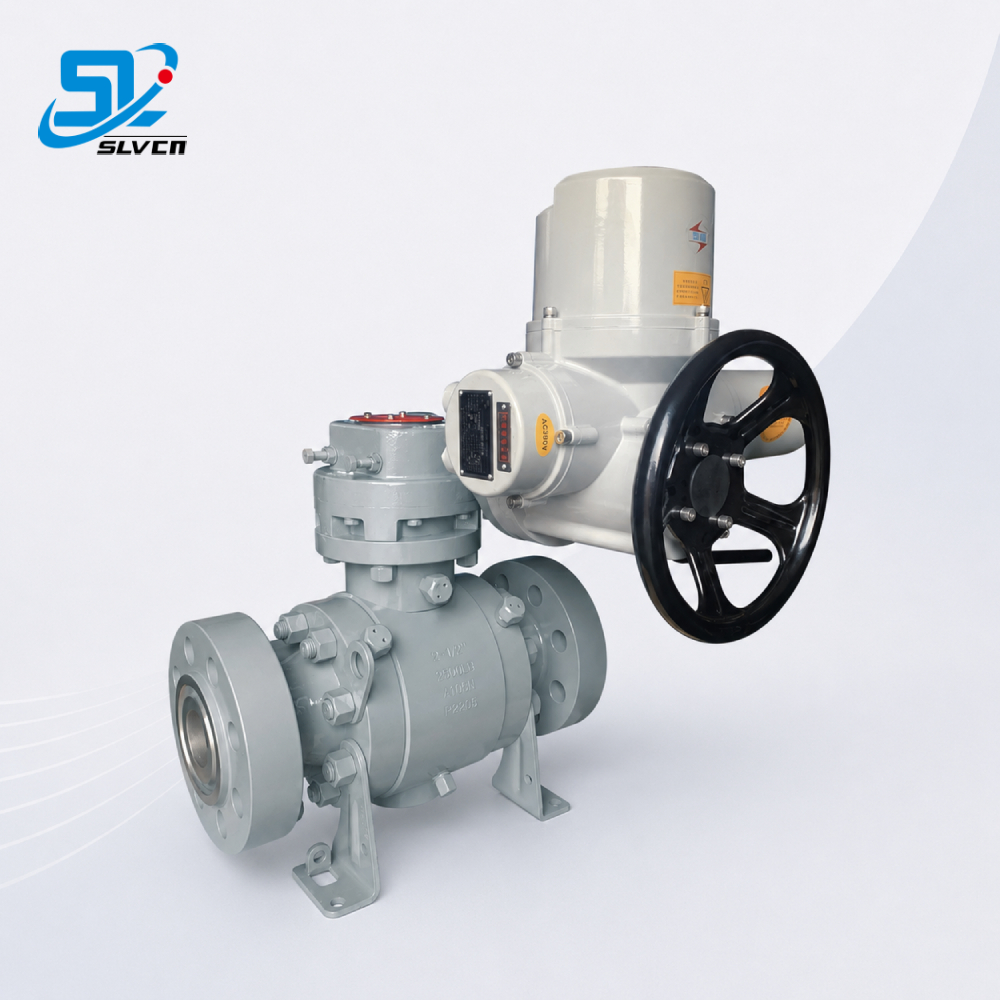
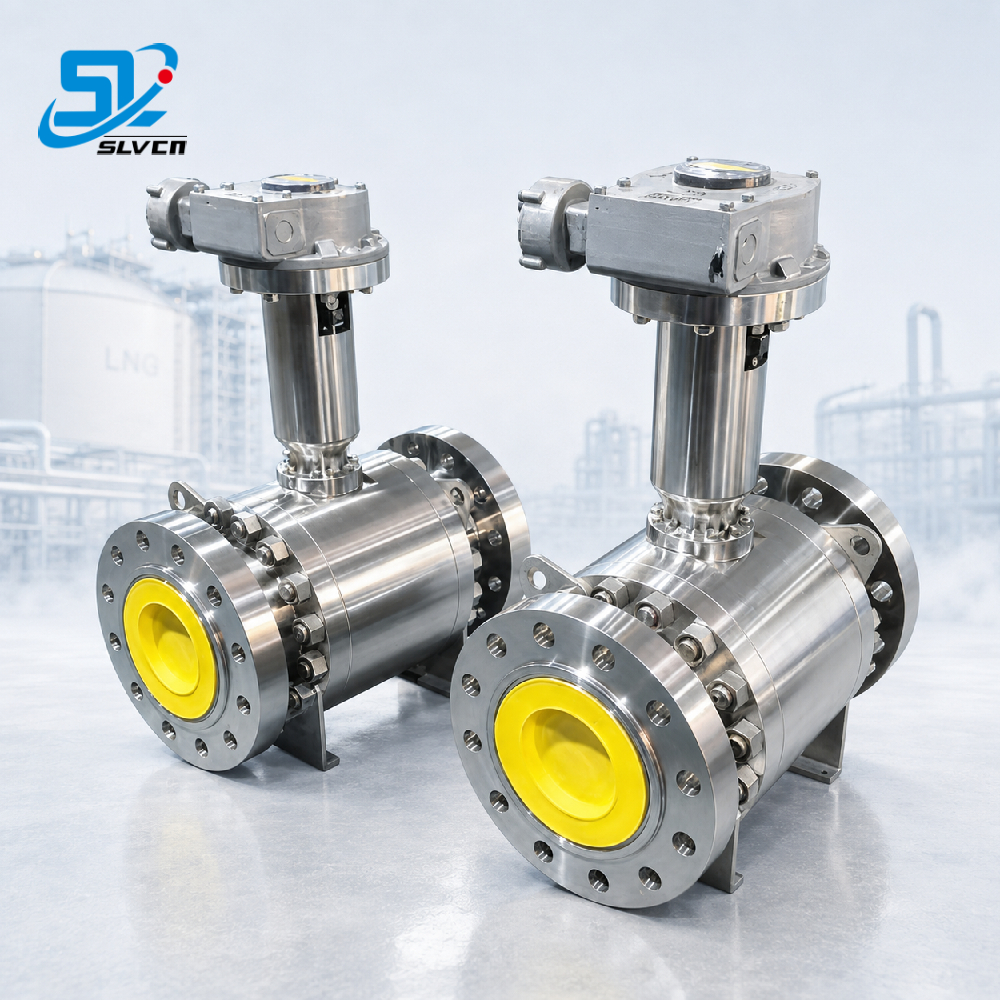
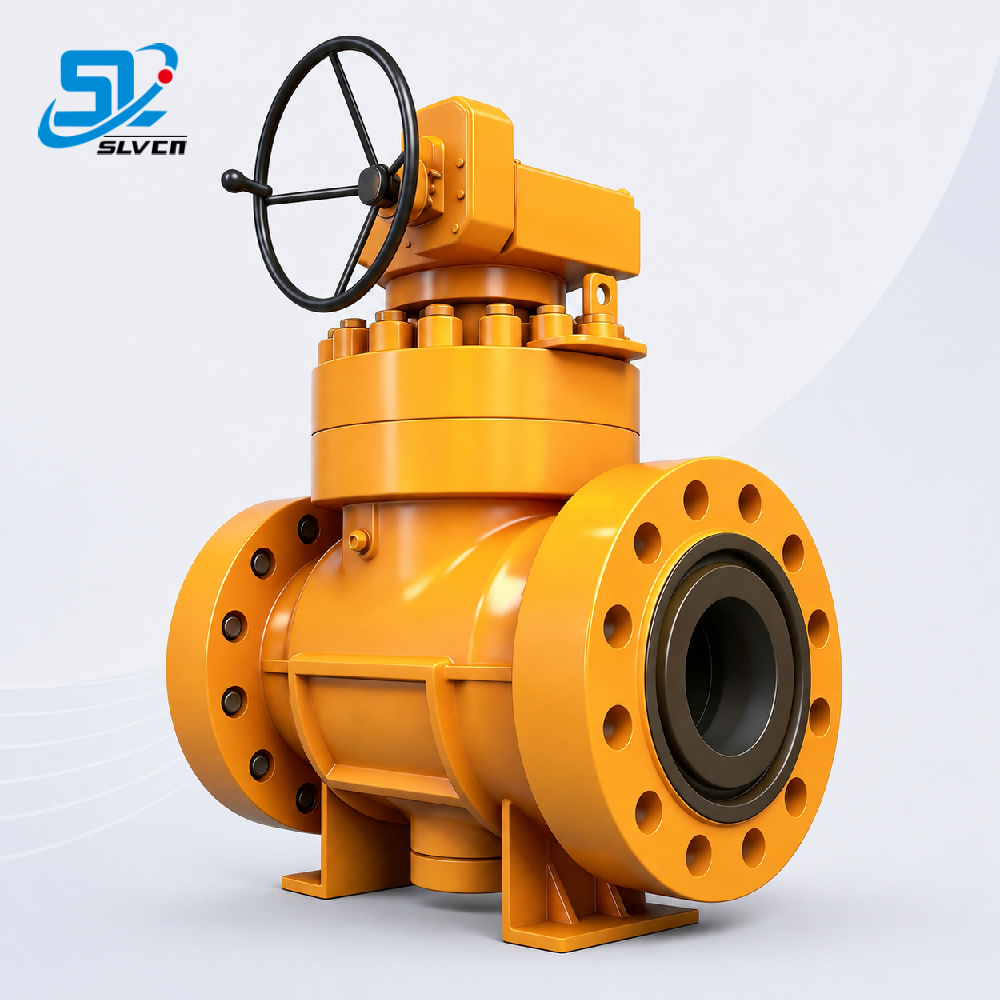
Our core product range covers forged trunnion-mounted and floating ball valves, top-entry and side-entry ball valves, fully welded ball valves, metal seated ball valves, cryogenic ball valves, high-pressure ball valves up to Class 2500 (PN420) and customized higher pressure ratings, as well as high-temperature service valves. Compared with conventional cast valves, SLVCN forged valves feature higher material density, superior mechanical strength, improved resistance to pressure fluctuations and thermal shock, and significantly longer service life under severe service conditions.
Consult Our Engineering Team



SLVCN valves are widely used in long-distance oil & gas transmission pipelines, LNG storage and regasification terminals, offshore platforms and deepwater projects, power plants, refineries, compressor stations, and high-pressure chemical processing units. Whether handling flammable media, corrosive fluids, sour service media (H₂S), ultra-low temperatures, or extreme differential pressures, our valves ensure stable operation, bubble-tight shut-off, and maximum system safety in accordance with international sealing and performance standards.
Safety and reliability are embedded in every design. Our forged ball valves are equipped with Double Block and Bleed (DBB) structures, anti-blowout stems, fire-safe designs in accordance with API 607 / API 6FA, anti-static devices, emergency sealing systems, and pressure-balanced seating structures suitable for high differential pressure operation. Valves can be designed with SPE or DPE seat configurations based on application requirements. For sour service environments, materials and sealing systems comply with NACE MR0175 / ISO 15156 requirements.
Every severe service valve undergoes uncompromising validation before commissioning in mission-critical pipelines.
100% of manufactured valves undergo high-pressure hydrostatic shell testing, low-pressure gas seat testing, and Rate A bubble-tight verification to ensure zero visible leakage under full working pressures.
Full positive material identification (PMI), ultrasonic testing (UT), magnetic particle inspection (MPI), and microstructure hardness checks ensure strict compliance with ASTM A105, LF2, F11, F22, F51 Duplex, and Inconel alloys.
SLVCN operates proprietary high-temperature thermal cycle ovens and dedicated cryogenic testing chambers down to -196°C to prove torque repeatability and sealing tightness across extreme thermal shocks.
Today, SLVCN serves customers in more than 100 countries and regions, supplying valves to EPC contractors, engineering companies, and end users across Europe, the Middle East, Southeast Asia, and the Americas. Backed by strong engineering expertise, advanced manufacturing, and rigorous quality control, SLVCN is committed to delivering safe, durable, and truly engineered valve solutions for the world’s most demanding industrial projects.
Explore our complete range of certified forged ball valves engineered for abrasive slurries, high temperatures, high pressures, and cryogenic flow control.


 18061659285

