


Leave Your Message
Precision-engineered gear-actuated and trunnion-mounted ball valves designed for high-differential pressures, underground burial, and extreme gas transmission applications.
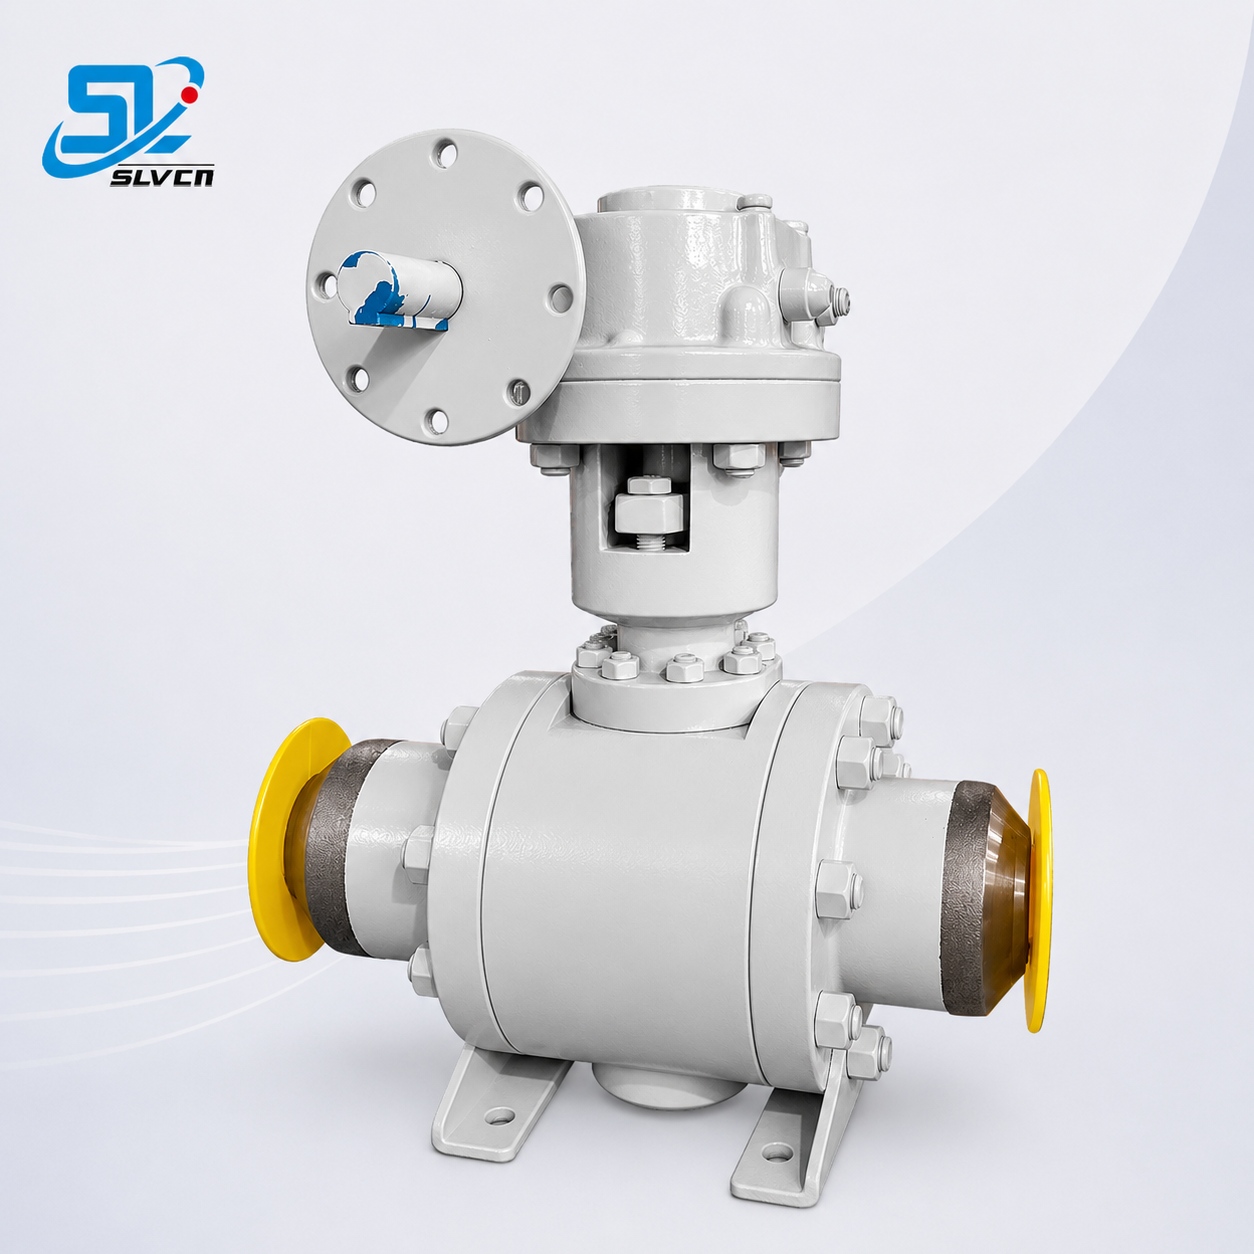
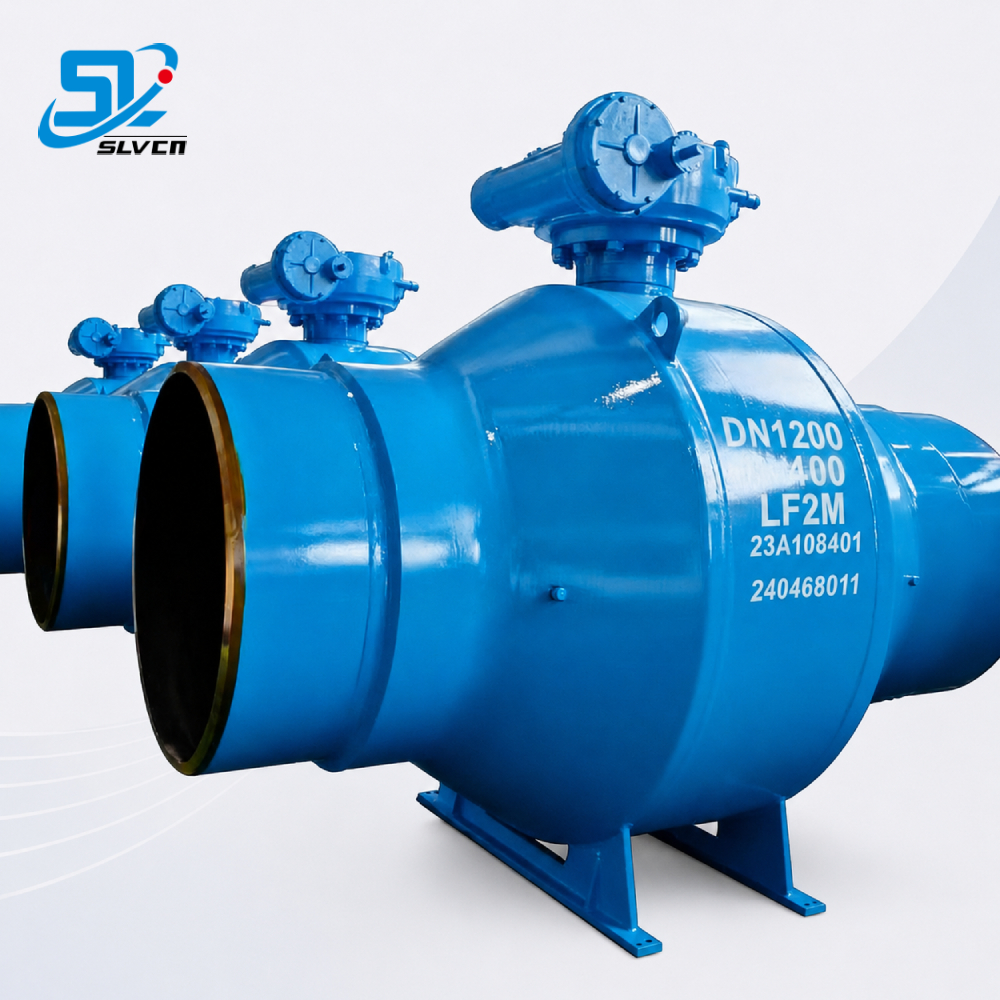
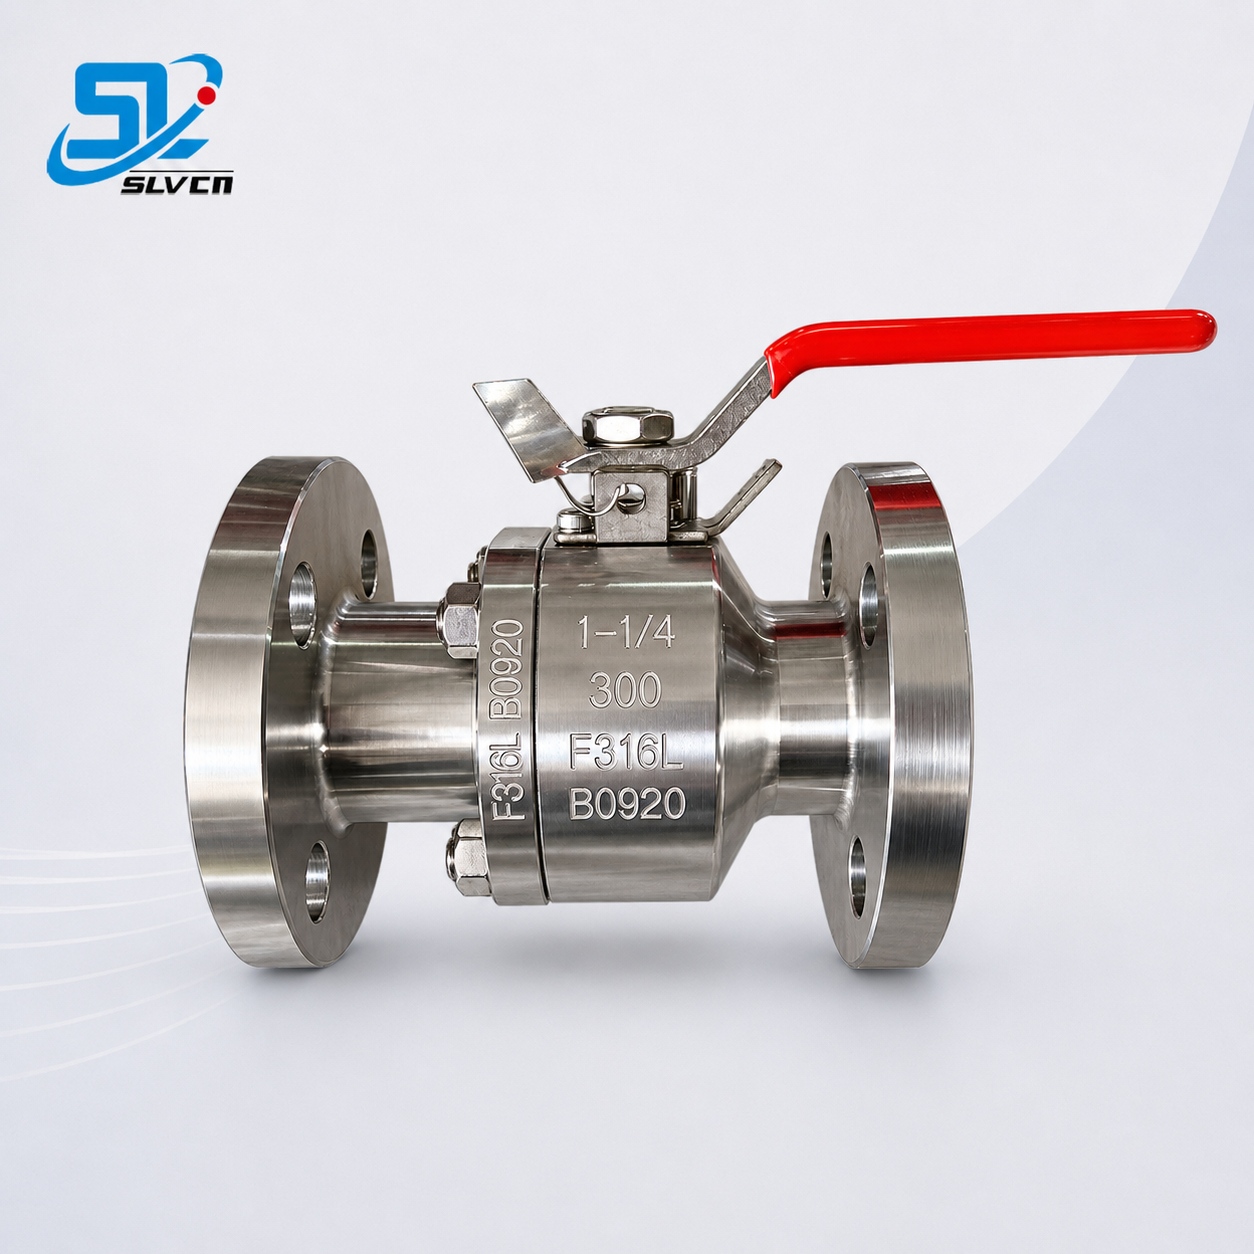
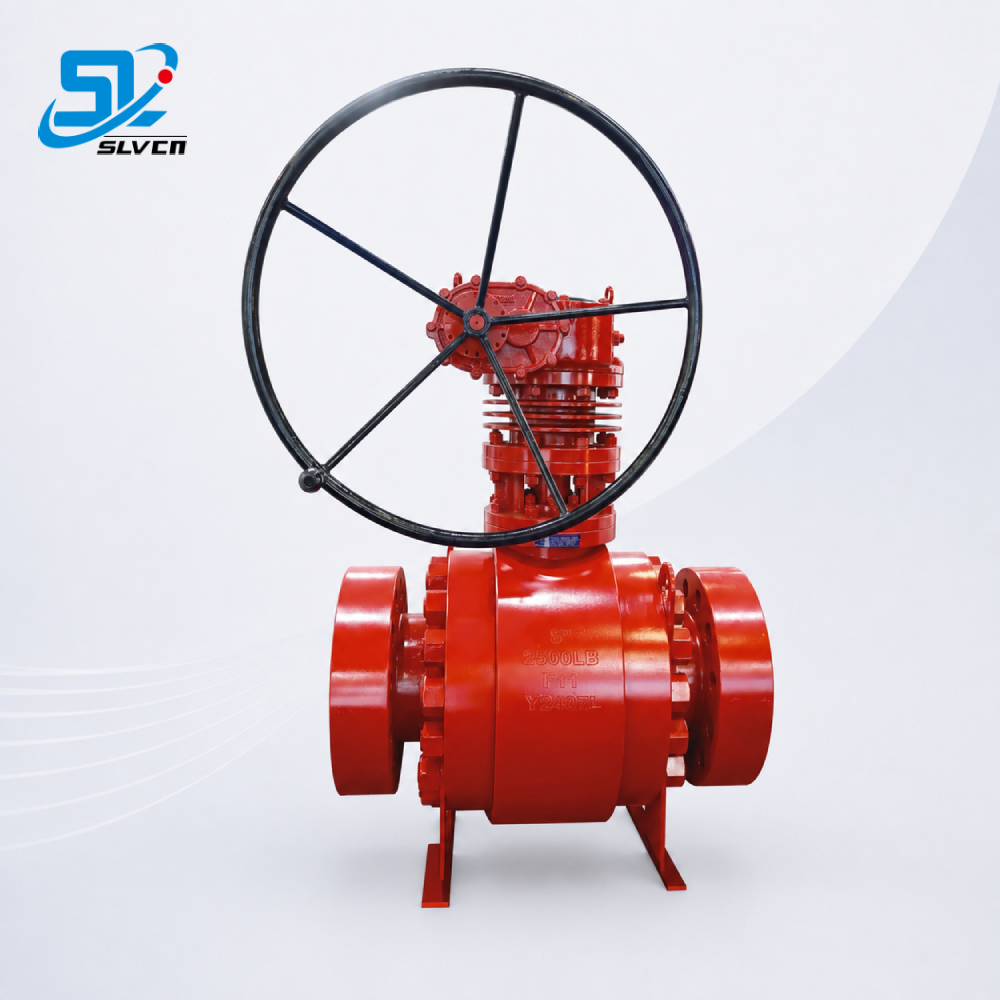
Global natural gas transmission infrastructure is experiencing unprecedented technological advancement. As energy networks transition toward higher operating pressures (up to ASME Class 1500 and Class 2500) and expanded pipeline diameters (up to 48", 56", and beyond), manual lever operation becomes physically impossible due to extreme hydrodynamic breakout torque.
A heavy-duty gear ball valve for large diameter gas pipelines serves as the critical mechanical barrier and isolation unit. Utilizing enclosed multi-stage worm or planetary gearboxes with high reduction ratios, these valves enable safe, smooth, single-operator manual actuation under full differential line pressure, preventing dangerous water-hammer effects, cavitation, and sudden gas decompression.
Modern gear-operated valves are engineered not only for basic quarter-turn isolation but also to accommodate strict fugitive emissions standards (ISO 15848-1 Class A/AH), hydrogen-blend transport compatibility, and long-term subterranean deployment without maintenance.
An in-depth look at how advanced gearbox design, forged valve metallurgy, and trunnion-mounted mechanics combine to guarantee failsafe quarter-turn isolation.
Equipped with ductile iron or cast steel gear housings, heat-treated alloy steel worms, and high-tensile aluminum-bronze worm gears. Built-in adjustable mechanical travel stops ensure exact 0° to 90° positioning, preventing seal pinching and premature seat destruction.
For large diameter pipelines (12" to 56"), the ball is securely anchored via top and bottom trunnion bearings. Line pressure forces the upstream seat ring against the ball rather than moving the ball downstream, drastically lowering torque and minimizing seat wear.
Both upstream and downstream seats provide independent, bi-directional pressure sealing. With the valve fully closed, fluid trapped in the body cavity can be vented through the bleed valve, verifying zero seat leakage without interrupting pipeline flow.
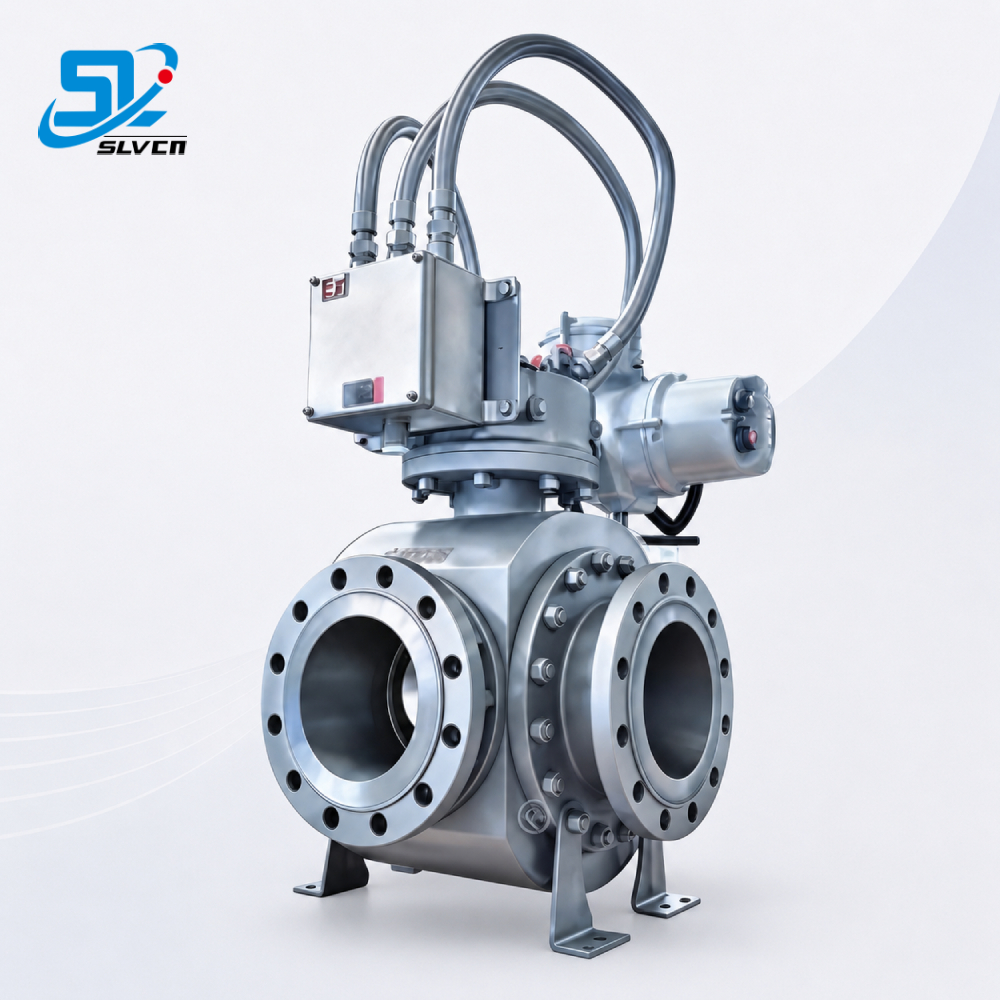
Our core product range covers forged trunnion-mounted and floating ball valves, top-entry and side-entry ball valves, fully welded ball valves, metal seated ball valves, cryogenic ball valves, high-pressure ball valves up to Class 2500 (PN420) and customized higher pressure ratings, as well as high-temperature service valves.
Compared with conventional cast valves, SLVCN forged valves feature higher material density, superior mechanical strength, improved resistance to pressure fluctuations and thermal shock, and significantly longer service life under severe service conditions.
Engineered to handle extreme differential pressures, abrasive shale gas particles, cryogenic liquid gas, and sour natural gas media across global networks.
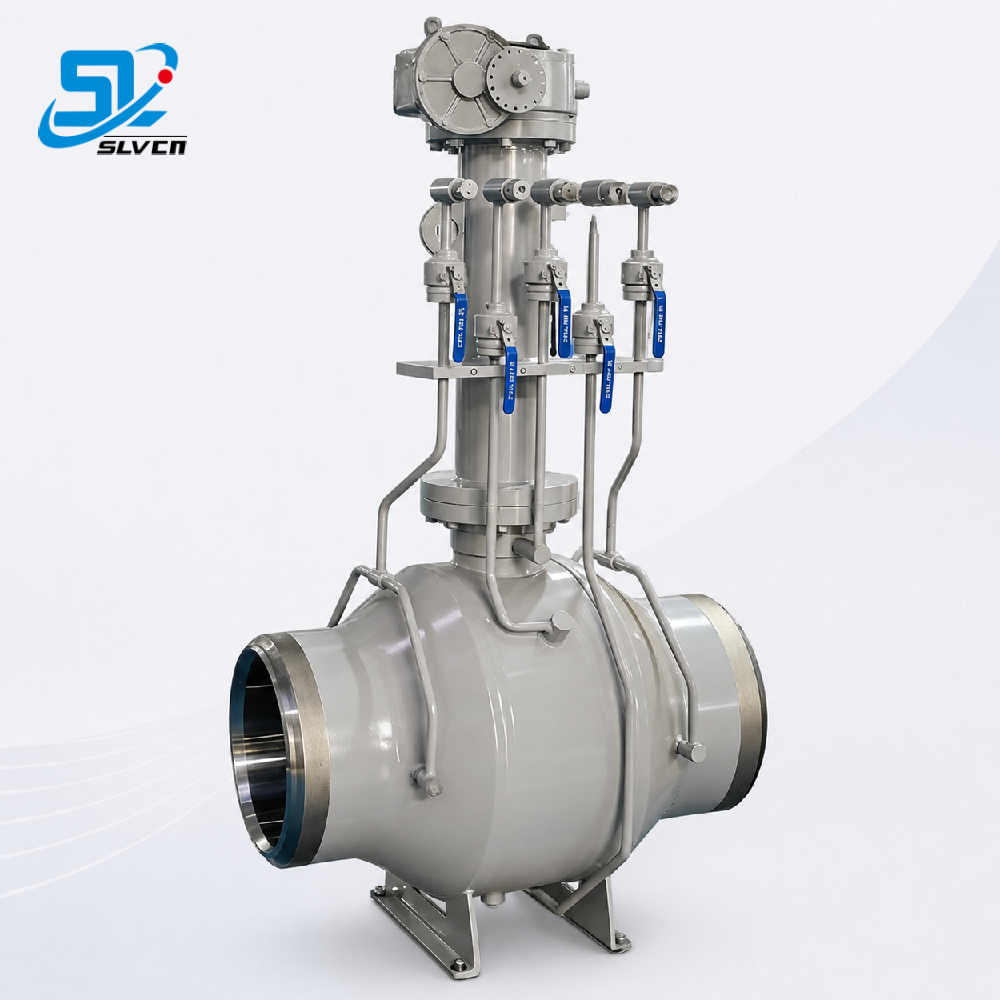
Strategically installed every 15 to 30 kilometers along cross-country gas trunklines. Fully welded gear-operated valves ensure reliable emergency line sectioning and complete isolation during pipeline maintenance or sudden pressure drops.
Compressor manifolds experience continuous cyclic vibrations and intense thermal fluctuations. Forged trunnion gear valves absorb pressure pulsations while providing absolute shut-off to protect high-value centrifugal turbine compressors.
High-cycle injection and withdrawal wells subject valves to bi-directional high-pressure flow carrying sand and moisture. Metal-seated gear valves with Tungsten Carbide (TC) coating withstand severe erosion and hydrate formation.
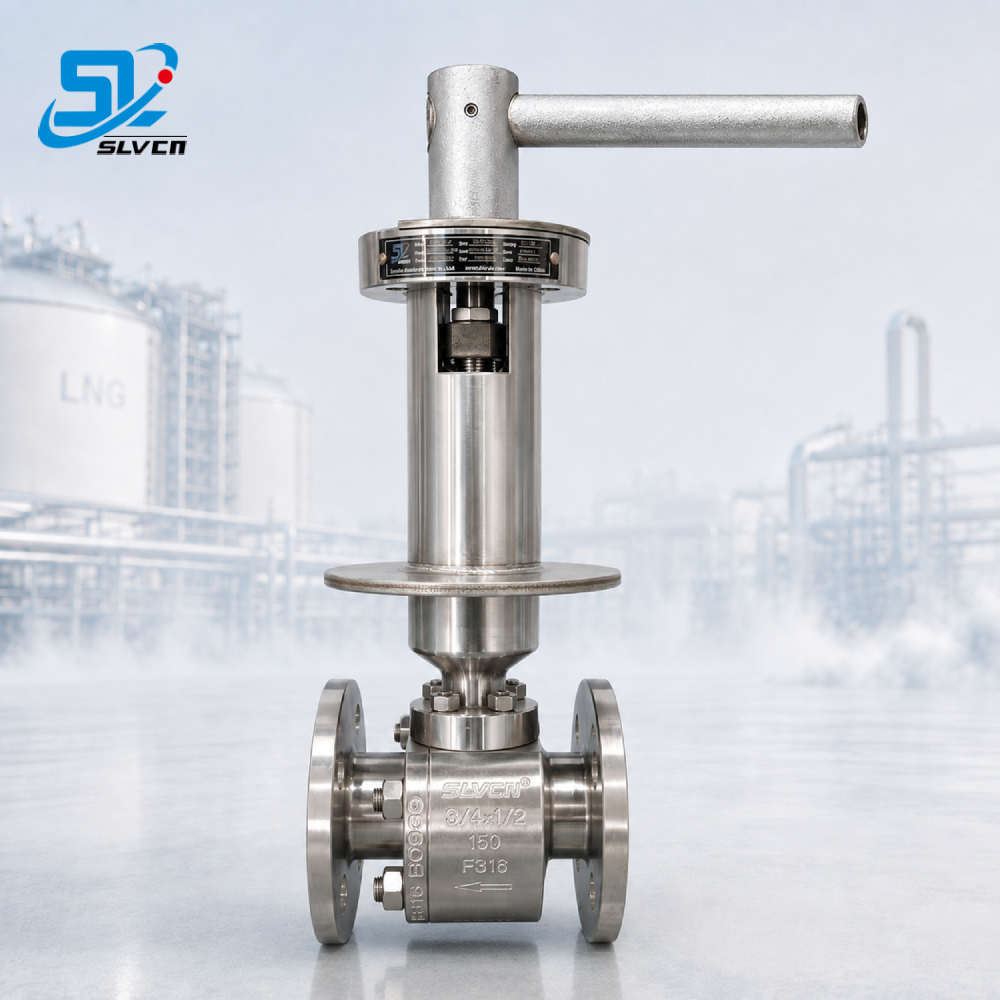
Designed with extended bonnets and specialized gas relief vapor columns, SLVCN cryogenic gear ball valves operate reliably down to -196°C, managing boil-off gas (BOG) and high-pressure LNG send-out headers.

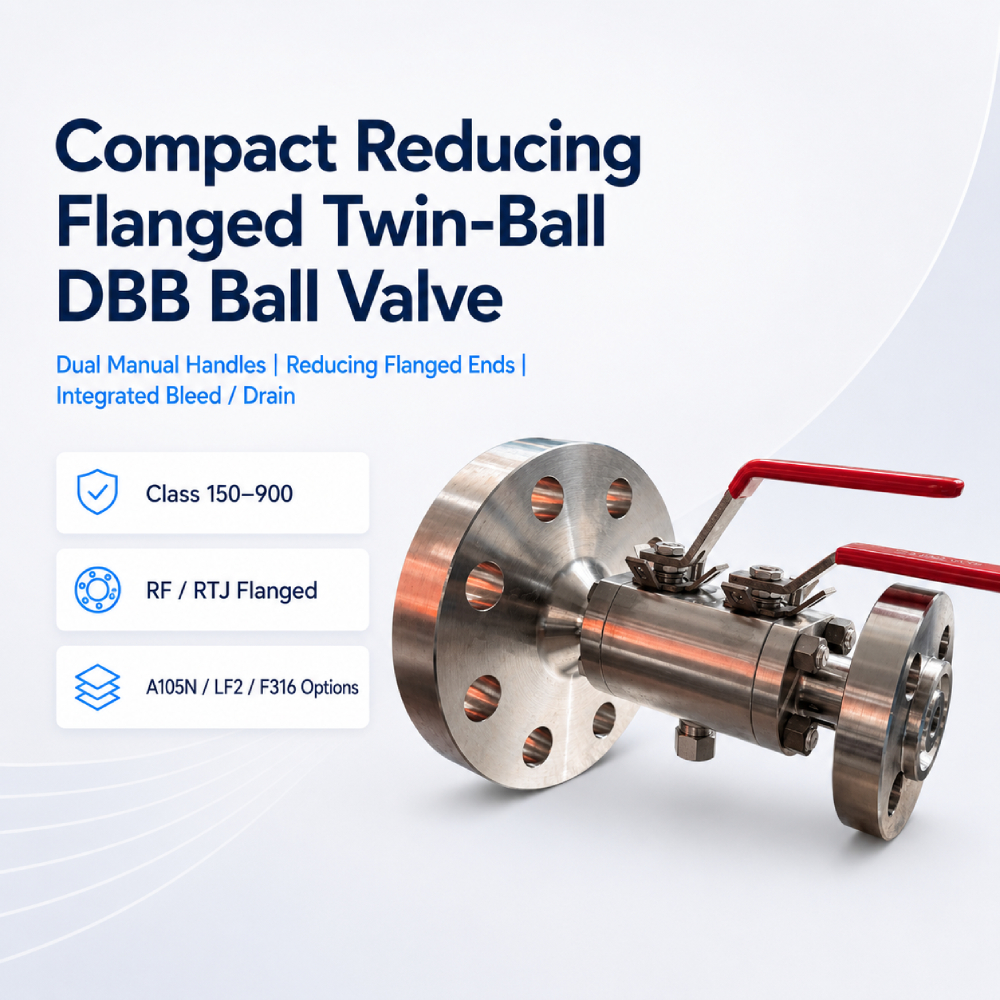
Safety and reliability are embedded in every design. Our forged ball valves are equipped with Double Block and Bleed (DBB) structures, anti-blowout stems, fire-safe designs in accordance with API 607 / API 6FA, anti-static devices, emergency sealing systems, and pressure-balanced seating structures suitable for high differential pressure operation.
Valves can be designed with Single Piston Effect (SPE) or Double Piston Effect (DPE) seat configurations based on application requirements. For sour service environments, materials and sealing systems comply with NACE MR0175 / ISO 15156 requirements.
Designed for High Pressure, High Temperature, and Cryogenic Applications, SLVCN valves are widely used in long-distance oil & gas transmission pipelines, LNG storage and regasification terminals, offshore platforms and deepwater projects, power plants, refineries, compressor stations, and high-pressure chemical processing units.
To ensure consistent quality, each valve undergoes a complete series of inspections and performance tests in accordance with API 6D, API 598, and ISO 5208, including shell test, seat leakage test (Rate A / zero visible leakage), fire-safe test, cryogenic test, operational torque test, dimensional inspection, and PMI material verification.
SLVCN is certified to ISO 9001, CE, and API standards, and our products comply with API 6D, ASME B16.34, DIN, ANSI, and JIS specifications. We provide extensive customization covering materials including A105, LF2, F11, F22, F51, and Inconel with intelligent actuation.


Years of Engineering Experience

With over 30 years of manufacturing experience, SLVCN is a professional designer and manufacturer of high-performance forged steel ball valves for critical industrial applications. We specialize in extreme working conditions including high pressure, high temperature, and cryogenic environments, providing safe and reliable flow control solutions for global industrial projects where operational reliability is non-negotiable.
Today, SLVCN serves customers in more than 100 countries and regions, supplying valves to EPC contractors, engineering companies, and end users across Europe, the Middle East, Southeast Asia, and the Americas. Backed by strong engineering expertise, advanced manufacturing, and rigorous quality control, SLVCN is committed to delivering safe, durable, and truly engineered valve solutions for the world’s most demanding industrial projects.
Contact Flow Control EngineersExplore our complete range of certified forged, trunnion-mounted, floating, cryogenic, and high-pressure ball valves designed for mission-critical industrial flow control.


 18061659285

