


Leave Your Message
High-performance forged steel gear ball valves engineered for critical industrial applications in Toronto and across North America.



With over 30 years of manufacturing experience, SLVCN is a professional designer and manufacturer of high-performance forged steel ball valves for critical industrial applications. We specialize in extreme working conditions including high pressure, high temperature, and cryogenic environments, providing safe and reliable flow control solutions for global industrial projects where operational reliability is non-negotiable.
As a trusted gear ball valve factory and manufacturer serving the Toronto market and the broader Canadian industrial sector, SLVCN delivers engineered valve solutions that meet the stringent requirements of North American energy infrastructure, petrochemical facilities, and municipal utilities.
Contact UsToronto and the Greater Toronto Area (GTA) represent one of Canada's most active industrial and energy hubs. The demand for high-performance gear ball valves continues to grow across multiple sectors.
Ontario's extensive pipeline network, connecting to major North American energy corridors, relies on precision gear-operated ball valves for mainline isolation, pressure regulation, and emergency shut-off. Toronto-based EPC contractors and pipeline operators specify API 6D-compliant trunnion-mounted ball valves for long-distance transmission projects.
With Canada's expanding LNG export capacity and Toronto's role as a logistics and engineering hub, cryogenic ball valves rated down to -196°C are in high demand. SLVCN's cryogenic gear ball valves are engineered for LNG storage, regasification terminals, and liquid nitrogen distribution systems operating in Ontario.
Toronto's power infrastructure — including natural gas peaking plants and combined-cycle facilities — demands high-temperature, high-pressure ball valves with gear actuators for reliable steam and fuel gas control. SLVCN's valves are rated for Class 600 to Class 2500 service in power plant applications.
The Hamilton–Toronto industrial corridor hosts numerous chemical processing facilities requiring corrosion-resistant ball valves in exotic materials (F51 duplex, Inconel) for handling aggressive media. SLVCN's NACE MR0175-compliant valves address sour service and high-chloride environments common in Ontario's chemical sector.
Toronto's municipal water treatment and distribution infrastructure increasingly adopts gear-operated ball valves for large-diameter isolation service. SLVCN supplies fully welded and flanged ball valves in sizes up to 36" for water utility projects across the GTA.
Northern Ontario's mining operations and Toronto-based engineering firms sourcing for resource sector projects require heavy-duty gear ball valves resistant to abrasion, slurry, and extreme pressure differentials. SLVCN's metal-seated ball valves deliver exceptional durability in these demanding environments.
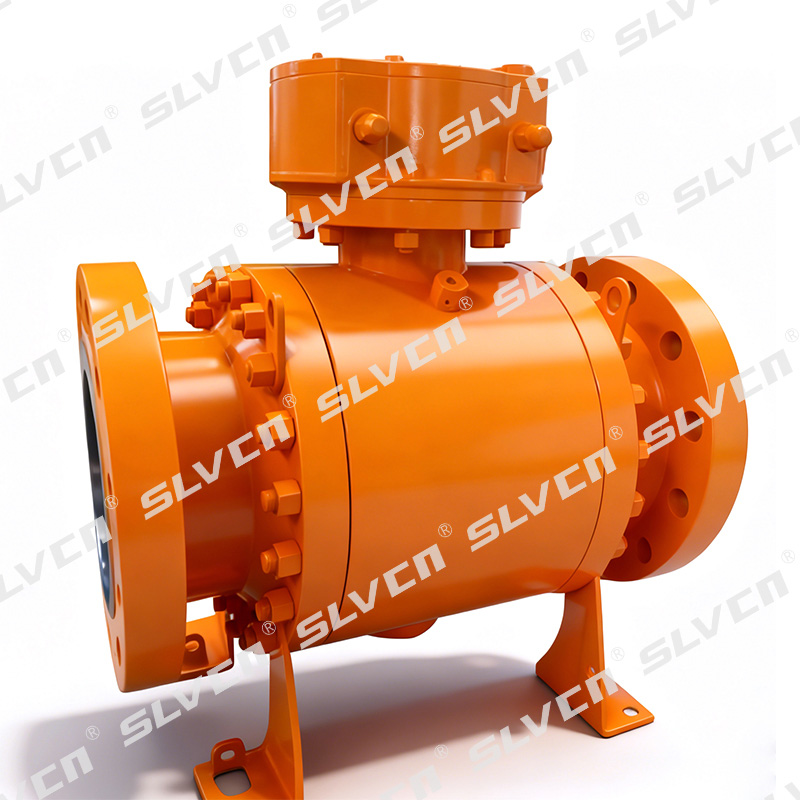
Our core product range covers forged trunnion-mounted and floating ball valves, top-entry and side-entry ball valves, fully welded ball valves, metal seated ball valves, cryogenic ball valves, high-pressure ball valves up to Class 2500 (PN420) and customized higher pressure ratings, as well as high-temperature service valves.
Compared with conventional cast valves, SLVCN forged valves feature higher material density, superior mechanical strength, improved resistance to pressure fluctuations and thermal shock, and significantly longer service life under severe service conditions.
The global and Canadian gear ball valve market is undergoing rapid transformation driven by energy transition, digitalization, and tightening safety regulations.
Toronto's industrial operators are increasingly adopting gear ball valves integrated with intelligent electric actuators, position sensors, and IIoT connectivity. Real-time valve monitoring, predictive maintenance, and remote operation are becoming standard requirements for new pipeline and plant projects in Ontario, reducing downtime and improving safety compliance.
Canada's national hydrogen strategy and Ontario's growing hydrogen economy are creating new demand for hydrogen-compatible gear ball valves. SLVCN's forged steel valves with enhanced sealing systems and anti-permeation designs are positioned to serve emerging hydrogen transmission and storage infrastructure in the Toronto region.
As oil & gas exploration moves into deeper and more challenging reservoirs, demand for Class 1500, Class 2500, and beyond pressure-rated gear ball valves is accelerating. SLVCN's capability to manufacture and test valves beyond Class 2500 positions us as a preferred supplier for Canada's offshore and high-pressure onshore projects.
Canadian regulatory bodies and international standards organizations are tightening fugitive emission requirements (ISO 15848, TA-Luft) and fire-safe performance standards. SLVCN proactively designs valves to exceed API 607, API 6FA, and low-emission packing requirements, ensuring compliance for Toronto-area operators facing increasing ESG scrutiny.
Toronto's engineering procurement contractors demand shorter lead times and greater customization flexibility. SLVCN's advanced manufacturing infrastructure supports rapid prototyping, special material procurement (Inconel, Hastelloy, duplex stainless), and expedited production schedules to meet tight project timelines in the competitive North American market.
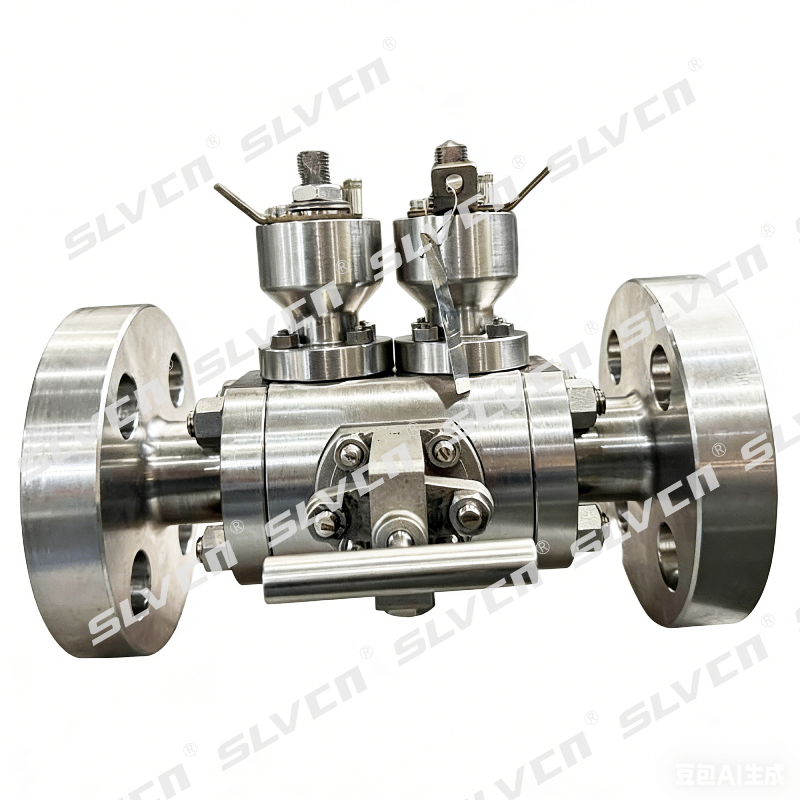
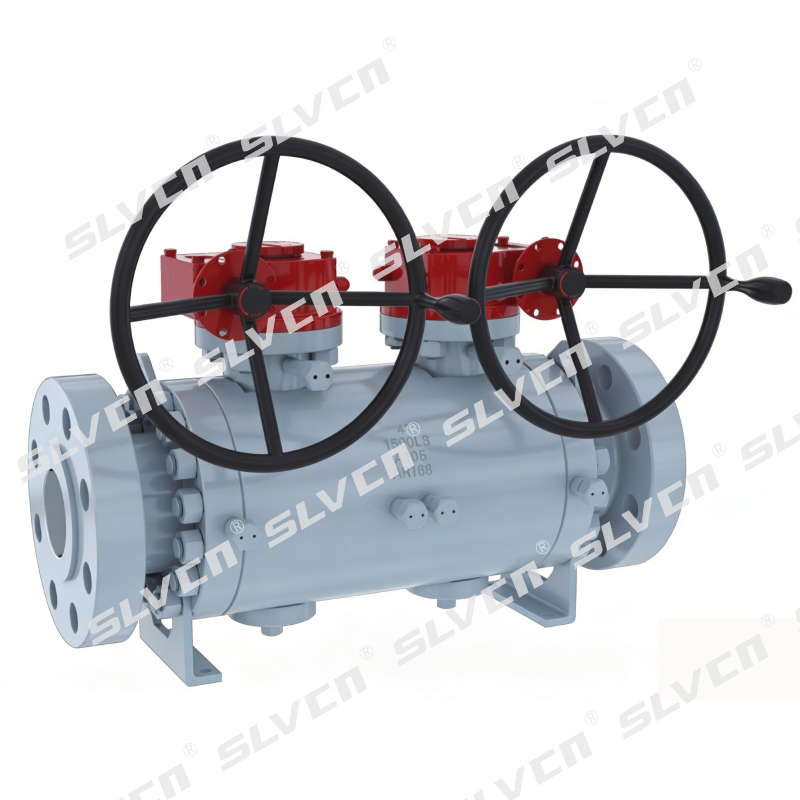
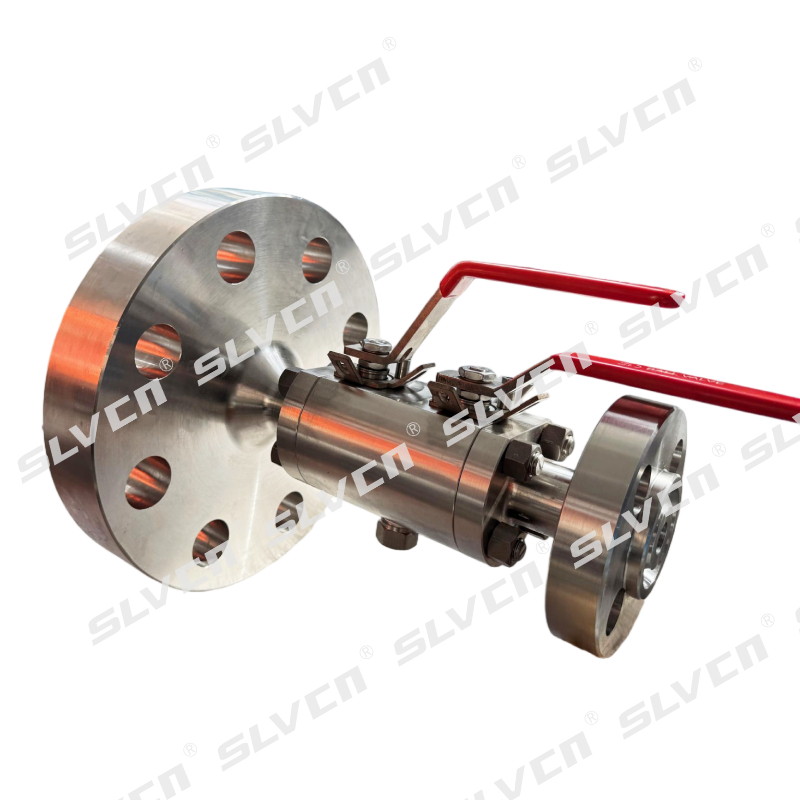
Double Block and Bleed (DBB) valve configurations are increasingly specified for new pipeline projects in Ontario to minimize process isolation risks and reduce fugitive emissions. SLVCN's integrated and twin-ball DBB trunnion-mounted ball valves with worm gear operators offer a compact, reliable solution for Toronto-area pipeline operators.
Designed for high-pressure mainline isolation in oil & gas transmission pipelines, SLVCN trunnion-mounted gear ball valves deliver bubble-tight shut-off and reliable long-term performance across Canada's extensive pipeline network.
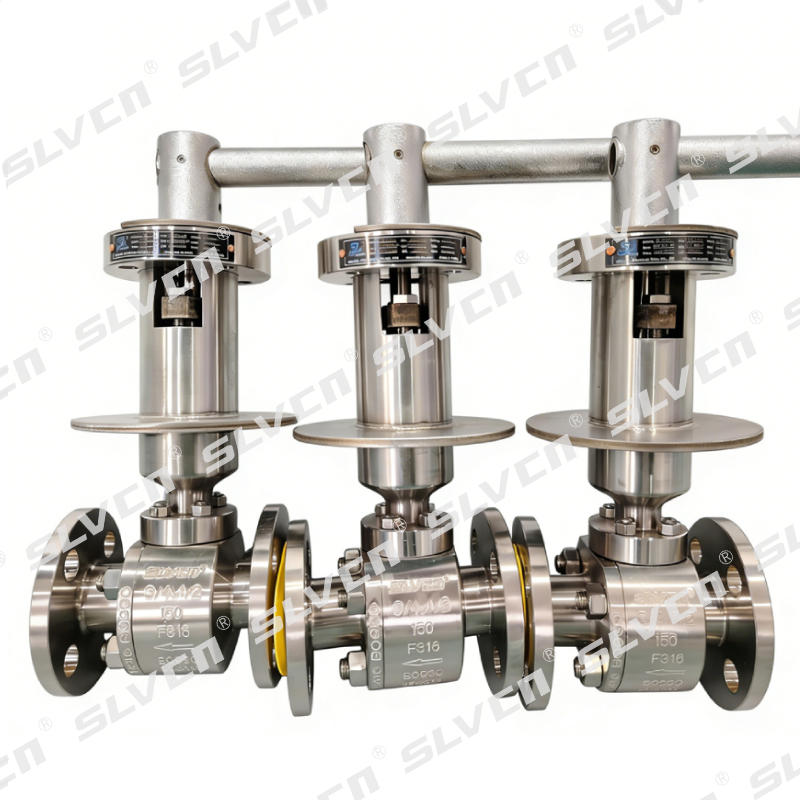
Cryogenic gear ball valves with extended bonnets and locking devices are engineered for LNG terminal service at temperatures down to -196°C, meeting the most stringent safety and performance standards for Canada's LNG export facilities.
Compact, corrosion-resistant forged ball valves with gear operators are designed for offshore platform service, with fire-safe certification (API 6FA) and anti-corrosion coatings suitable for marine environments.
Metal-seated and NACE-compliant gear ball valves handle corrosive, high-temperature, and sour service media in refinery and chemical processing environments, with material options including F11, F22, F51, and Inconel alloys.
High-pressure, high-cycle gear ball valves with pressure-balanced seating are specified for natural gas compressor stations, providing reliable isolation and blow-down capability under extreme differential pressure conditions.
High-temperature service gear ball valves rated for steam and hot water service are deployed in combined-cycle power plants, district heating systems, and industrial utility networks across the Toronto metropolitan area.


Safety and reliability are embedded in every design. Our forged ball valves are equipped with Double Block and Bleed (DBB) structures, anti-blowout stems, fire-safe designs in accordance with API 607 / API 6FA, anti-static devices, emergency sealing systems, and pressure-balanced seating structures suitable for high differential pressure operation.
Valves can be designed with SPE or DPE seat configurations based on application requirements. For sour service environments, materials and sealing systems comply with NACE MR0175 / ISO 15156 requirements — a critical specification for many Toronto-area oil sands and pipeline projects.
To ensure consistent quality, each valve undergoes a complete series of inspections and performance tests in accordance with API 6D, API 598, and ISO 5208, including shell test, seat leakage test (Rate A / zero visible leakage), fire-safe test, cryogenic test, operational torque test, dimensional inspection, and PMI material verification. SLVCN operates dedicated cryogenic testing facilities to validate valve performance at ultra-low temperatures down to −196°C.
SLVCN is certified to ISO 9001, CE, and API standards, and our products comply with API 6D, ASME B16.34, DIN, ANSI, and JIS specifications. We provide extensive customization capabilities covering sizes from 1/2" to 36", full bore or reduced bore, special materials including A105, LF2, F11, F22, F51, Inconel, various soft and metal seat designs, and intelligent actuation with pneumatic, electric, and gear operators — meeting the full spectrum of Toronto industrial project specifications.
Today, SLVCN serves customers in more than 100 countries and regions, supplying valves to EPC contractors, engineering companies, and end users across Europe, the Middle East, Southeast Asia, and the Americas. Backed by strong engineering expertise, advanced manufacturing, and rigorous quality control, SLVCN is committed to delivering safe, durable, and truly engineered valve solutions for the world's most demanding industrial projects.
For Toronto-based buyers, procurement managers, and engineering firms, SLVCN offers dedicated technical support, competitive lead times, full documentation packages (MTR, ITP, databook), and compliance with Canadian and North American project specifications. Our global supply chain and logistics capabilities ensure reliable delivery to Toronto, Hamilton, Calgary, Edmonton, and all major Canadian industrial centres.
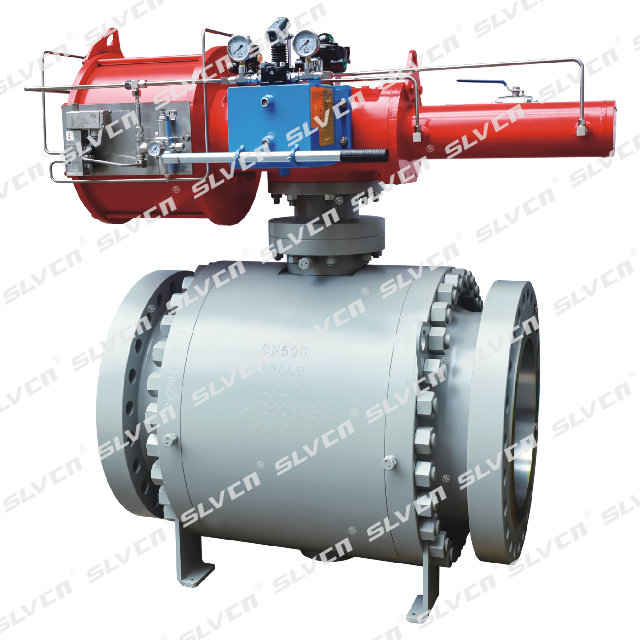
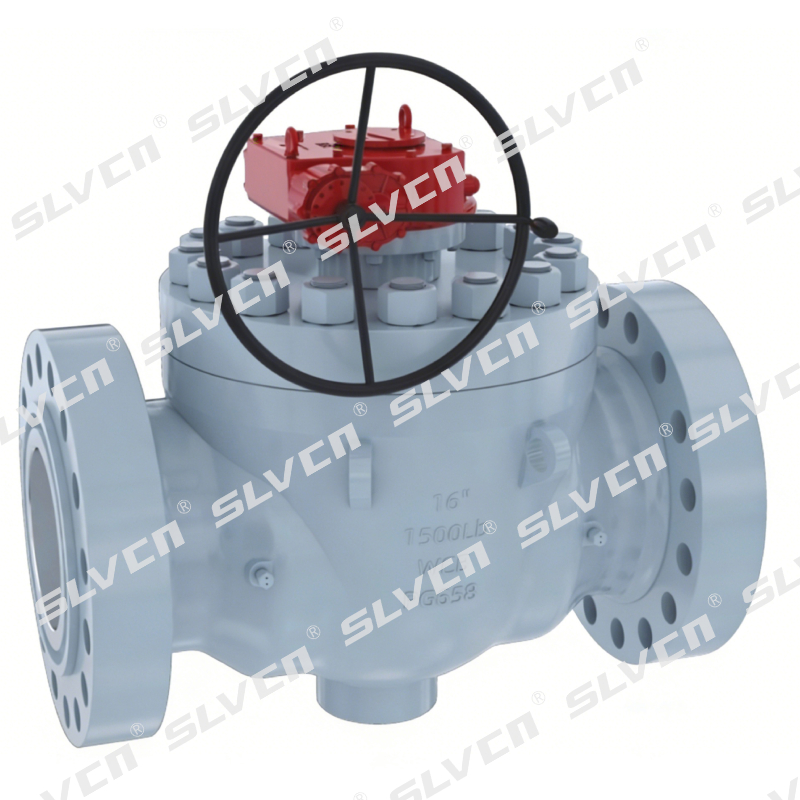
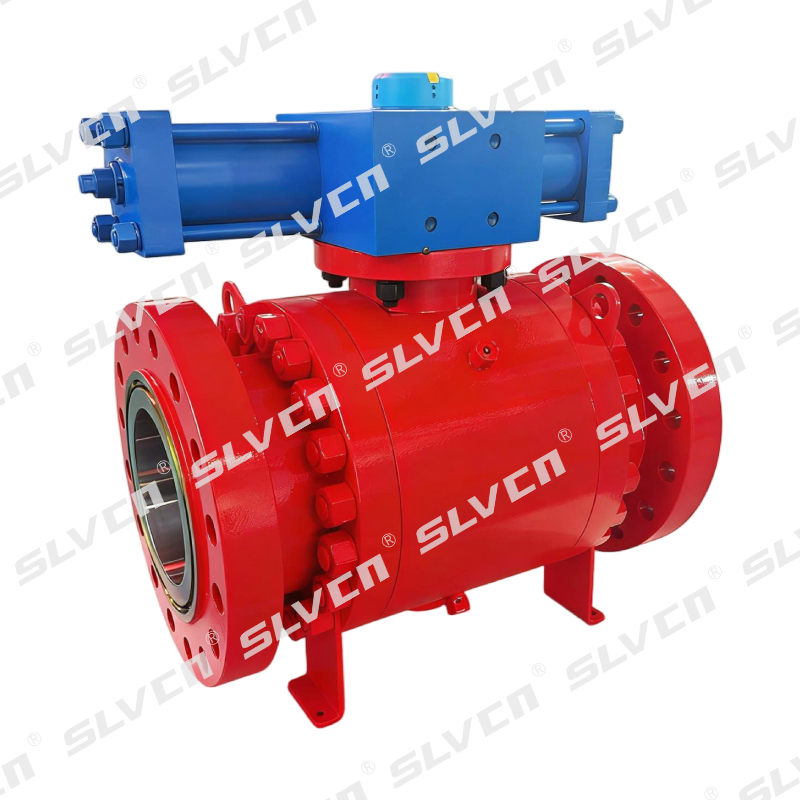
Explore our full range of forged steel ball valves, DBB valves, and actuated valve assemblies for every industrial application.
Get expert technical consultation, competitive pricing, and fast delivery for your next industrial valve project in Toronto, Ontario, and across Canada.
Contact Us Today


 +86 18913944686

