


Leave Your Message



With over 30 years of extensive manufacturing experience, SLVCN has evolved into a globally recognized professional designer and manufacturer of high-performance forged steel ball valves. Our commitment to engineering excellence makes us a premier supplier for critical industrial applications across Brazil and the broader South American continent.
Brazil’s rapidly expanding industrial landscape—from the ultra-deepwater pre-salt oil fields off the coast of Rio de Janeiro to the massive iron ore mining operations in Minas Gerais—demands equipment that can withstand extreme operational stresses. We specialize in extreme working conditions including high pressure, high temperature, and cryogenic environments. SLVCN provides safe, robust, and highly reliable flow control solutions tailored for localized Brazilian industrial projects where operational reliability is absolutely non-negotiable.
Brazil represents one of the most dynamic and challenging industrial environments globally. The unique geographical and operational conditions require specialized forged valves that exceed standard casting capabilities.

The discovery of the pre-salt layer (Camada do Pré-sal) in the Santos and Campos basins has revolutionized Brazil's energy sector. Extracting oil and gas from depths exceeding 2,000 meters beneath thick layers of salt involves unprecedented pressures and highly corrosive environments. Designed for High Pressure, High Temperature, and Cryogenic Applications, SLVCN forged valves are widely used in offshore platforms, FPSO (Floating Production Storage and Offloading) vessels, and deepwater subsea tie-backs. Our valves handle extreme differential pressures and sour service media (H₂S) effortlessly.
In mining hubs like Carajás and Minas Gerais, transporting highly abrasive iron ore slurry over hundreds of kilometers requires valves with exceptional structural integrity. Compared with conventional cast valves, SLVCN forged valves feature significantly higher material density and superior mechanical strength, preventing the micro-porosity issues that lead to catastrophic failures in high-vibration slurry pipelines.
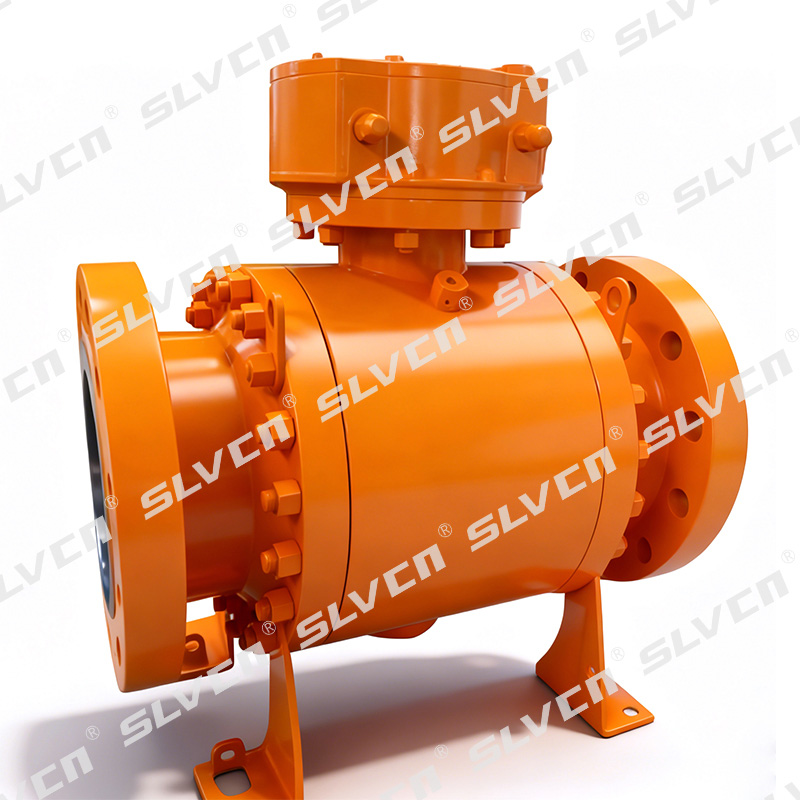
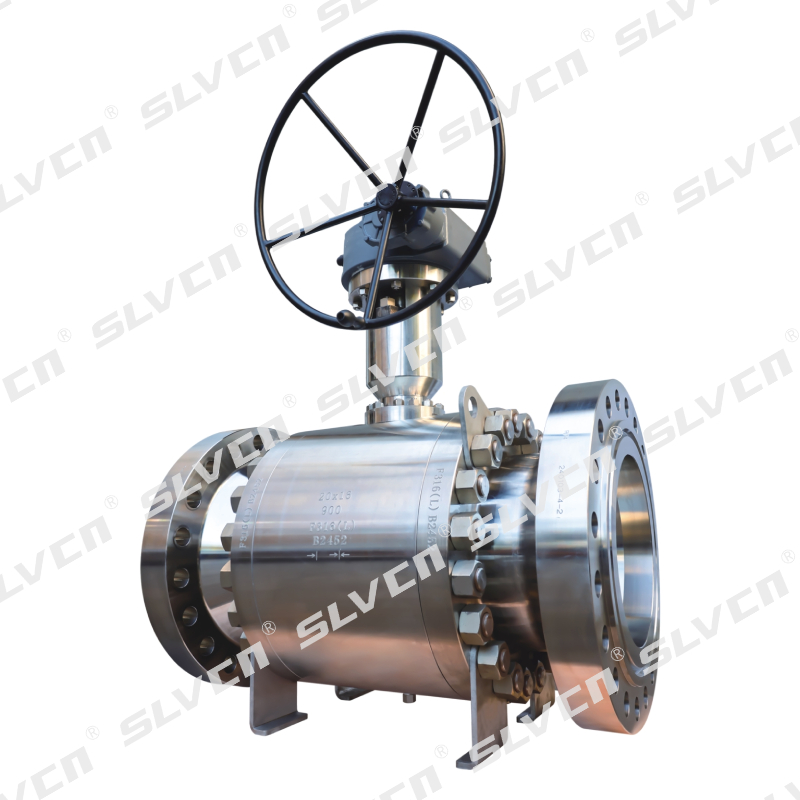
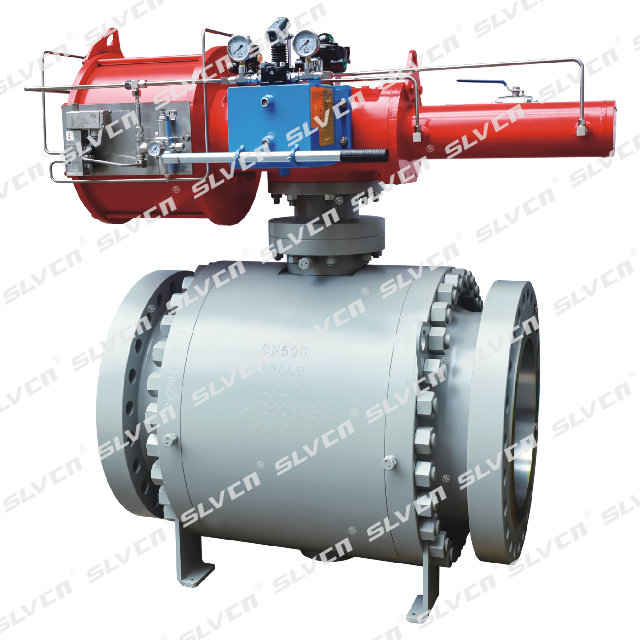
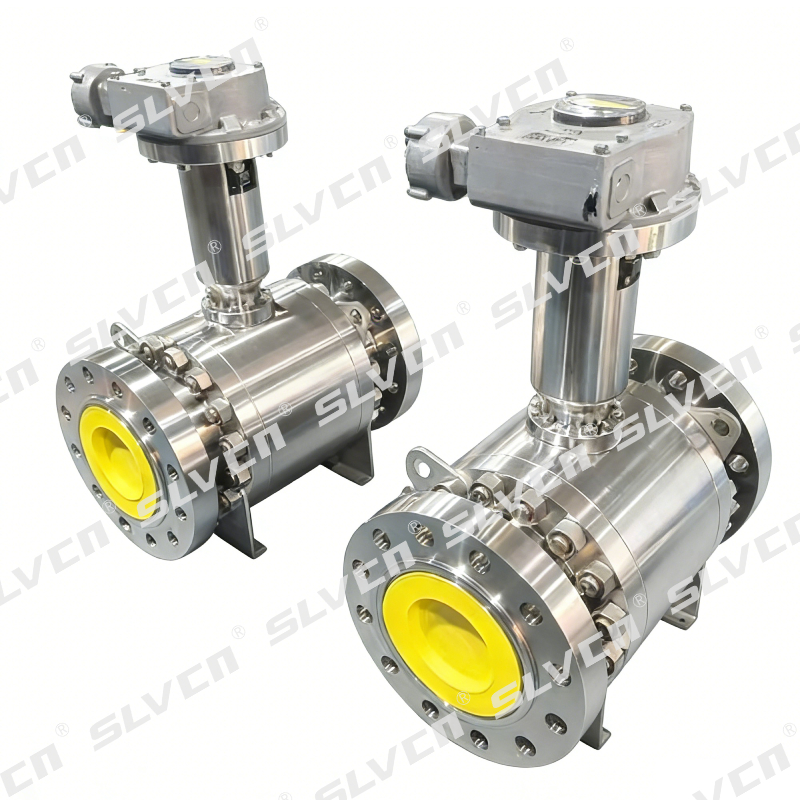
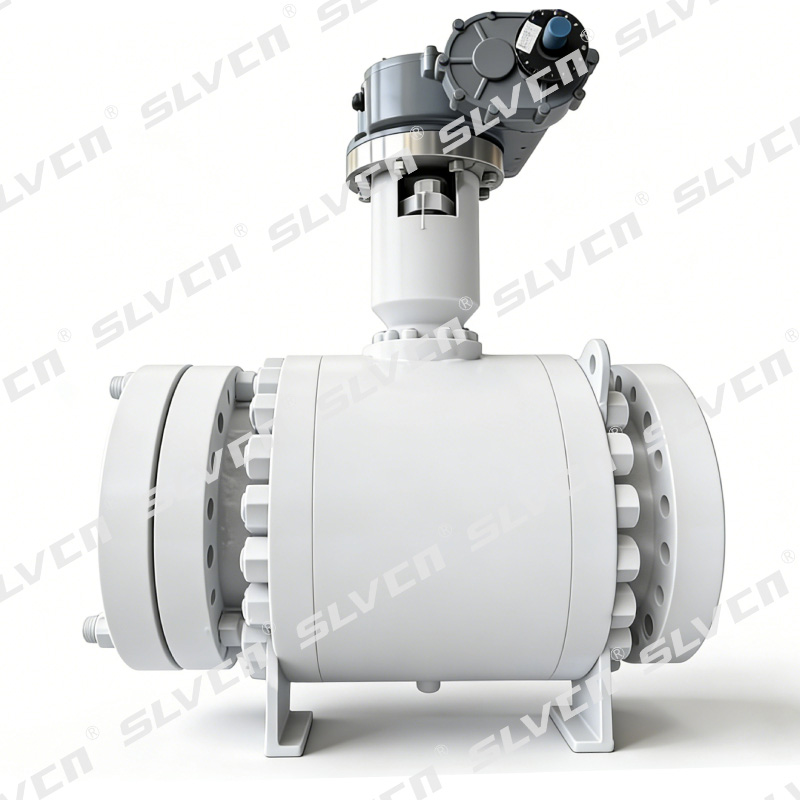
Our core product range covers forged trunnion-mounted and floating ball valves, top-entry and side-entry ball valves, fully welded ball valves, metal seated ball valves, and cryogenic ball valves. We engineer solutions for high-pressure applications up to Class 2500 (PN420) and offer customized higher pressure ratings, as well as high-temperature service valves specifically adapted to Brazil's stringent regulatory standards like NR-13.
Forged steel eliminates the hidden defects such as shrinkage, gas porosity, and inclusions often found in cast materials. This results in improved resistance to pressure fluctuations, thermal shock, and significantly longer service life under severe service conditions typical in Brazilian refineries like REPLAN and RNEST.
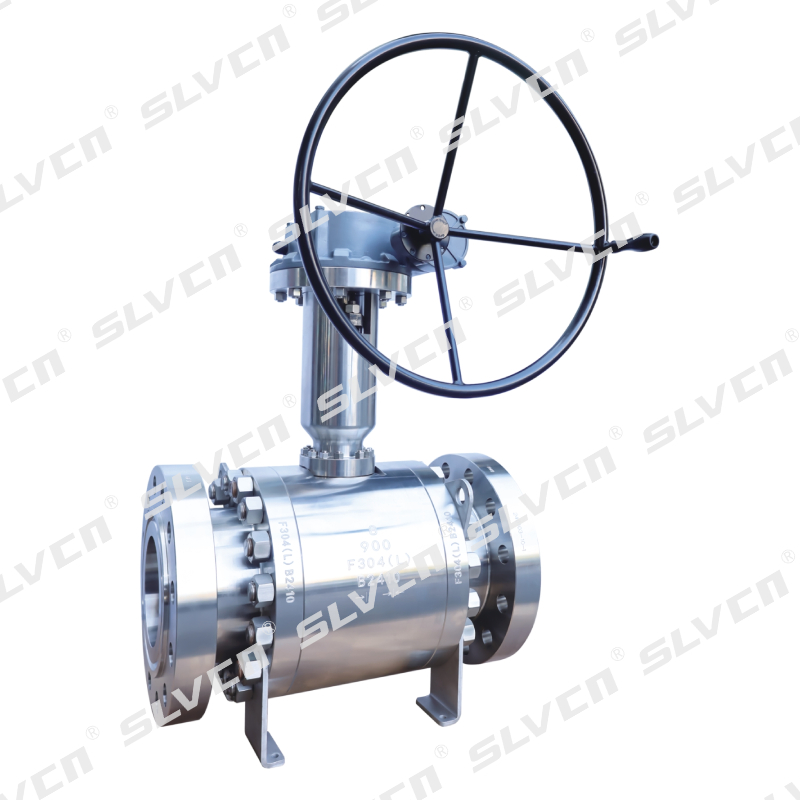
With Brazil expanding its natural gas infrastructure through LNG storage and regasification terminals in Baía de Todos os Santos and Pecém, our cryogenic valves ensure bubble-tight shut-off. We operate dedicated cryogenic testing facilities to validate valve performance at ultra-low temperatures down to −196°C.
Whether handling flammable media, corrosive fluids, or ultra-low temperatures, our valves ensure stable operation and maximum system safety. Valves can be designed with Single Piston Effect (SPE) or Double Piston Effect (DPE) seat configurations based on specific pipeline application requirements.
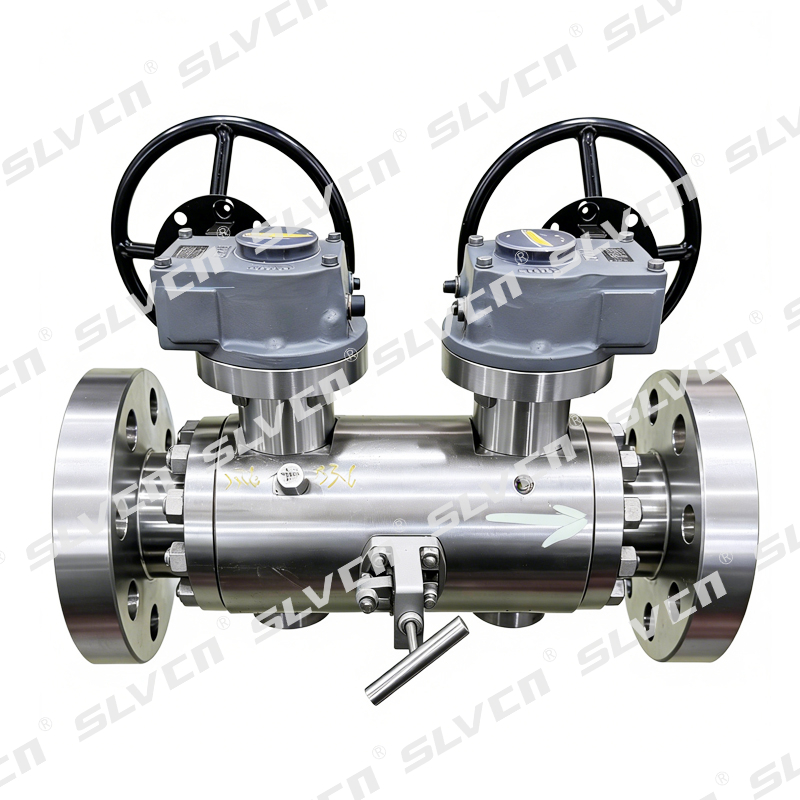
Safety and reliability are embedded in every design. As Brazil's environmental agency (IBAMA) implements stricter regulations on fugitive emissions, SLVCN is at the forefront of the industry trend. Our forged ball valves are equipped with Double Block and Bleed (DBB) structures, anti-blowout stems, fire-safe designs in accordance with API 607 / API 6FA, anti-static devices, emergency sealing systems, and pressure-balanced seating structures suitable for high differential pressure operation.
Furthermore, the Brazilian energy transition—highlighted by the booming sugarcane ethanol industry in São Paulo and emerging green hydrogen projects—demands intelligent flow control. We provide extensive customization capabilities including intelligent actuation with pneumatic, electric, and gear operators, ready for integration into automated, digitalized plant control systems. For sour service environments, our materials and sealing systems strictly comply with NACE MR0175 / ISO 15156 requirements.

To ensure consistent quality for the Brazilian market, each valve undergoes a complete series of rigorous inspections and performance tests in accordance with international standards.
Our testing protocols exceed standard requirements. We conduct tests in accordance with API 6D, API 598, and ISO 5208. This includes high-pressure shell tests, seat leakage tests (Rate A / zero visible leakage), fire-safe tests, operational torque tests, strict dimensional inspections, and Positive Material Identification (PMI) verification to guarantee the metallurgical integrity of every forged component sent to Brazil.
SLVCN is certified to ISO 9001, CE, and API standards, and our products comply with API 6D, ASME B16.34, DIN, ANSI, and JIS specifications. We provide extensive customization capabilities covering sizes from 1/2” to 36”, full bore or reduced bore, and special materials including A105, LF2, F11, F22, F51, and Inconel, ensuring perfect compatibility with local Brazilian piping systems.
Today, SLVCN serves customers in more than 100 countries and regions. We supply premium forged valves to major EPC contractors, engineering companies, and end users across Europe, the Middle East, Southeast Asia, and the Americas. With a strong focus on the rapidly developing South American market, specifically Brazil, SLVCN is backed by strong engineering expertise, advanced manufacturing capabilities, and rigorous quality control. We are deeply committed to delivering safe, durable, and truly engineered valve solutions for the world’s most demanding industrial projects.


 +86 18905154687