


Leave Your Message
Engineered for high-differential pressure, rapid actuation, and absolute sealing integrity in severe cryogenic oxidizer service.
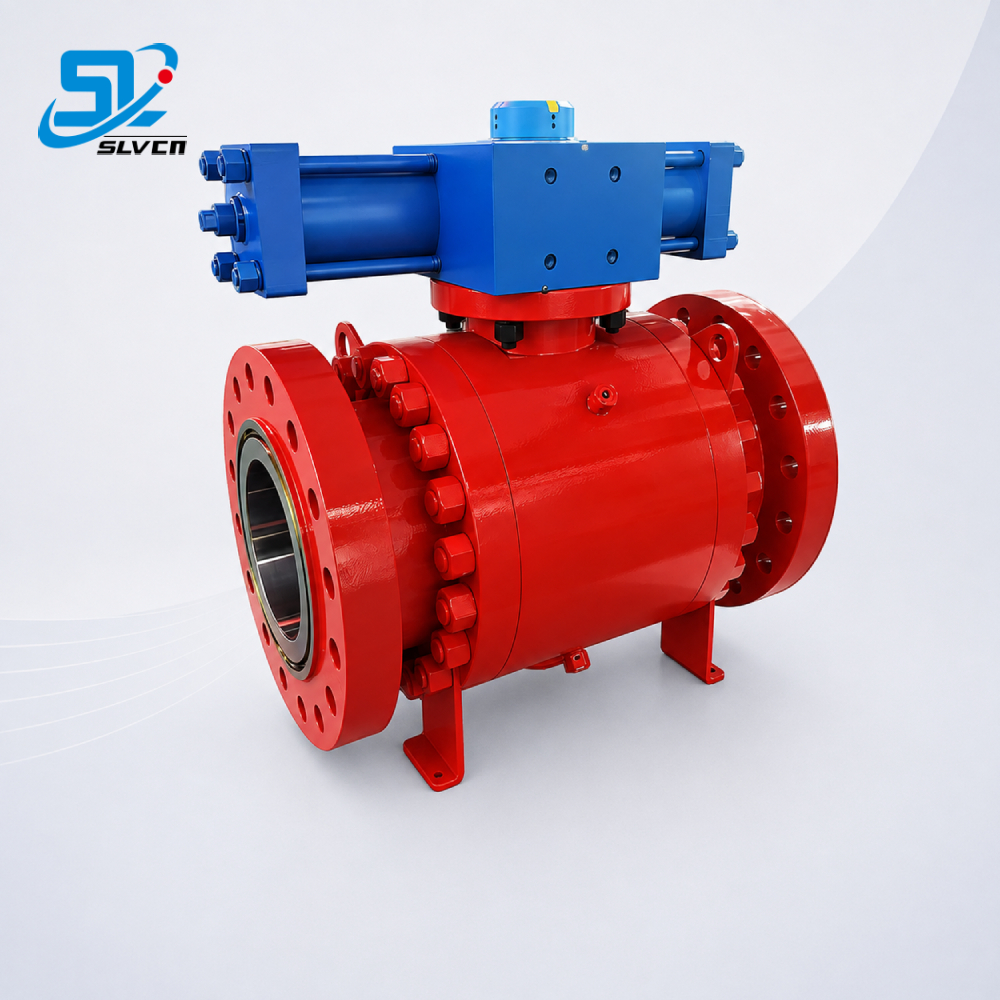
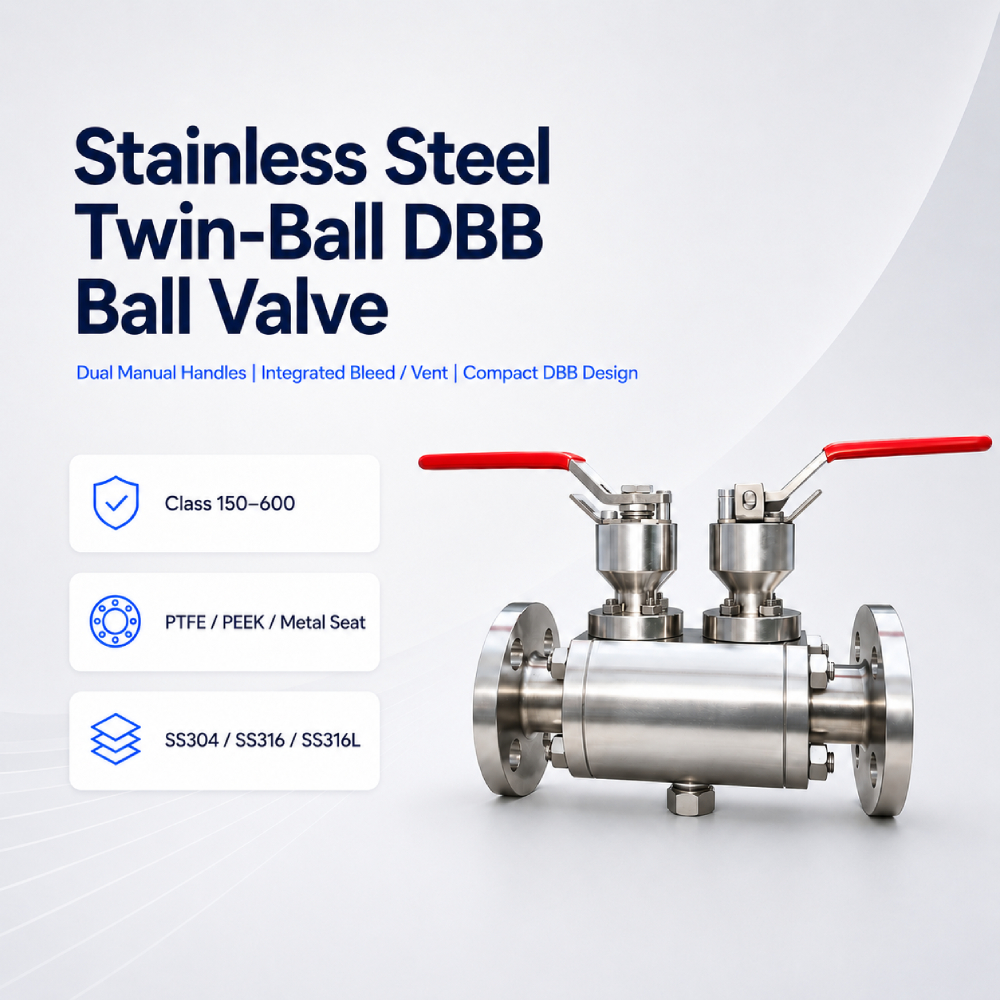
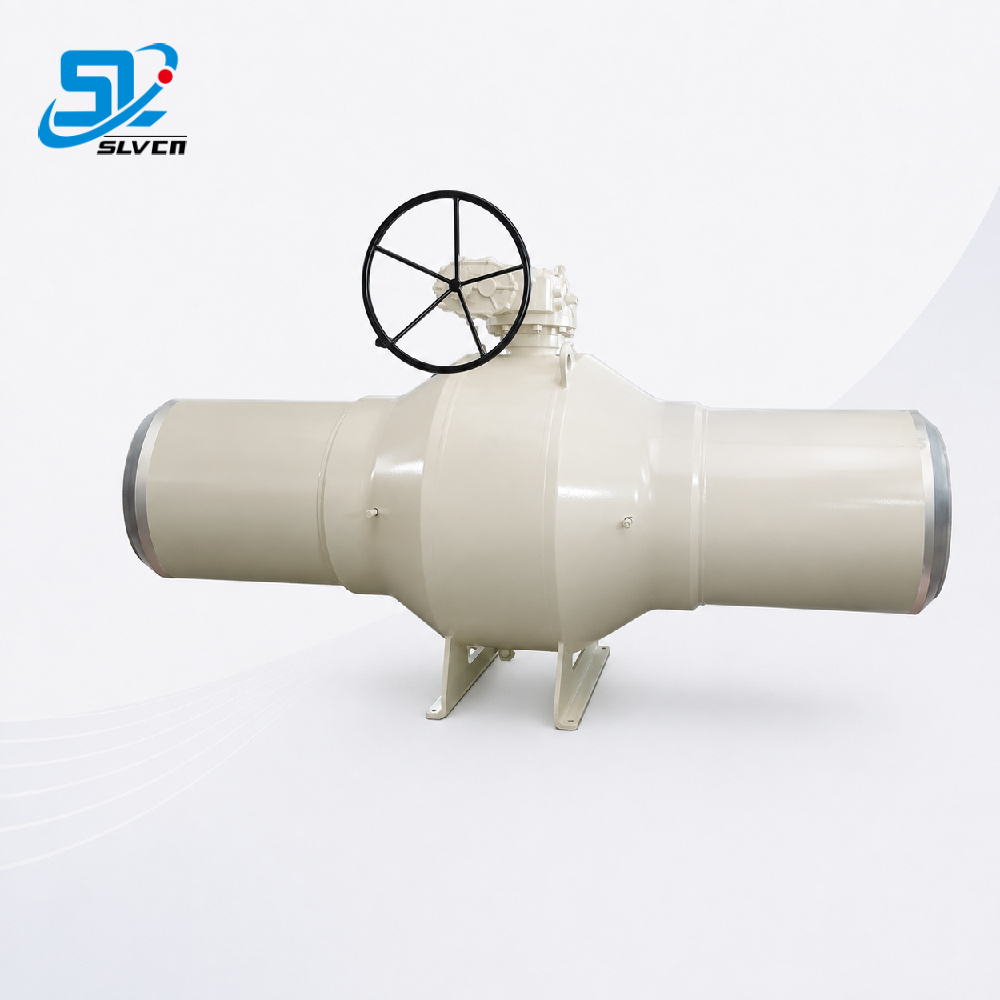
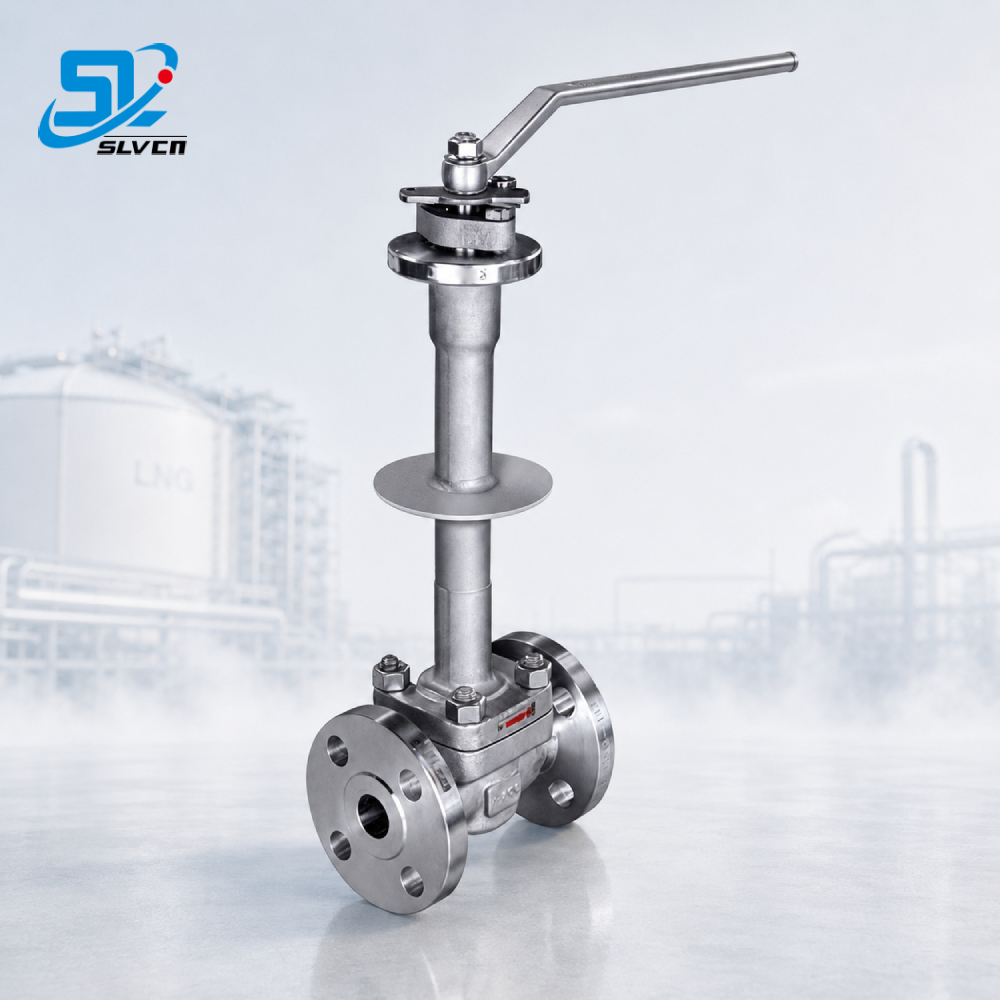
The modern aerospace and commercial launch vehicle ecosystem is experiencing an unprecedented surge driven by orbital mega-constellations, deep space lunar exploration (such as NASA's Artemis initiative), and rapid commercial launch cadences. Liquid Oxygen (LOX, with a normal boiling point of −182.96°C / 90.19 K) serves as the primary oxidizer for the vast majority of liquid-propellant rocket engines, paired alongside liquid methane (Methalox), RP-1 kerosene, or liquid hydrogen (Hydrolox).
Handling liquid oxygen at extreme pressures—ranging from ambient transfer lines up to 6000 PSI high-pressure pre-burner feed systems and umbilical disconnect manifolds—presents unforgiving engineering hurdles. While conventional cast ball valves are susceptible to micro-porosity, crystalline micro-fissures, and brittle fracture at cryogenic temperatures, forged ball valves have emerged as the mandated standard for aerospace ground support equipment (GSE), mobile launch platforms, and rocket propulsion testing facilities.
Forging grain flow alignment delivers uniform grain structures that eliminate sub-surface defects, offering exceptional fracture toughness and superior resistance to structural failure under thermal shock during rapid LOX chill-down sequences.

Liquid oxygen environments present severe fire and rapid combustion hazards. SLVCN forged valves undergo multi-stage precision degreasing, solvent ultrasonic cleaning, and ultraviolet blacklight inspection to ensure non-volatile residue (NVR) levels under Level A/B cleanliness specifications.
Trapped liquid oxygen in a closed valve cavity can expand up to 860 times its liquid volume upon ambient boil-off. Our forged designs incorporate automatic cavity pressure relief systems (Single Piston Effect seats or drilled ball equalization holes) to avoid explosive overpressurization.
In accordance with BS 6364 and MSS SP-134, an extended vapor column positions the stem packing seals away from the cryogenic fluid. The formed boil-off gas buffer ensures the packing maintains ambient elasticity, eliminating cryogenic gland freezing and stem leakage.
From launch pad quick-disconnect umbilicals to high-mass flow engine static fire testing, forged valves provide the reliability required for critical launch timelines.
During the terminal launch countdown, thousands of gallons of LOX are pumped at high velocity to the launch vehicle tanks. Forged trunnion ball valves control the rapid pre-chill, bulk fill, replenish, and close-loop bleed operations. Their full-bore hydraulic efficiency minimizes pressure drop and boiling vapor cavitation.
Rocket propulsion development requires thousands of seconds of engine test runs where valves withstand extreme cyclical vibration, cryogenic shock, and rapid shut-down cycles. Fast-acting Scotch Yoke pneumatic and hydraulic actuators execute 90-degree valve stroking in sub-second timeframes to safely abort firings during anomalies.
Extended stem, top-entry, and fully welded forged ball valves are welded directly into vacuum-jacketed cryogenic vacuum lines to achieve maximum thermal insulation and eliminate potential flange leak paths across the spaceport network.

| Parameter | Aerospace LOX Handling Standard | Engineering Benefit for Spaceport GSE |
|---|---|---|
| Nominal Body Material | Forged ASTM A182 F316/F316L, Monel 400/K500, Inconel 718 | Eliminates structural brittle transition; highly resistant to oxygen particle impact ignition. |
| Operating Temperature | −196°C to +120°C (−320°F to +248°F) | Withstands liquid nitrogen chill-down, liquid oxygen loading, and ambient purge cycles. |
| Pressure Rating | ASME Class 150 to Class 2500 (PN20 to PN420 / up to 6000 PSI) | Supports low-pressure bulk bunkering up to extreme-pressure gas pressurization feed systems. |
| Seat & Sealing System | Kel-F (PCTFE), Virgin PTFE, or Stellite/Tungsten Carbide Metal-to-Metal | Resilient cryogenic bubble-tight shut-off without polymer cracking or seat distortion. |
| Stem Packing & Seals | Multi-ring V-Pack PTFE with Inconel/Elgiloy Spring Energizer | Compensates for thermal expansion differences; maintains fugitive emission tightness. |
| Safety & Testing Codes | API 6D, API 598, BS 6364, API 607 / API 6FA, ISO 15848 | Fully validated fire-safe, cryogenic leak tested with helium mass spectrometer protocols. |

Over 30 years of manufacturing experience in high-performance forged steel valves
About Us: With over 30 years of manufacturing experience, SLVCN is a professional designer and manufacturer of high-performance forged steel ball valves for critical industrial applications. We specialize in extreme working conditions including high pressure, high temperature, and cryogenic environments, providing safe and reliable flow control solutions for global industrial projects where operational reliability is non-negotiable.
Core Product: Our core product range covers forged trunnion-mounted and floating ball valves, top-entry and side-entry ball valves, fully welded ball valves, metal seated ball valves, cryogenic ball valves, high-pressure ball valves up to Class 2500 (PN420) and customized higher pressure ratings, as well as high-temperature service valves. Compared with conventional cast valves, SLVCN forged valves feature higher material density, superior mechanical strength, improved resistance to pressure fluctuations and thermal shock, and significantly longer service life under severe service conditions.
Severe Service Capability: Designed for High Pressure, High Temperature, and Cryogenic Applications, SLVCN valves are widely used in long-distance oil & gas transmission pipelines, LNG storage and regasification terminals, offshore platforms and deepwater projects, power plants, refineries, compressor stations, and high-pressure chemical processing units. Whether handling flammable media, corrosive fluids, sour service media (H₂S), ultra-low temperatures, or extreme differential pressures, our valves ensure stable operation, bubble-tight shut-off, and maximum system safety in accordance with international sealing and performance standards.


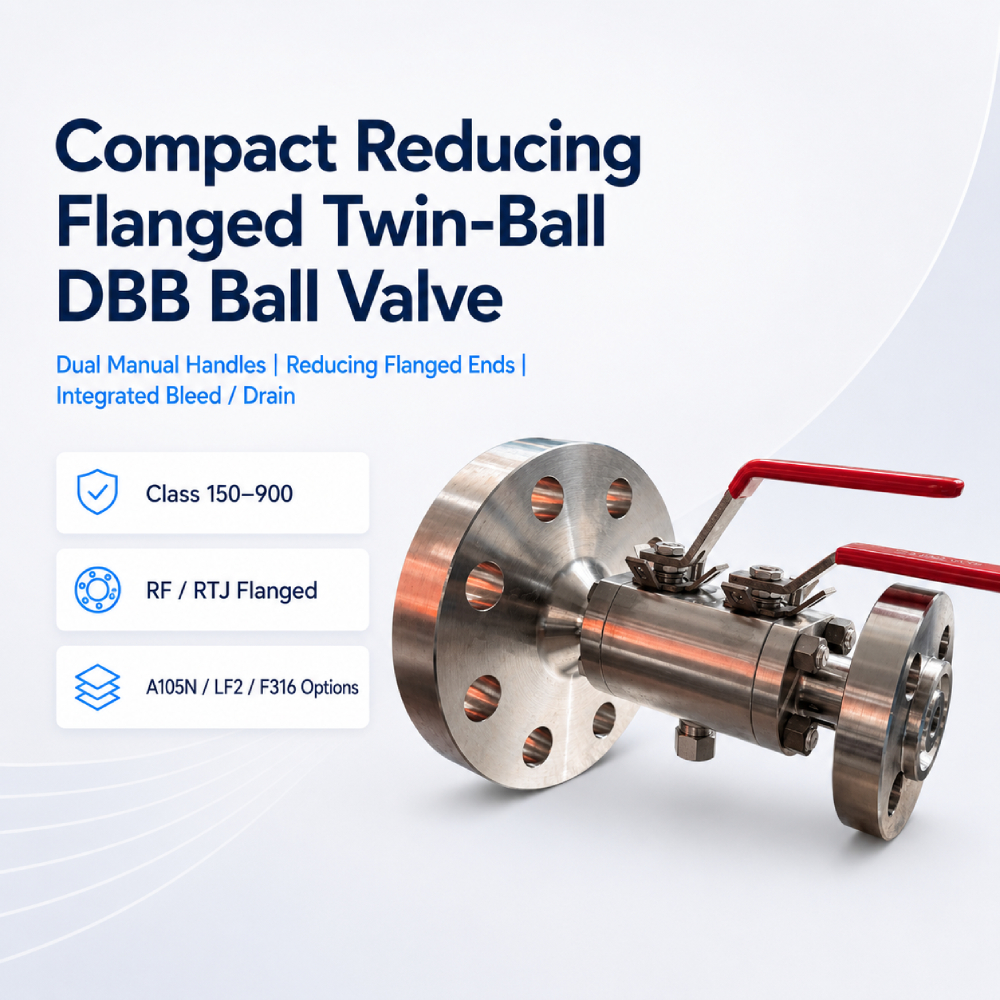
Safety and reliability are embedded in every design. Our forged ball valves are equipped with Double Block and Bleed (DBB) structures, anti-blowout stems, fire-safe designs in accordance with API 607 / API 6FA, anti-static devices, emergency sealing systems, and pressure-balanced seating structures suitable for high differential pressure operation. Valves can be designed with SPE or DPE seat configurations based on application requirements. For sour service environments, materials and sealing systems comply with NACE MR0175 / ISO 15156 requirements.
To ensure consistent quality, each valve undergoes a complete series of inspections and performance tests in accordance with API 6D, API 598, and ISO 5208, including shell test, seat leakage test (Rate A / zero visible leakage), fire-safe test, cryogenic test, operational torque test, dimensional inspection, and PMI material verification. SLVCN operates dedicated cryogenic testing facilities to validate valve performance at ultra-low temperatures down to −196°C.
SLVCN is certified to ISO 9001, CE, and API standards, and our products comply with API 6D, ASME B16.34, DIN, ANSI, and JIS specifications. We provide extensive customization capabilities covering sizes from 1/2” to 36”, full bore or reduced bore, special materials including A105, LF2, F11, F22, F51, Inconel, various soft and metal seat designs, and intelligent actuation with pneumatic, electric, and gear operators.
Today, SLVCN serves customers in more than 100 countries and regions, supplying valves to EPC contractors, engineering companies, and end users across Europe, the Middle East, Southeast Asia, and the Americas. Backed by strong engineering expertise, advanced manufacturing, and rigorous quality control, SLVCN is committed to delivering safe, durable, and truly engineered valve solutions for the world’s most demanding industrial projects.
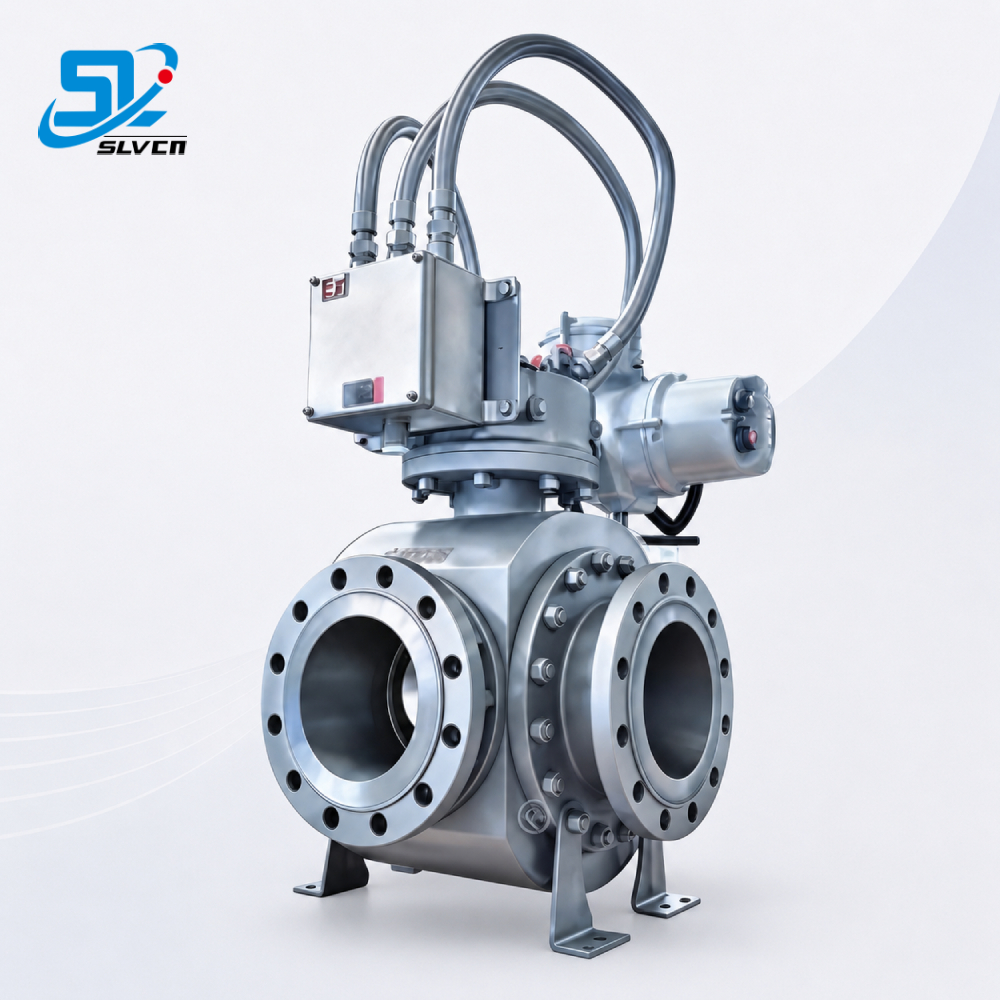
Explore our certified product line of trunnion-mounted, floating, fully welded, and DBB valve configurations engineered for extreme industrial and cryogenic service.


 18061659285

