


Leave Your Message
High-Performance Valves Designed for Canadian Industrial Applications
Canada's diverse industrial infrastructure presents unique challenges and opportunities for floating ball valve applications. From the oil sands operations in Alberta to the petrochemical facilities in Sarnia, Ontario, and the LNG terminals in British Columbia, Canadian industries demand valve solutions that can withstand extreme temperature variations, harsh environmental conditions, and rigorous operational requirements.
The Canadian valve market is characterized by stringent safety standards, compliance with CSA (Canadian Standards Association) requirements, and a growing emphasis on environmental protection. Floating ball valves play a critical role in flow control applications across oil and gas transmission, mining operations, pulp and paper production, hydroelectric power generation, and municipal water treatment facilities throughout the country.
With Canada's commitment to energy security and infrastructure modernization, the demand for high-quality, reliable floating ball valves continues to grow. Industries require valves that can perform consistently in temperatures ranging from -50°C in northern operations to high-temperature applications in refining processes, making material selection and design engineering crucial factors for Canadian applications.
Specialized Floating Ball Valve Solutions for Diverse Canadian Operations
Critical flow control in SAGD operations, bitumen processing, and heavy oil extraction facilities across Alberta's oil sands region, requiring valves resistant to abrasive slurries and high temperatures.
High-pressure gas processing, sour gas handling, and pipeline distribution systems throughout Western Canada, demanding NACE-compliant materials and fire-safe designs.
LNG liquefaction facilities in BC, cryogenic storage terminals, and regasification units requiring valves capable of operating at temperatures down to -196°C with zero leakage.
Hydroelectric facilities, thermal power plants, and nuclear stations across provinces like Quebec, Ontario, and Manitoba, requiring reliable isolation and control valves.
Potash mines in Saskatchewan, copper and gold operations in BC and Ontario, and iron ore facilities in Quebec and Labrador, handling corrosive and abrasive process fluids.
Refineries in Edmonton, Montreal, and Sarnia processing crude oil into fuels and chemicals, requiring high-performance valves for critical process control applications.
Canada's commitment to net-zero emissions by 2050 is driving investment in carbon capture, utilization, and storage (CCUS) projects. Floating ball valves are essential in CO₂ compression, transportation, and injection systems. Alberta's carbon trunk line and emerging hydrogen production facilities require specialized valves capable of handling high-purity gases and supercritical CO₂ conditions.
British Columbia's LNG Canada project and other proposed facilities represent billions in infrastructure investment. These projects demand large quantities of cryogenic-rated floating ball valves for liquefaction trains, storage tanks, and loading terminals. The extreme cold climate and seismic considerations of BC's coast require valves with enhanced material specifications and extended stem designs.
Aging pipeline infrastructure across Canada is undergoing systematic upgrades to meet modern safety standards. The Trans Mountain Expansion, Enbridge Line 3 replacement, and other pipeline projects require thousands of high-integrity isolation valves. Regulatory emphasis on leak detection, emergency shutdown systems, and automated valve actuation is driving demand for advanced ball valve technologies with remote monitoring capabilities.
Canadian industrial environments present unique challenges that standard valve designs may not adequately address. SLVCN's floating ball valves are specifically engineered to meet the demanding requirements of Canadian operations, incorporating design features and material selections that ensure reliable performance across the country's diverse climate zones and industrial applications.
Our valves undergo rigorous cold temperature testing to validate performance in Canada's harsh winters, where ambient temperatures can drop below -40°C. Extended bonnet designs provide additional thermal insulation for buried pipeline applications, while special stem packing configurations prevent freeze-up and maintain sealing integrity in extreme cold.
For sour gas applications common in Western Canada, SLVCN valves are manufactured with NACE MR0175/ISO 15156 compliant materials and undergo stringent quality control to prevent sulfide stress cracking. Fire-safe designs meeting API 607 and API 6FA standards provide critical safety protection for refineries and processing facilities.
Compliance with Canadian regulatory requirements is built into every valve design. Our products meet CSA standards, CRN (Canadian Registration Number) requirements for pressure-retaining components, and incorporate features that facilitate compliance with environmental regulations including fugitive emission standards.
SLVCN is committed to supporting Canadian industrial projects with comprehensive valve solutions, technical expertise, and responsive service. Our experience supplying valves to major Canadian EPC contractors, oil and gas operators, and industrial end-users spans decades, covering projects from offshore Newfoundland to the Alberta oil sands, and from Arctic mining operations to southern Ontario manufacturing facilities.
We understand that Canadian projects often operate under tight timelines, remote locations, and challenging logistics. Our project management team works closely with Canadian engineering firms, procurement departments, and construction contractors to ensure timely delivery, complete documentation, and full traceability of all valve components.
Material certifications, Canadian Registered Number (CRN) documentation, NACE compliance certificates, and complete quality assurance packages are provided as standard with every valve shipment. Our engineering team can assist with valve selection, specification review, and customization to meet specific project requirements including special materials, actuator configurations, and testing protocols.
Long-term operational reliability is supported through our comprehensive after-sales service program. We maintain an inventory of critical spare parts, provide technical support for maintenance procedures, and can arrange field service support for commissioning, troubleshooting, and emergency repairs. Our commitment to Canadian customers extends throughout the entire lifecycle of our valves, ensuring maximum uptime and operational efficiency.

Over 30 years of manufacturing experience


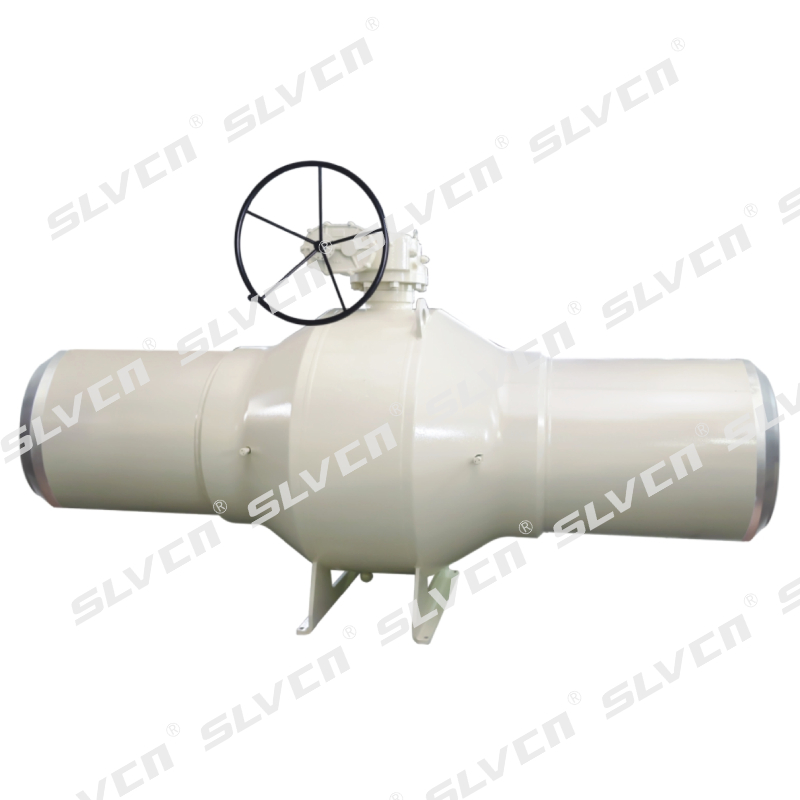
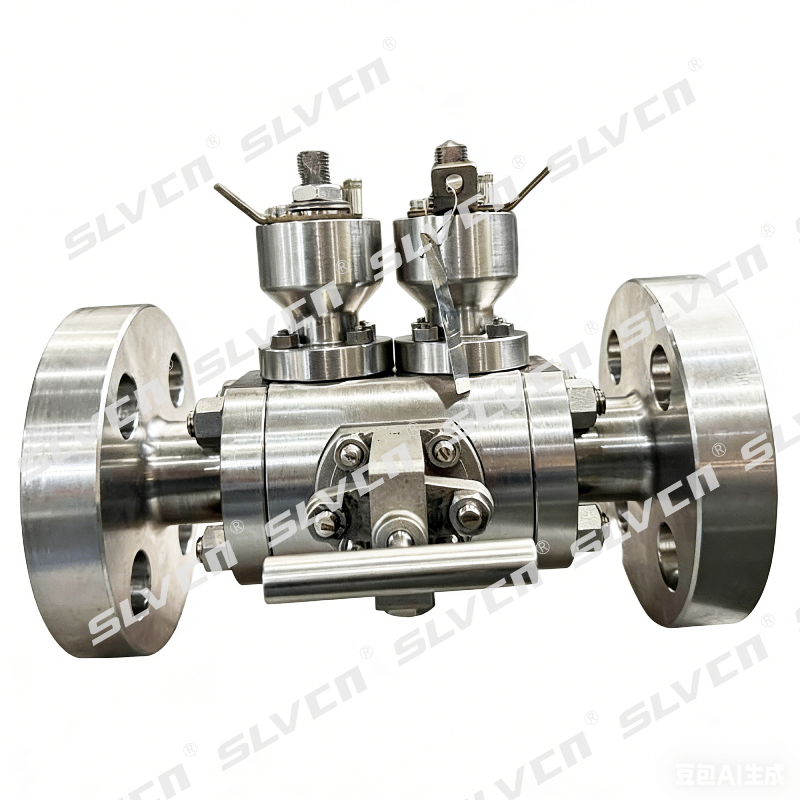
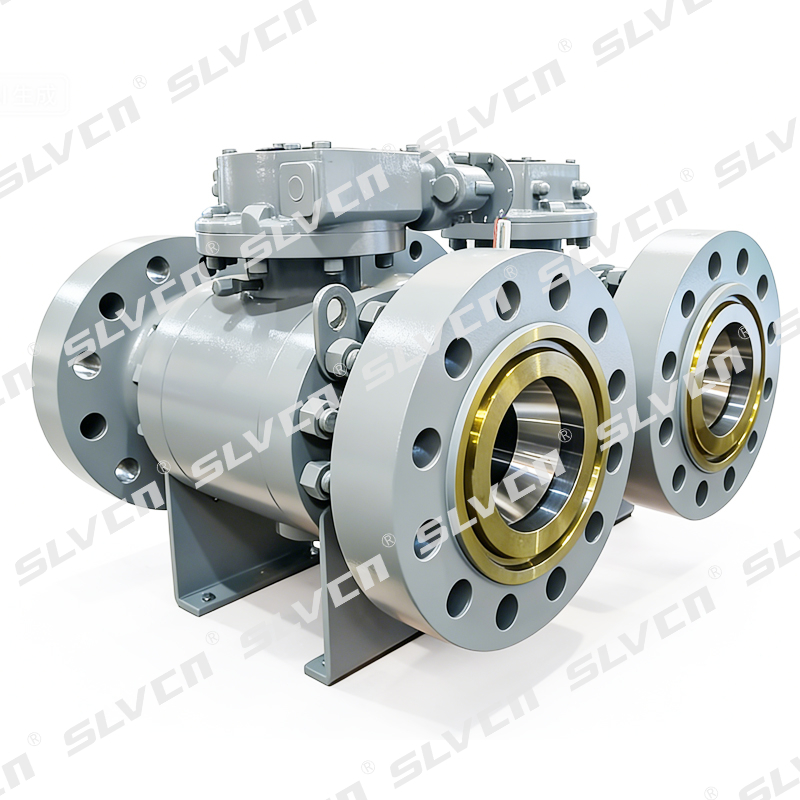
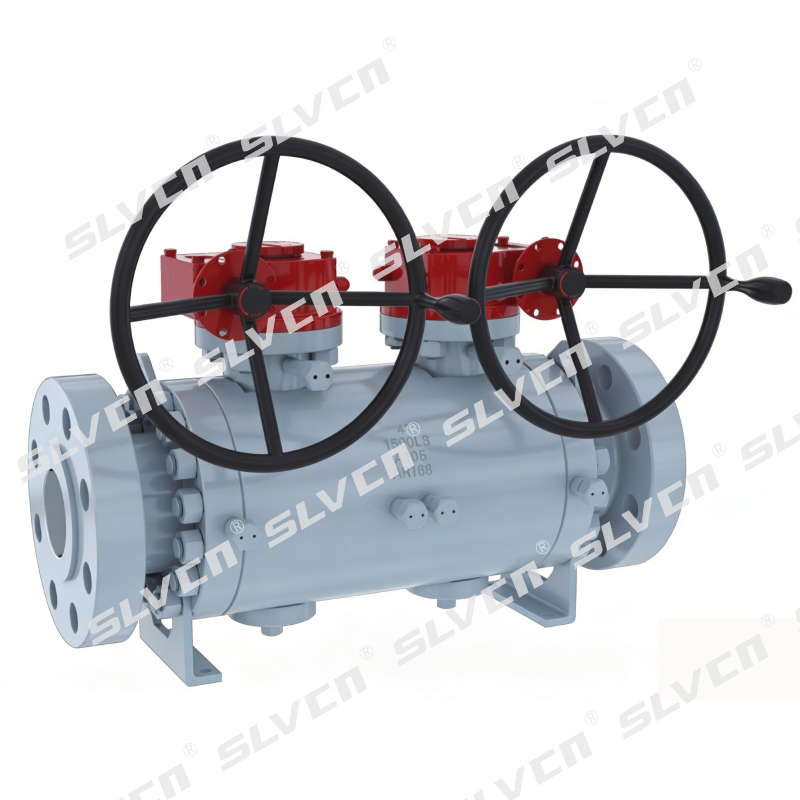
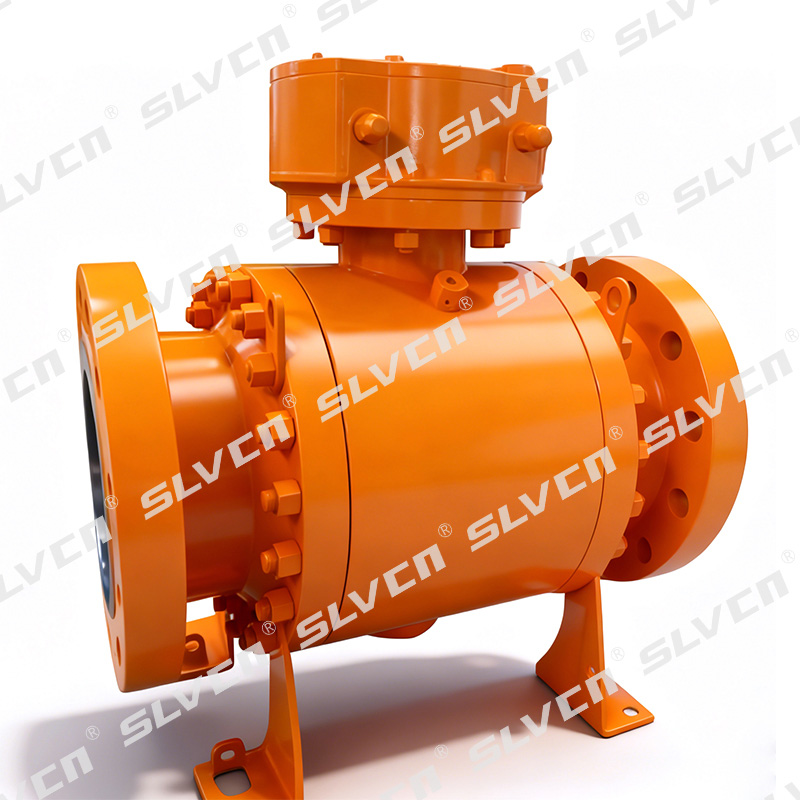
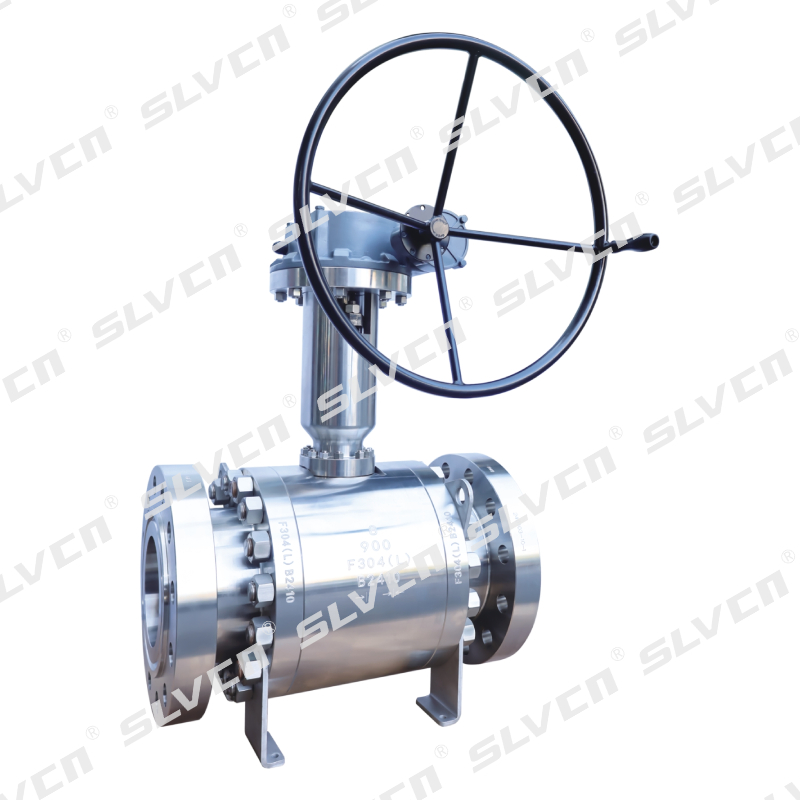
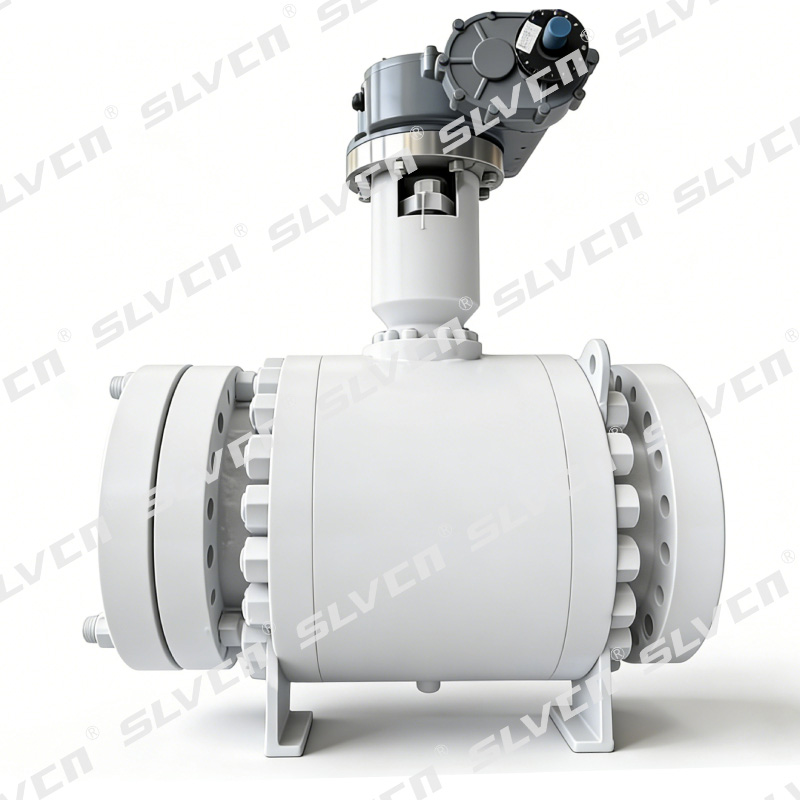
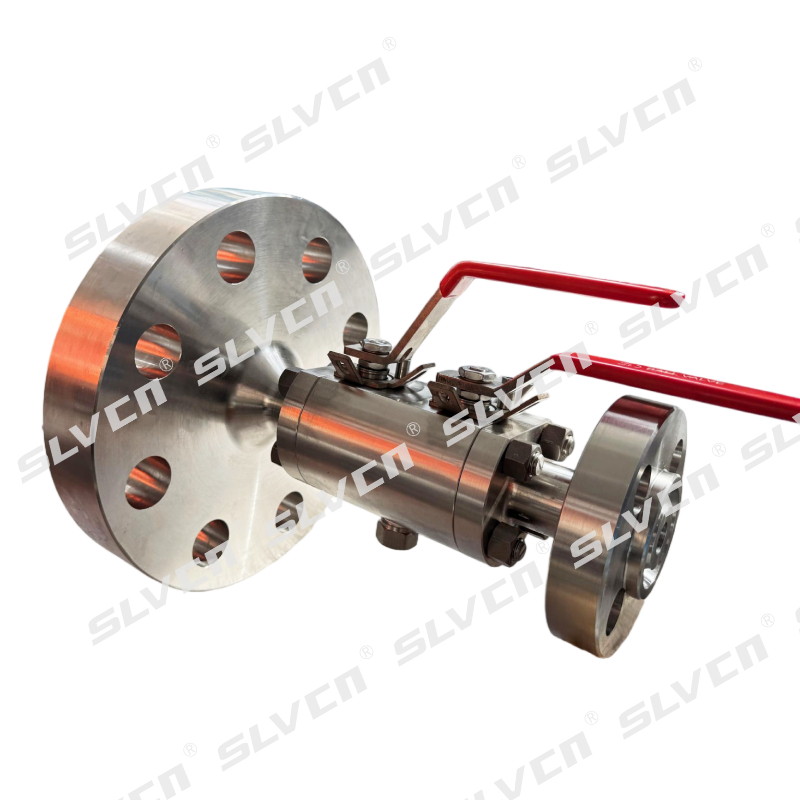
Our core product range covers forged trunnion-mounted and floating ball valves, top-entry and side-entry ball valves, fully welded ball valves, metal seated ball valves, cryogenic ball valves, high-pressure ball valves up to Class 2500 (PN420) and customized higher pressure ratings, as well as high-temperature service valves. Compared with conventional cast valves, SLVCN forged valves feature higher material density, superior mechanical strength, improved resistance to pressure fluctuations and thermal shock, and significantly longer service life under severe service conditions.
Designed for High Pressure, High Temperature, and Cryogenic Applications, SLVCN valves are widely used in long-distance oil & gas transmission pipelines, LNG storage and regasification terminals, offshore platforms and deepwater projects, power plants, refineries, compressor stations, and high-pressure chemical processing units. Whether handling flammable media, corrosive fluids, sour service media (H₂S), ultra-low temperatures, or extreme differential pressures, our valves ensure stable operation, bubble-tight shut-off, and maximum system safety in accordance with international sealing and performance standards.


Today, SLVCN serves customers in more than 100 countries and regions, supplying valves to EPC contractors, engineering companies, and end users across Europe, the Middle East, Southeast Asia, and the Americas. Backed by strong engineering expertise, advanced manufacturing, and rigorous quality control, SLVCN is committed to delivering safe, durable, and truly engineered valve solutions for the world's most demanding industrial projects.
Premium Valve Solutions for Every Canadian Industrial Application


 +86 18905154687