


Leave Your Message
High-performance DBB valves engineered for Norway's demanding offshore, subsea, and onshore energy infrastructure
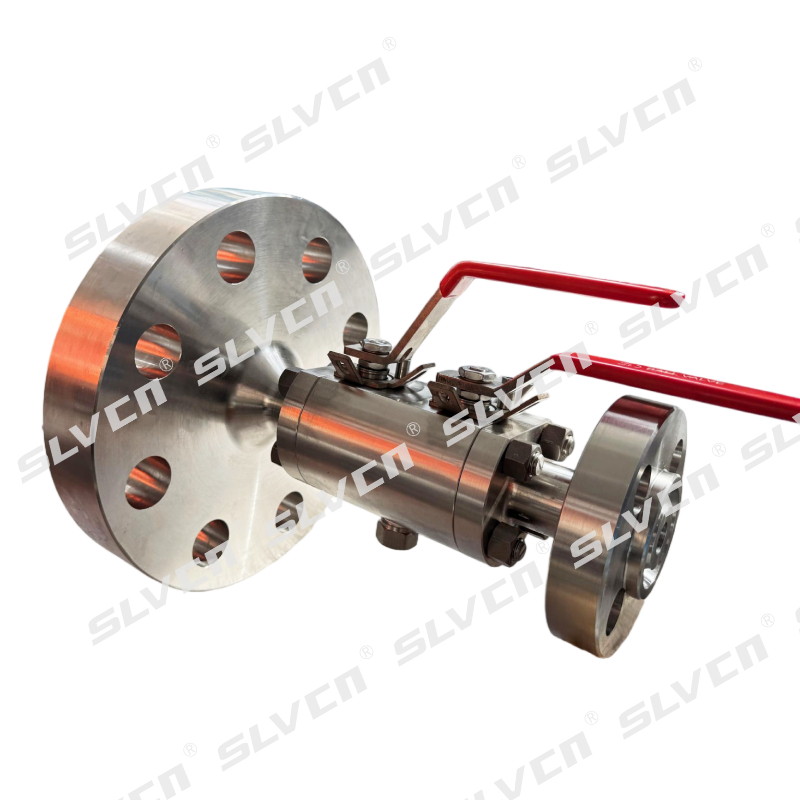
Norway stands as one of the world's foremost energy producers, with a highly sophisticated oil and gas industry anchored in the North Sea and the Norwegian Continental Shelf (NCS). The country's industrial infrastructure demands valve solutions of the highest caliber — particularly Double Block and Bleed (DBB) valves — which are indispensable for safe isolation, maintenance, and pressure management across upstream, midstream, and downstream operations.
The Norwegian oil and gas sector, governed by strict HSE regulations from the Petroleum Safety Authority Norway (PSA), mandates the use of certified, high-integrity isolation valves in all critical service lines. DBB valves — providing two independent sealing barriers with a bleed cavity between them — are the industry-standard solution for achieving zero-leakage isolation and safe depressurization in live pipeline systems.
Wellhead and Christmas tree valve packages for high-pressure crude and gas extraction.
DBB valves rated to −196°C for Equinor's Hammerfest LNG and Snøhvit facilities.
Valve solutions for Norway's growing hydrogen and offshore wind power infrastructure.
Isolation valves for Gassled — Europe's largest natural gas transmission network.
From Arctic offshore platforms to onshore processing terminals, DBB valves play a mission-critical role across Norway's entire energy value chain
DBB valves for process piping, chemical injection, and utility systems on Equinor, Aker BP, and ConocoPhillips-operated platforms on the Ekofisk, Johan Sverdrup, and Troll fields.
Compact DBB valve assemblies for subsea wellheads and manifolds, enabling safe isolation at extreme water depths on the Norwegian Continental Shelf.
High-pressure DBB valves for gas processing, NGL fractionation, and rich gas compression at Norway's largest onshore gas processing terminals.
Cryogenic-rated DBB valves for the Snøhvit LNG facility — Europe's first offshore LNG project — requiring bubble-tight isolation at temperatures down to −163°C.
Sour-service and high-purity DBB valves for Norway's Northern Lights CCS project and emerging green hydrogen production facilities along the western coast.
High-differential pressure DBB valves for subsea gas compression systems, supporting Norway's strategy to extend field life and maximize recovery rates.
High-temperature and corrosion-resistant DBB valves for crude distillation, hydrotreating, and fluid catalytic cracking units at Norway's largest refinery.
Valve packages for Hywind Tampen floating wind farms and offshore power-from-shore cable infrastructure supporting Norway's electrification ambitions.
Norway's energy transition, digital transformation, and stringent safety regulations are reshaping the valve procurement landscape
As Norway pushes exploration into the Barents Sea and deeper NCS regions, valve suppliers must meet increasingly demanding specifications for low-temperature performance, corrosion resistance, and reliability under extreme hydrostatic pressure. DBB valves rated for cryogenic and Arctic service are experiencing the strongest growth in procurement volume.
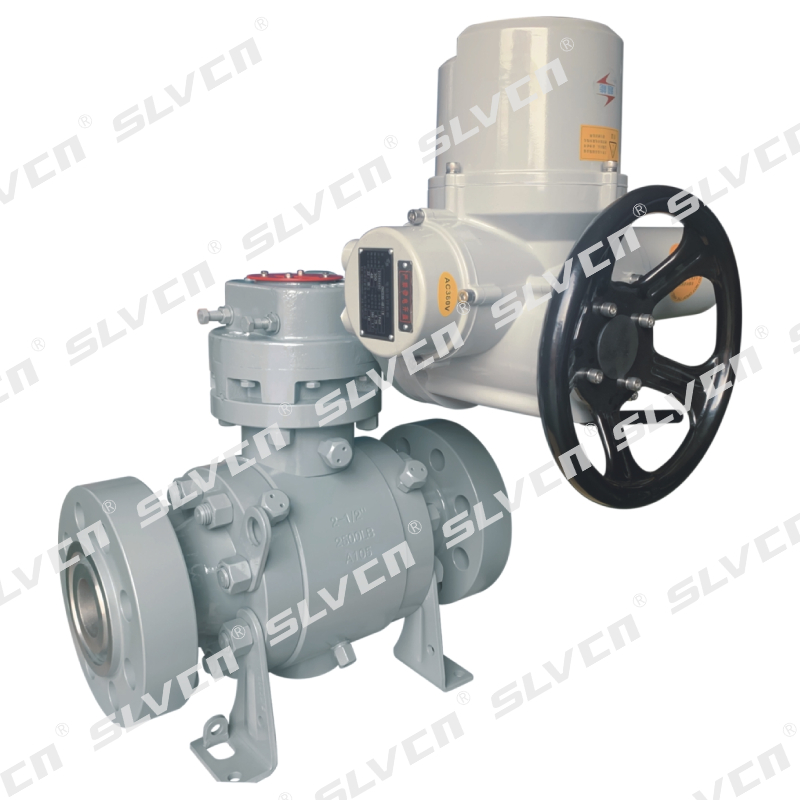
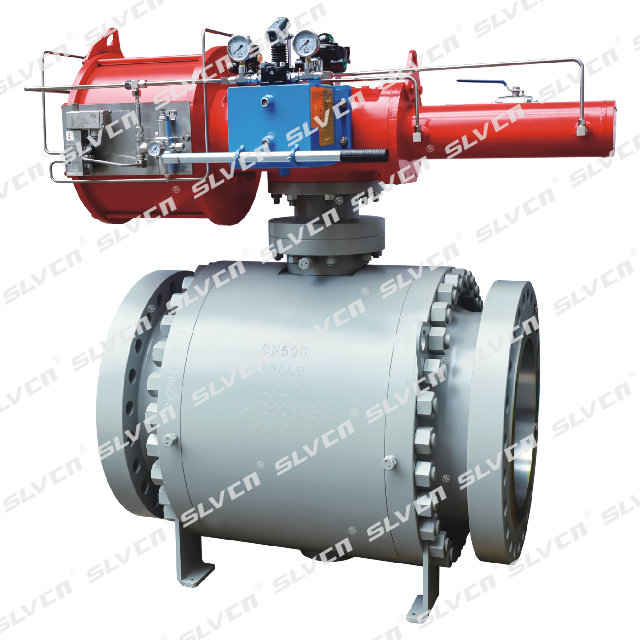
Norwegian operators are rapidly adopting intelligent valve solutions with integrated positioners, diagnostic sensors, and remote monitoring capabilities compatible with Equinor's Integrated Operations (IO) framework. Electric and pneumatic actuated DBB valves with HART, Profibus, or Foundation Fieldbus communication are now standard specifications in new FEED packages.
Norway's commitment to net-zero by 2050 is driving investment in carbon capture and storage (CCS), green hydrogen production, and electrified offshore platforms. Each of these emerging sectors requires specialized DBB valve configurations — from ultra-clean hydrogen service to high-CO₂ concentration sour service — creating new demand streams beyond traditional oil and gas.
Following enhanced PSA Norway guidelines on process safety and hydrocarbon leak prevention, operators on the NCS are upgrading aging valve infrastructure with certified DBB assemblies that meet the latest API 6D, NORSOK M-630, and NACE MR0175 requirements. This regulatory push is creating a significant retrofit and replacement market across Norway's mature fields.
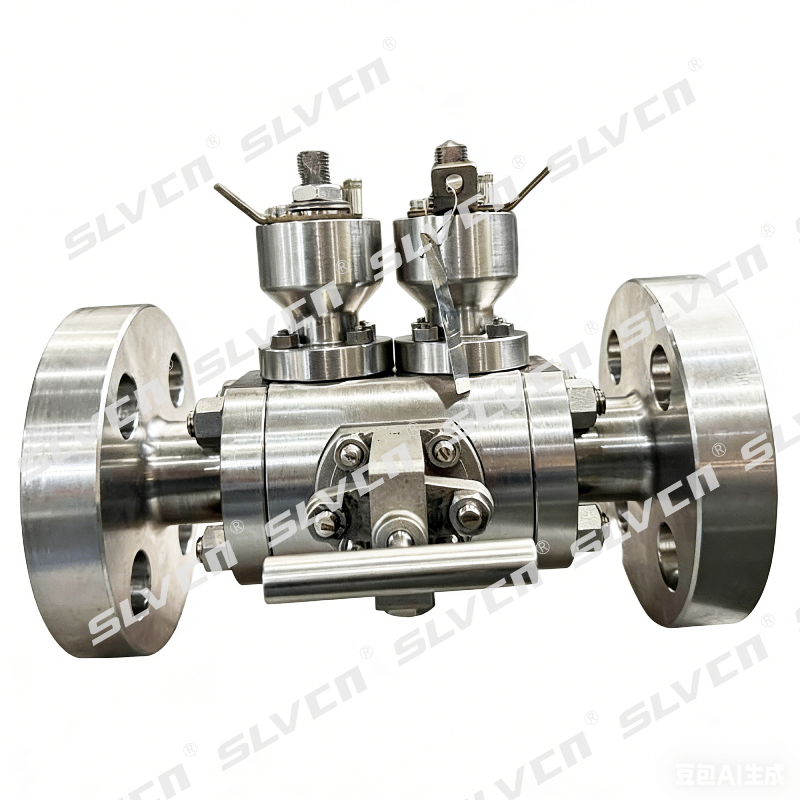
Norway's growing fleet of floating production, storage, and offloading (FPSO) vessels — including Johan Castberg and Balder X — requires compact, weight-optimized DBB valve assemblies that minimize topside footprint while delivering full API 6D performance. Integrated twin-ball DBB designs are increasingly specified for FPSO topsides and turret mooring systems.
Norway's NORSOK standards and Equinor's supplier qualification requirements increasingly favor manufacturers with proven track records in European energy projects, full material traceability, and the ability to provide rapid technical support. Global manufacturers with European distribution and after-sales service networks are gaining competitive advantage in the Norwegian market.
Understanding the technical and regulatory imperatives behind DBB valve adoption in Norwegian energy operations
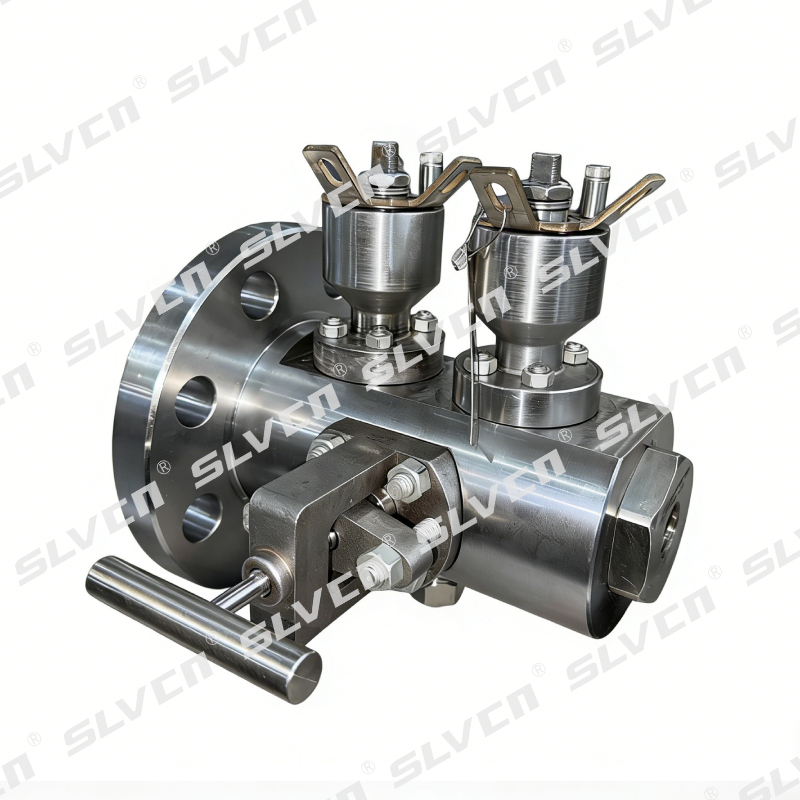
DBB valves provide two independent seating surfaces — each capable of holding full line pressure — with a monitored bleed cavity between them. This double-barrier principle is mandatory for isolation of hydrocarbon lines during maintenance, instrument calibration, and hot-work permits on Norwegian offshore installations.
The integrated bleed port allows operators to safely vent, drain, or monitor the cavity pressure between the two seats, confirming isolation integrity before breaking containment. This capability is critical for NORSOK Z-015 safe work permit procedures and PSA-mandated isolation verification protocols.
Replacing traditional double-valve-with-bleed-nipple arrangements, a single-body DBB valve reduces weight, installation footprint, potential leak points, and total installed cost — critical advantages for weight-sensitive offshore topsides and FPSO applications where every kilogram and square meter has a cost.
SLVCN DBB valves are available with LF2, F304L, F316L, and F51 duplex stainless steel body materials, combined with cryogenic-grade stem packing and PTFE or metal seats, ensuring reliable operation from −196°C LNG service to +450°C high-temperature refinery applications.
All SLVCN DBB valves are manufactured and tested in compliance with API 6D, API 598, ISO 5208 Rate A, ASME B16.34, and can be supplied with NORSOK M-630 MDS material documentation, DNV/Bureau Veritas third-party inspection, and full EN 10204 3.1/3.2 material certification packages.
For Norwegian fields producing sour gas with H₂S content, SLVCN DBB valves are available in full NACE MR0175 / ISO 15156 compliance, with hardness-controlled body materials, NACE-compliant stem and seat alloys, and elastomer seals rated for H₂S partial pressures per NACE TM0177 requirements.



With over 30 years of manufacturing experience, SLVCN is a professional designer and manufacturer of high-performance forged steel ball valves for critical industrial applications. We specialize in extreme working conditions including high pressure, high temperature, and cryogenic environments, providing safe and reliable flow control solutions for global industrial projects where operational reliability is non-negotiable.
As a trusted supplier to Norway's energy sector, SLVCN delivers Double Block and Bleed valve solutions that meet the stringent requirements of NORSOK, PSA Norway, and international API/ISO standards. Our dedicated engineering team works closely with Norwegian EPC contractors and end users to develop customized valve packages for North Sea platforms, LNG terminals, and pipeline systems.
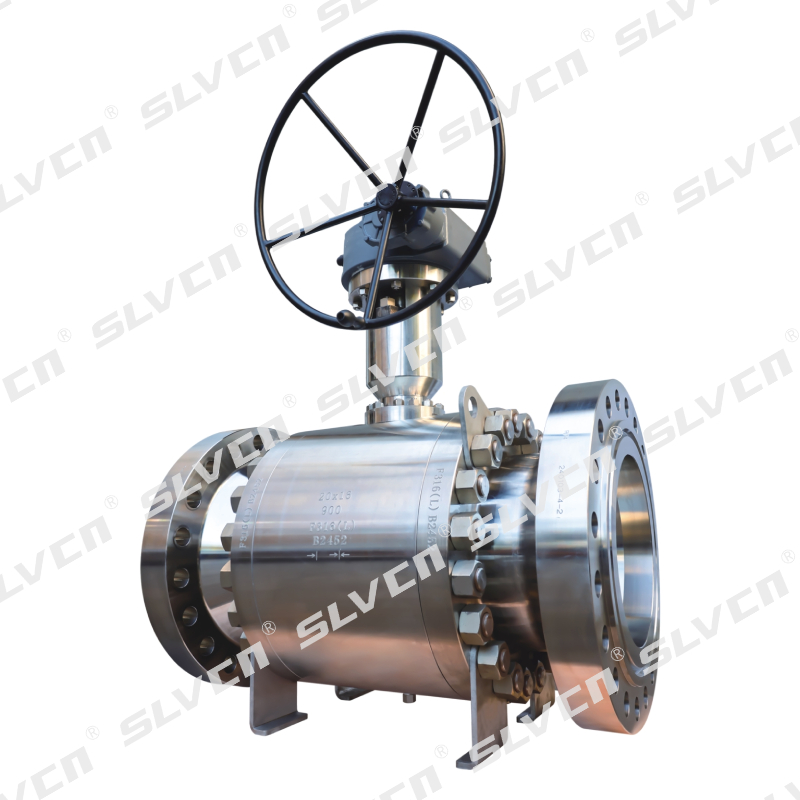
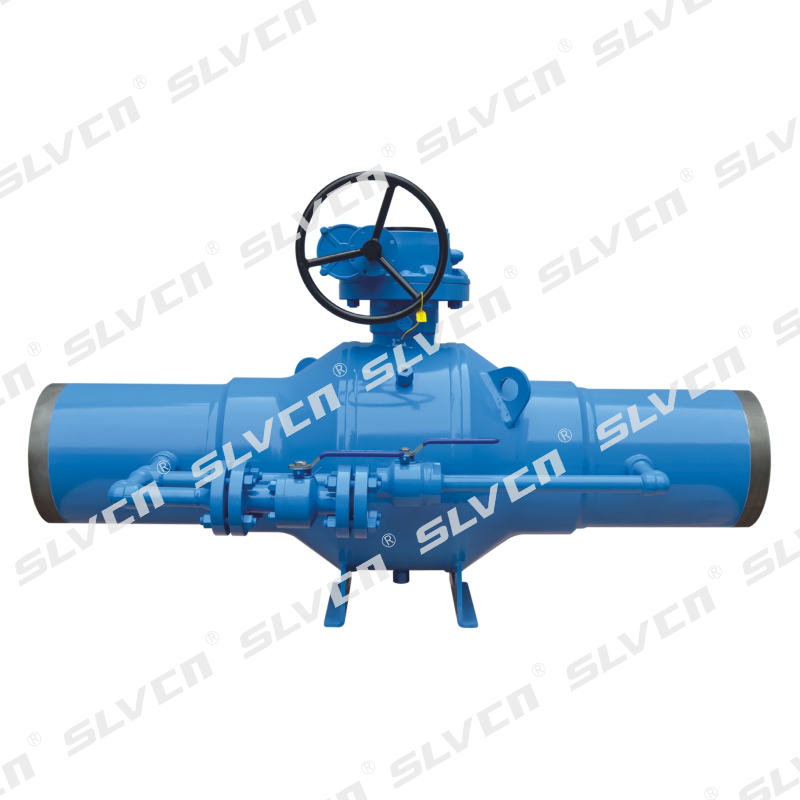
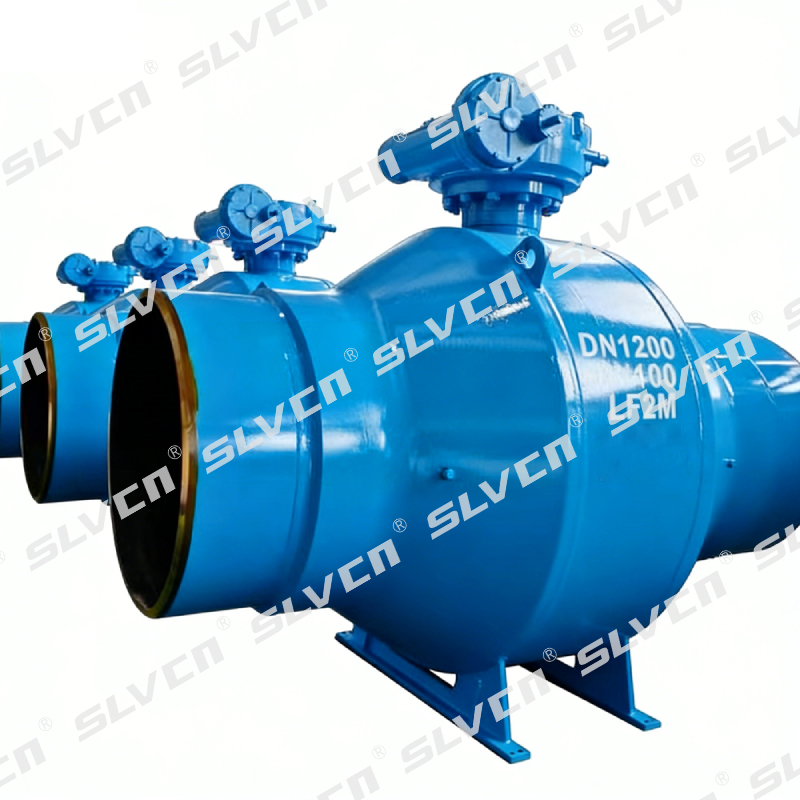
Contact UsOur core product range covers forged trunnion-mounted and floating ball valves, top-entry and side-entry ball valves, fully welded ball valves, metal seated ball valves, cryogenic ball valves, high-pressure ball valves up to Class 2500 (PN420) and customized higher pressure ratings, as well as high-temperature service valves.
Compared with conventional cast valves, SLVCN forged valves feature higher material density, superior mechanical strength, improved resistance to pressure fluctuations and thermal shock, and significantly longer service life under severe service conditions — making them the preferred choice for Norway's demanding North Sea and Arctic environments.

Safety and reliability are embedded in every design. Our forged ball valves are equipped with Double Block and Bleed (DBB) structures, anti-blowout stems, fire-safe designs in accordance with API 607 / API 6FA, anti-static devices, emergency sealing systems, and pressure-balanced seating structures suitable for high differential pressure operation.
Valves can be designed with SPE (Single Piston Effect) or DPE (Double Piston Effect) seat configurations based on application requirements. For sour service environments prevalent in Norwegian North Sea fields, materials and sealing systems comply with NACE MR0175 / ISO 15156 requirements, ensuring safe operation in H₂S-containing hydrocarbon streams.
SLVCN's DBB valves are designed for the full lifecycle of Norwegian energy assets — from first oil through late-life enhanced recovery — providing consistent isolation performance, minimal maintenance requirements, and full traceability of all pressure-containing components.
Every SLVCN valve is manufactured and tested to the highest international standards demanded by Norway's energy industry
To ensure consistent quality, each valve undergoes a complete series of inspections and performance tests in accordance with API 6D, API 598, and ISO 5208, including shell test, seat leakage test (Rate A / zero visible leakage), fire-safe test, cryogenic test, operational torque test, dimensional inspection, and PMI material verification. SLVCN operates dedicated cryogenic testing facilities to validate valve performance at ultra-low temperatures down to −196°C — critical for Norway's LNG and Arctic service applications.
SLVCN is certified to ISO 9001, CE, and API standards, and our products comply with API 6D, ASME B16.34, DIN, ANSI, and JIS specifications. We provide extensive customization capabilities covering sizes from 1/2" to 36", full bore or reduced bore, special materials including A105, LF2, F11, F22, F51, Inconel, various soft and metal seat designs, and intelligent actuation with pneumatic, electric, and gear operators. All documentation packages can be prepared to meet NORSOK M-630 and EN 10204 3.1/3.2 requirements for Norwegian operator qualification.

Today, SLVCN serves customers in more than 100 countries and regions, supplying valves to EPC contractors, engineering companies, and end users across Europe, the Middle East, Southeast Asia, and the Americas. Backed by strong engineering expertise, advanced manufacturing, and rigorous quality control, SLVCN is committed to delivering safe, durable, and truly engineered valve solutions for the world's most demanding industrial projects — including Norway's North Sea, Barents Sea, and Arctic energy frontier.
As a dedicated double bleed valve manufacturer and supplier for Norway, SLVCN offers full project support from initial technical consultation and valve selection through manufacturing, third-party inspection, documentation preparation, and on-time delivery to Norwegian ports and project sites. Our experienced export team ensures full compliance with Norwegian import requirements and Equinor/Aker BP supplier qualification standards.
Request a Quote for Norway ProjectsExplore our full range of double block and bleed valves and forged ball valves designed for Norway's oil & gas, LNG, and energy transition projects


 +86 18913944686

