


Leave Your Message
Engineered for Kazakhstan's demanding oil & gas pipeline, LNG, and refinery environments — certified to API 6D, ASME, and international standards.
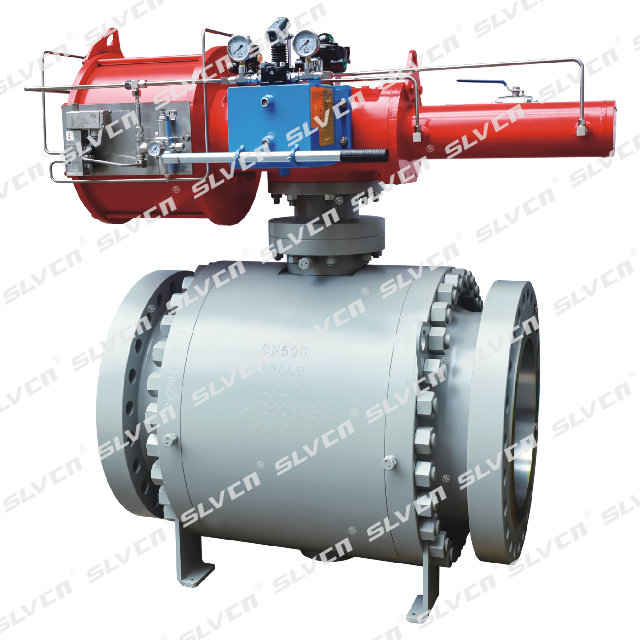
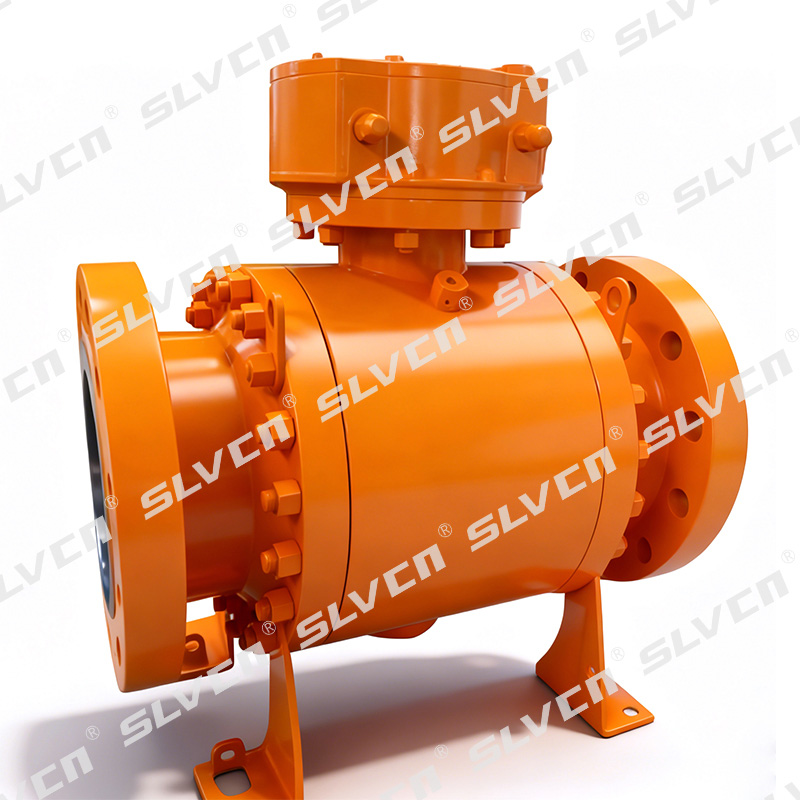
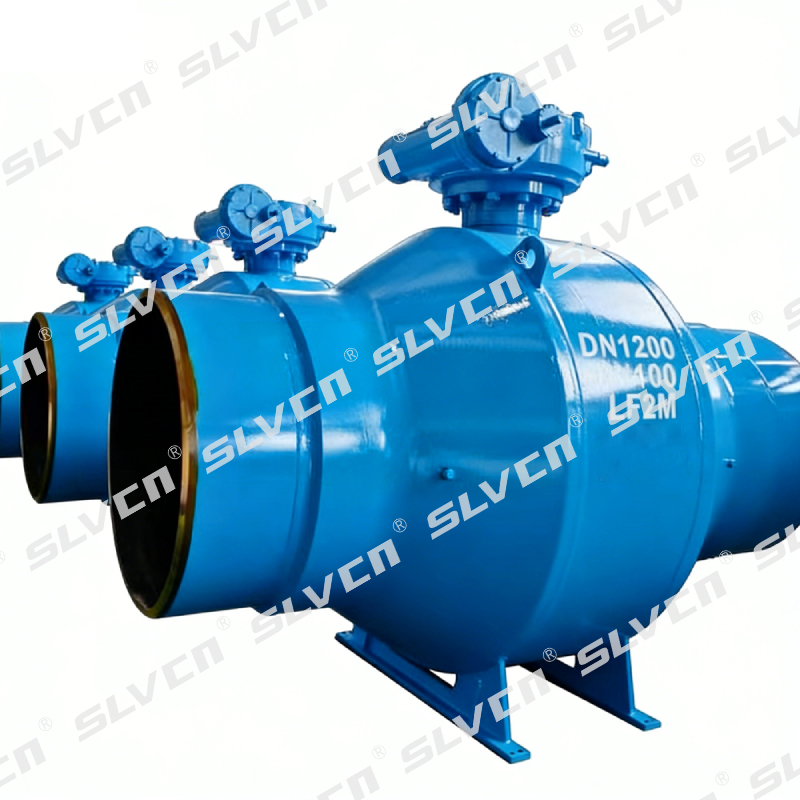
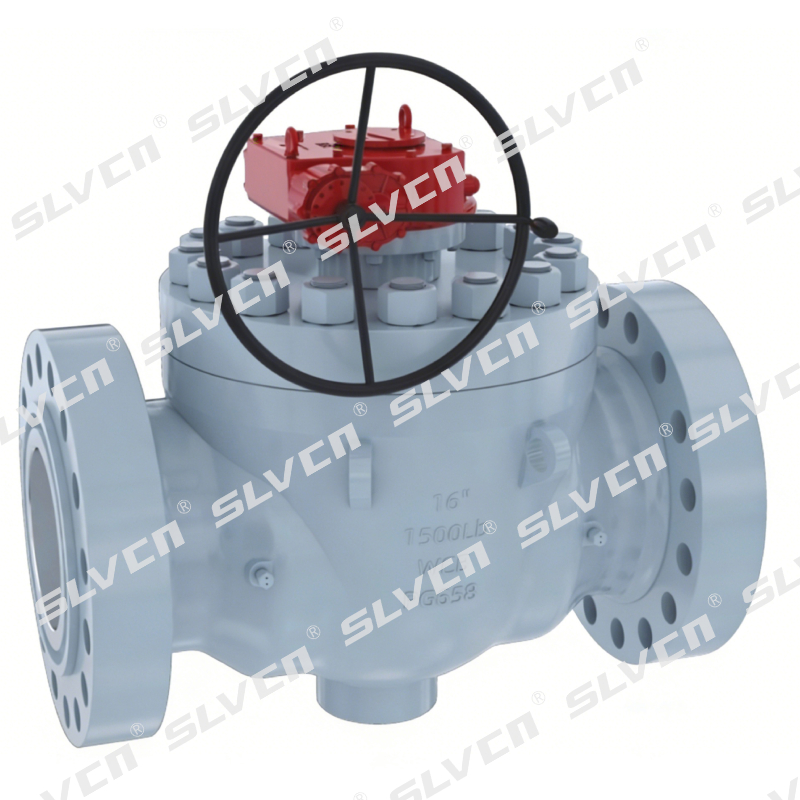



With over 30 years of manufacturing experience, SLVCN is a professional designer and manufacturer of high-performance forged steel ball valves for critical industrial applications. We specialize in extreme working conditions including high pressure, high temperature, and cryogenic environments, providing safe and reliable flow control solutions for global industrial projects where operational reliability is non-negotiable.
Today, SLVCN serves customers in more than 100 countries and regions, supplying valves to EPC contractors, engineering companies, and end users across Europe, the Middle East, Southeast Asia, and the Americas. Backed by strong engineering expertise, advanced manufacturing, and rigorous quality control, SLVCN is committed to delivering safe, durable, and truly engineered valve solutions for the world's most demanding industrial projects — including Kazakhstan's rapidly expanding energy infrastructure.
Contact UsKazakhstan is Central Asia's largest energy producer, home to world-class oilfields including Tengiz, Kashagan, and Karachaganak. The nation's vast pipeline networks, LNG facilities, and petrochemical complexes demand the highest-specification Double Block & Bleed (DBB) valve technology.
Kazakhstan's giant oilfields operate under extreme high-pressure, high-H₂S sour service conditions. DBB valves with NACE MR0175-compliant materials are essential for safe isolation and bleed operations in wellhead and pipeline manifold systems across these world-scale projects.
KazTransOil operates thousands of kilometers of trunk pipelines transporting crude oil to export terminals. Fully welded trunnion-mounted DBB ball valves are the preferred choice for buried and above-ground pipeline isolation, offering zero-leakage performance and minimal maintenance requirements in remote steppe environments.
Kazakhstan's major refineries in Atyrau and Pavlodar are undergoing significant modernization programs. High-integrity DBB valves with metal-seated designs are increasingly specified for severe-service applications including catalytic cracking units, high-temperature process lines, and safety-critical isolation duties.
With Kazakhstan developing its LNG infrastructure to diversify energy exports, cryogenic DBB ball valves rated for −196°C service are in growing demand for LNG storage, loading, and regasification terminals. SLVCN's dedicated cryogenic testing facility validates every valve to international performance standards.
Kazakhstan's extensive natural gas processing infrastructure, including plants operated by KazMunayGas, requires high-pressure DBB valves for compressor station isolation, pig trap closures, and pressure safety systems. Class 600 to Class 2500 forged DBB valves deliver reliable performance under cyclic pressure conditions.
Kazakhstan's Green Economy Concept targets significant renewable energy expansion. Emerging hydrogen production and distribution projects will require specialized DBB valve solutions for hydrogen service, with anti-static designs and ATEX-compliant actuation systems suited for the unique challenges of clean energy infrastructure.
Kazakhstan's valve industry is evolving rapidly, driven by energy sector investment, localization policies, and international safety standards adoption. Understanding these trends helps procurement teams make informed sourcing decisions.
Kazakhstan's government mandates increasing local content (KZ content) in oil & gas procurement. International valve manufacturers partnering with local distributors and service providers in Almaty, Atyrau, and Nur-Sultan (Astana) can better meet these requirements while ensuring rapid delivery and on-site technical support.
Major Kazakhstan operators including TengizChevroil, Agip KCO, and KazMunayGas increasingly specify API 6D, API 607 fire-safe, and NACE MR0175 compliant valves. SLVCN's full certification portfolio directly addresses these procurement requirements, simplifying vendor qualification processes.
Kazakhstan's digital oilfield initiatives are driving demand for intelligent valve solutions with electric actuators, position feedback, and SCADA integration. SLVCN offers pneumatic, electric, and gear-operated DBB valves compatible with modern digital control architectures used across Kazakhstan's major oil & gas facilities.
Kazakhstan's Kashagan field is notorious for extremely high H₂S concentrations. The demand for NACE-compliant sour service DBB valves using materials such as F22, F51 duplex stainless steel, and Inconel alloys is a key growth driver, requiring specialized manufacturing expertise that SLVCN has developed over decades.
Kazakhstan continues to expand its oil export capacity through projects like the Caspian Pipeline Consortium (CPC) expansion and new trans-Caspian routes. Each new pipeline segment requires hundreds of high-specification DBB ball valves for mainline isolation, scraper traps, and metering stations.
With global supply chain pressures, Kazakhstan's EPC contractors increasingly turn to established Chinese valve manufacturers like SLVCN for competitive pricing, shorter lead times, and proven quality. SLVCN's dedicated manufacturing facilities and stock programs ensure reliable delivery schedules for Kazakhstan project timelines.
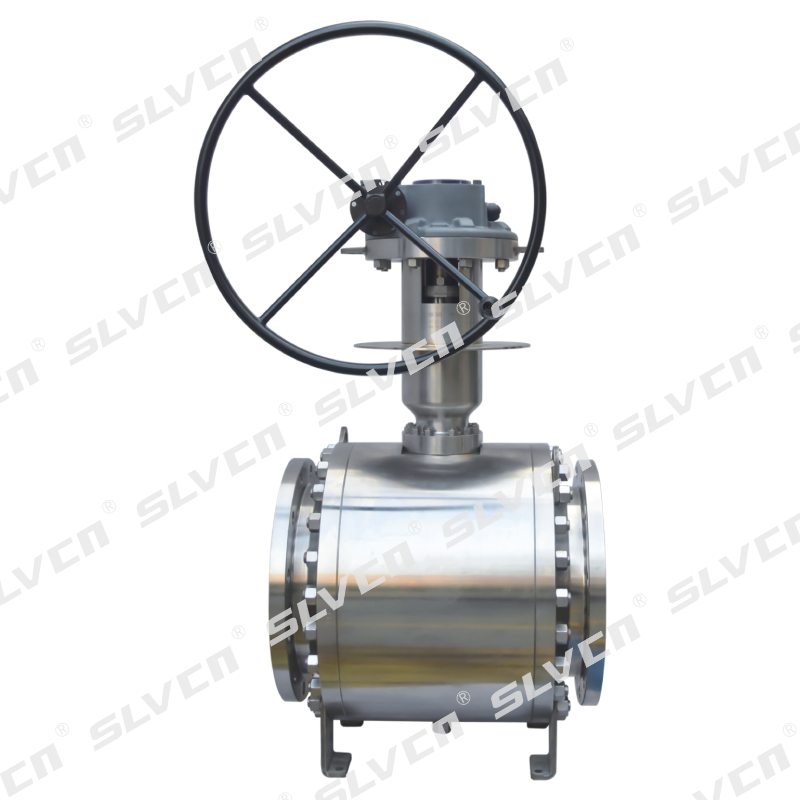
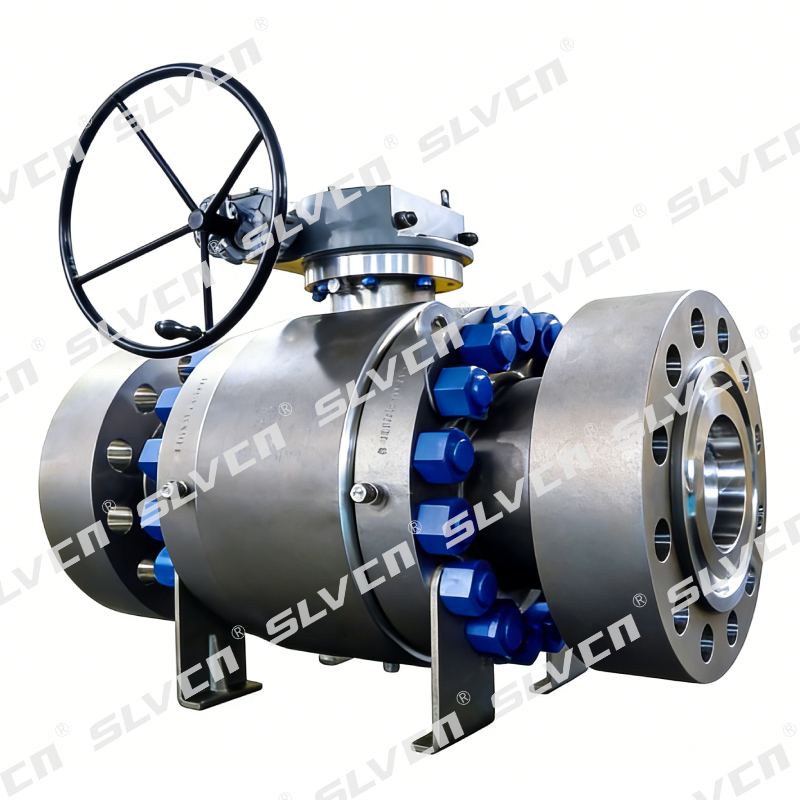
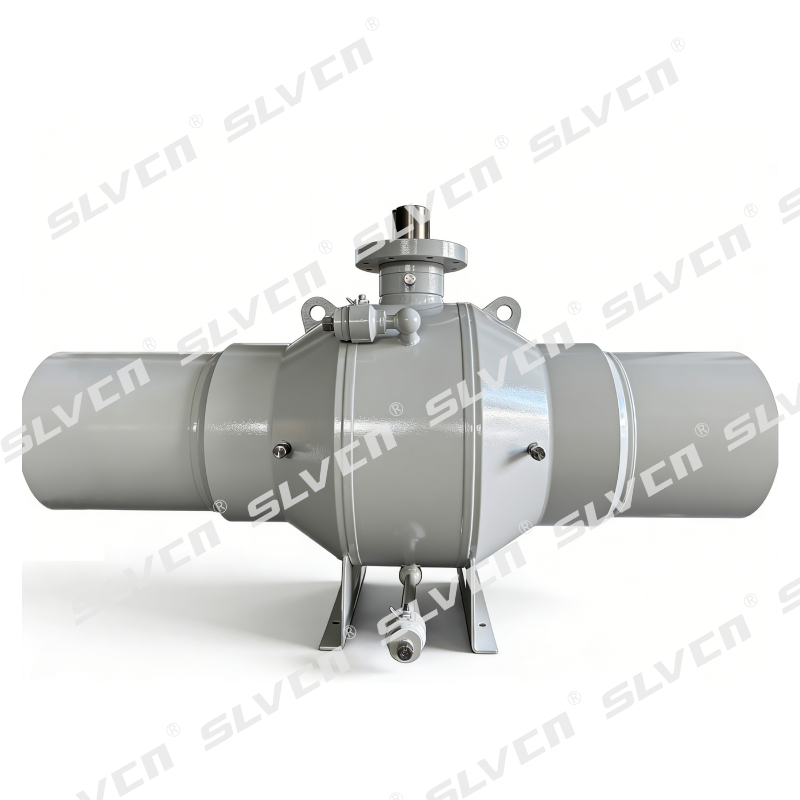
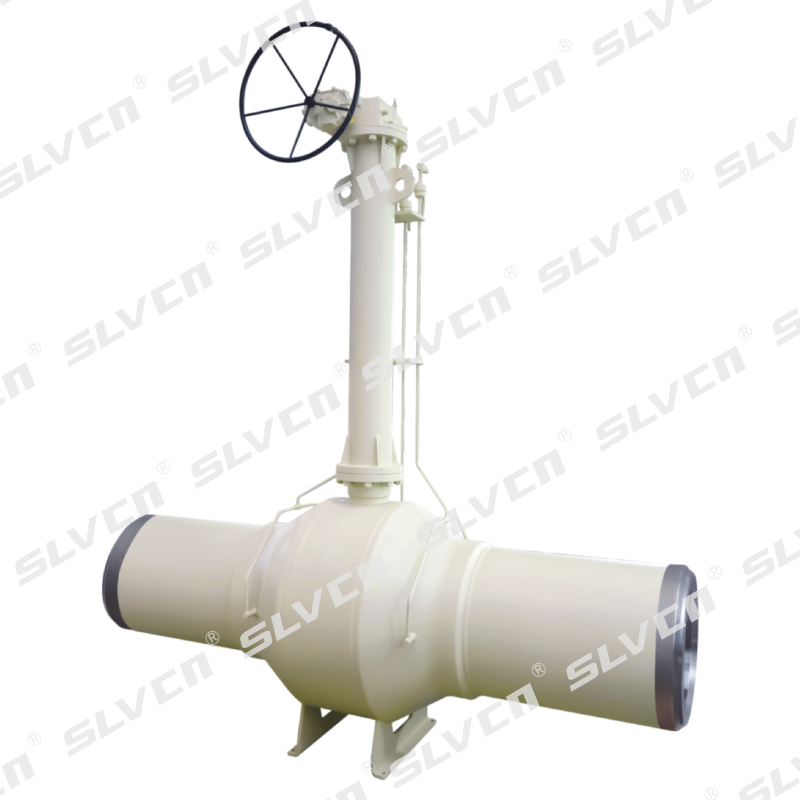
Our core product range covers forged trunnion-mounted and floating ball valves, top-entry and side-entry ball valves, fully welded ball valves, metal seated ball valves, cryogenic ball valves, high-pressure ball valves up to Class 2500 (PN420) and customized higher pressure ratings, as well as high-temperature service valves. Compared with conventional cast valves, SLVCN forged valves feature higher material density, superior mechanical strength, improved resistance to pressure fluctuations and thermal shock, and significantly longer service life under severe service conditions.
For Kazakhstan's unique operating environment — spanning extreme continental climate temperatures, high-pressure sour gas fields, and remote pipeline corridors — SLVCN's forged DBB valves offer the durability, sealing integrity, and low total cost of ownership that project operators and EPC contractors demand.
Designed for High Pressure, High Temperature, and Cryogenic Applications, SLVCN valves are widely used in long-distance oil & gas transmission pipelines, LNG storage and regasification terminals, offshore platforms and deepwater projects, power plants, refineries, compressor stations, and high-pressure chemical processing units. Whether handling flammable media, corrosive fluids, sour service media (H₂S), ultra-low temperatures, or extreme differential pressures, our valves ensure stable operation, bubble-tight shut-off, and maximum system safety in accordance with international sealing and performance standards.
In Kazakhstan specifically, SLVCN DBB valves are deployed across Tengiz field expansion projects, KazTransOil trunk pipeline systems, Atyrau refinery modernization programs, and emerging LNG terminal developments — providing operators with the confidence of certified, field-proven valve performance in every critical isolation point.

Safety and reliability are embedded in every design. Our forged ball valves are equipped with Double Block and Bleed (DBB) structures, anti-blowout stems, fire-safe designs in accordance with API 607 / API 6FA, anti-static devices, emergency sealing systems, and pressure-balanced seating structures suitable for high differential pressure operation. Valves can be designed with SPE or DPE seat configurations based on application requirements. For sour service environments, materials and sealing systems comply with NACE MR0175 / ISO 15156 requirements.
Kazakhstan's oil & gas operators face some of the world's most challenging service conditions: extreme cold winters reaching −40°C, high-pressure sour gas containing significant H₂S concentrations, and remote locations where valve failure carries enormous operational and environmental consequences. SLVCN's DBB valve designs address every one of these challenges through engineering solutions proven in the field across comparable global projects.
Every SLVCN valve is manufactured and tested to the most rigorous international standards, ensuring full compliance with Kazakhstan operator specifications and international project requirements.
To ensure consistent quality, each valve undergoes a complete series of inspections and performance tests in accordance with API 6D, API 598, and ISO 5208, including shell test, seat leakage test (Rate A / zero visible leakage), fire-safe test, cryogenic test, operational torque test, dimensional inspection, and PMI material verification. SLVCN operates dedicated cryogenic testing facilities to validate valve performance at ultra-low temperatures down to −196°C.
SLVCN is certified to ISO 9001, CE, and API standards, and our products comply with API 6D, ASME B16.34, DIN, ANSI, and JIS specifications. We provide extensive customization capabilities covering sizes from 1/2" to 36", full bore or reduced bore, special materials including A105, LF2, F11, F22, F51, Inconel, various soft and metal seat designs, and intelligent actuation with pneumatic, electric, and gear operators.

Today, SLVCN serves customers in more than 100 countries and regions, supplying valves to EPC contractors, engineering companies, and end users across Europe, the Middle East, Southeast Asia, and the Americas. Backed by strong engineering expertise, advanced manufacturing, and rigorous quality control, SLVCN is committed to delivering safe, durable, and truly engineered valve solutions for the world's most demanding industrial projects. For Kazakhstan-based projects, our dedicated export team provides full documentation support including MTRs, test certificates, and compliance packages tailored to local regulatory requirements.
Get a Kazakhstan Project QuoteExplore our full range of high-performance valves — each engineered for the demanding conditions found across Kazakhstan's oil, gas, and petrochemical industries.


 18061659285

