Leave Your Message
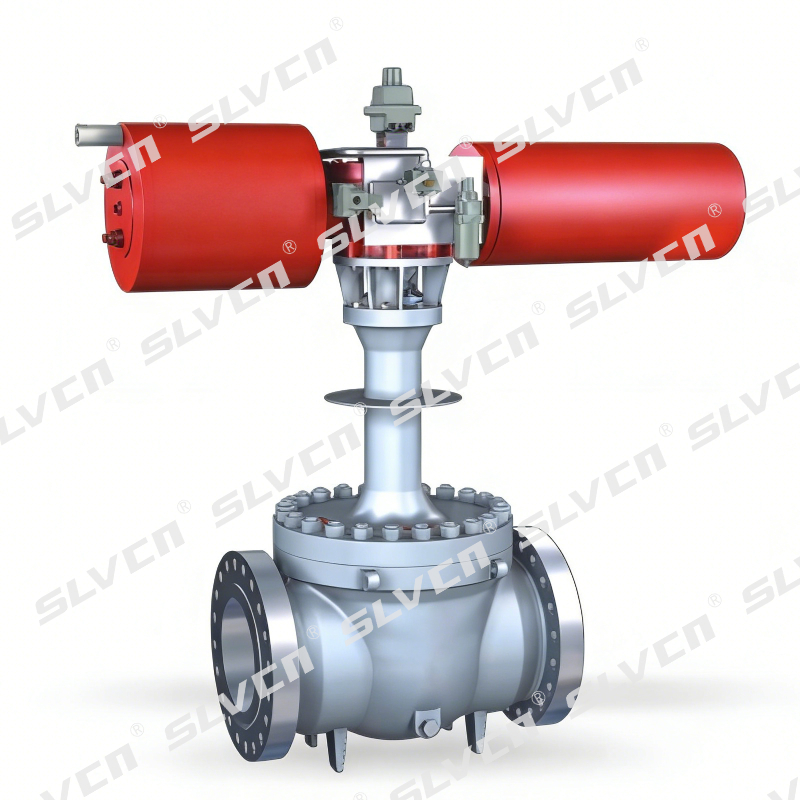
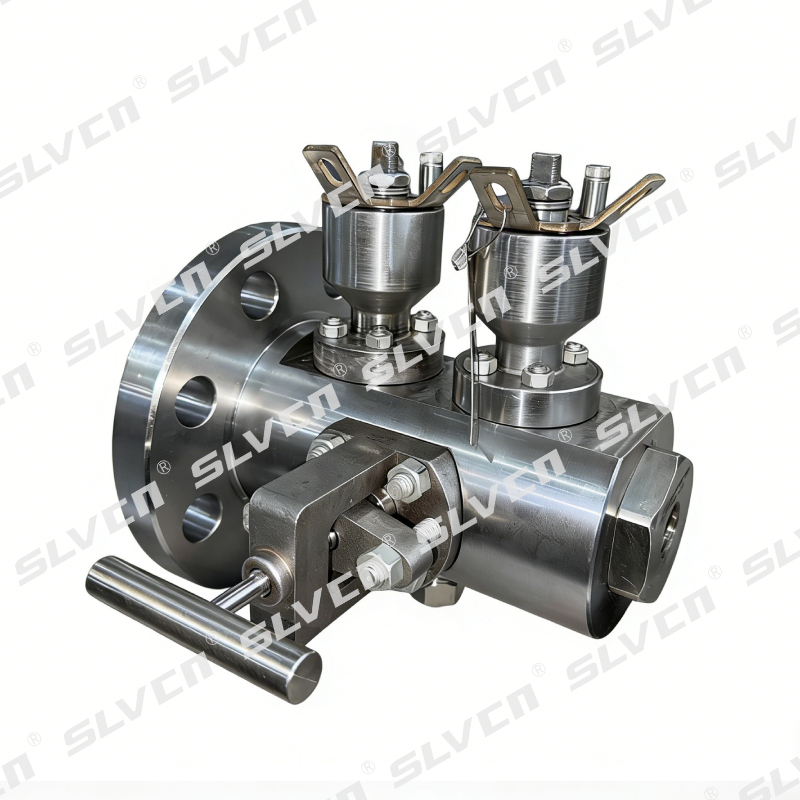
As the global energy transition accelerates, Solar Thermal Energy Plants, particularly Concentrated Solar Power (CSP), have emerged as a cornerstone of renewable energy stability. Unlike photovoltaic systems, CSP plants utilize mirrors to concentrate sunlight, heating a fluid (often molten salt or thermal oil) to generate steam and drive turbines. In this extreme operational environment, the Double Ball Valve (specifically with Double Block and Bleed - DBB structure) has become an indispensable component for safety and efficiency.
In the current industrial landscape, Solar Thermal Energy Plants operate at temperatures often exceeding 565°C (in molten salt systems) and pressures reaching Class 2500. Traditional cast valves frequently fail under the thermal cycling and corrosive nature of heat transfer fluids (HTF). This is where SLVCN’s forged steel double ball valves set the industry standard. By utilizing high-density forged materials, we eliminate the porosity issues common in casting, ensuring structural integrity during rapid temperature fluctuations.
The DBB structure provides two independent seating surfaces, ensuring a bubble-tight seal even if one seat is compromised.
Designed to handle extreme thermal expansion without jamming, crucial for molten salt storage tanks.
Meets API 6D and ISO 5208 Rate A standards, preventing costly HTF loss and environmental hazards.
The market for CSP is expanding rapidly in regions like the Middle East (MENA), China, and Spain. Modern plants are moving toward "Thermal Energy Storage" (TES) systems that require 24/7 operation. This shift has triggered several key trends in Double Ball Valve engineering:
Within a Concentrated Solar Power facility, the Double Ball Valve is utilized in several high-stakes zones:

Jiangsu Shoulong Valve Co., Ltd. (SLVCN) is a professional designer and manufacturer of high-performance forged steel ball valves for critical industrial applications. With over 30 years of manufacturing experience, we specialize in extreme working conditions including high pressure, high temperature, and cryogenic environments.
Our commitment to providing safe and reliable flow control solutions makes us a preferred partner for global industrial projects where operational reliability is non-negotiable. Whether it is a solar thermal plant in the desert or an LNG terminal on the coast, SLVCN valves are built to endure.
When selecting a Double Ball Valve for Solar Thermal Energy Plants, several technical parameters must be strictly adhered to. At SLVCN, our engineering team focuses on the following critical design elements:
For temperatures above 250°C, soft seats (PTFE/Devlon) are no longer viable. We utilize tungsten carbide or chromium carbide coatings on the ball and seat surfaces. This ensures a "Hard-Seal" that can withstand the abrasive nature of salt crystals and thermal shocks.
Safety is paramount. All our valves feature anti-blowout stems to prevent accidents under high pressure. Furthermore, our fire-safe designs comply with API 607 and API 6FA, ensuring the valve maintains its seal even in the event of an external fire, which is a critical safety requirement for plants handling flammable thermal oils.
In solar applications, fluid trapped in the valve cavity can expand rapidly due to heat. We offer Single Piston Effect (SPE) or Double Piston Effect (DPE) seat configurations. For solar thermal, a combination (DIB-1 or DIB-2) is often recommended to manage cavity pressure while maintaining isolation integrity.
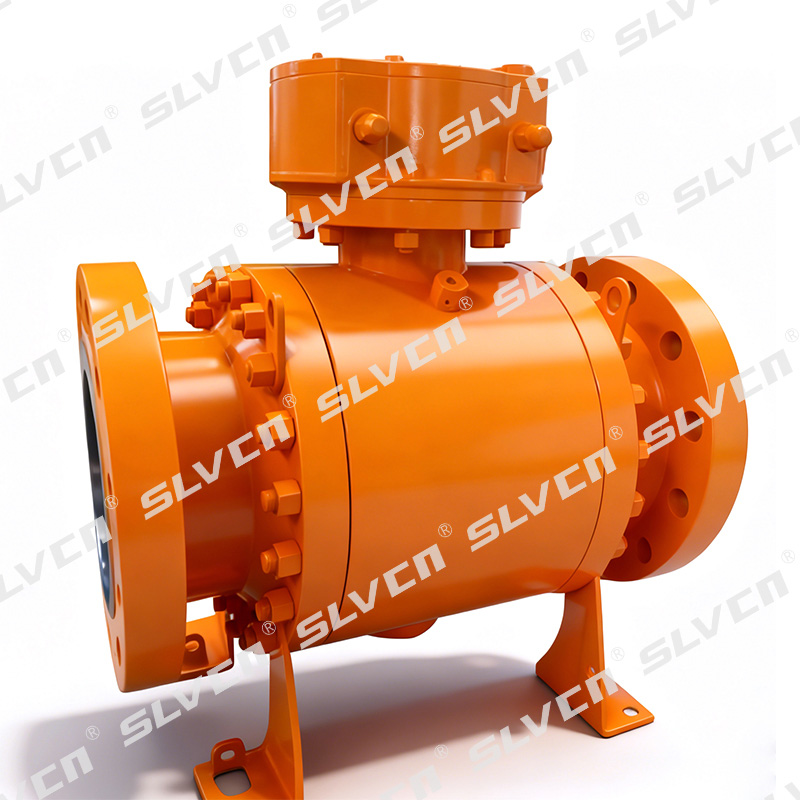
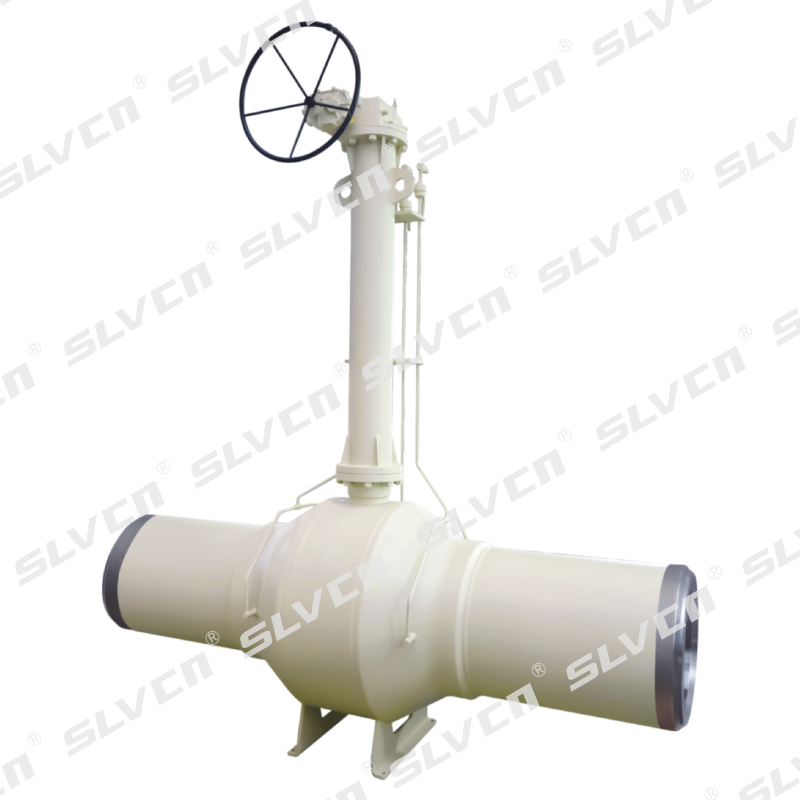
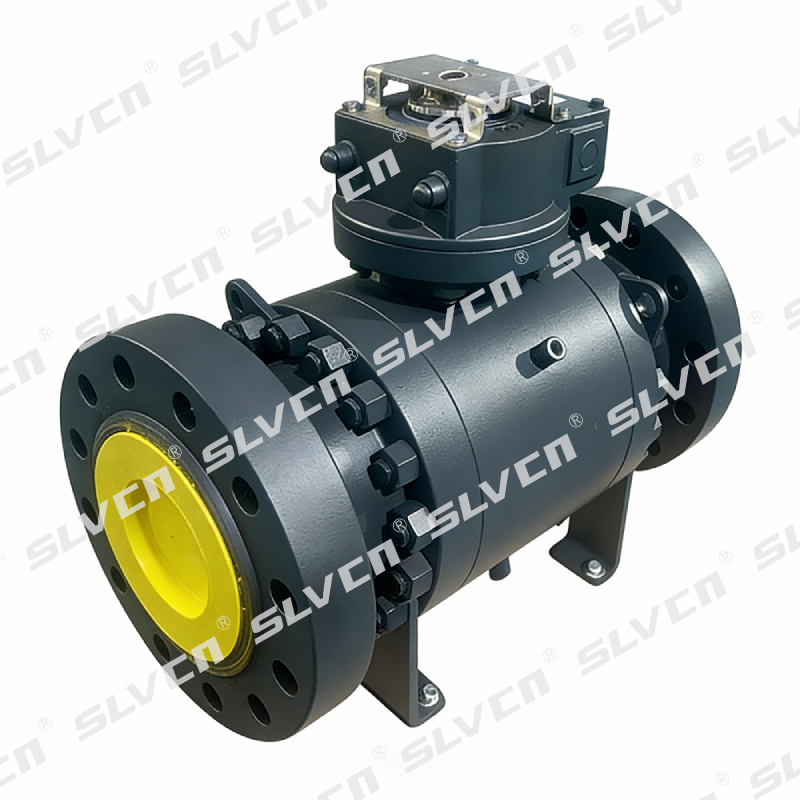
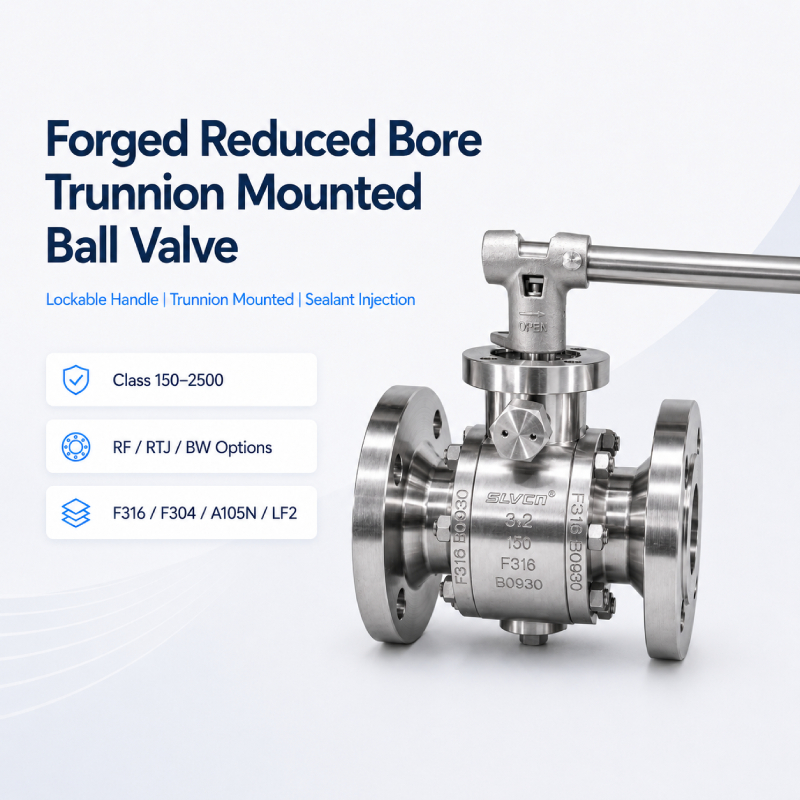
Our core product range covers forged trunnion-mounted and floating ball valves, top-entry and side-entry ball valves, fully welded ball valves, and metal seated ball valves. Compared with conventional cast valves, SLVCN forged valves feature higher material density, superior mechanical strength, and significantly longer service life under severe service conditions.
Designed for High Pressure, High Temperature, and Cryogenic Applications, SLVCN valves are widely used in long-distance oil & gas transmission, LNG storage, and power plants. Our forged ball valves are equipped with Double Block and Bleed (DBB) structures, anti-static devices, and emergency sealing systems to ensure maximum system safety.

The economic viability of a Solar Thermal Energy Plant depends on its "Levelized Cost of Energy" (LCOE). Unexpected downtime due to valve failure can cost operators millions. Our Double Ball Valve solutions are designed for longevity:
Low Torque Operation: By utilizing trunnion-mounted designs and advanced bearing materials, we reduce the operational torque, allowing for smaller, more cost-effective actuators and reducing wear on the stem seals.
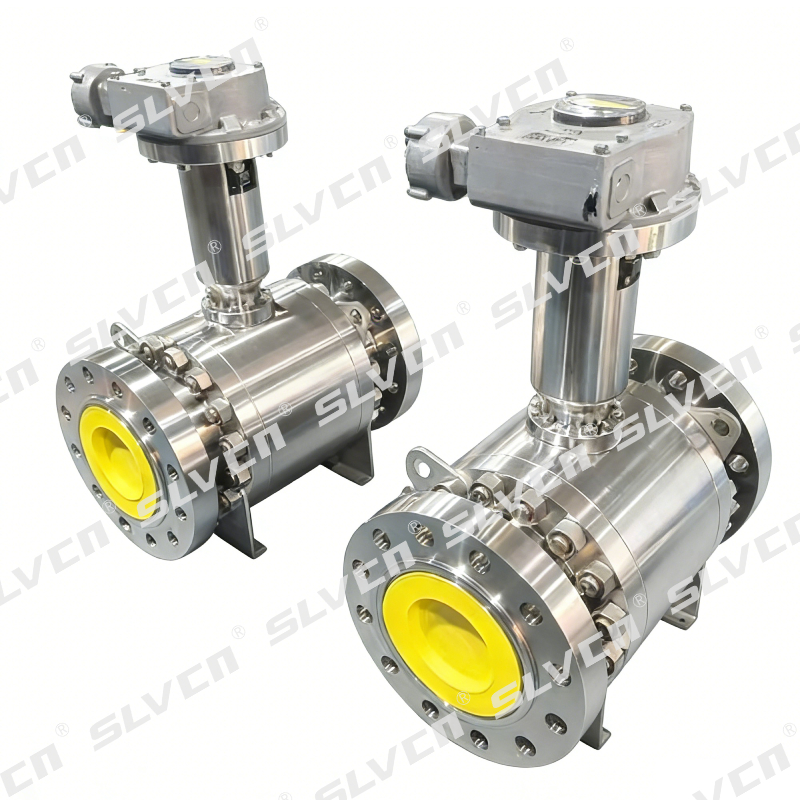
Ease of Maintenance: Our top-entry designs allow for in-line maintenance. Technicians can access the internal components without removing the valve body from the pipeline, which is vital for the complex piping systems found in CSP collector fields.
Rigorous Testing: Every valve undergoes shell tests, seat leakage tests (Rate A), and PMI material verification. For solar projects, we also offer high-temperature functional testing to simulate actual plant conditions before the valves leave our factory.
SLVCN is certified to ISO 9001, CE, and API standards. Our products comply with API 6D, ASME B16.34, DIN, ANSI, and JIS specifications. We operate dedicated cryogenic testing facilities to validate performance at temperatures down to −196°C, ensuring that every component meets the highest international standards.

Today, SLVCN serves customers in more than 100 countries, supplying valves to EPC contractors and end users across Europe, the Middle East, Southeast Asia, and the Americas.
Partner with SLVCN for engineered valve solutions that guarantee safety, efficiency, and long-term reliability in the most demanding solar thermal environments.
Contact Our Engineering Team


 18061659285