


Leave Your Message
High-performance forged carbon & alloy steel ball valves equipped with metal seats, scraper technology, and high-velocity hardfacings to withstand abrasive multi-phase slurry media.
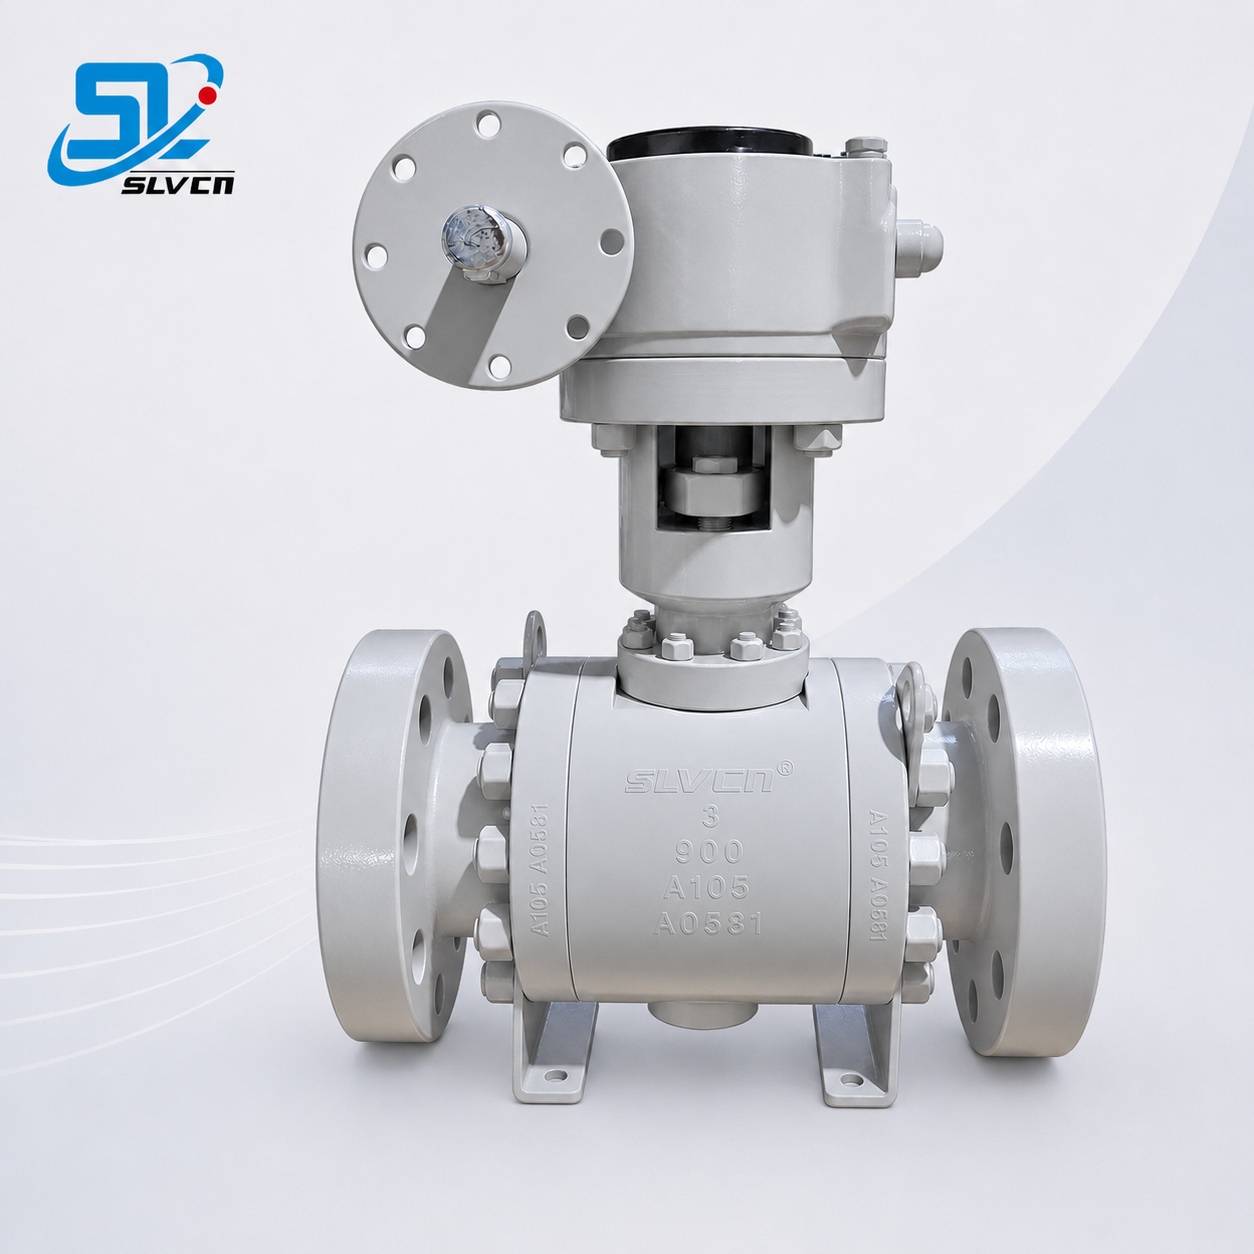
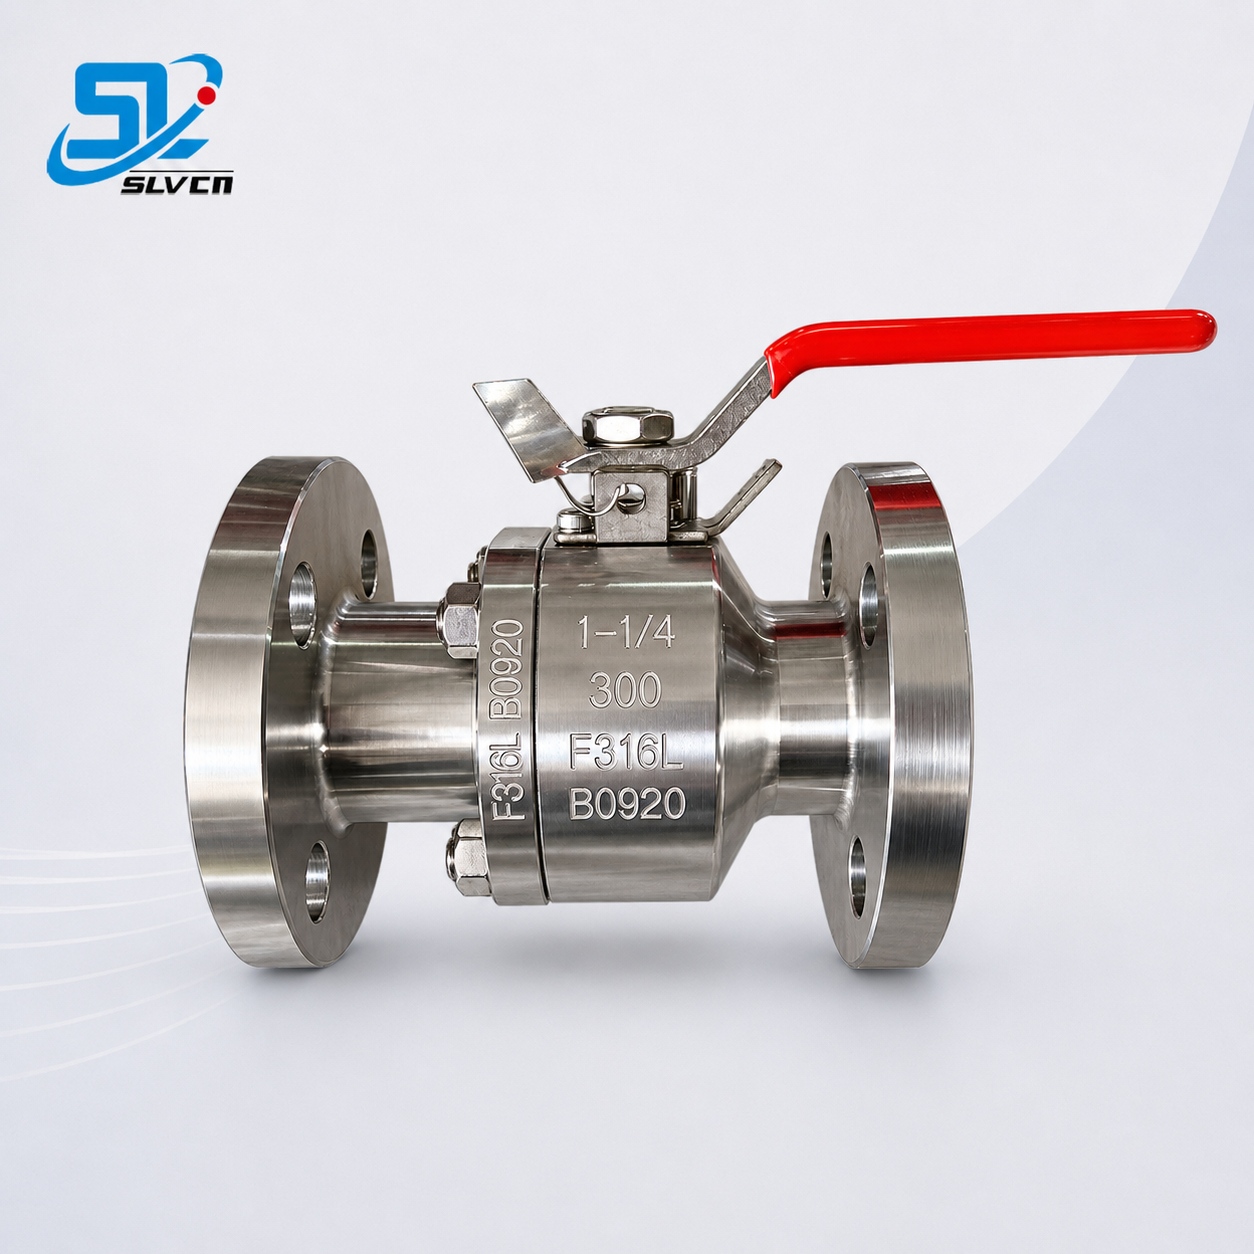
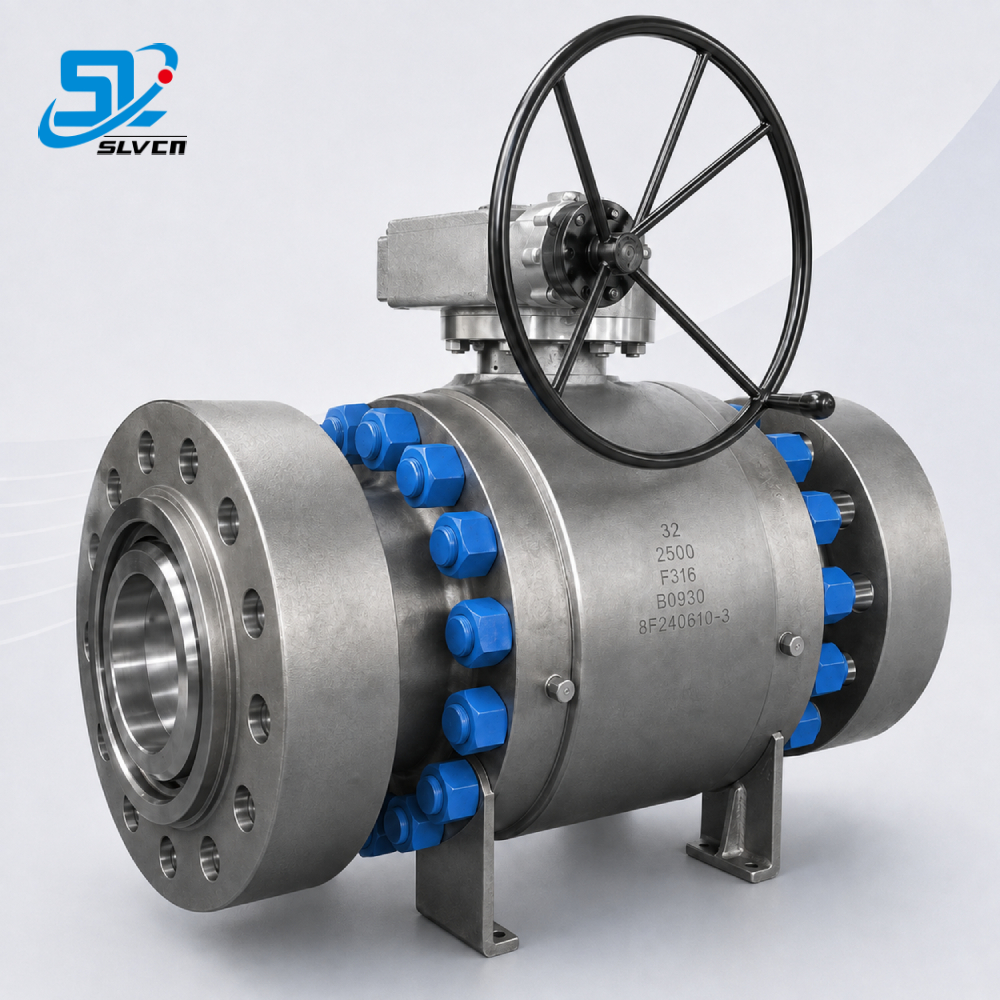
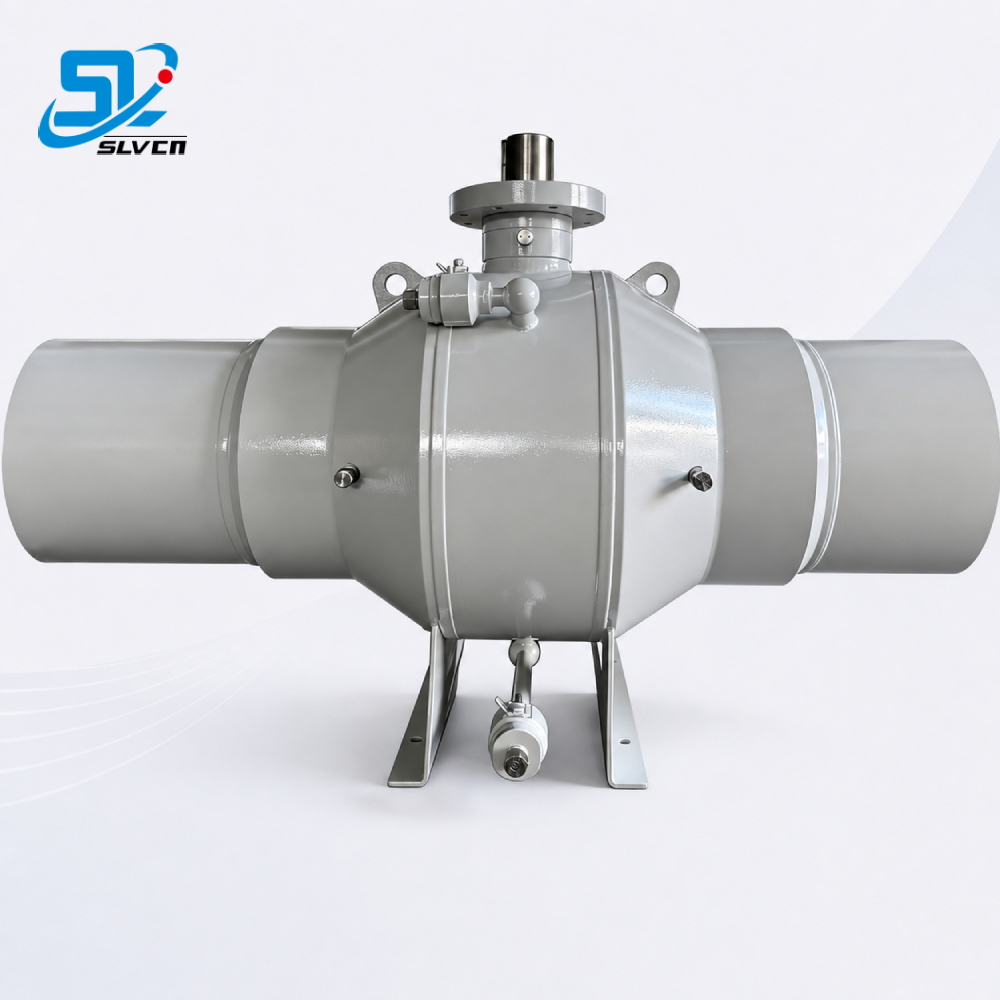
Understanding hydrodynamic erosion, solids impingement, and critical metallurgical requirements in severe slurry transport networks.
In modern industrial hydraulic transportation, abrasive slurry pipeline systems represent one of the most mechanically punishing operational environments. Whether transporting iron ore concentrates, bauxite, copper tailings, coal-water fuels, silica sand, or mineral process tailings across hundreds of kilometers, pipelines operate under high flow velocities and immense solid-particle loading. Under these extreme conditions, standard utility valves suffer rapid degradation, catastrophic seat washouts, stem binding, and wall thinning due to the combined effects of erosion, cavitation, and micro-abrasion.
The Carbon Steel Ball Valve—specifically manufactured utilizing high-density forged carbon steel grades such as ASTM A105N, LF2, and high-tensile alloy compositions—has emerged as the benchmark engineering solution for heavy slurry pipeline isolation. When engineered with severe-service metal-to-metal seating, proprietary tungsten carbide HVOF (High-Velocity Oxygen-Fuel) thermal coatings, and solid-deflecting scraper geometries, carbon steel ball valves deliver long-term structural integrity and bidirectional bubble-tight sealing (ISO 5208 Rate A) that conventional resilient-seated valves or pinch valves simply cannot achieve.
Capable of managing multi-phase slurries containing up to 65% to 75% solids by weight, resisting particle entrapment behind seats through precision spring-energized mechanisms.
Full-bore round cavity profile provides unrestricted flow matching pipe internal diameters, eliminating turbulence, localized eddy currents, and high-velocity impingement wear.
Micro-hardness exceeding 68–72 HRC via Tungsten Carbide (WC-Co-Cr) or Chrome Carbide coatings applied via hypersonic thermal spray to prevent micro-gouging and scratching.



With over 30 years of manufacturing experience, SLVCN is a professional designer and manufacturer of high-performance forged steel ball valves for critical industrial applications. We specialize in extreme working conditions including high pressure, high temperature, and cryogenic environments, providing safe and reliable flow control solutions for global industrial projects where operational reliability is non-negotiable.
Our core product range covers forged trunnion-mounted and floating ball valves, top-entry and side-entry ball valves, fully welded ball valves, metal seated ball valves, cryogenic ball valves, high-pressure ball valves up to Class 2500 (PN420) and customized higher pressure ratings, as well as high-temperature service valves. Compared with conventional cast valves, SLVCN forged valves feature higher material density, superior mechanical strength, improved resistance to pressure fluctuations and thermal shock, and significantly longer service life under severe service conditions.
Contact Our Technical TeamHigh-strength carbon steel substrates combined with state-of-the-art wear-resistant surface treatments engineered for high slurry velocities.
In slurry pipelines, abrasive particulate wear is accelerated when high hydraulic pressure forces sharp, angular mineral crystals (such as quartz, hematite, magnetite, or silica) across the sealing interface during open/close cycles. To guarantee operational survivability, the selection of the base forging material and hardfacing chemistry must be precisely tailored to slurry particle size distribution, solids percentage, carrier fluid pH, and pipeline operating pressure.
| Component | Material Specification | Surface Treatment / Coating | Key Performance Attribute in Slurry Service |
|---|---|---|---|
| Forged Valve Body | ASTM A105N / A350 LF2 / A694 F60/F65 | Epoxy Primer / Polyurethane / ENP Lining | Superior impact toughness, grain uniformity, zero porosity compared to castings; withstands water hammer. |
| Ball Core (Trim) | Forged Carbon Steel + F316 / F51 Duplex | HVOF Tungsten Carbide (WC-Co-Cr, 150-300 μm) | Surface hardness > 70 HRC. Extreme resistance to sliding abrasion, gouging, and fine-particle scour. |
| Metal Seat Rings | ASTM A182 F316 / F51 / Inconel 718 | HVOF Tungsten Carbide or Stellite Gr. 6 Overlay | Sharp scraper profile removes caked slurry cake from ball sphere during rotation; spring-energized sealing. |
| Stem Architecture | 17-4PH (UNS S17400) / Inconel 625 / XM-19 | QPQ / Nitriding / Hard Chrome Plated | Ultra-high torsional yield strength; anti-blowout shoulder with anti-static continuity to dissipate friction charges. |
| Seat Springs & O-Rings | Inconel X-750 Belleville Springs + HNBR/FKM | Enclosed Spring Cavity with Dirt Excluder Seals | Prevents solid slurry packing inside spring wells, maintaining constant mechanical contact with ball surface. |
Conventional valves fail in slurry duty because particles migrate into the cavity behind the seat rings, packing tightly and preventing the seat from flexing. SLVCN carbon steel slurry ball valves integrate a secondary dirt excluder seal ring combined with an active scraper leading edge on the metal seat. As the ball rotates, the scraper edge mechanically shears off consolidated slurry film, ensuring clean metal-to-metal seating without wedging or particulate seizure.
Designed for High Pressure, High Temperature, and Cryogenic Applications, SLVCN valves are widely used in long-distance oil & gas transmission pipelines, LNG storage and regasification terminals, offshore platforms and deepwater projects, power plants, refineries, compressor stations, and high-pressure chemical processing units. Whether handling flammable media, corrosive fluids, sour service media (H₂S), ultra-low temperatures, or extreme differential pressures, our valves ensure stable operation, bubble-tight shut-off, and maximum system safety in accordance with international sealing and performance standards.

Standardized compliance across API 6D, ASME B16.34, ISO 15848 low-fugitive emission, and NACE MR0175 sour gas specifications.

Safety and reliability are embedded in every design. Our forged ball valves are equipped with Double Block and Bleed (DBB) structures, anti-blowout stems, fire-safe designs in accordance with API 607 / API 6FA, anti-static devices, emergency sealing systems, and pressure-balanced seating structures suitable for high differential pressure operation. Valves can be designed with SPE (Single Piston Effect) or DPE (Double Piston Effect) seat configurations based on application requirements. For sour service environments, materials and sealing systems comply with NACE MR0175 / ISO 15156 requirements.
From mineral tailings dams to coal gasification black water circuits, where carbon steel metal-seated ball valves provide irreplaceable operational security.
Long-distance hydraulic pipelines conveying iron ore and copper concentrate over 100–400 km under high operating pressures (Class 600 to Class 1500), where seat failure causes catastrophic shutdown.
Managing high-temperature "black water" and "grey water" slurries loaded with fine char particles and fly ash in entrained-flow coal gasifiers, operating up to 280°C under severe differential pressure.
Thermal power plant FGD limestone slurry recirculation loops requiring forged carbon steel valves with corrosion/erosion-resistant claddings to overcome scaling, pitting, and crystalline buildup.
Underground paste backfill distribution and high-volume surface tailings storage facility (TSF) decant discharge lines, maintaining bubble-tight isolation to safeguard environmental ecosystems.
Digestion circuits operating with highly alkaline caustic red mud slurries at elevated temperatures, requiring high-strength forged carbon steel bodies with erosion-resistant nickel alloys or stellite trims.
Bitumen extraction pipelines carrying quartz-heavy oil sands slurry at high flow rates, demanding trunnion-supported valves with hardened tungsten carbide trims to prevent rapid wall thinning.
Every valve undergoes rigorous non-destructive examination, hydrostatic shell testing, and zero-leakage seat verification to guarantee absolute field dependability.
To ensure consistent quality, each valve undergoes a complete series of inspections and performance tests in accordance with API 6D, API 598, and ISO 5208, including shell test, seat leakage test (Rate A / zero visible leakage), fire-safe test, cryogenic test, operational torque test, dimensional inspection, and PMI material verification. SLVCN operates dedicated cryogenic testing facilities to validate valve performance at ultra-low temperatures down to −196°C.
SLVCN is certified to ISO 9001, CE, and API standards, and our products comply with API 6D, ASME B16.34, DIN, ANSI, and JIS specifications. We provide extensive customization capabilities covering sizes from 1/2″ to 36″, full bore or reduced bore, special materials including A105, LF2, F11, F22, F51, Inconel, various soft and metal seat designs, and intelligent actuation with pneumatic, electric, and gear operators.
Today, SLVCN serves customers in more than 100 countries and regions, supplying valves to EPC contractors, engineering companies, and end users across Europe, the Middle East, Southeast Asia, and the Americas. Backed by strong engineering expertise, advanced manufacturing, and rigorous quality control, SLVCN is committed to delivering safe, durable, and truly engineered valve solutions for the world’s most demanding industrial projects.
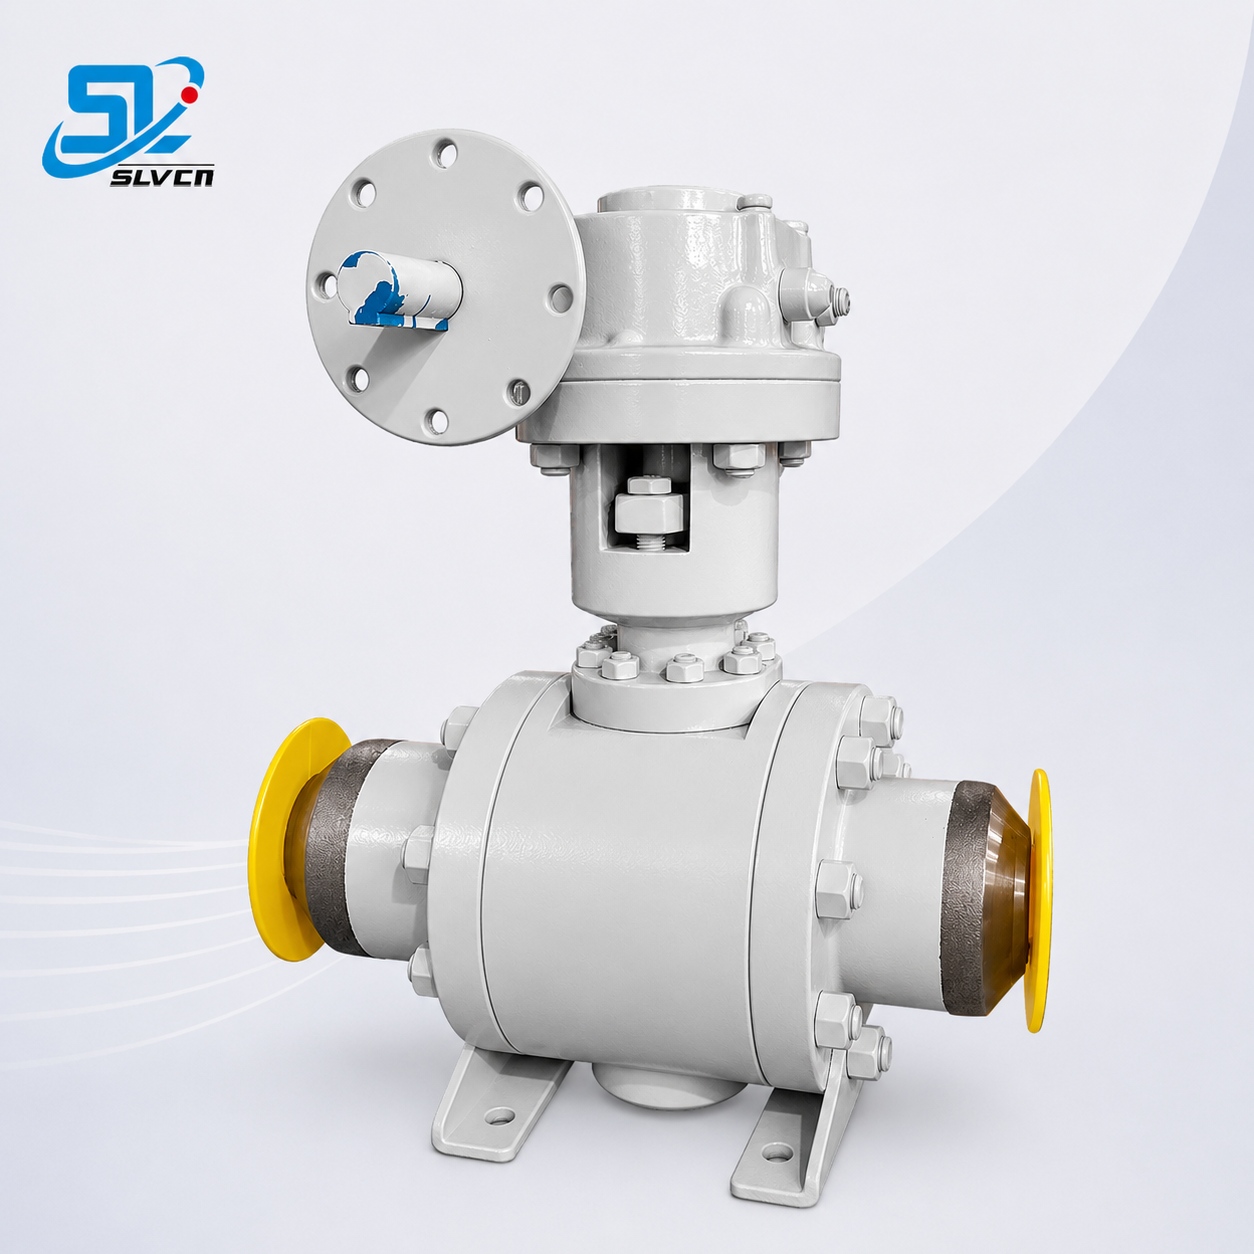
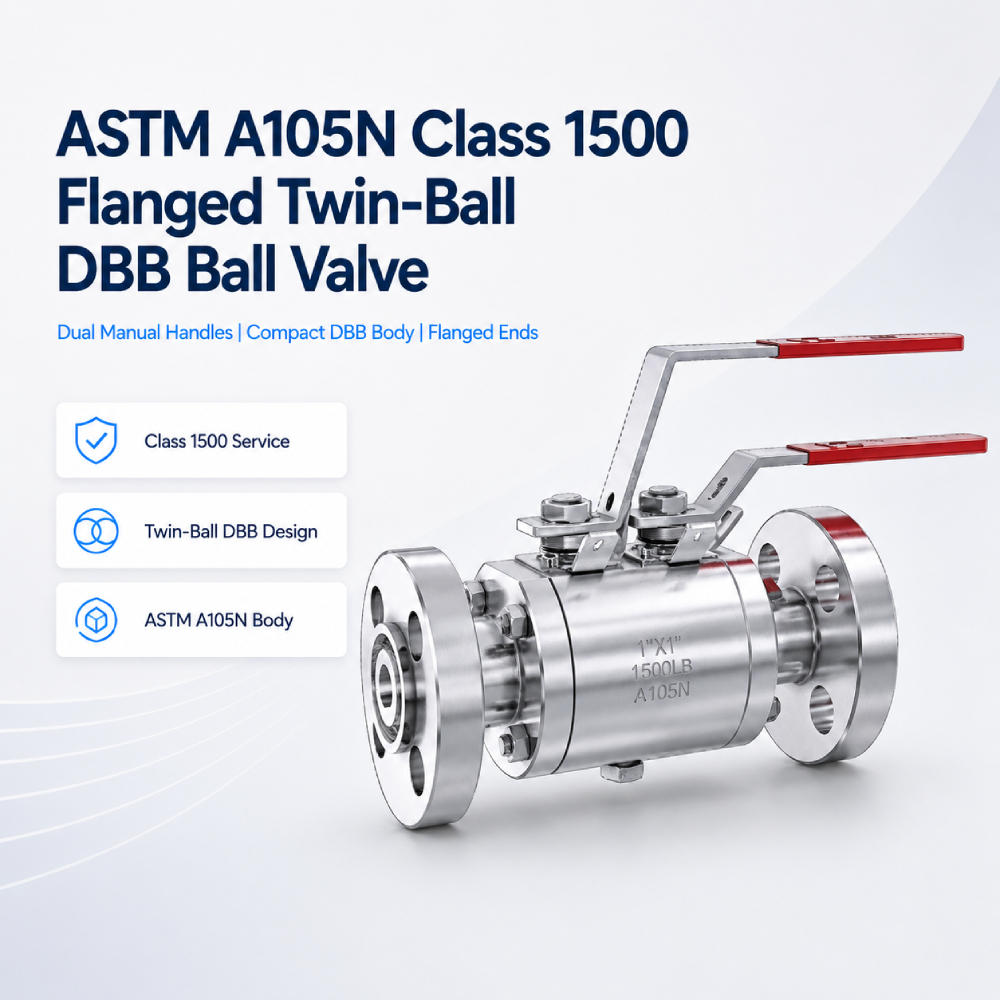
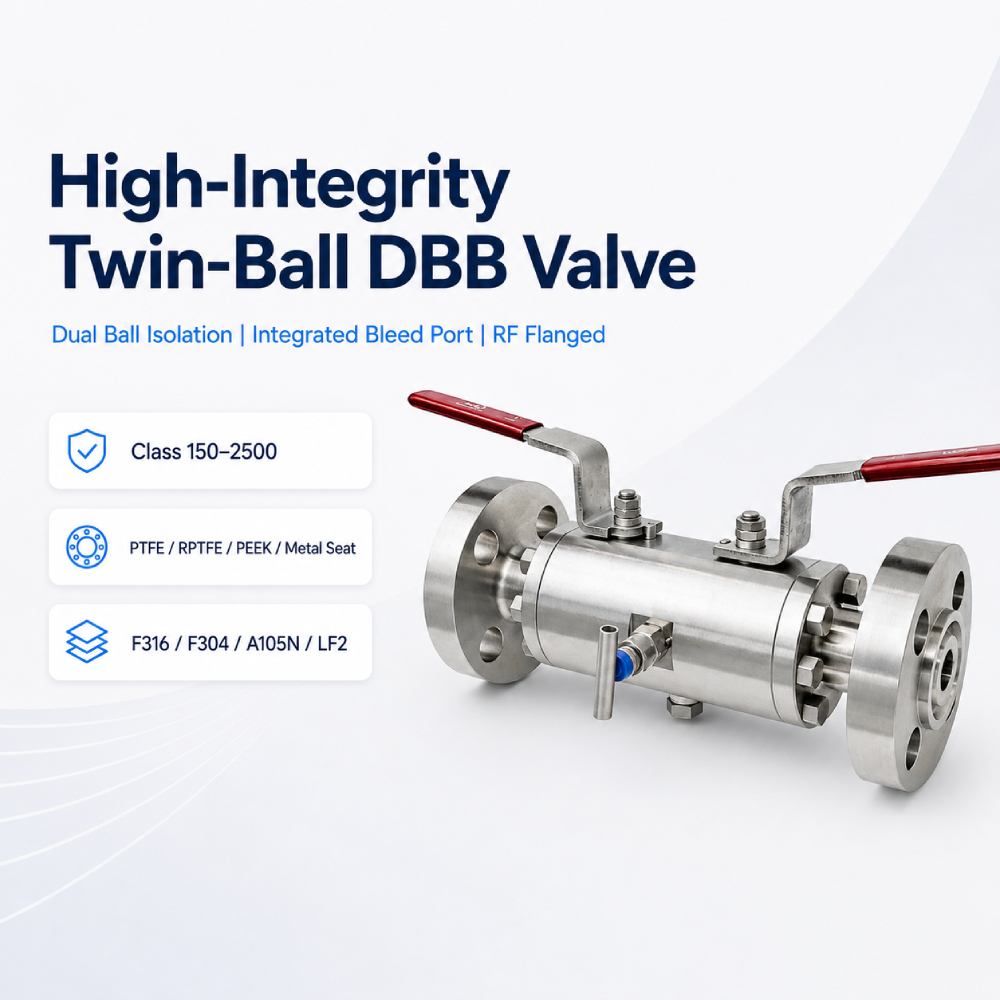
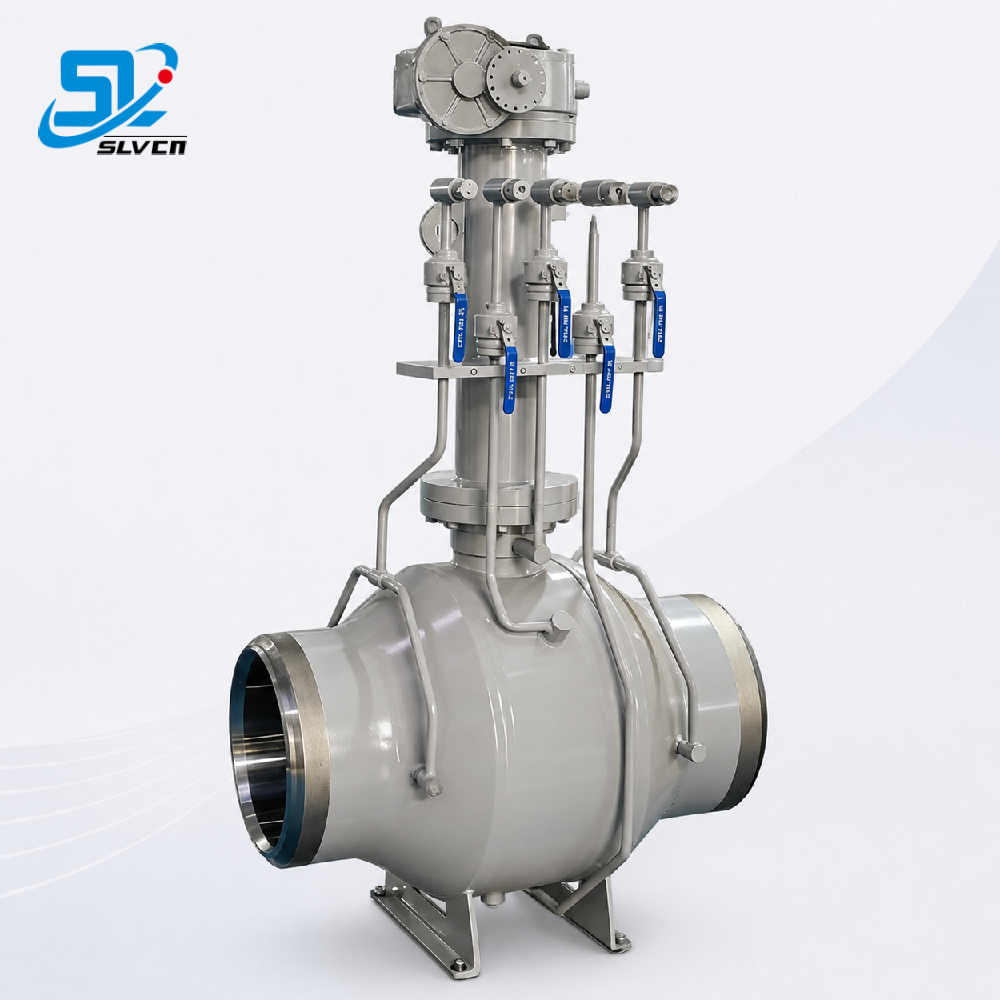
Discover our complete range of trunnion-mounted, floating, high-pressure, metal-seated, and fully welded double block and bleed (DBB) ball valves.


 18061659285

