Leave Your Message
Explore our comprehensive range of high-performance forged steel ball valves designed for Mumbai's demanding industrial applications
Mumbai, India's financial capital and industrial powerhouse, stands as a critical hub for valve manufacturing and distribution in the Asia-Pacific region. The city's strategic location on the western coast, combined with its world-class port infrastructure including Jawaharlal Nehru Port Trust (JNPT) and Mumbai Port, positions it as an ideal gateway for both domestic distribution and international export of industrial valves, particularly carbon steel ball valves.
The Mumbai Metropolitan Region (MMR) hosts a diverse industrial ecosystem spanning oil and gas processing, petrochemicals, power generation, pharmaceuticals, chemical manufacturing, and marine applications. Major industrial zones including the Mumbai-Pune Industrial Corridor, Thane-Belapur Industrial Belt, and the developing Navi Mumbai Special Economic Zone create substantial demand for high-quality carbon steel ball valves.
The presence of major refineries such as Bharat Petroleum Corporation Limited (BPCL) refinery and Hindustan Petroleum Corporation Limited (HPCL) facilities in the Mumbai region, along with numerous chemical processing plants in the MIDC (Maharashtra Industrial Development Corporation) areas, drives continuous demand for reliable flow control solutions. These facilities require valves capable of handling corrosive media, high pressures, and extreme temperature variations—specifications that premium carbon steel ball valves are designed to meet.
Mumbai serves as a critical node in India's oil and gas infrastructure. The city's proximity to offshore oil fields in the Arabian Sea, including the Mumbai High fields operated by Oil and Natural Gas Corporation (ONGC), creates significant demand for specialized valves for offshore platforms, subsea applications, and onshore processing facilities. Carbon steel ball valves with anti-corrosion coatings and marine-grade specifications are essential for these harsh operating environments.
Several factors are accelerating the demand for high-performance carbon steel ball valves in Mumbai:
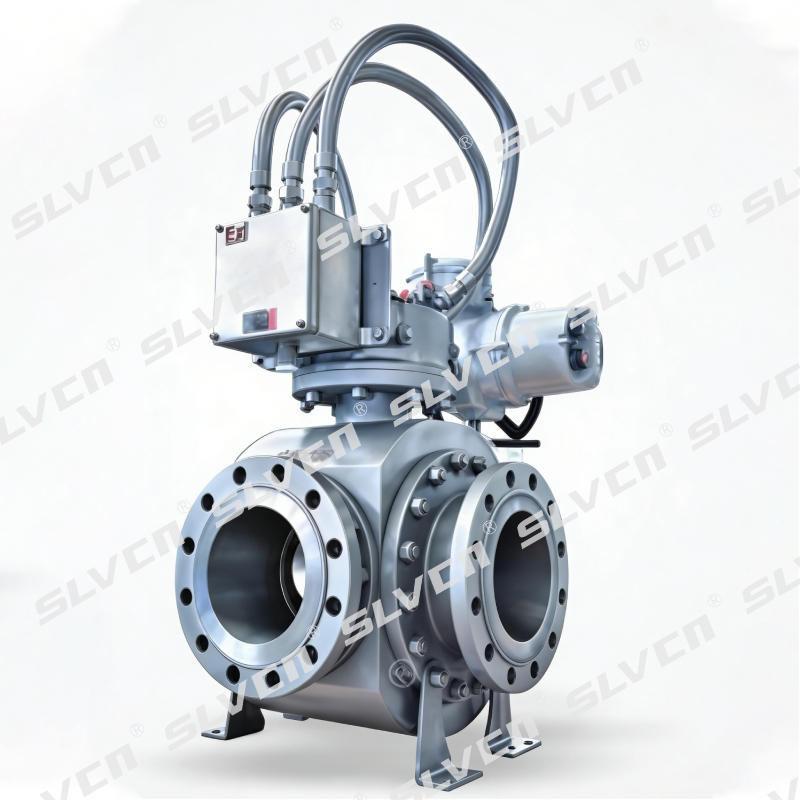
Mumbai's industrial sector is increasingly adopting Industry 4.0 technologies. Modern carbon steel ball valves are now being integrated with smart actuators, position sensors, and IoT connectivity, enabling real-time monitoring, predictive maintenance, and remote operation. This digital transformation is particularly evident in new installations at refineries, chemical plants, and offshore platforms serving the Mumbai region.
Development of enhanced carbon steel alloys and specialized coatings to resist corrosion in Mumbai's coastal industrial environment
Valves engineered for high differential pressure, thermal shock resistance, and severe service conditions common in process industries
Implementation of fire-safe designs, double block and bleed configurations, and fugitive emission control complying with international standards
Environmental regulations in Maharashtra, including stricter emission norms and fugitive emission standards, are driving demand for low-emission valve designs. Carbon steel ball valves with advanced stem sealing systems, anti-static devices, and fire-safe certifications are becoming mandatory in many applications. Mumbai-based industries are increasingly specifying valves that comply with API 607, API 6FA, ISO 15848, and NACE MR0175 standards.
The Indian government's "Make in India" initiative has encouraged local manufacturing of high-quality industrial valves. While Mumbai itself has limited heavy manufacturing space due to urban density, the surrounding regions in Maharashtra and Gujarat host numerous valve manufacturing facilities that serve the Mumbai market. However, there remains significant demand for premium imported valves from established manufacturers, particularly for critical applications where reliability is non-negotiable.
The Mumbai High oil fields, located approximately 160 kilometers off the Mumbai coast, represent one of India's largest offshore oil and gas producing regions. These platforms require specialized carbon steel ball valves designed for:
The BPCL Mumbai Refinery in Mahul and surrounding petrochemical facilities process millions of tons of crude oil annually. These operations demand carbon steel ball valves for:
Mumbai's transition toward cleaner fuels has accelerated LNG adoption. The city's gas distribution infrastructure, operated by Mahanagar Gas Limited (MGL) and industrial consumers, requires specialized cryogenic ball valves for LNG storage, regasification, and distribution systems. These valves must maintain zero leakage at temperatures as low as -196°C while providing reliable shut-off for safety-critical applications.
Thermal power plants in and around Mumbai, including the Dahanu Thermal Power Station and various captive power plants, utilize carbon steel ball valves in:
Mumbai's Thane-Belapur belt hosts numerous chemical and pharmaceutical manufacturing units requiring precise flow control. Applications include:
Mumbai's status as a major port city and shipbuilding center creates demand for marine-grade carbon steel ball valves for:
Mumbai's humid, salt-laden coastal atmosphere presents significant corrosion challenges for industrial equipment. Carbon steel ball valves deployed in Mumbai require:
The Mumbai valve market faces challenges with substandard and counterfeit products. End users increasingly demand:
Project timelines in Mumbai's fast-paced industrial environment demand reliable supply chains. Solutions include:
Carbon steel ball valves for Mumbai applications typically utilize:
Mumbai's diverse industrial applications require valves across various pressure classes:
Valves supplied to Mumbai projects must comply with international standards:

Over 30 years of manufacturing experience


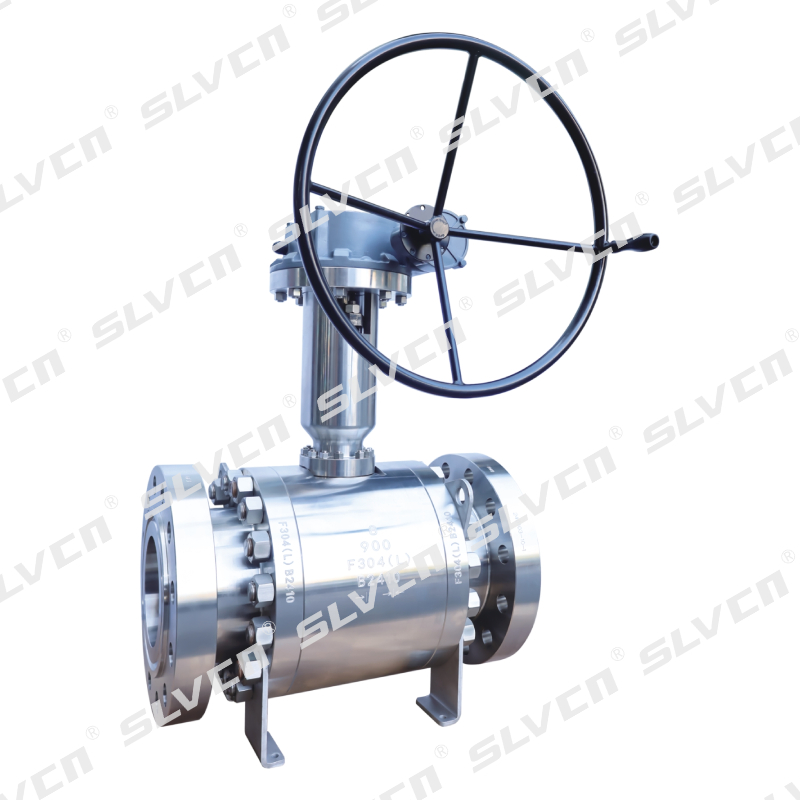
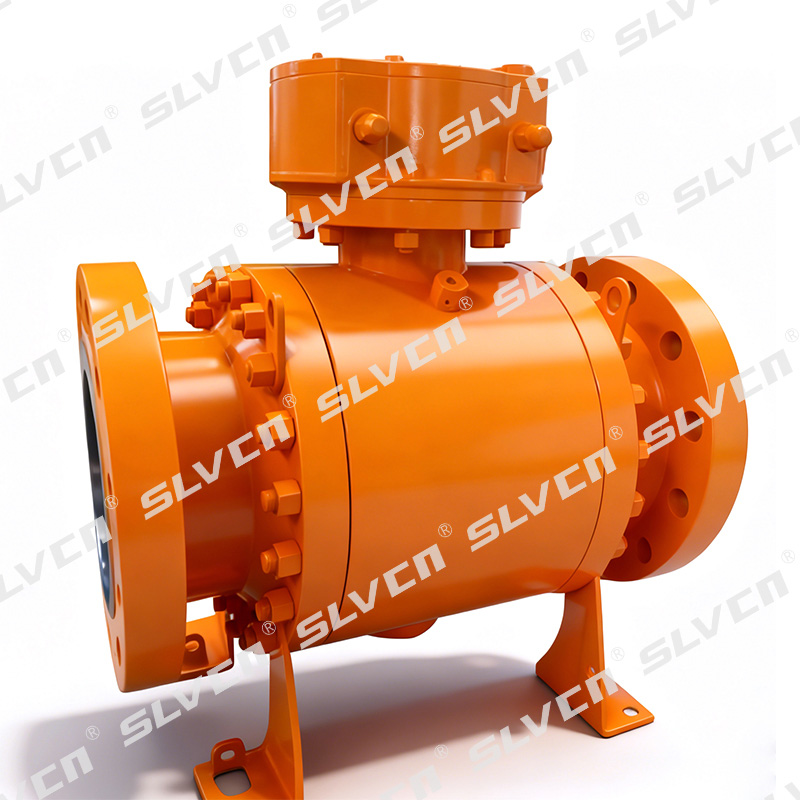
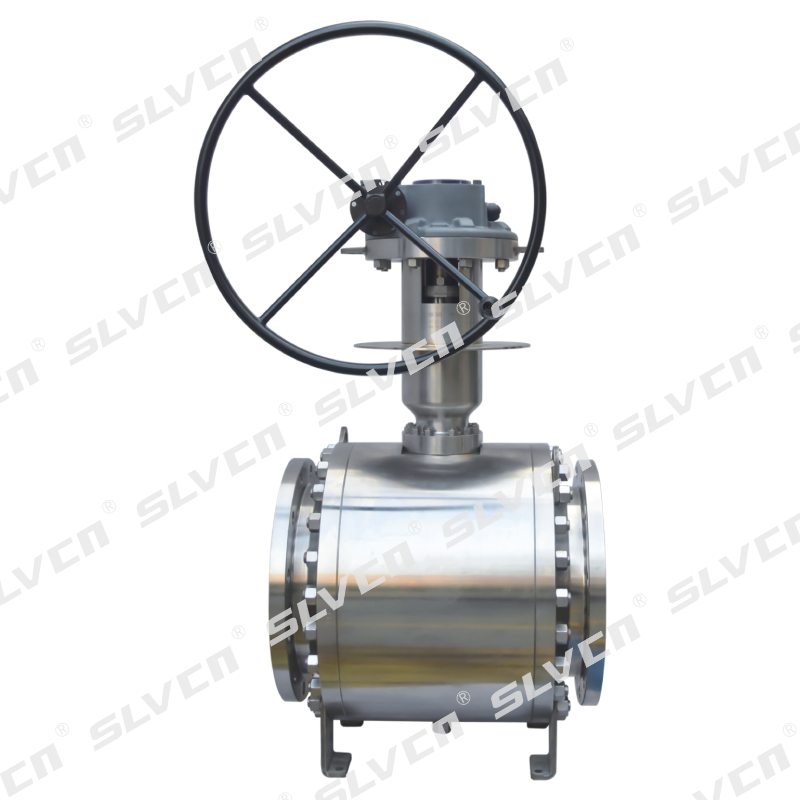
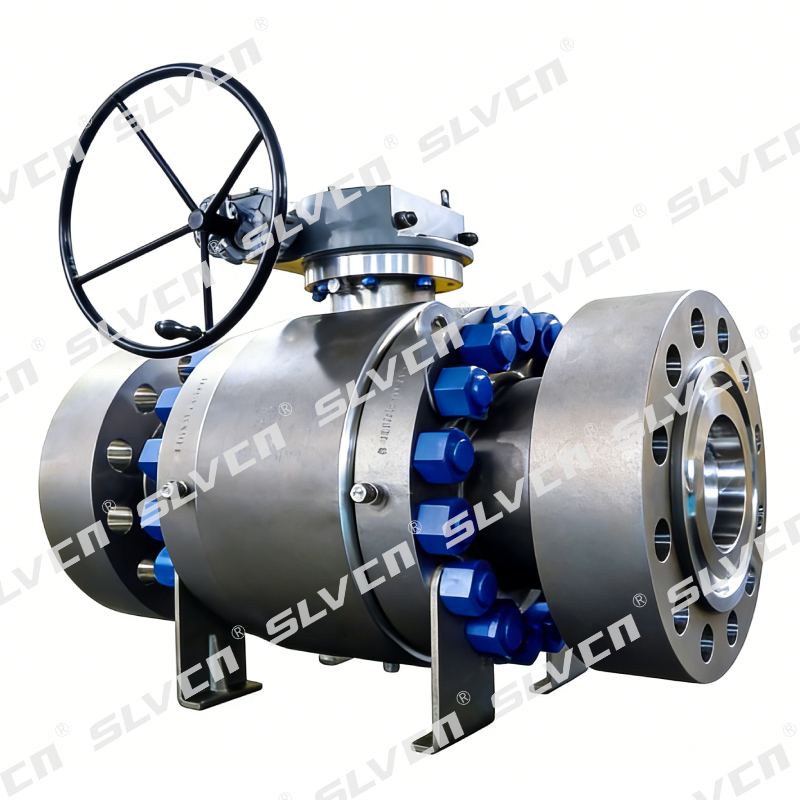
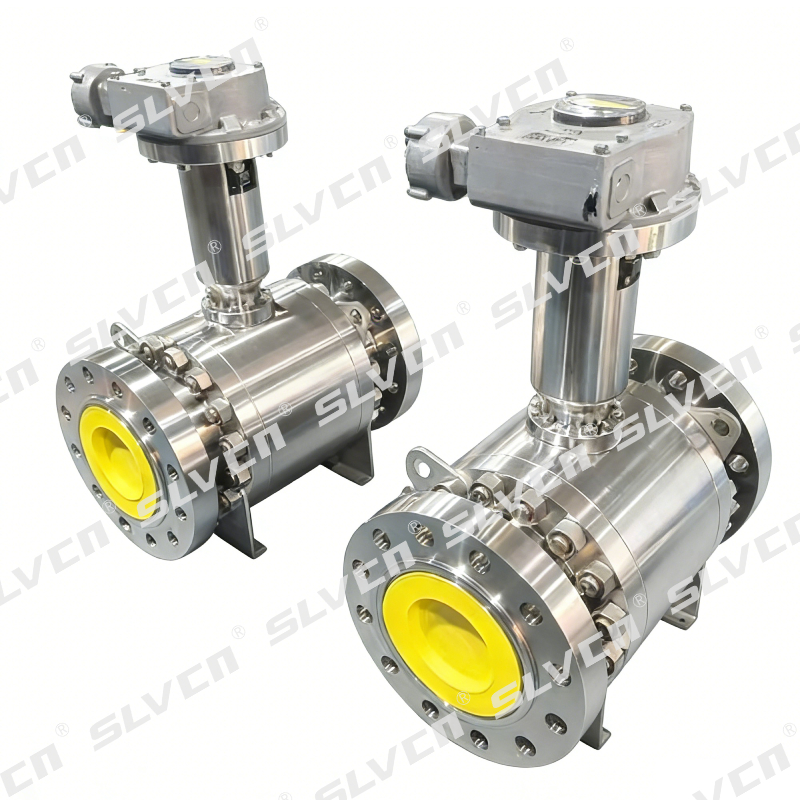
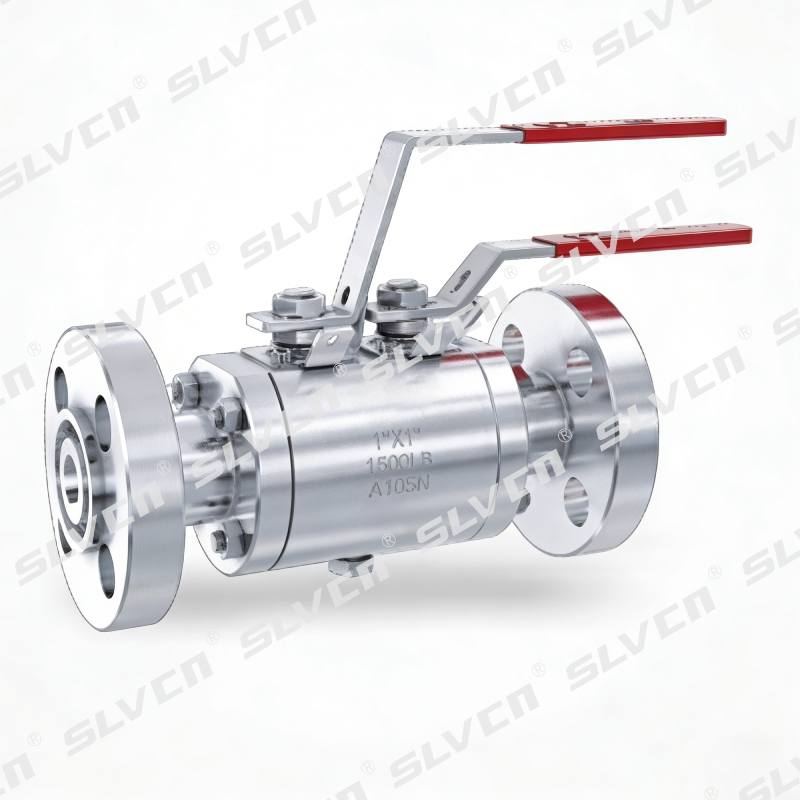
Our core product range covers forged trunnion-mounted and floating ball valves, top-entry and side-entry ball valves, fully welded ball valves, metal seated ball valves, cryogenic ball valves, high-pressure ball valves up to Class 2500 (PN420) and customized higher pressure ratings, as well as high-temperature service valves. Compared with conventional cast valves, SLVCN forged valves feature higher material density, superior mechanical strength, improved resistance to pressure fluctuations and thermal shock, and significantly longer service life under severe service conditions.
Designed for High Pressure, High Temperature, and Cryogenic Applications, SLVCN valves are widely used in long-distance oil & gas transmission pipelines, LNG storage and regasification terminals, offshore platforms and deepwater projects, power plants, refineries, compressor stations, and high-pressure chemical processing units. Whether handling flammable media, corrosive fluids, sour service media (H₂S), ultra-low temperatures, or extreme differential pressures, our valves ensure stable operation, bubble-tight shut-off, and maximum system safety in accordance with international sealing and performance standards.


Comprehensive valve solutions engineered for reliability in critical industrial applications
Selecting a reliable valve supplier for Mumbai's demanding industrial applications requires careful consideration of several factors: manufacturing quality, compliance with international standards, material traceability, testing capabilities, technical support, and after-sales service. The harsh operating conditions in Mumbai's industrial facilities—ranging from corrosive coastal atmospheres to high-pressure petrochemical processes—demand valves that are engineered for reliability, not just price competitiveness.
With over 30 years of manufacturing experience and a proven track record in supplying high-performance forged steel ball valves to demanding industrial projects worldwide, SLVCN offers Mumbai's industrial sector access to world-class valve technology. Our comprehensive product range, rigorous quality control, international certifications, and commitment to customer support make us an ideal partner for your critical flow control requirements.
Whether you're involved in offshore oil and gas development, refinery operations, LNG terminals, power generation, chemical processing, or any other critical industrial application in the Mumbai region, SLVCN's forged carbon steel ball valves provide the reliability, safety, and performance your projects demand. Our valves are designed to withstand the unique challenges of Mumbai's industrial environment while delivering years of trouble-free operation.
For technical inquiries, product specifications, or project-specific requirements, our experienced engineering team is ready to provide comprehensive support. We understand the critical nature of valve selection in industrial applications and are committed to helping you choose the optimal solution for your specific operating conditions.


 +86 18905154687