


Leave Your Message
Explore our high-performance forged and welded carbon steel ball valves configured for critical British infrastructure applications.
The United Kingdom's industrial sector is undergoing a profound transformation. As the nation targets Net-Zero carbon emissions by 2050, the demand for highly reliable flow control components like carbon steel ball valves is reaching new technical heights. From the traditional offshore oil and gas extraction fields in the North Sea to the rapidly developing hydrogen networks and Carbon Capture, Utilization, and Storage (CCUS) projects in industrial clusters like Teesside, Humber, and Grangemouth, high-integrity valves are critical to system safety.
Carbon steel remains the material of choice for high-pressure piping systems across Great Britain due to its excellent tensile strength, impact resistance, and cost-effectiveness. In the UK's demanding marine and sub-zero environments, specifications such as ASTM A105 (forged carbon steel) and ASTM A350 LF2 (low-temperature carbon steel) are standard requirements to prevent brittle fractures. As UK engineering, procurement, and construction (EPC) contractors design the next generation of energy infrastructure, they require suppliers who comply with stringent European and international certifications, ensuring absolute sealing performance under pressure fluctuations.



With over 30 years of manufacturing experience, SLVCN is a professional designer and manufacturer of high-performance forged steel ball valves for critical industrial applications. We specialize in extreme working conditions including high pressure, high temperature, and cryogenic environments, providing safe and reliable flow control solutions for global industrial projects where operational reliability is non-negotiable.
Through our dedicated engineering team and state-of-the-art testing facilities, SLVCN bridges the gap between high-precision Chinese manufacturing and the strict safety requirements of United Kingdom operators. Our valves are designed to meet the rigorous demands of British standards, offering an optimal balance of cost-efficiency and uncompromising quality.
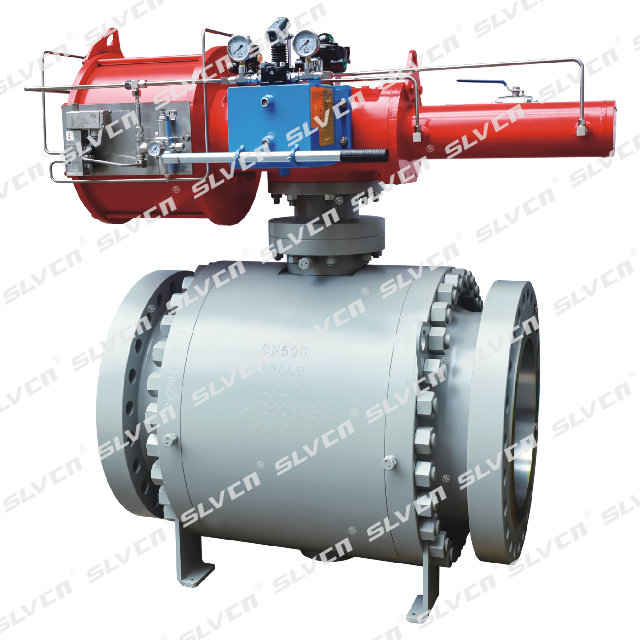
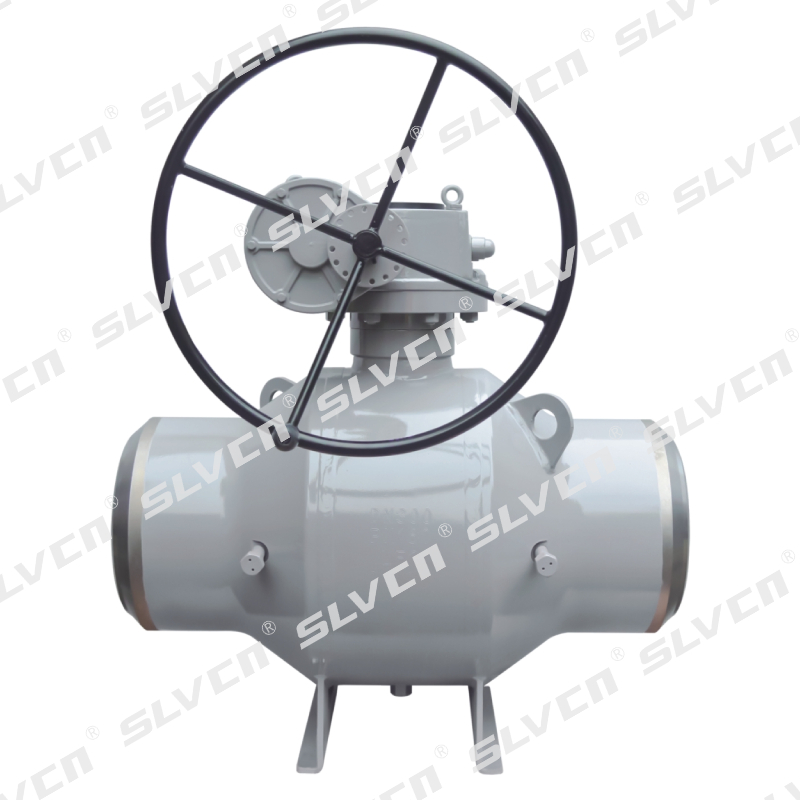
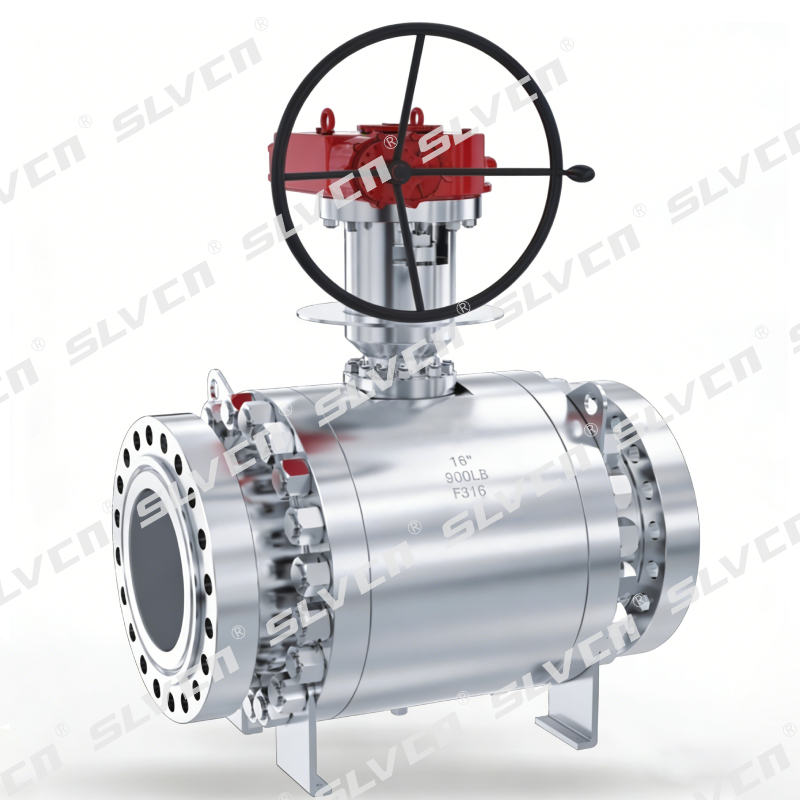
Inquire for UK ProjectsOur core product range covers forged trunnion-mounted and floating ball valves, top-entry and side-entry ball valves, fully welded ball valves, metal seated ball valves, cryogenic ball valves, high-pressure ball valves up to Class 2500 (PN420) and customized higher pressure ratings, as well as high-temperature service valves. Compared with conventional cast valves, SLVCN forged valves feature higher material density, superior mechanical strength, improved resistance to pressure fluctuations and thermal shock, and significantly longer service life under severe service conditions.
1. North Sea Offshore Platforms & Deepwater Operations: Our high-pressure metal-seated trunnion valves are deployed to withstand corrosive saline environments and high differential pressures on oil & gas production platforms.
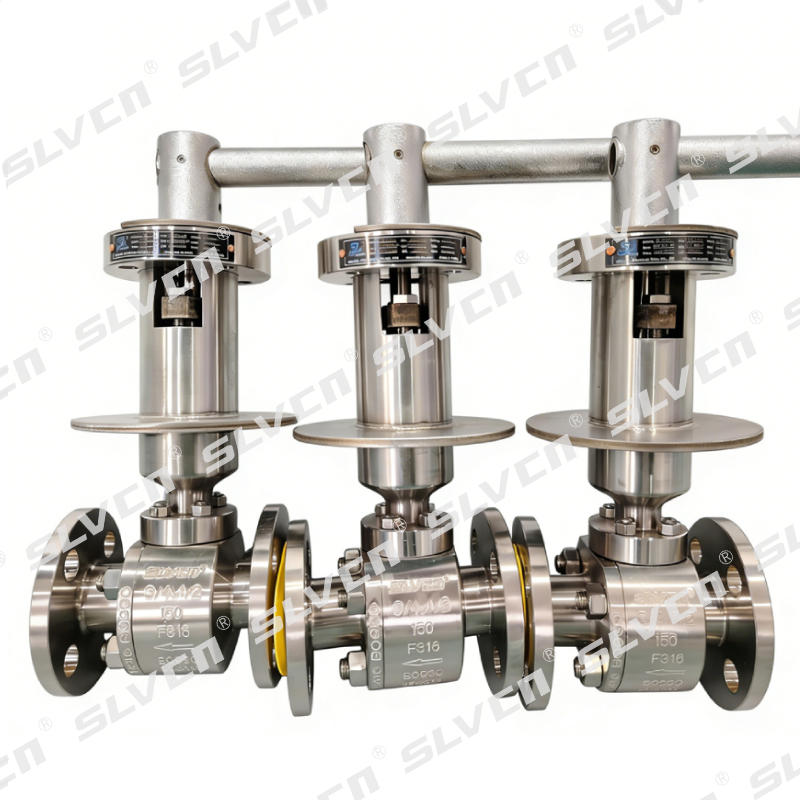
2. UK LNG Import Terminals (Isle of Grain, South Hook, Dragon): Cryogenic ball valves engineered to operate reliably at temperatures down to -196°C, ensuring safe isolation during LNG unloading, storage, and regasification.
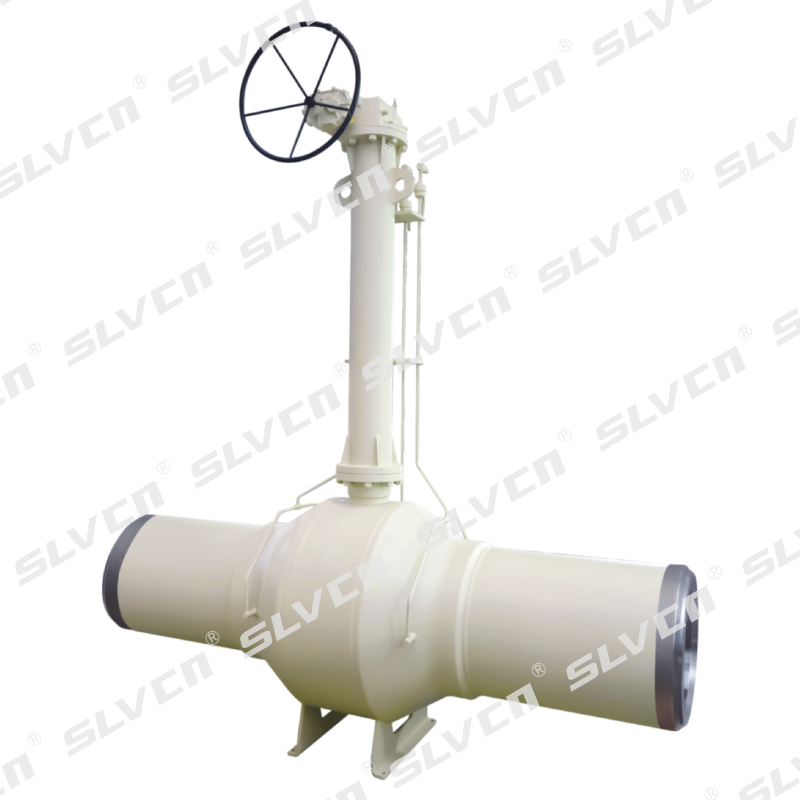
3. High-Pressure Gas Grid Isolation: Fully welded buried ball valves with extended stems allow maintenance crews to isolate major gas transmission pipelines across Scotland, England, and Wales without gas escape.

Whether handling flammable media, corrosive fluids, sour service media (H₂S), ultra-low temperatures, or extreme differential pressures, our valves ensure stable operation, bubble-tight shut-off, and maximum system safety in accordance with international sealing and performance standards.

Safety and reliability are embedded in every design. Our forged ball valves are equipped with Double Block and Bleed (DBB) structures, anti-blowout stems, fire-safe designs in accordance with API 607 / API 6FA, anti-static devices, emergency sealing systems, and pressure-balanced seating structures suitable for high differential pressure operation. Valves can be designed with SPE (Single Piston Effect) or DPE (Double Piston Effect) seat configurations based on application requirements. For sour service environments, materials and sealing systems comply with NACE MR0175 / ISO 15156 requirements, which is a key necessity for UK North Sea applications.
To ensure consistent quality, each valve undergoes a complete series of inspections and performance tests in accordance with API 6D, API 598, and ISO 5208, including shell test, seat leakage test (Rate A / zero visible leakage), fire-safe test, cryogenic test, operational torque test, dimensional inspection, and PMI material verification. SLVCN operates dedicated cryogenic testing facilities to validate valve performance at ultra-low temperatures down to -196°C.
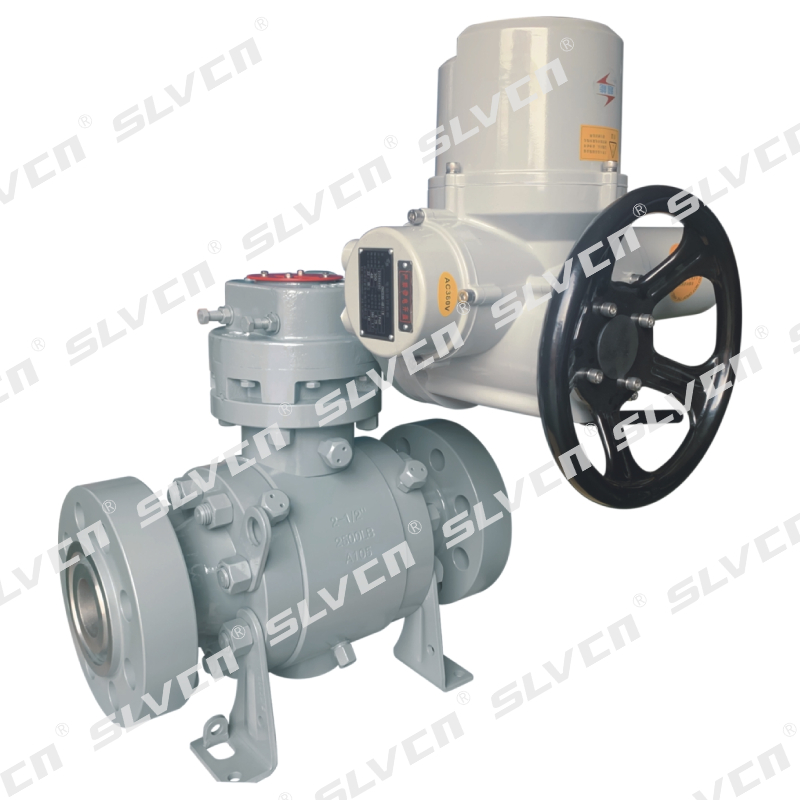
SLVCN is certified to ISO 9001, CE, and API standards, and our products comply with API 6D, ASME B16.34, DIN, ANSI, and JIS specifications. We provide extensive customization capabilities covering sizes from 1/2” to 36”, full bore or reduced bore, special materials including A105, LF2, F11, F22, F51, Inconel, various soft and metal seat designs, and intelligent actuation with pneumatic, electric, and gear operators.
Today, SLVCN serves customers in more than 100 countries and regions, supplying valves to EPC contractors, engineering companies, and end users across Europe, the Middle East, Southeast Asia, and the Americas. Backed by strong engineering expertise, advanced manufacturing, and rigorous quality control, SLVCN is committed to delivering safe, durable, and truly engineered valve solutions for the world’s most demanding industrial projects.
For British engineering companies managing projects locally in the UK or globally in the North Sea, Middle East, or Africa, SLVCN offers rapid design verification, transparent material traceability (EN 10204 3.1 & 3.2), and reliable delivery timelines. We ensure that our forged carbon steel ball valves seamlessly integrate with complex automated control systems, providing the ultimate safety barrier in critical pipelines.
Select from our comprehensive line of valves engineered for high-pressure, cryogenic, and high-temperature service across the UK chemical, gas, and energy sectors.


 18061659285

