


Leave Your Message
Advanced hermetic welding, thermal shock dissipation, and metal-to-metal sealing for molten salt and high-pressure steam utility circuits.
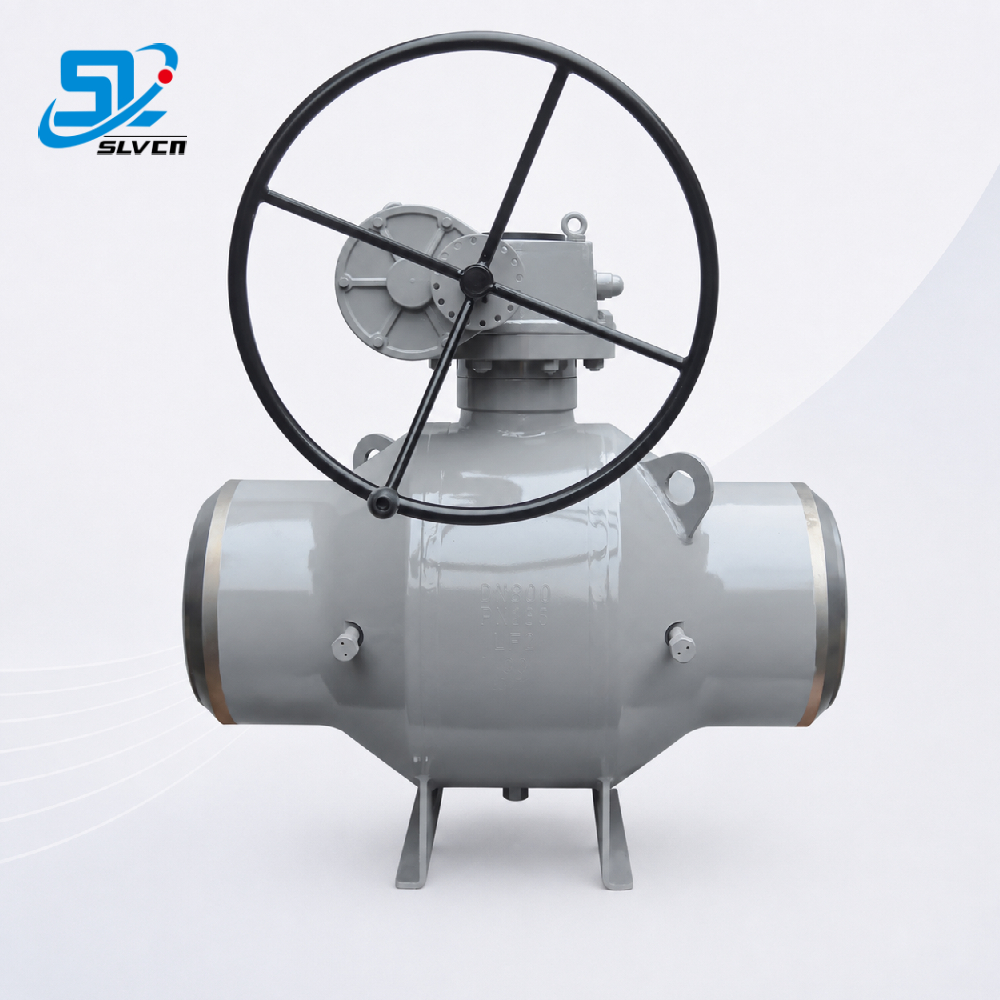
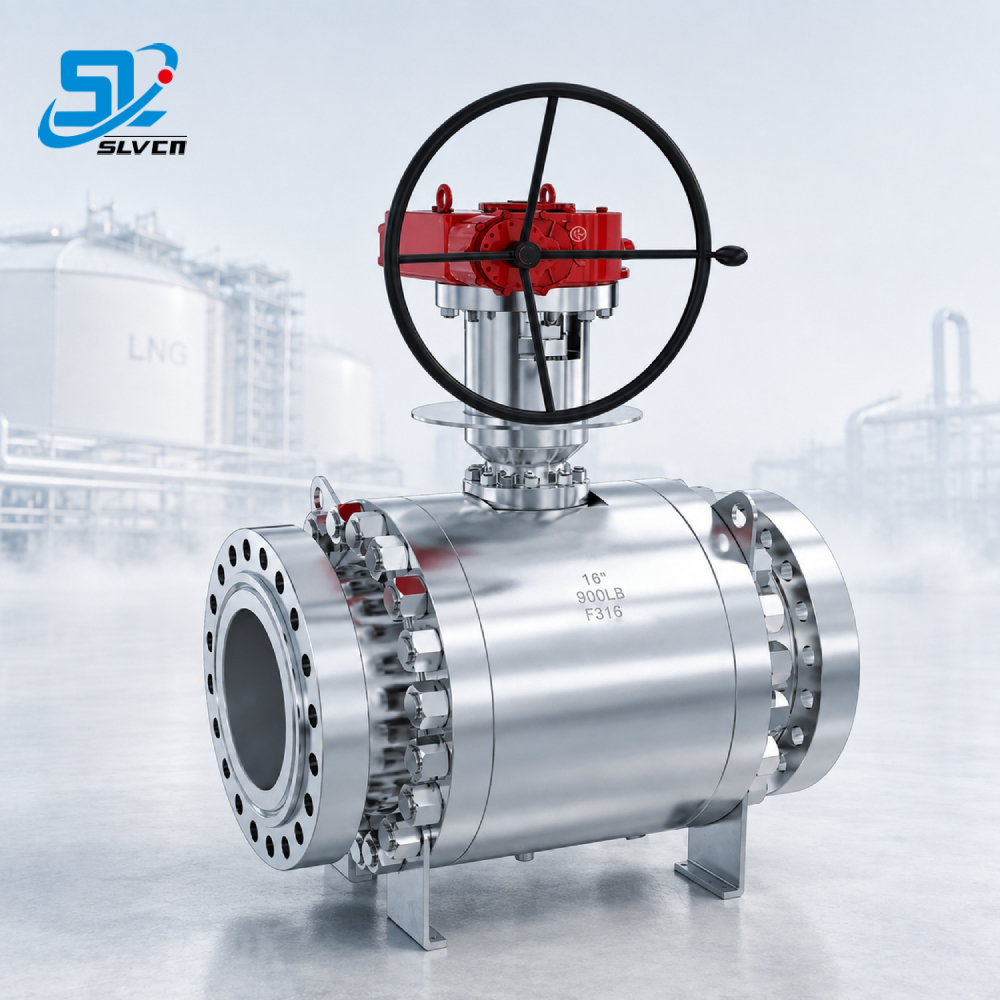
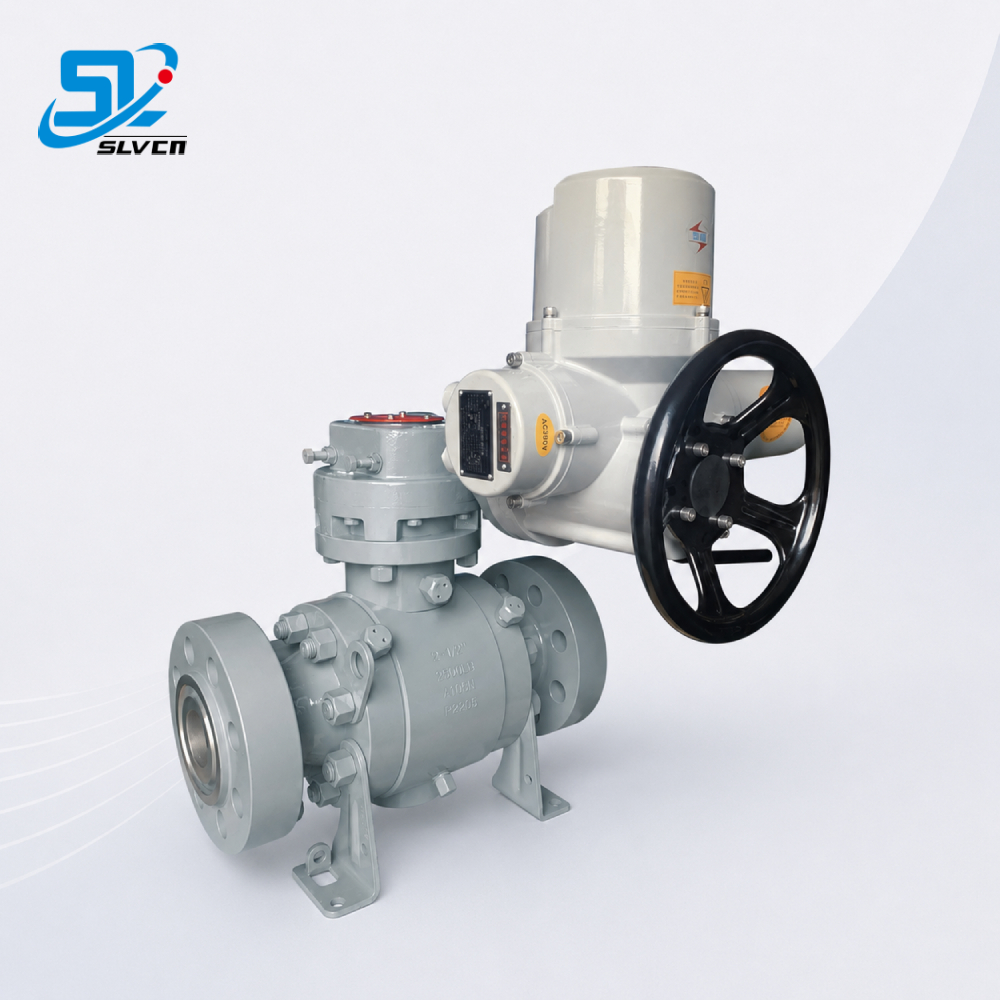
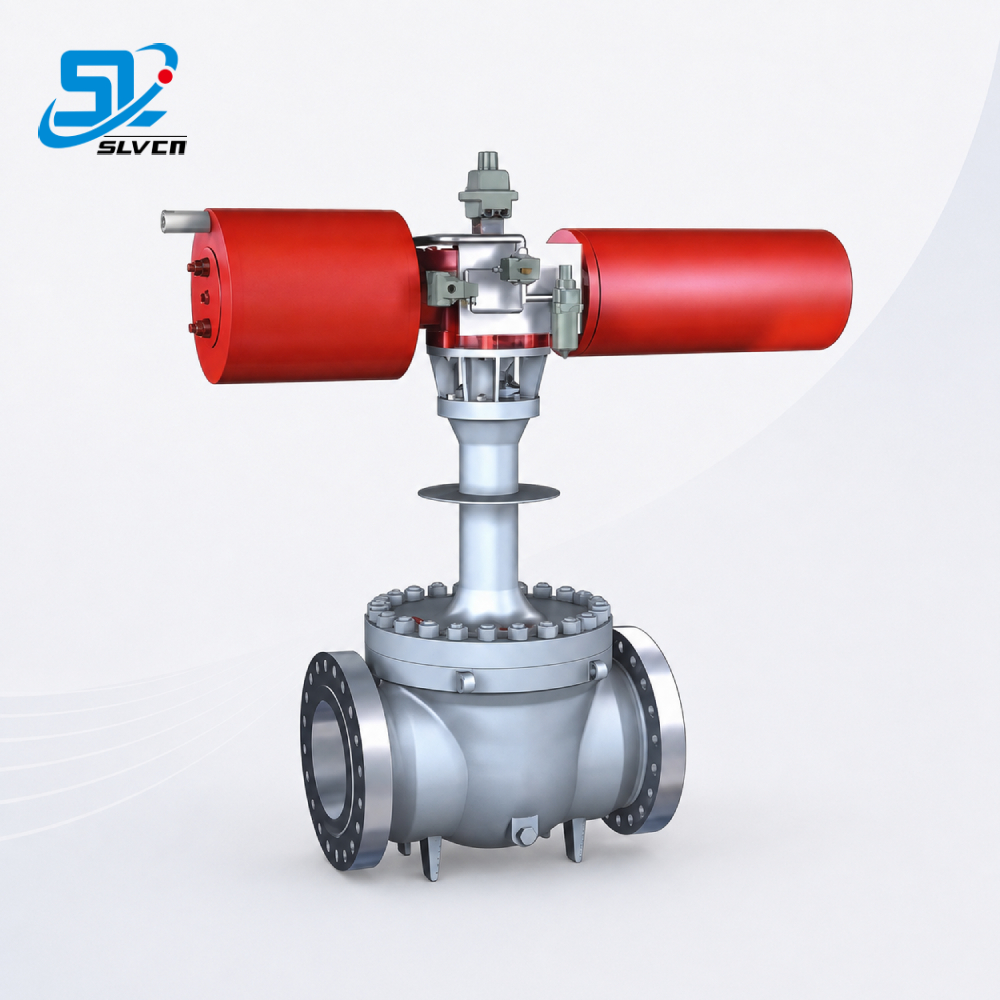
Concentrated Solar Power (CSP) systems using molten nitrate salts (operating between 290°C and 565°C) encounter intense creep and bolt-loosening issues with flanged joints. Butt welded end connections eliminate mechanical flanged leak paths, ensuring zero fugitive emissions and safeguarding against crystallization at joint seals.
Solar thermal receivers and Thermal Energy Storage (TES) loops experience rapid temperature transitions from day-night cycles and cloud transient events. High-integrity forged butt welded valves withstand high ΔT thermal gradients, preventing thermal cracking and mechanical deformation.
Next-generation CSP plants are advancing toward Supercritical CO2 (sCO2) cycles and ultra-supercritical steam cycles exceeding 600°C. Butt welded forged ball valves deliver streamlined flow passages, low pressure drop, and exceptional burst-pressure tolerance under high static and dynamic pressures.
In modern CSP parabolic trough, solar tower, and linear Fresnel architectures, valve selection determines overall plant availability. Valves installed on the molten salt cold and hot storage loops must satisfy demanding operational criteria:
Design Specifications: ASME B16.34, API 6D, ASME B16.25 (Butt Weld Ends), ISO 5208.
Pressure Class Spectrum: ASME Class 150 to Class 2500 (PN20 to PN420).
Specialty Metallurgy: ASTM A182 F316/F316H, Alloy 800H, Inconel 625, F11, F22, and duplex formulations tailored for molten salt corrosion resistance.
Quality Assurance: Full NDT including RT/UT on weld preps, helium leak testing, high-temperature cycle endurance tests, and PMI traceability.
Over 30 years of manufacturing experience


With over 30 years of manufacturing experience, SLVCN is a professional designer and manufacturer of high-performance forged steel ball valves for critical industrial applications. We specialize in extreme working conditions including high pressure, high temperature, and cryogenic environments, providing safe and reliable flow control solutions for global industrial projects where operational reliability is non-negotiable.
Our core product range covers forged trunnion-mounted and floating ball valves, top-entry and side-entry ball valves, fully welded ball valves, metal seated ball valves, cryogenic ball valves, high-pressure ball valves up to Class 2500 (PN420) and customized higher pressure ratings, as well as high-temperature service valves. Compared with conventional cast valves, SLVCN forged valves feature higher material density, superior mechanical strength, improved resistance to pressure fluctuations and thermal shock, and significantly longer service life under severe service conditions.
Designed for High Pressure, High Temperature, and Cryogenic Applications, SLVCN valves are widely used in long-distance oil & gas transmission pipelines, LNG storage and regasification terminals, offshore platforms and deepwater projects, power plants, refineries, compressor stations, and high-pressure chemical processing units. Whether handling flammable media, corrosive fluids, sour service media (H₂S), ultra-low temperatures, or extreme differential pressures, our valves ensure stable operation, bubble-tight shut-off, and maximum system safety in accordance with international sealing and performance standards.
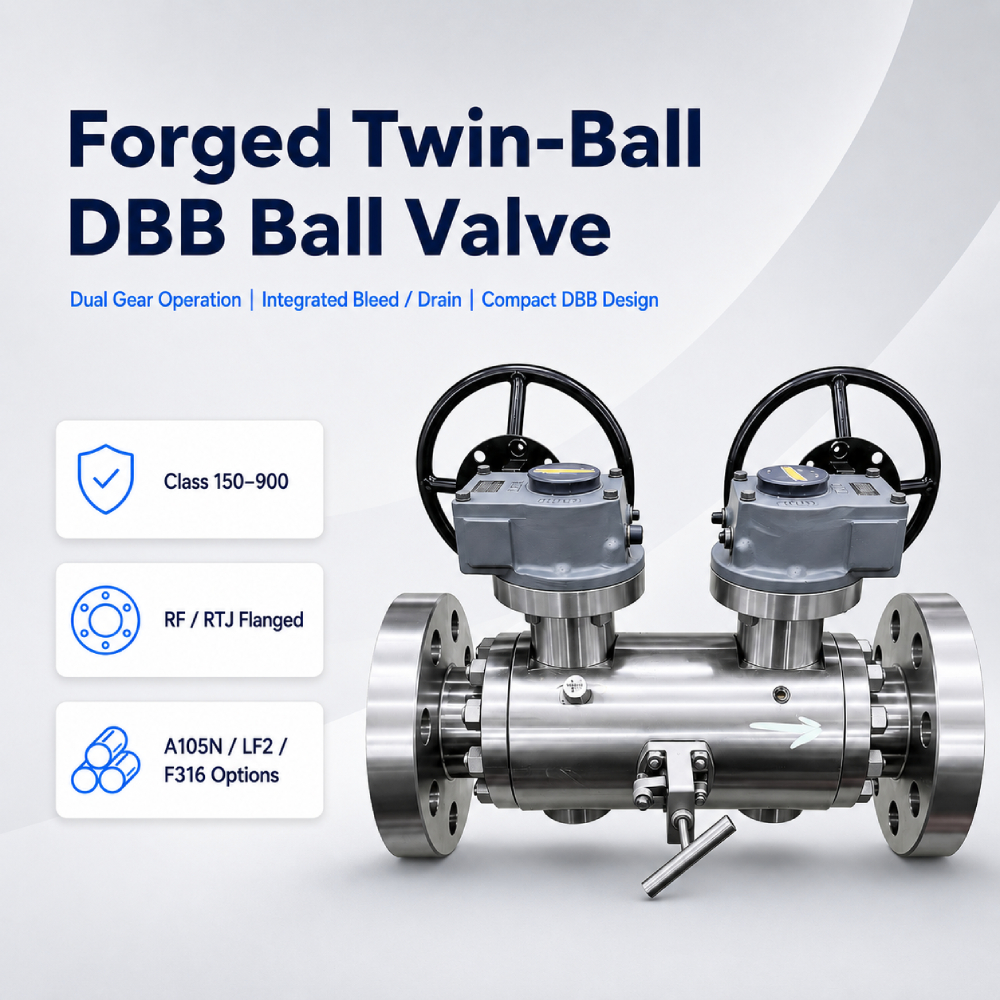
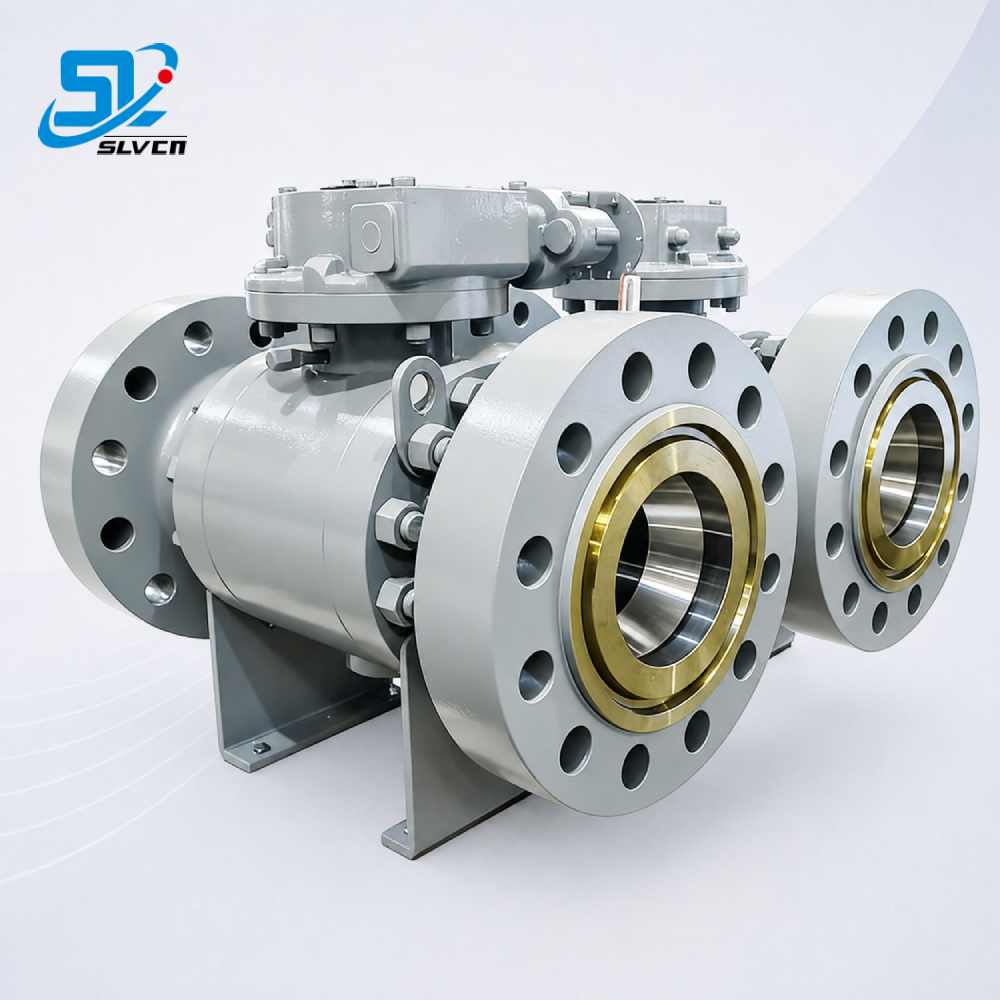
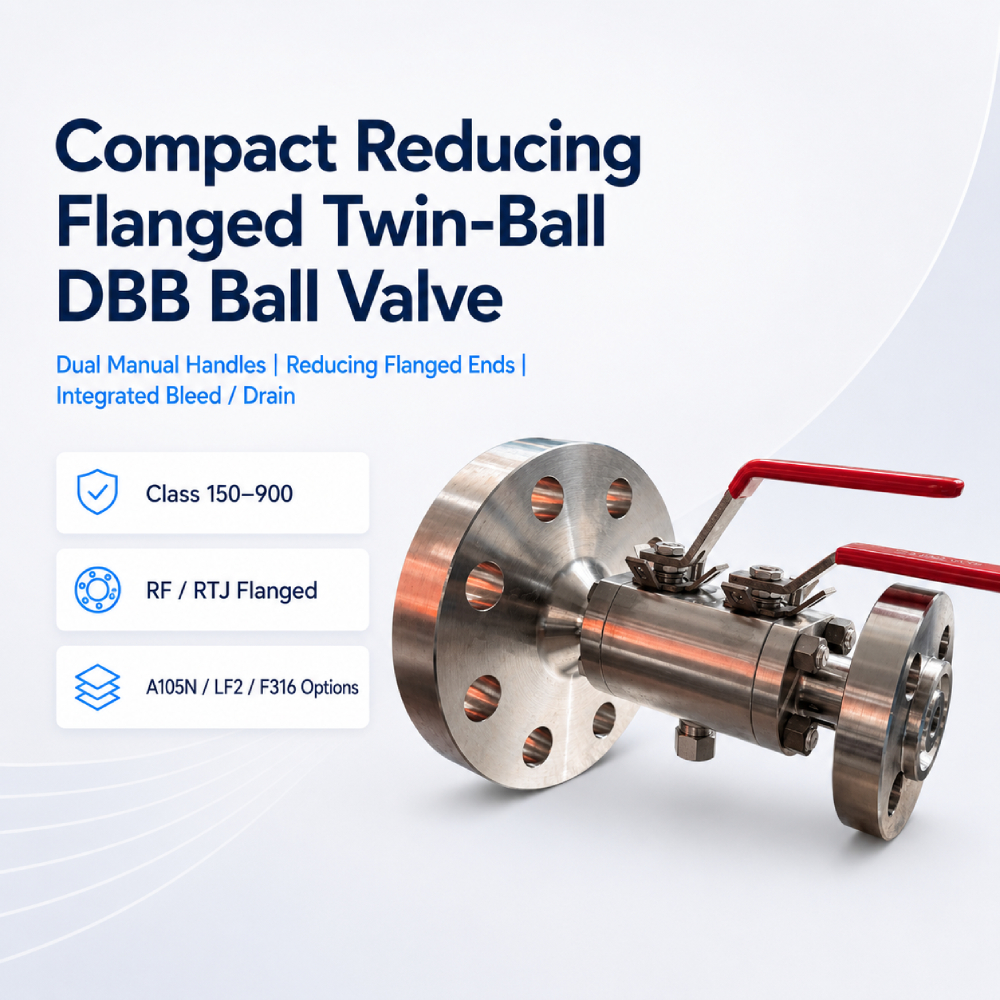
Safety and reliability are embedded in every design. Our forged ball valves are equipped with Double Block and Bleed (DBB) structures, anti-blowout stems, fire-safe designs in accordance with API 607 / API 6FA, anti-static devices, emergency sealing systems, and pressure-balanced seating structures suitable for high differential pressure operation. Valves can be designed with SPE or DPE seat configurations based on application requirements. For sour service environments, materials and sealing systems comply with NACE MR0175 / ISO 15156 requirements.


To ensure consistent quality, each valve undergoes a complete series of inspections and performance tests in accordance with API 6D, API 598, and ISO 5208, including shell test, seat leakage test (Rate A / zero visible leakage), fire-safe test, cryogenic test, operational torque test, dimensional inspection, and PMI material verification. SLVCN operates dedicated cryogenic testing facilities to validate valve performance at ultra-low temperatures down to −196°C.
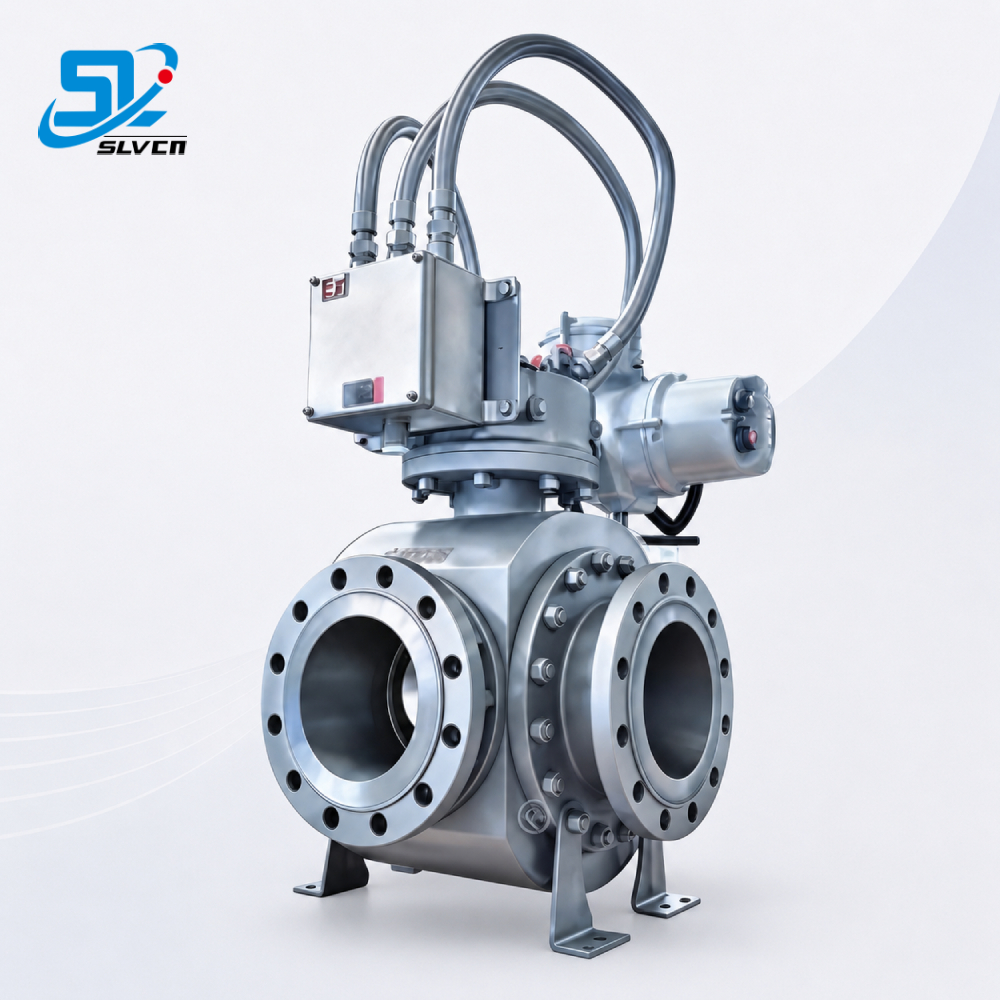
SLVCN is certified to ISO 9001, CE, and API standards, and our products comply with API 6D, ASME B16.34, DIN, ANSI, and JIS specifications. We provide extensive customization capabilities covering sizes from 1/2” to 36”, full bore or reduced bore, special materials including A105, LF2, F11, F22, F51, Inconel, various soft and metal seat designs, and intelligent actuation with pneumatic, electric, and gear operators.

Today, SLVCN serves customers in more than 100 countries and regions, supplying valves to EPC contractors, engineering companies, and end users across Europe, the Middle East, Southeast Asia, and the Americas. Backed by strong engineering expertise, advanced manufacturing, and rigorous quality control, SLVCN is committed to delivering safe, durable, and truly engineered valve solutions for the world’s most demanding industrial projects.
High pressure forged valves, double block and bleed designs, and custom actuated valves built for severe service conditions.


 18061659285

