When it comes to industrial valves, having a high-quality High Temp Ball Valve really can’t be overstated. Experts like Dr. Emily Carter, who’s pretty much a go-to in valve tech, always say, “Reliable high-temperature solutions are key to keeping things running smoothly.” As industries push for more durability and better performance, it’s super important to know which manufacturers truly excel at making these essential parts.
Picking the right OEM for a High Temp Ball Valve isn’t always straightforward. The market’s kinda tricky—lots of companies focus on cutting corners to save a buck, which can mean questionable quality. If you ignore that, you risk equipment failures or even safety issues. Brands like Swagelok and Val-Matic are generally reliable, but even they’ve had recalls before. That’s why doing your homework and thoroughly vetting suppliers is a must for procurement folks.
When lives and investments are on the line, just throwing caution to the wind isn’t an option. You gotta find that sweet spot between good performance and fair price. Manufacturers should give you dependable quality without cutting corners. Making a smart choice now can save you tons of headaches later and keep things running at peak performance.
Understanding High Temp Ball Valves and Their Importance in Industry
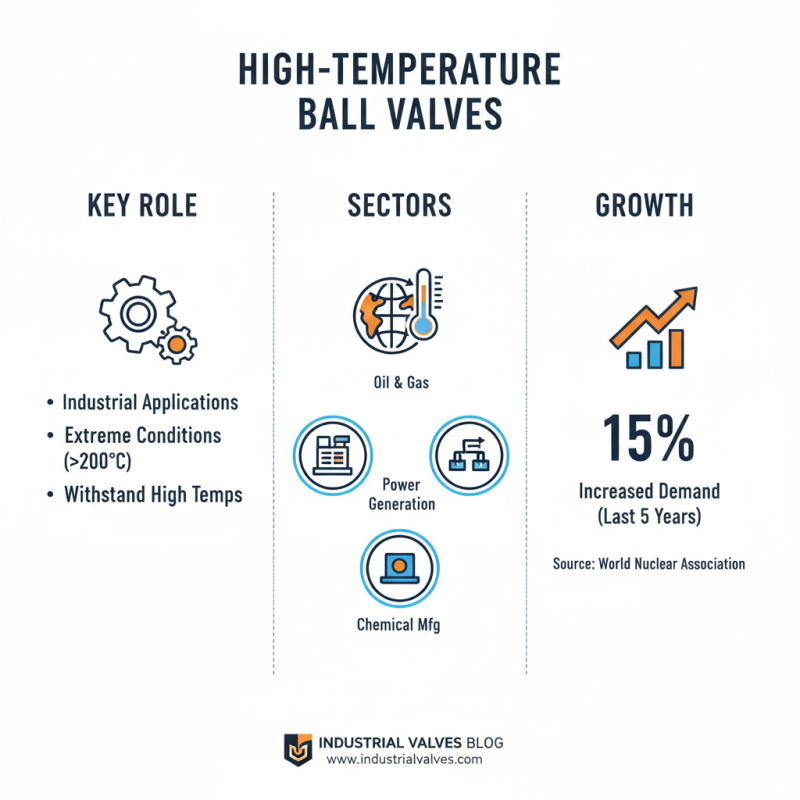
High temperature ball valves play a crucial role in various industrial applications. These valves are designed to operate under extreme conditions, often exceeding 200°C. Their ability to withstand high temperatures is essential for processes in sectors like oil and gas, power generation, and chemical manufacturing. According to the World Nuclear Association, the demand for reliable ball valves in high-temperature environments has increased by 15% over the past five years.
The materials used in manufacturing High Temp Valves are specifically selected for their strength and resistance. Stainless steel and high-performance polymers are common choices. These materials ensure longevity and prevent leaks, which can be costly. In fact, a report by the American Society of Mechanical Engineers states that leaks in industrial systems can lead to losses of up to 5% of production capacity.
However, selecting the right high temp valve is not always straightforward. Manufacturers must consider factors like pressure ratings and compatibility with various fluids. Miscalculations can lead to equipment failure. Regular maintenance and inspection are necessary but often overlooked. Many industries face challenges in keeping up with these needs, leading to potential operational risks.
Criteria for Selecting High Quality OEM High Temp Ball Valve Manufacturers
When selecting high-quality OEM high temp ball valve manufacturers, several criteria are crucial. Look for manufacturers with certifications. ISO 9001 or similar certifications ensure adherence to international quality standards. According to recent industry reports, valves that meet these standards typically last longer and perform better under high-temperature conditions.
Consider the production capacity and experience of the manufacturer. A company with over ten years in the industry often understands the nuances of materials and design for high temp applications. Materials such as stainless steel and specialized alloys are critical for durability. The right choice can prevent costly failures in your system.
Additionally, review customer feedback and performance metrics. High-quality OEMs will have positive testimonials and low failure rates. For instance, reports indicate that valves with a Ball Valve Floating Ball design offer enhanced sealing capabilities and better flow control. This means fewer leaks and improved efficiency in operations. Consider these aspects to make an informed choice.
Overview of Key Players in the High Temp Ball Valve Manufacturing Sector
In the high temperature ball valve manufacturing sector, several key players stand out. They specialize in producing valves that can withstand extreme conditions and applications. These manufacturers focus on quality materials, advanced technology, and innovative designs. Their products play a vital role in industries like petrochemical, oil and gas, and energy.
One notable aspect is the variability in production standards. Some manufacturers may prioritize cost over quality. This can lead to performance issues in critical applications. Others may struggle with maintaining consistent quality due to rapid production demands. Ensuring reliability while meeting market needs is a constant challenge.
Collaboration and feedback from end-users can enhance product development. Manufacturers benefit from understanding real-world applications. They can refine their products based on user experiences. However, gathering this information can be difficult. Ongoing communication is essential but often overlooked. As the industry evolves, adapting to customer needs remains a key concern.
Top 10 High Quality OEM High Temp Ball Valve Manufacturers You Should Know
| Manufacturer Location |
Production Capacity (Units/Year) |
Material Certifications |
Temperature Rating (°C) |
Typical Applications |
| North America |
150,000 |
ISO 9001, API 6D |
-40 to 200 |
Oil & Gas, Chemical |
| Europe |
100,000 |
ATEX, CE Mark |
-20 to 250 |
Pharmaceutical, Food Processing |
| Asia |
200,000 |
ISO 9001, ASME |
-10 to 300 |
Power Generation, Water Treatment |
| South America |
80,000 |
ISO 45001, API 607 |
-40 to 220 |
Mining, Construction |
| Middle East |
60,000 |
LOTO, NACE |
0 to 260 |
Petrochemical, HVAC |
Top 10 Manufacturers with Exceptional Reputation and Quality Standards
In the realm of high-temperature applications, selecting the right OEM high temp ball valve manufacturer is crucial. Recent industry reports highlight that manufacturers with a solid reputation often lead in quality standards. The global market for high-pressure ball valves is expected to grow significantly, driven by diverse industries such as oil and gas, chemical processing, and power generation. This growth underscores the importance of choosing a manufacturer that prioritizes durability and performance.
When assessing manufacturers, consider those with stringent testing processes. An ideal manufacturer often conducts rigorous quality checks, ensuring their products withstand extreme conditions. Data indicates that valves failing to meet these benchmarks can lead to costly downtime and safety hazards. It's essential to recognize that even reputed manufacturers can experience quality lapses. Customer reviews and independent testing can provide insights into real-world performance.
Tips: Always verify certifications. Look for manufacturers compliant with international standards. Engaging with experienced suppliers can also shed light on less visible aspects of product quality. Seeking ongoing feedback from users can help identify potential weaknesses in valve designs or functionalities. Remember, investing time in research can significantly impact operational efficiency and safety in high-pressure systems.
Top 10 High Quality OEM High Temp Ball Valve Manufacturers
Key Features and Innovations Offered by Leading Manufacturers
High temperature ball valves are crucial in various industries, from oil and gas to chemical processing. Leading manufacturers prioritize durability, reliability, and performance. Significant innovations have emerged to improve functionality. Many manufacturers now employ advanced materials like AISI 316 stainless steel, enhancing resistance to corrosion and high pressure.
Recent industry reports indicate that about 30% of high temp ball valves now feature smart technology. This allows for remote monitoring and automation, reducing the risk of leaks and failures. Sensors integrated into the valves can provide real-time data, enhancing safety protocols.
However, not all manufacturers excel in these areas. Some still rely on outdated designs, compromising performance. This inconsistency necessitates careful selection when investing in high-quality OEM options. The industry must reflect on these shortcomings to elevate standards and ensure safety in high-temperature environments.
Case Studies: Successful Applications of High Temp Ball Valves
High Temperature Ball Valve
serve a crucial role in various industries, particularly in oil and gas applications. Case studies highlight their effectiveness in demanding environments, showcasing their ability to withstand extreme pressure and temperature. A notable example includes their application in steam processes. These valves can handle temperatures up to 600°F, ensuring safe and reliable operation.
In one case, an energy company successfully implemented high temperature ball valves in their steam pipeline systems. This not only improved efficiency but also minimized maintenance costs. Data from industry reports indicate that facilities employing these valves reported a 30% decrease in downtime. This improvement directly correlates with the enhanced durability of high temperature ball valves over traditional options.
Tips:
Ensure regular inspections of high temperature ball valves. This proactive approach helps identify potential wear and tear before they lead to failures. Some facilities may overlook this aspect, leading to unexpected shutdowns. Additionally, proper installation is critical. Always adhere to the manufacturer’s guidelines to optimize performance and longevity. Remember, investing in high temperature ball valves is investing in operational integrity.
Future Trends in High Temp Ball Valve Manufacturing and Technology
The manufacturing and technology of high temperature ball valves are evolving.
New materials are being explored to enhance durability and performance. Innovations focus on improving heat resistance while maintaining flexibility in design. Lightweight metals and advanced polymers are becoming more common. These materials can withstand extreme conditions.
Industry experts foresee automation impacting future production. Robotics will play a significant role in assembly lines. This could increase efficiency but also raises concerns about job losses. Balancing technology and human skill may be challenging. Moreover, companies must invest in training to adapt.
Sustainability is another critical trend. Manufacturers are exploring eco-friendly processes. Reducing waste and energy consumption is crucial for the environment. However, adopting new practices often comes with high initial costs. The long-term benefits may not be immediately visible. Thus, companies must carefully evaluate their strategies moving forward.
The Ultimate Guide to Fully Welded Flanged Trunnion Mounted Ball Valves: Advantages and Applications
The Ultimate Guide to Fully Welded Flanged Trunnion Mounted Ball Valves: Advantages and Applications
Fully welded flanged trunnion mounted ball valves have become essential components in modern pipeline systems, particularly within the oil and gas sector. One of the standout features of these valves is their fully welded one-piece body design, which eliminates the risks associated with bolted joint leakage. According to industry reports, improper sealing at bolted joints can account for up to 30% of pipeline failures, highlighting the necessity of adopting such innovative designs for enhanced reliability.
In addition to their robust construction, these valves feature heavy-duty flanged ends, ensuring secure integration into large-diameter energy and infrastructure pipelines. The trunnion mounted ball design provides stable sealing under high-pressure conditions, a critical requirement given that industry standards often mandate operations exceeding 1500 psi in high-stakes environments. Furthermore, these valves are engineered to provide zero external leakage, which is particularly vital in isolation applications where environmental safety and operational efficiency are paramount.
Manufactured under strict quality control standards, fully welded flanged trunnion mounted ball valves exemplify reliability in global projects. According to data from the International Energy Agency, the global demand for high-integrity pipeline components is projected to grow by over 5% annually, reflecting the increasing importance of durable and leak-free technologies. As industries evolve, these advanced valves stand out as a vital solution to meet the demands of modern infrastructure while minimizing environmental impact.
FAQS
: They are used in industries like petrochemical, oil and gas, and energy. They handle extreme conditions.
Many conduct rigorous testing processes. Certifications and independent reviews can help gauge reliability.
Yes, they can lead to costly downtime. Poor quality may cause safety hazards in critical applications.
User feedback helps refine products. However, gathering this feedback can be challenging and often overlooked.
Regular inspections can prevent failures. Facilities that neglect this may face unexpected shutdowns and increased costs.
They should prioritize durable materials and performance. Look for those with a solid reputation and customer feedback.
Yes, even the best can have lapses. Continuous user feedback is important to identify these weaknesses.
Adhering to guidelines ensures optimal performance. Mistakes can lead to premature wear or valve failure.
Balancing cost and quality is tough. Rapid demands can lead to inconsistent product quality, affecting reliability.
Investing time in research can enhance efficiency and safety. It’s vital for maintaining high-pressure systems.
Conclusion
High Temp Ball Valves play a crucial role in various industrial applications, particularly in processes that require the management of high temperatures and pressures. Understanding the significance of these valves is essential when selecting a high-quality OEM manufacturer. Key criteria include the durability, performance, and reliability of the valves, which are vital for operational efficiency and safety.
In the competitive landscape of high temp ball valve manufacturing, several key players stand out for their exceptional quality standards and innovative features. From advanced materials to cutting-edge designs, these manufacturers consistently deliver solutions that meet the demands of modern industries. Case studies highlight successful applications in sectors such as oil and gas, chemical processing, and power generation, showcasing the effectiveness of high temp ball valves. Looking forward, emerging trends indicate continuous advancements in technology and materials, suggesting a promising future for high temp ball valve manufacturing.





 +86 18905154687