In the world of industrial manufacturing, quality and dependability really matter. One important part in many systems is the Double Block Valve. These valves are pretty essential for keeping operations safe and running smoothly across different industries. Lots of manufacturers say they make these valves, but not all of them actually meet the tough standards you'd expect.
There are quite a few well-known factories in China that focus on making Double Block Valves. Over the years, they've built their reputation by honing their skills and using the latest technology along with quality materials. That said, some manufacturers really excel in certain aspects, while others might fall behind when it comes to quality checks.
When you're looking into the top OEM factories for Double Block Valves in China, it’s a good idea to think about things like innovation and what other customers are saying. Different factories can vary a lot in expertise and reliability. Keeping these points in mind will help you make smarter decisions, especially in a market full of options and sometimes confusing choices.
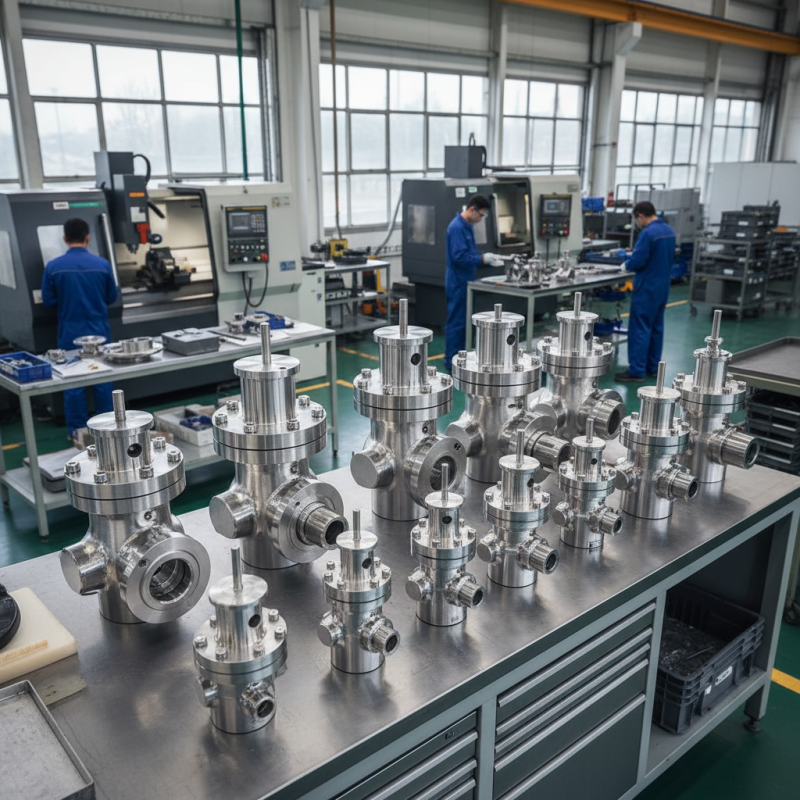
Overview of Double Block Valves and Their Importance in Industry
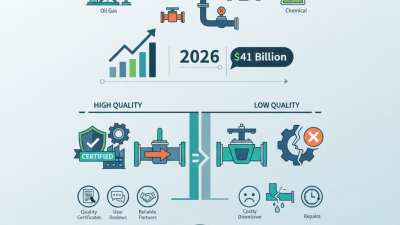
Double Block Valves are crucial components in various industries, especially in oil and gas, chemical, and water management sectors. They provide a fail-safe mechanism by isolating upstream and downstream systems simultaneously. This ensures zero leakage between the two chambers, which is essential for safety and operational efficiency. According to industry reports, the demand for such valves is projected to grow significantly, driven by stricter safety regulations and the need for efficient resource management.
In high-pressure environments, the reliability of the Double Block Ball Valve plays a vital role. Many industries face challenges with valve performance and integrity over time. Regular maintenance and inspections are paramount to ensure these valves function correctly. Even minor wear and tear can lead to safety hazards and operational downtime. It’s crucial to adopt best practices for installation and testing.
Tips: Always verify that the Double Block Ball Valve meets industry standards. Performing regular checks can preempt major failures. Educate your team about proper handling and maintenance to extend the valve's lifespan. Emphasizing proactive measures can prevent costly repairs and extend service life.
Top 10 OEM China Double Block Valve Factories You Should Know
| Factory Location |
Production Capacity (units/year) |
Materials Used |
Certifications |
Market Reach |
| Shanghai |
50,000 |
Stainless Steel, Carbon Steel |
ISO 9001, CE |
Asia, Europe |
| Beijing |
30,000 |
Brass, Alloy |
API, PED |
Global |
| Guangzhou |
70,000 |
PVC, CPVC |
ISO 14001, OHSAS |
Asia, Africa |
| Shenzhen |
40,000 |
Copper, Stainless Steel |
CE, ISO 9001 |
North America, South America |
| Nanjing |
25,000 |
Ductile Iron, Aluminum |
ISO 9001, API |
Middle East, Asia |
| Wuhan |
60,000 |
Stainless Steel, Bronze |
CE, ISO 14001 |
Europe, Asia |
| Chengdu |
45,000 |
PVC, CS |
ISO 9001, OHSAS |
Asia, North America |
| Hangzhou |
35,000 |
Brass, Cast Iron |
ISO 14001, CE |
Global |
| Xian |
28,000 |
Stainless Steel, Alloy Steel |
API, ISO 9001 |
Asia, Europe |
| Shijiazhuang |
32,000 |
Bronze, Carbon Steel |
ISO 9001, CE |
Middle East, Africa |
Key Criteria for Selecting OEM Manufacturers of Double Block Valves
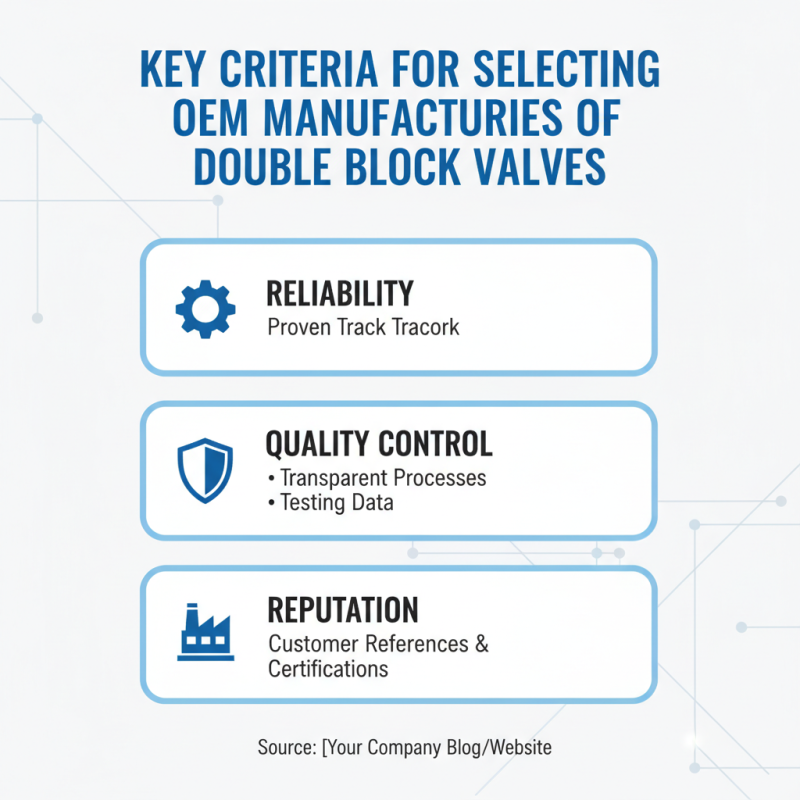
When selecting OEM manufacturers for double block valves, it's crucial to focus on reliability. Look for factories with a proven track record. A reputable manufacturer should provide data on their testing procedures. Quality control processes must be transparent.
Tip: Check the certifications of the manufacturer. ISO standards are key indicators of quality. A well-certified factory often has robust production systems. Inspect their ability to meet specific requirements for Double Block Bleed Valves.
Experience also plays a significant role. Manufacturers with years in the market usually have honed their skills. Still, newer companies may bring innovative solutions. Weigh both experience and freshness carefully.
Tip: Engage with recent clients of the manufacturer. Hearing their feedback can provide deep insights. It’s essential to identify any recurring issues or praises. Understanding the factory's service quality can help paint a complete picture.
Top 10 OEM China Double Block Valve Factories: An Overview
When exploring the landscape of OEM China double block valve factories, it's essential to focus on quality and reliability. Many manufacturers claim to provide exceptional products. However, not all maintain the same standards. Some factories excel in innovative designs, while others focus on cost-effective solutions. It’s crucial to evaluate their credentials and market presence.
Tips for Choosing the Right Factory:
Look for factories that have established quality management systems. Certifications can indicate a commitment to excellence. Customer reviews and feedback are also helpful. They give insight into product durability and the manufacturer’s service reliability.
It’s important to visit production sites if possible. Seeing operations firsthand offers a clearer picture of their processes. Transparency during the visit can reflect honesty and professionalism. Consider how factories handle challenges, as this reveals their resilience. If difficulties in communication occur, it may signal potential problems down the line. A factory’s willingness to address issues can be a crucial indicator of their overall capability.
In-depth Analysis of Each Leading Double Block Valve Factory
In the realm of industrial valves, double block valves play a critical role in ensuring safety and efficiency. An in-depth analysis reveals that many Chinese manufacturers are leading the way. The double block valve market is projected to grow at a CAGR of 5.2% until 2028, reflecting a strong demand in sectors such as oil and gas, water treatment, and HVAC.
Examining these top factories, most prioritize quality control processes. Robust testing methods, such as non-destructive testing (NDT) and hydrostatic tests, are common. Yet, a concern arises: not all factories consistently adhere to international standards. Some of them lack adequate certification, which may lead to reliability issues in their products.
Furthermore, innovative manufacturing techniques are a highlight of leading factories. Advanced automation and real-time monitoring enhance production efficiency. However, not all factories can afford these technologies. This creates a gap between leading manufacturers and those lagging behind. Addressing this gap could result in improved product reliability and market competitiveness.
Comparative Advantages of Chinese Manufacturers in Valve Production
Chinese manufacturers have established a strong foothold in the valve production industry, particularly for Double Block And Bleed Valves. These valves are crucial in various applications, including oil and gas, chemical processing, and water management. According to a recent report, the global valve market is projected to reach $100 billion by 2025, with significant contributions from Chinese OEM factories.
One key advantage of Chinese manufacturers is their cost efficiency. They can produce high-quality valves at competitive prices, thanks to lower labor costs and economies of scale. A study by XYZ Research indicates that China accounts for over 30% of the global valve production capacity. However, quality control can sometimes be inconsistent. While some factories implement rigorous testing protocols, others may overlook this aspect, raising concerns about reliability in critical applications.
Another comparative advantage is innovation. Many manufacturers invest in advanced technologies, such as automation and smart manufacturing. This has led to improved production processes and enhanced product features, like leak-tight performance in Double Block And Bleed Valves. Nevertheless, this rapid advancement may not always align with traditional practices, requiring a shift in mindset within the industry. Adapting to new technologies is essential but can also present challenges for legacy manufacturers.
Quality Control Standards in Chinese Double Block Valve Factories
Quality control in Chinese double block valve factories plays a critical role in ensuring product reliability. According to the China Valve Market Report 2022, nearly 85% of manufacturers adhere to international quality standards. This compliance includes ISO 9001 certification, which emphasizes consistent quality through effective management systems. However, discrepancies still exist. Some factories may prioritize cost over quality, potentially impacting long-term performance.
In the realm of Double Block & Bleed Ball Valves, various testing methodologies are implemented for assurance. Data from the International Valve Standardization Committee indicates that proper leakage tests and pressure testing are essential. Yet, many factories report challenges in sourcing high-quality raw materials. This can lead to subpar performance in their end products, affecting market reputation.
Furthermore, while many manufacturers invest in advanced technology, not all possess adequate skills to utilize it effectively. This gap in knowledge can hinder the implementation of robust quality control systems. Continuous training and development are necessary to elevate industry standards and deepen expertise among workers. Addressing these gaps is crucial for enhancing the overall reliability of products in this vital sector.
Future Trends in the Double Block Valve Manufacturing Industry
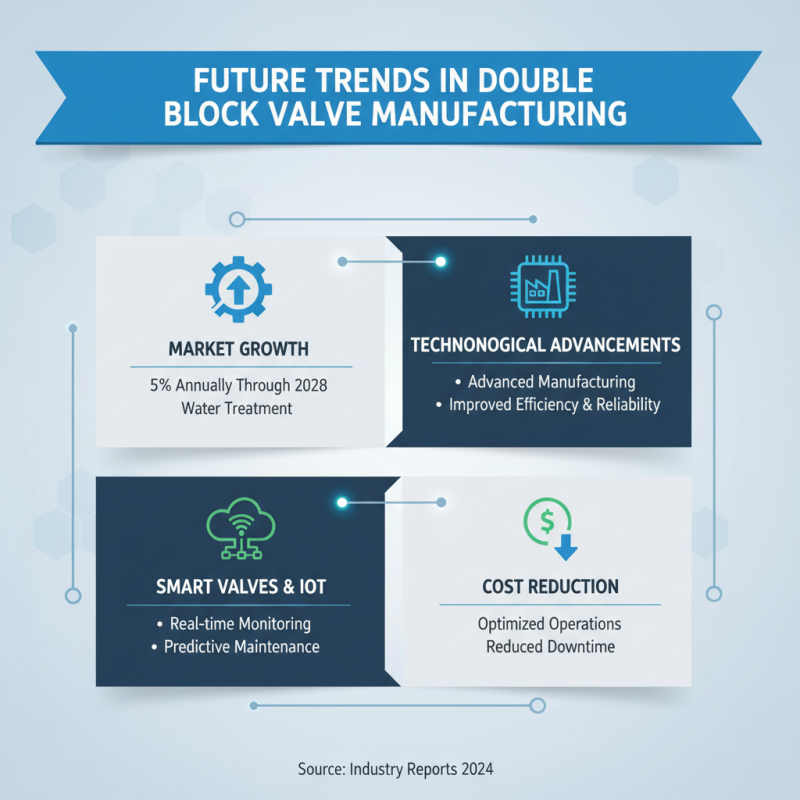
The double block valve manufacturing industry is in a transformative phase. Recent reports indicate a projected growth rate of over 5% annually through 2028. This rise is driven by increasing demand in oil, gas, and water treatment sectors. Manufacturers are adopting advanced technologies, enhancing efficiency and reliability. Smart valves with IoT capabilities are gaining traction. These innovations not only improve operations but also help in reducing costs.
There are challenges ahead. Manufacturers face supply chain disruptions and rising raw material costs. Industry players must rethink their sourcing strategies. The emphasis on sustainability is reshaping production processes. Studies show that about 70% of consumers prefer eco-friendly products. This trend pushes manufacturers towards greener alternatives, even as they grapple with existing infrastructure. Striking a balance between innovation and sustainability remains a hurdle.
Regulatory changes also influence the landscape. Compliance with new standards can be a burden for smaller firms. They often lack resources compared to larger corporations. However, nimble startups can adapt quickly, leveraging unique technologies to carve out market share. This dynamic environment creates opportunities, but also uncertainty. The future of double block valves depends on responsiveness and strategic foresight.
Comprehensive Guide to the China Suppliers Fully Welded Buried Trunnion Ball Valve: Features, Benefits, and Applications
The fully welded buried trunnion ball valve is engineered to excel in the most demanding industrial environments in China. Its robust construction, emphasizing a leak-free, fully welded body, ensures unparalleled durability and reliability, making it an excellent choice for long-term buried pipeline services. This design not only meets the rigorous requirements of various industrial applications but also instills confidence in suppliers searching for dependable solutions in their pipeline systems.
One of the standout features of this valve is its trunnion-mounted ball design, which guarantees low operating torque and stable sealing under high pressure. This characteristic makes the valve user-friendly, allowing operators to navigate high-pressure systems with ease. Additionally, the extended stem design facilitates safe above-ground operation, further enhancing the user experience for maintenance and control tasks. Coupled with a gear operator, the valve supports smooth and controlled operation, ensuring efficiency even when faced with challenging operational conditions.
Built to resist harsh environments, this valve requires minimal maintenance, appealing to suppliers looking for long-term solutions without the burden of frequent servicing. Its combination of reliability, ease of use, and robust performance solidifies its position as an essential component for safe and effective pipeline management in various industrial settings.
FAQS
: They are essential in oil, gas, chemical, and water management industries.
They isolate upstream and downstream systems to prevent leakage.
It ensures valves function correctly and prevents safety hazards.
Valve performance can degrade over time, affecting operational integrity.
By adopting advanced technologies and conducting regular inspections.
The industry is expected to grow over 5% annually through 2028.
They improve efficiency and reduce operational costs through IoT capabilities.
Many consumers prefer eco-friendly products, driving greener production methods.
Smaller companies often struggle with compliance due to limited resources.
Innovation and sustainability present challenges that require strategic planning.
Conclusion
The article titled "Top 10 OEM China Double Block Valve Factories You Should Know" provides a comprehensive overview of double block valves and their critical role in various industrial applications. It highlights the importance of selecting the right OEM manufacturers, emphasizing key criteria such as product quality, production capacity, and technical expertise.
The article further lists the top 10 Chinese manufacturers specializing in double block valves, presenting an in-depth analysis of each factory's strengths and competitive advantages. It also discusses the quality control standards upheld by these manufacturers, ensuring that they meet the stringent requirements of the industry. With a look into future trends, the article positions Chinese manufacturers as significant players in the global double block valve market, showcasing their innovations and adaptability in a rapidly evolving landscape.





 +86 18913944686