Leave Your Message
Zero-leakage, high-integrity ball valves optimized for direct-buried underground distribution lines, thermal chambers, and district energy substations.
Modern District Heating Networks (DHN) represent the central pillar of municipal energy decarbonization and thermal efficiency across Europe, North America, Northern Asia, and expanding global metropolitan centers. As municipal energy frameworks transition from legacy steam-driven systems to advanced 4th and 5th Generation Low-Temperature District Heating and Cooling (4GDH / 5GDHC) systems, subsurface infrastructure requirements have undergone profound changes. Modern networks operate continuously beneath high-density urban roads, conveying pressurized hot water, secondary return loops, and industrial waste heat across expansive underground pipeline grids.
Underground direct-buried installations demand zero maintenance over extended design lifespans exceeding 30 to 50 years. In these subsurface environments, civil excavation costs for repairs can exceed the original component value by factors of ten. Consequently, high-performance forged steel ball valves have replaced legacy gate and globe valves as the universal standard for primary isolation, branch sectionalizing, and district energy substations. Equipped with fully welded bodies, premium polymeric or metal-to-metal sealing systems, and long-stem extension kits, ball valves ensure minimal thermal loss, bubble-tight sealing, and uncompromised structural integrity against ground settling and high cyclic thermal loads.

District heating lines experience severe axial expansion and contraction due to dynamic seasonal temperature variations (20°C to 180°C). Forged ball valves withstand multi-ton pipeline axial forces without seat distortion or body deformation.
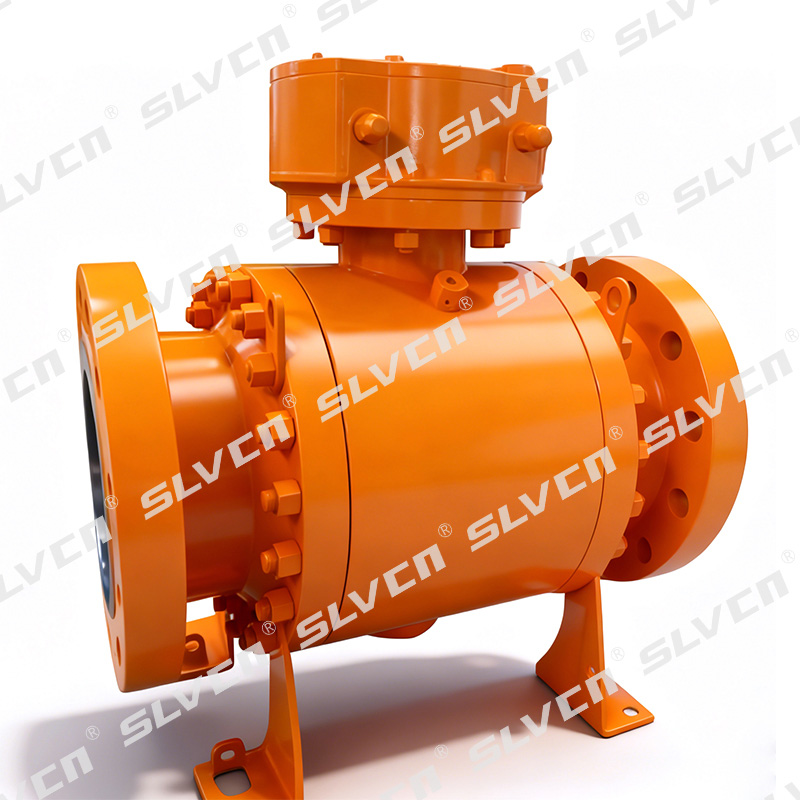
Directly buried ball valves eliminate costly concrete valve chambers. Featuring all-welded forged construction, specialized external anti-corrosion PUR/PE coatings, and extended stainless steel stems for effortless surface manipulation.
Engineered with bidirectional SPE/DPE seating configurations, carbon-filled PTFE, or hardened metal-to-metal seating (Stellite / Tungsten Carbide), securing zero visible leakage (API 598 / ISO 5208 Rate A) even with particulate-laden water.
Ball valves play a decisive operational role across multiple critical nodes in district heating and cooling infrastructure:
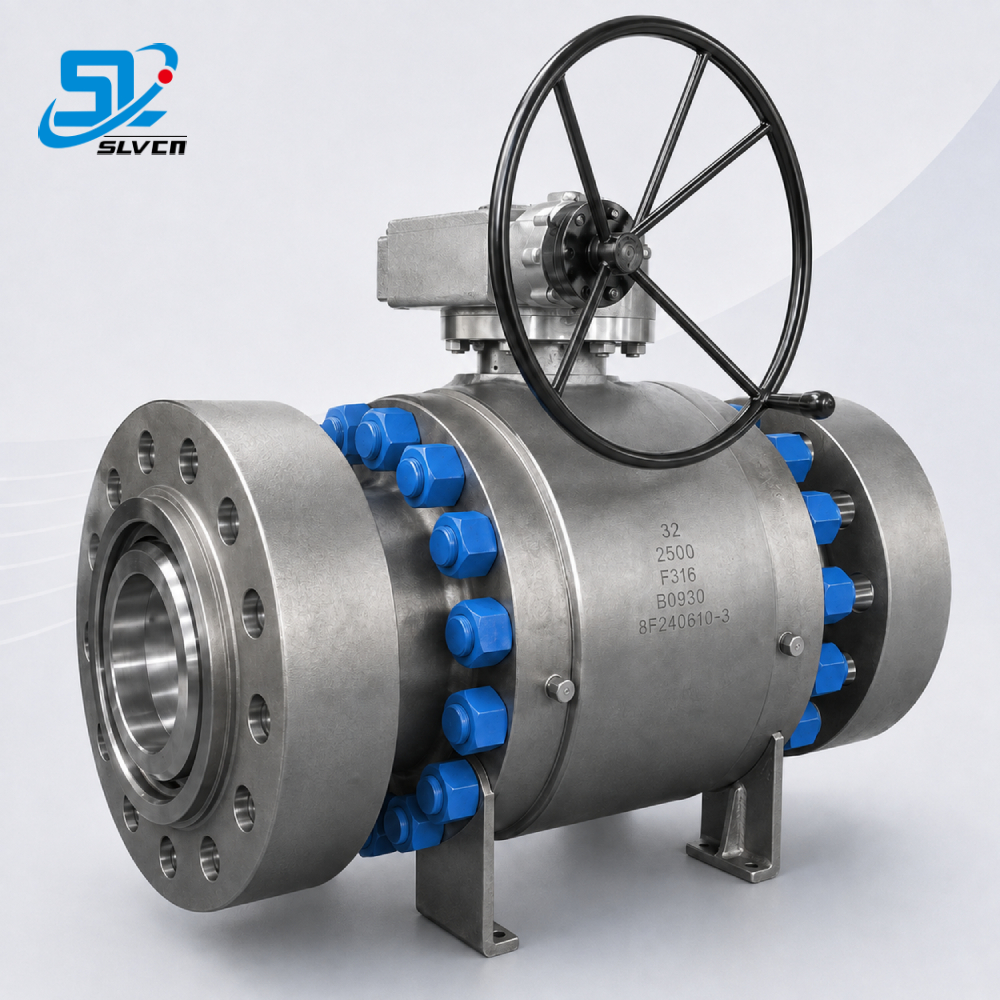
1. Primary Transmission Mainlines: Large-diameter (DN200 to DN900 / 8" to 36") fully welded trunnion mounted ball valves isolate major district arteries. They accommodate high differential operating pressures (PN16 to PN40 / ASME Class 150-600) and provide rapid emergency shut-off capabilities during network upsets.
2. Deep Geothermal & CHP Interconnections: Combined Heat and Power (CHP) plants, biomass boilers, and geothermal extraction facilities introduce aggressive media with dissolved minerals and high continuous temperatures. Forged stainless steel (F316, F51) and metal-seated ball valves eliminate erosion and cavitation damage.
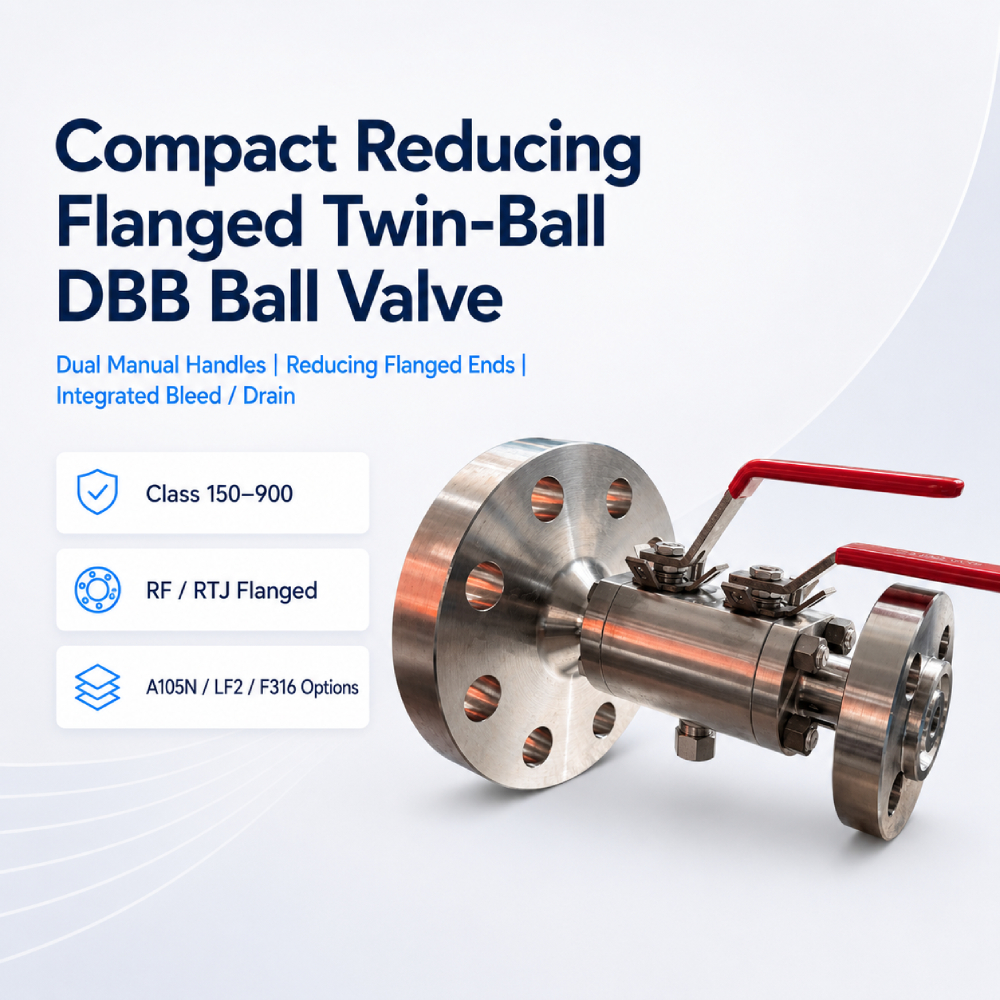
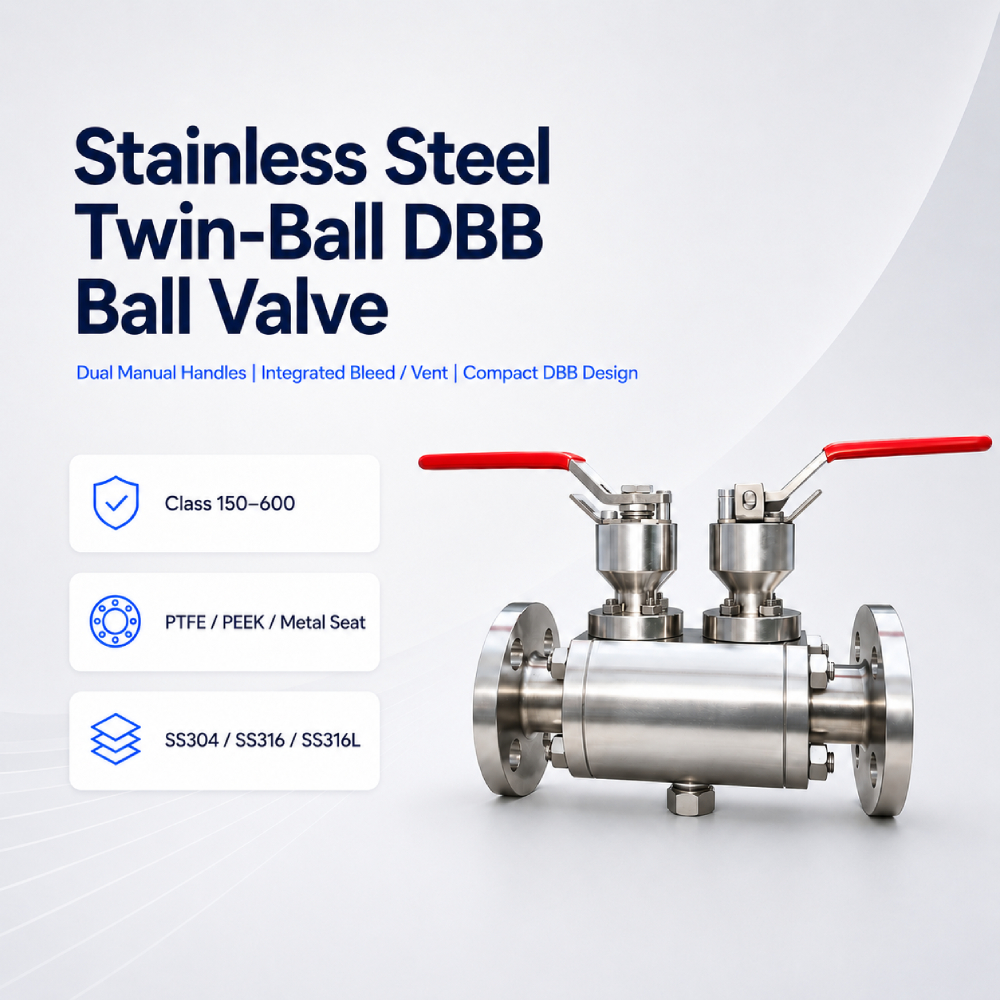
3. Sectionalizing & Branch Isolation: Underground branch lines incorporate compact twin-ball double block and bleed (DBB) valves. This allows localized pipeline draining, venting, and pressure testing without interrupting service across the broader municipal network.
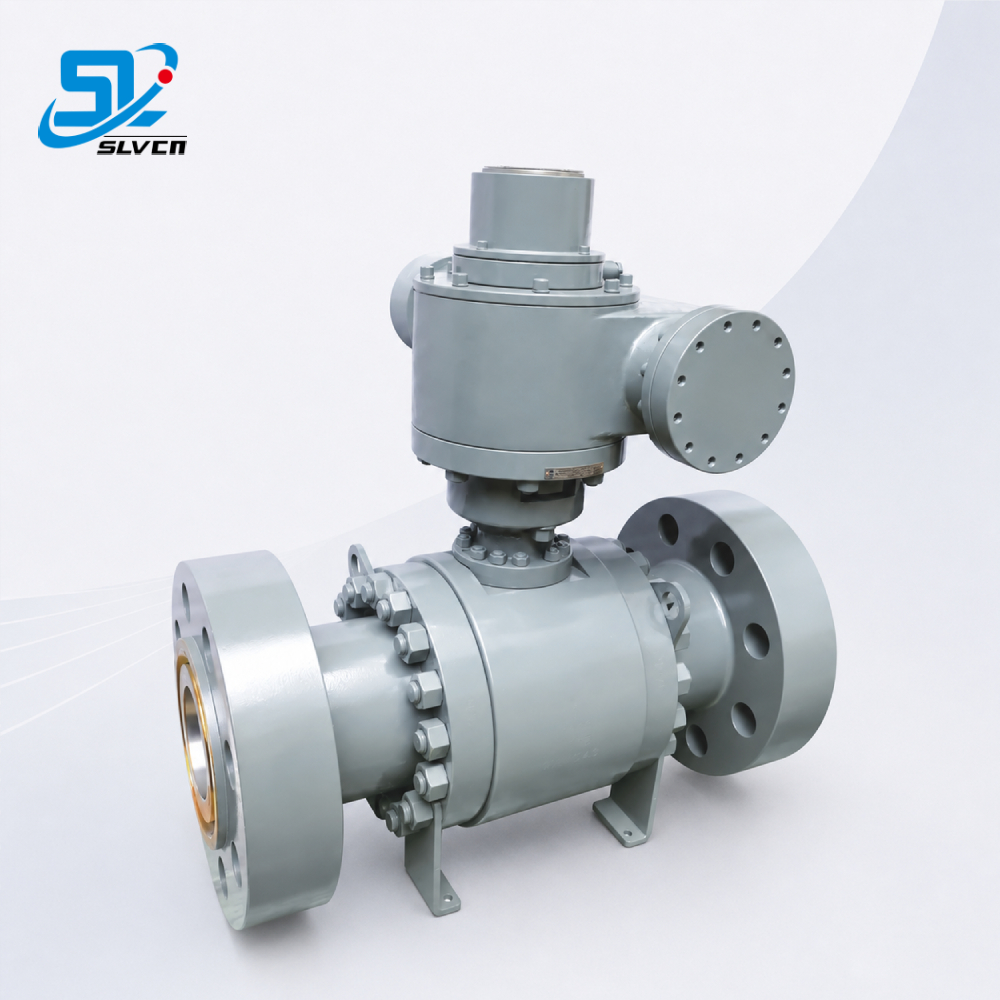
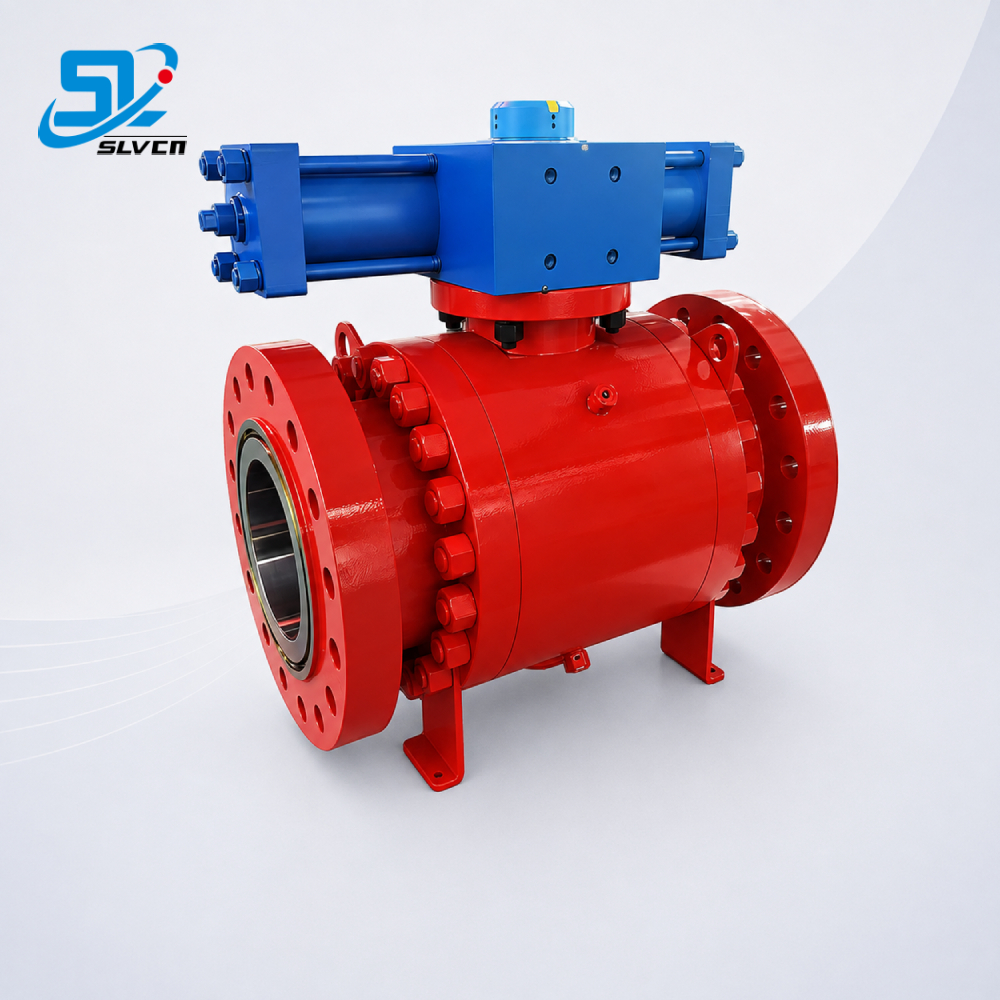
4. Building Entry Substations (Heat Exchanger Skids): Floating and trunnion-mounted valves equipped with electric or electro-hydraulic actuators enable automated balancing, peak-load shaving, and smart metering integration with central SCADA platforms.

Intelligent monitoring, smart diagnostics, and materials science tailored for next-generation multi-energy subsurface grids.
Modern buried ball valves integrate wireless torque, temperature, and acoustic leakage sensors within extended bonnet assemblies, streaming real-time operational telemetry to municipal SCADA dispatchers before minor seal degradation becomes critical.
Valves are factory-encapsulated with high-density polyurethane (PUR) foam insulation and seamless high-density polyethylene (HDPE) outer casing matching EN 253 / EN 488 standards, minimizing thermal conductivity down to λ ≤ 0.026 W/(m·K).
Next-generation district energy valves are engineered to support dual fluid modes: handling seasonal low-temperature waste heat, industrial steam recovery, and high-efficiency geothermal loops with corrosion-resistant metallurgy (F316/F51/Inconel).
With over 30 years of manufacturing experience, SLVCN is a professional designer and manufacturer of high-performance forged steel ball valves for critical industrial applications. We specialize in extreme working conditions including high pressure, high temperature, and cryogenic environments, providing safe and reliable flow control solutions for global industrial projects where operational reliability is non-negotiable.
Contact Engineering Team
Forged valve metallurgy engineered for extreme pressures, dynamic thermal gradients, and underground pipeline stresses.
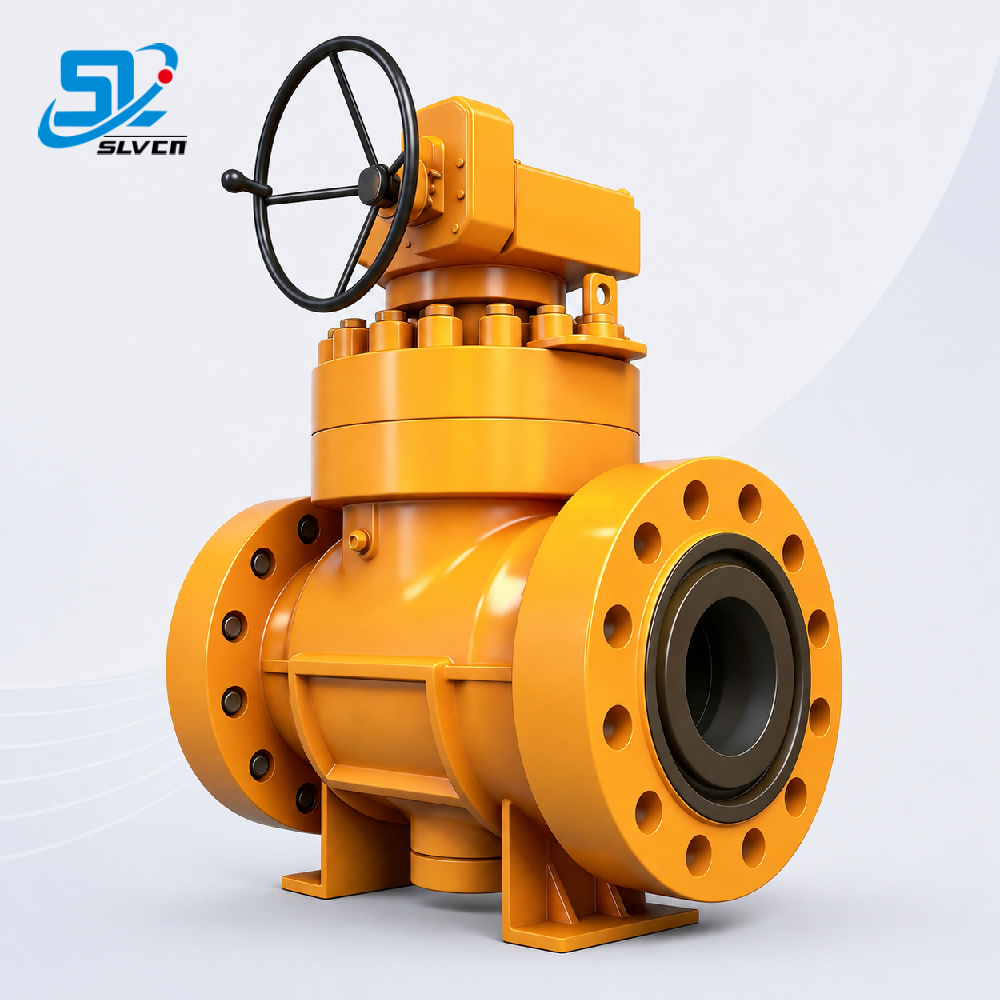
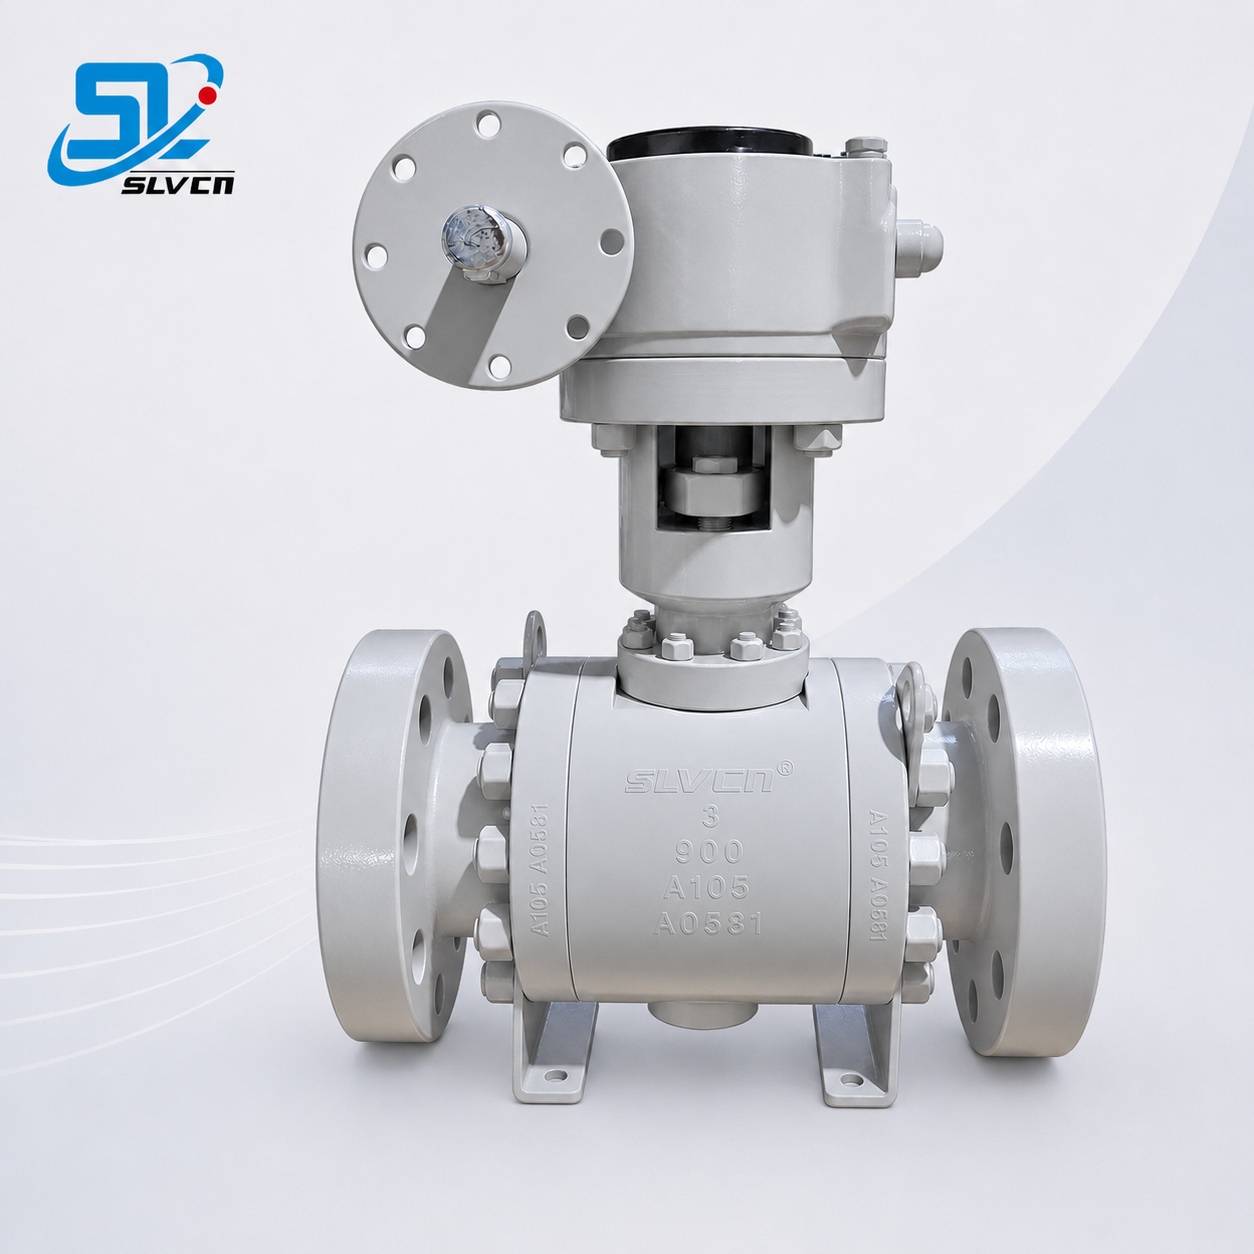
Our core product range covers forged trunnion-mounted and floating ball valves, top-entry and side-entry ball valves, fully welded ball valves, metal seated ball valves, cryogenic ball valves, high-pressure ball valves up to Class 2500 (PN420) and customized higher pressure ratings, as well as high-temperature service valves. Compared with conventional cast valves, SLVCN forged valves feature higher material density, superior mechanical strength, improved resistance to pressure fluctuations and thermal shock, and significantly longer service life under severe service conditions.
Designed for High Pressure, High Temperature, and Cryogenic Applications, SLVCN valves are widely used in long-distance oil & gas transmission pipelines, LNG storage and regasification terminals, offshore platforms and deepwater projects, power plants, refineries, compressor stations, and high-pressure chemical processing units. Whether handling flammable media, corrosive fluids, sour service media (H₂S), ultra-low temperatures, or extreme differential pressures, our valves ensure stable operation, bubble-tight shut-off, and maximum system safety in accordance with international sealing and performance standards.
Safety and reliability are embedded in every design. Our forged ball valves are equipped with Double Block and Bleed (DBB) structures, anti-blowout stems, fire-safe designs in accordance with API 607 / API 6FA, anti-static devices, emergency sealing systems, and pressure-balanced seating structures suitable for high differential pressure operation. Valves can be designed with SPE or DPE seat configurations based on application requirements. For sour service environments, materials and sealing systems comply with NACE MR0175 / ISO 15156 requirements.
To ensure consistent quality, each valve undergoes a complete series of inspections and performance tests in accordance with API 6D, API 598, and ISO 5208, including shell test, seat leakage test (Rate A / zero visible leakage), fire-safe test, cryogenic test, operational torque test, dimensional inspection, and PMI material verification. SLVCN operates dedicated cryogenic testing facilities to validate valve performance at ultra-low temperatures down to −196°C. Certified to ISO 9001, CE, and API standards; sizes from 1/2” to 36”; materials include A105, LF2, F11, F22, F51, and Inconel.
Today, SLVCN serves customers in more than 100 countries and regions, supplying valves to EPC contractors, engineering companies, and end users across Europe, the Middle East, Southeast Asia, and the Americas. Backed by strong engineering expertise, advanced manufacturing, and rigorous quality control, SLVCN is committed to delivering safe, durable, and truly engineered valve solutions for the world’s most demanding industrial projects.
Whether for subterranean municipal district energy networks, high-pressure steam distribution headers, or subsea and cryogenic pipelines, SLVCN provides custom engineering, full material traceability (EN 10204 3.1 / 3.2), and direct project lifecycle support from conception to commissioning.


Explore SLVCN's full spectrum of forged, DBB, metal-seated, top-entry, and actuated ball valves for severe thermal and industrial pipelines.



 18061659285