


Leave Your Message
Serving the Capital's Energy, Water, and Process Industries
London, as one of the world's leading financial and commercial capitals, maintains a sophisticated industrial infrastructure that demands reliable flow control solutions. The city's industrial landscape includes critical sectors such as district heating networks, water treatment and distribution facilities, pharmaceutical manufacturing, food and beverage processing, data center cooling systems, and backup power generation facilities. The Greater London area hosts numerous industrial estates including Park Royal, Barking and Dagenham, and Silvertown, where actuated ball valves play essential roles in process automation and safety systems.
The Thames Gateway development and London's ongoing infrastructure modernization projects require advanced valve technology that can deliver precise control, rapid response times, and fail-safe operation. Actuated ball valves are particularly valued in London's urban environment where space constraints, noise regulations, and the need for remote operation make automated valve solutions indispensable.
London's industrial valve market is experiencing significant transformation driven by several key trends. The push toward net-zero carbon emissions by 2050 has accelerated investment in energy-efficient systems, where smart actuated valves with advanced monitoring capabilities play a crucial role. The UK government's commitment to green technology and sustainable infrastructure has created substantial demand for valve automation solutions that optimize energy consumption and reduce operational costs.
The integration of Industrial Internet of Things (IIoT) technology is revolutionizing valve operation in London's facilities. Modern actuated ball valves now feature built-in sensors, wireless communication capabilities, and predictive maintenance algorithms that align with Industry 4.0 initiatives. This digital transformation enables real-time monitoring, remote diagnostics, and data-driven decision-making, particularly valuable in London's high-value industrial operations where downtime can be extremely costly.
Brexit has also influenced the London valve market, with increased focus on supply chain resilience and preference for suppliers who can provide comprehensive local support, rapid delivery, and compliance with both UK and international standards. The emphasis on British manufacturing and European partnerships has created opportunities for reliable valve suppliers who can demonstrate quality, certification, and responsive service.
London's super sewer project, one of Europe's largest infrastructure investments, requires thousands of high-performance actuated valves for flow control, isolation, and emergency shut-off functions. The project's demanding specifications for reliability, longevity, and fail-safe operation in wastewater environments demonstrate the critical importance of quality valve solutions in major London infrastructure projects.
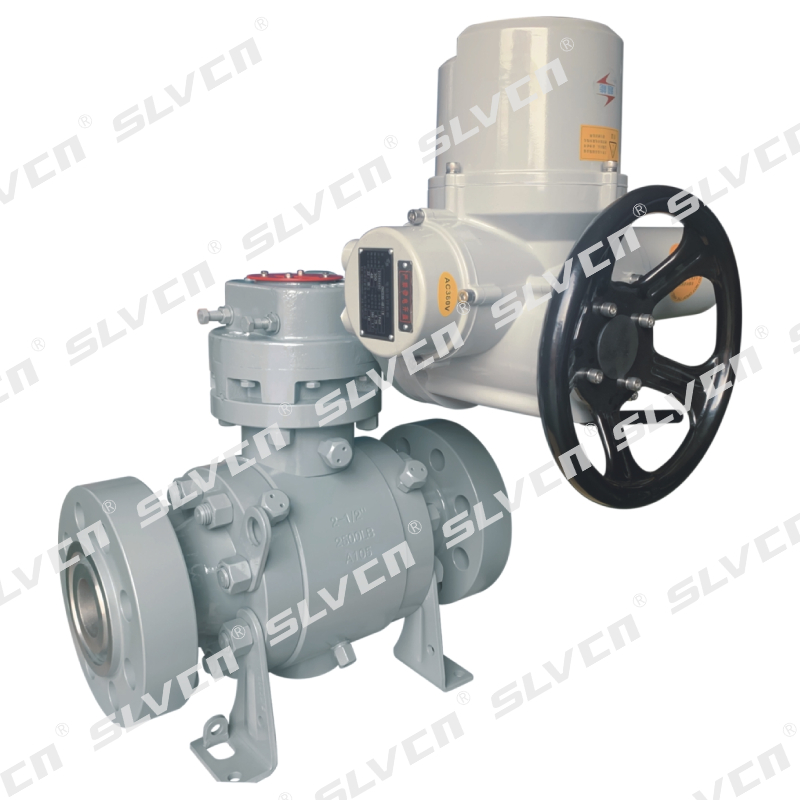
Actuated ball valves in this application must withstand aggressive media, provide bubble-tight shut-off, and operate reliably in confined underground spaces where maintenance access is limited. Electric actuators with position feedback and remote control capabilities are essential for the tunnel's automated control systems.


London's expanding district heating schemes, including the pioneering South East London Combined Heat and Power (SELCHP) system, rely heavily on automated valve technology. These networks distribute heat from central energy centers to thousands of buildings, requiring precise flow control, rapid response to demand fluctuations, and fail-safe isolation capabilities.
Actuated ball valves in district heating applications must handle high-temperature water (up to 120°C), provide excellent throttling characteristics, and integrate seamlessly with building management systems (BMS). The ability to modulate flow based on real-time demand while maintaining tight shut-off when required makes actuated ball valves ideal for these applications.
London's thriving pharmaceutical and biotechnology sector, concentrated in areas like the Imperial College London campus and the Francis Crick Institute, demands the highest standards in process control. Actuated ball valves used in these facilities must meet stringent hygienic standards, provide validation documentation, and offer precise control for critical processes such as fermentation, purification, and sterile filling operations.
Stainless steel actuated ball valves with electropolished surfaces, sanitary connections, and FDA-compliant materials are essential. Pneumatic actuators are often preferred in cleanroom environments due to their intrinsically safe operation and lack of electrical components that could generate particulates.
London's unique operational environment presents specific challenges that make actuated ball valves particularly suitable. The city's variable climate, with temperature fluctuations and high humidity, requires valve materials and actuators that can perform reliably across a wide temperature range. Compact actuated ball valves are ideal for London's space-constrained installations, whether in basement plant rooms, rooftop equipment areas, or confined industrial facilities.
The quarter-turn operation of ball valves, combined with electric or pneumatic actuation, provides rapid shut-off capability essential for safety systems and emergency response scenarios. This is particularly critical in London's dense urban environment where industrial incidents must be contained quickly to protect public safety and minimize environmental impact.
All actuated ball valves supplied for London projects must comply with relevant British and European standards, including BS EN ISO 5211 for actuator mounting, BS EN 12266 for testing, and the Pressure Equipment Directive (PED) 2014/68/EU for pressure-containing equipment. ATEX certification is required for installations in potentially explosive atmospheres, common in chemical processing and fuel handling facilities.
Electrical actuators must meet UK electrical safety regulations and EMC directives, while control systems must integrate with standard industrial protocols such as Modbus, Profibus, and Foundation Fieldbus commonly used in London's industrial facilities.
London's ambition to become a leading smart city is driving demand for intelligent valve solutions that can communicate with centralized control systems, provide real-time operational data, and enable predictive maintenance strategies. Modern actuated ball valves equipped with smart positioners, wireless communication modules, and advanced diagnostics are becoming standard in new installations and retrofit projects.
The Greater London Authority's focus on energy efficiency and carbon reduction creates opportunities for valve solutions that optimize system performance. Actuated ball valves with precise modulating control can significantly reduce energy consumption in HVAC systems, process cooling, and district heating applications by maintaining optimal flow conditions and eliminating energy waste from over-pumping or excessive system pressures.
London's stringent environmental regulations and commitment to sustainability influence valve selection criteria. Fugitive emission standards require valve designs with enhanced stem sealing systems and low-leakage characteristics. Actuated ball valves with metal-seated designs and fire-safe certifications are increasingly specified for applications handling hydrocarbons and flammable materials.
The circular economy principles being adopted across London's industries favor valve products with long service life, maintainability, and recyclable materials. Modular actuator designs that allow component replacement rather than complete unit disposal align with these sustainability objectives while reducing lifecycle costs for facility operators.
For London-based projects requiring reliable, high-performance actuated ball valves, choosing a supplier with proven expertise, comprehensive certification, and responsive technical support is essential.
Contact Our London Technical TeamOver 30 years of manufacturing experience

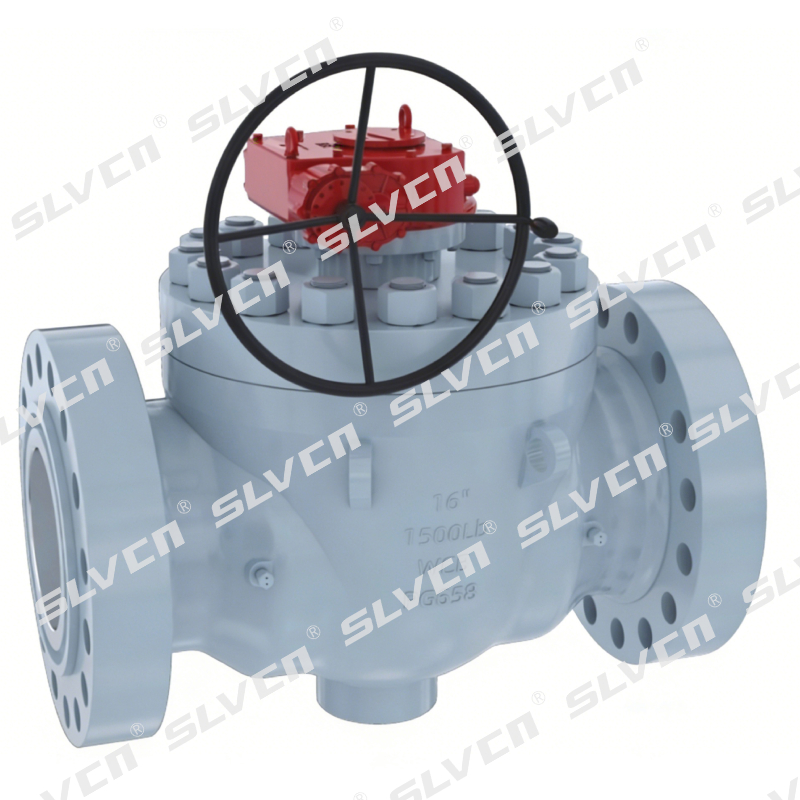
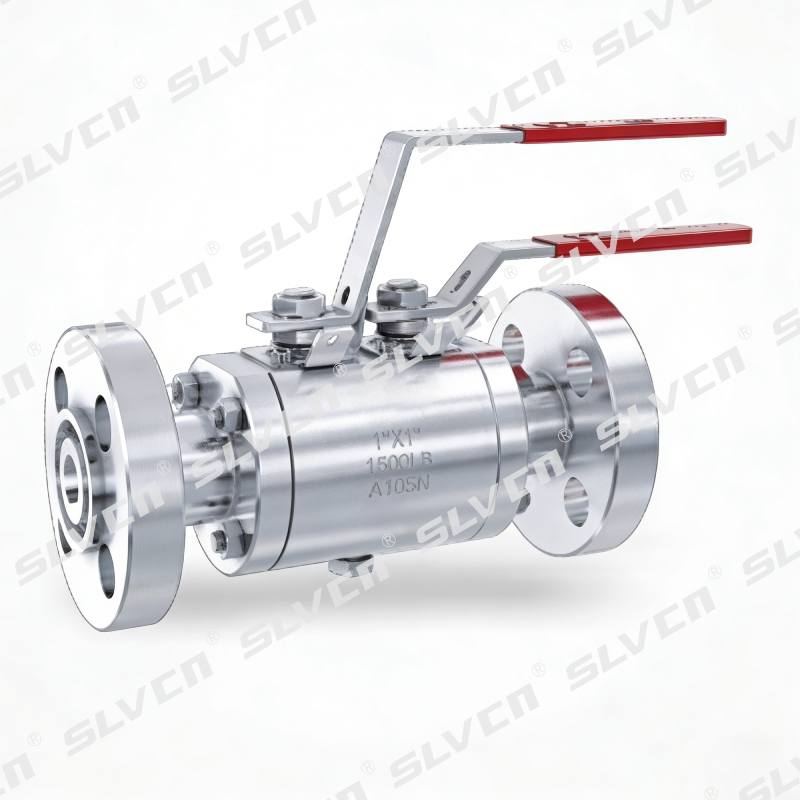
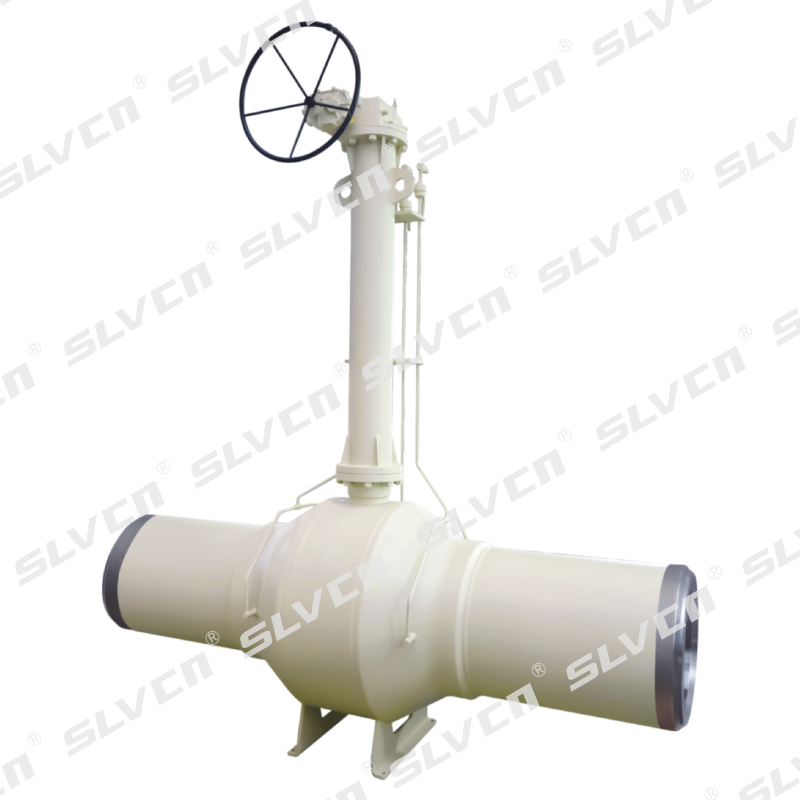
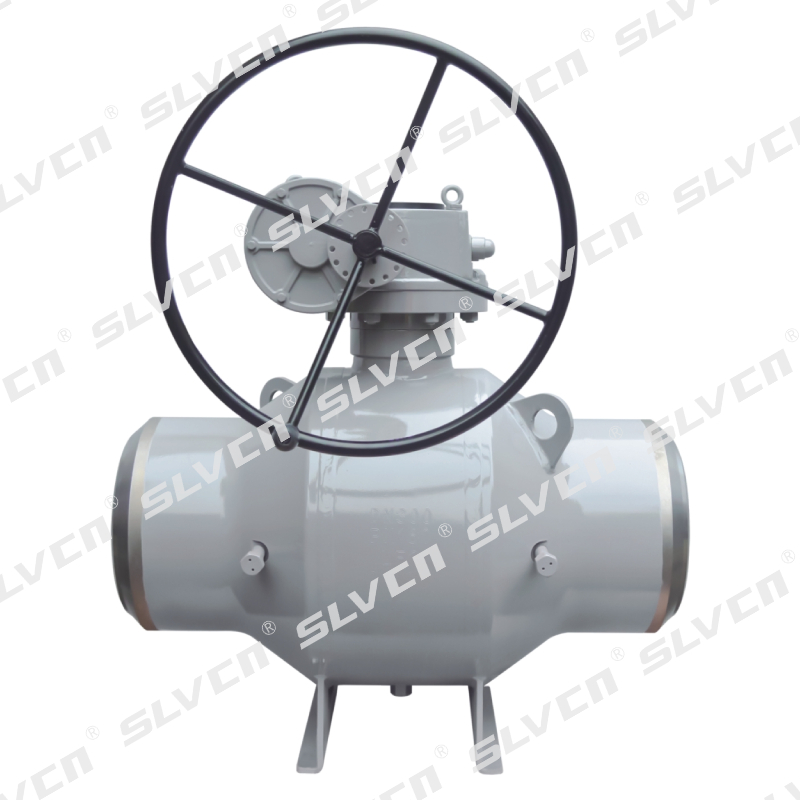
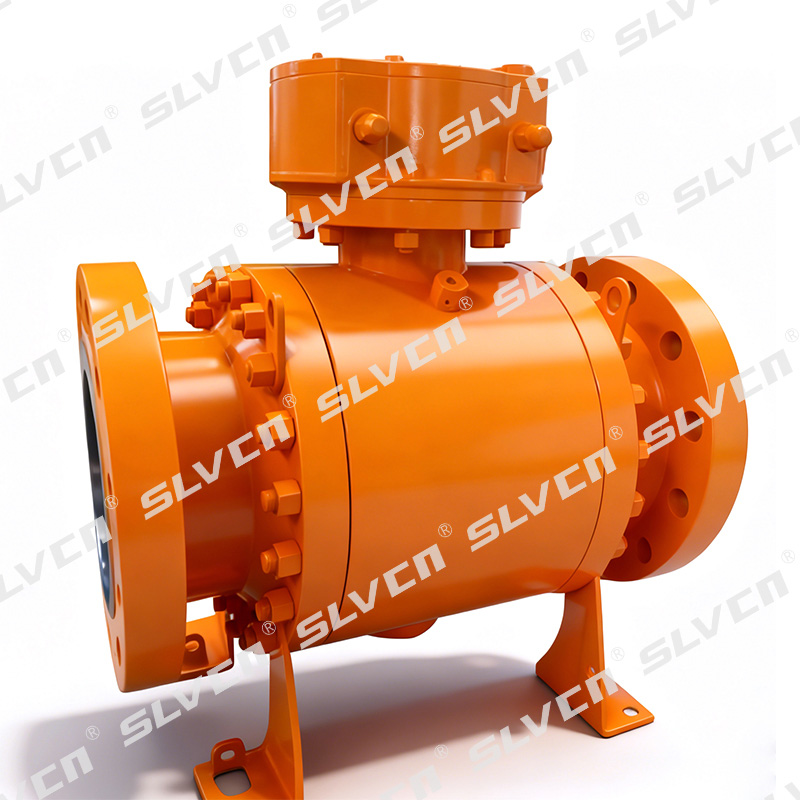
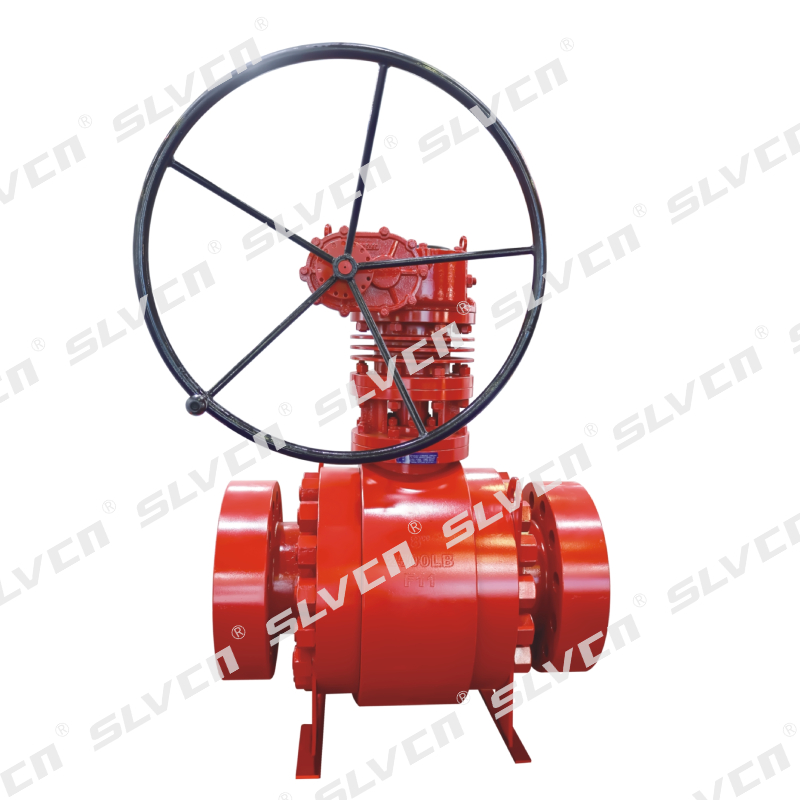
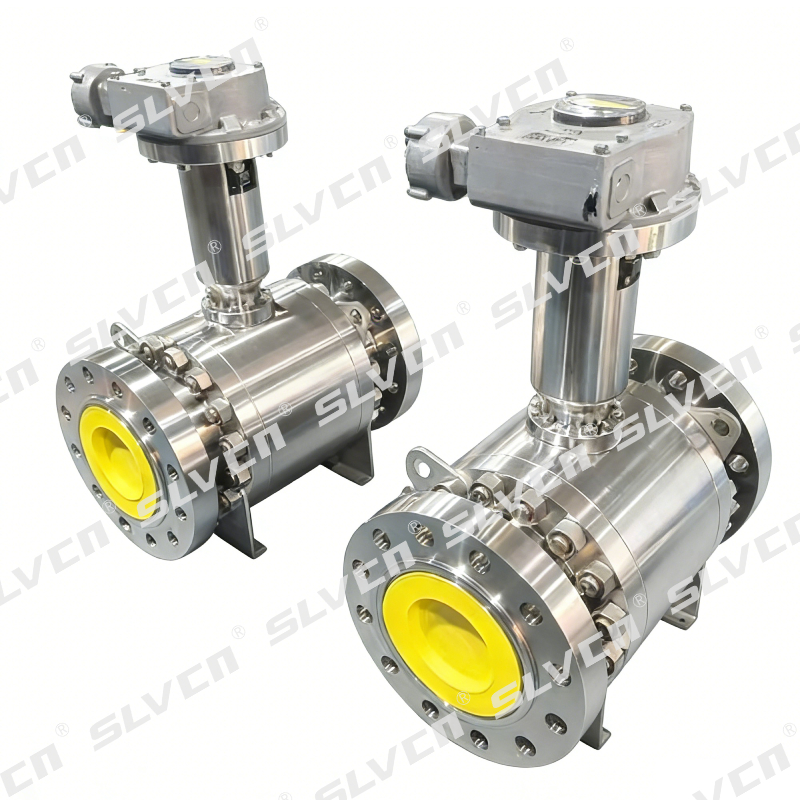
Our core product range covers forged trunnion-mounted and floating ball valves, top-entry and side-entry ball valves, fully welded ball valves, metal seated ball valves, cryogenic ball valves, high-pressure ball valves up to Class 2500 (PN420) and customized higher pressure ratings, as well as high-temperature service valves. Compared with conventional cast valves, SLVCN forged valves feature higher material density, superior mechanical strength, improved resistance to pressure fluctuations and thermal shock, and significantly longer service life under severe service conditions.
Designed for High Pressure, High Temperature, and Cryogenic Applications, SLVCN valves are widely used in long-distance oil & gas transmission pipelines, LNG storage and regasification terminals, offshore platforms and deepwater projects, power plants, refineries, compressor stations, and high-pressure chemical processing units. Whether handling flammable media, corrosive fluids, sour service media (H₂S), ultra-low temperatures, or extreme differential pressures, our valves ensure stable operation, bubble-tight shut-off, and maximum system safety in accordance with international sealing and performance standards.


Comprehensive Range of High-Performance Valve Solutions


 +86 18905154687