


Leave Your Message
In the rapidly evolving landscape of global energy, Liquefied Natural Gas (LNG) has emerged as a critical bridge fuel toward a lower-carbon future. At the heart of this transition are LNG Liquefaction Terminals—complex industrial hubs where natural gas is treated and cooled to -162°C (-260°F) for efficient transport. Within these facilities, the Actuated Ball Valve serves as the primary guardian of flow control, ensuring safety, efficiency, and environmental compliance.
Engineered to withstand temperatures as low as -196°C, utilizing extended bonnets to protect actuator integrity and ensure bubble-tight sealing.
Capable of managing pressures up to Class 2500 (PN420), these valves are forged to prevent porosity and handle extreme thermal cycling.
Equipped with pneumatic, electric, or hydraulic systems for Emergency Shut Down (ESD) scenarios, providing response times measured in seconds.
The global LNG market is currently undergoing a massive expansion phase. With major projects coming online in the United States, Qatar, and Australia, the demand for high-integrity valve solutions has never been higher. Actuated ball valves for LNG liquefaction terminals are no longer just "off-the-shelf" components; they are highly engineered assets designed for a 30-year service life. The move toward larger liquefaction trains (mega-trains) requires larger bore valves—often up to 36 inches—that can handle massive volumes of gas without compromising on torque or sealing performance.

With over 30 years of manufacturing experience, SLVCN is a professional designer and manufacturer of high-performance forged steel ball valves for critical industrial applications. We specialize in extreme working conditions including high pressure, high temperature, and cryogenic environments, providing safe and reliable flow control solutions for global industrial projects where operational reliability is non-negotiable.
Our forged valves feature higher material density and superior mechanical strength compared to conventional cast valves. This makes them exceptionally resistant to pressure fluctuations and thermal shock, ensuring a significantly longer service life under the severe conditions found in LNG terminals.
Contact Our Engineering TeamBefore liquefaction, natural gas must be stripped of impurities like CO2 and H2S. Our Metal Seated DBB Ball Valves are essential here, handling corrosive sour service media in compliance with NACE MR0175 standards. The Double Block and Bleed (DBB) design allows for safe maintenance and isolation without shutting down the entire line.
This is where the magic happens. Natural gas is cooled via heat exchangers. Actuated ball valves here must be "Cryogenic Ready." SLVCN’s cryogenic valves utilize specialized lip seals and PCTFE or metal seats to maintain a bubble-tight shut-off even when the metal components contract at ultra-low temperatures.
Once liquefied, LNG is stored in massive cryogenic tanks. Actuated valves manage the boil-off gas (BOG) and liquid transfer. Reliability is paramount because any valve failure could lead to pressure build-up or hazardous leaks. Our valves feature anti-blowout stems and fire-safe designs certified to API 607.
The final stage involves transferring LNG to carriers. This requires valves that can handle high flow rates and frequent actuation. The integration of intelligent electric actuators allows for precise control of the loading process, minimizing the risk of "water hammer" and ensuring the safety of the vessel and the pier.
The industry is moving toward Intelligent Flow Control. We are integrating IoT sensors into our actuated ball valves to monitor torque, temperature, and leakage in real-time. This "Smart Valve" approach enables predictive maintenance, reducing unplanned downtime in LNG terminals—which can cost operators millions of dollars per day.
Furthermore, as the world looks toward Hydrogen, the expertise gained in LNG cryogenic valves is being pivoted to handle liquid hydrogen, which requires even more extreme temperature management (-253°C). SLVCN is at the forefront of this material science research, testing new alloys and sealing compounds to meet the next generation of energy challenges.
To ensure consistent quality, each SLVCN valve undergoes a complete series of inspections and performance tests in accordance with API 6D, API 598, and ISO 5208. This includes shell tests, seat leakage tests (Rate A / zero visible leakage), fire-safe tests, and our specialized cryogenic tests down to -196°C. We are proud to be certified to ISO 9001, CE, and API standards, serving customers in more than 100 countries.
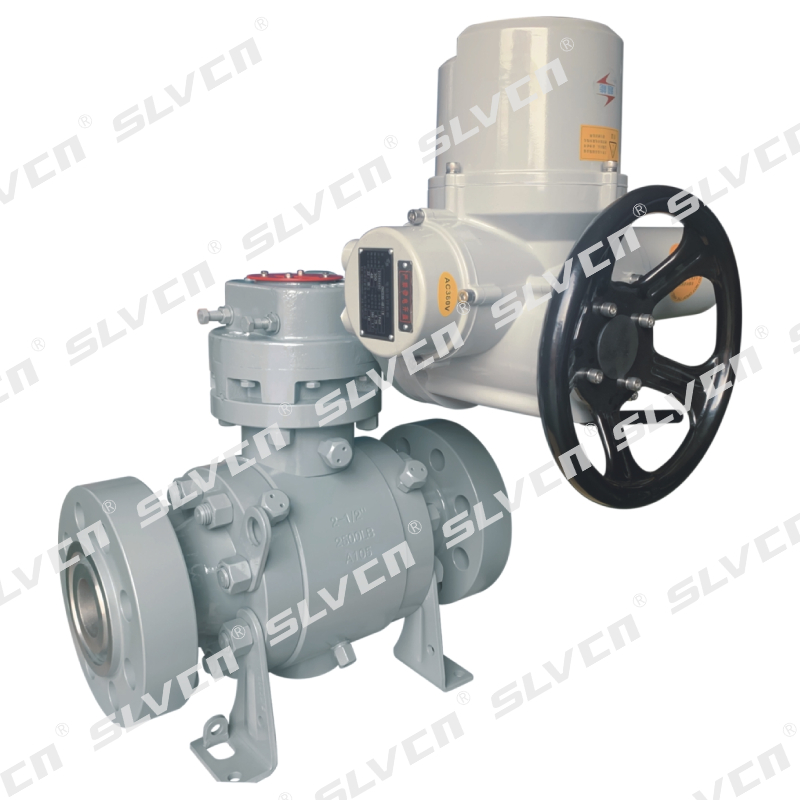 Class 2500 A105 Trunnion Ball Valve - Electric Actuator
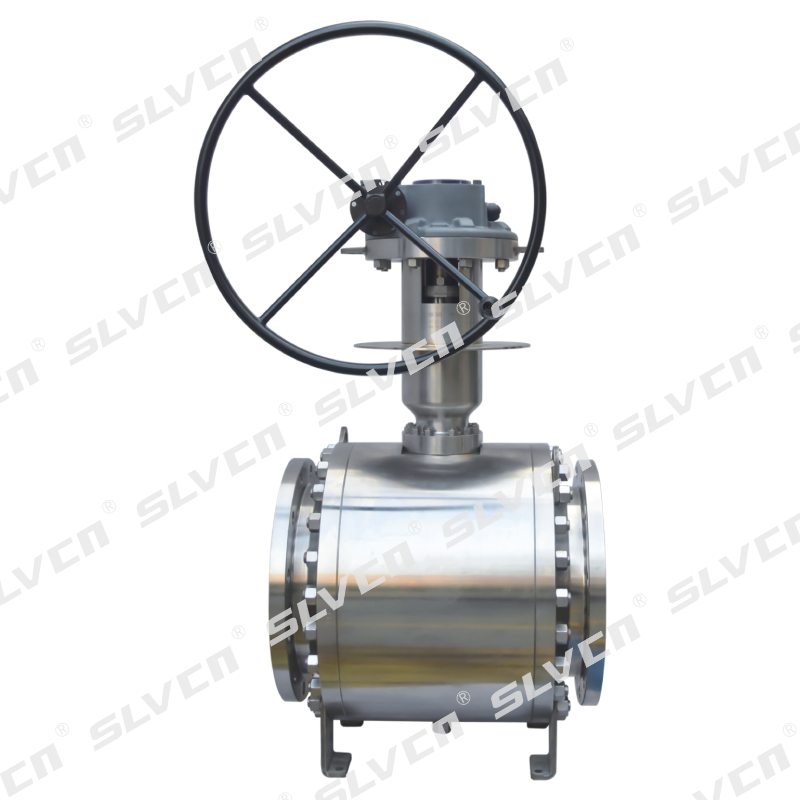 Compact Cryogenic Trunnion Ball Valve with Worm Gear
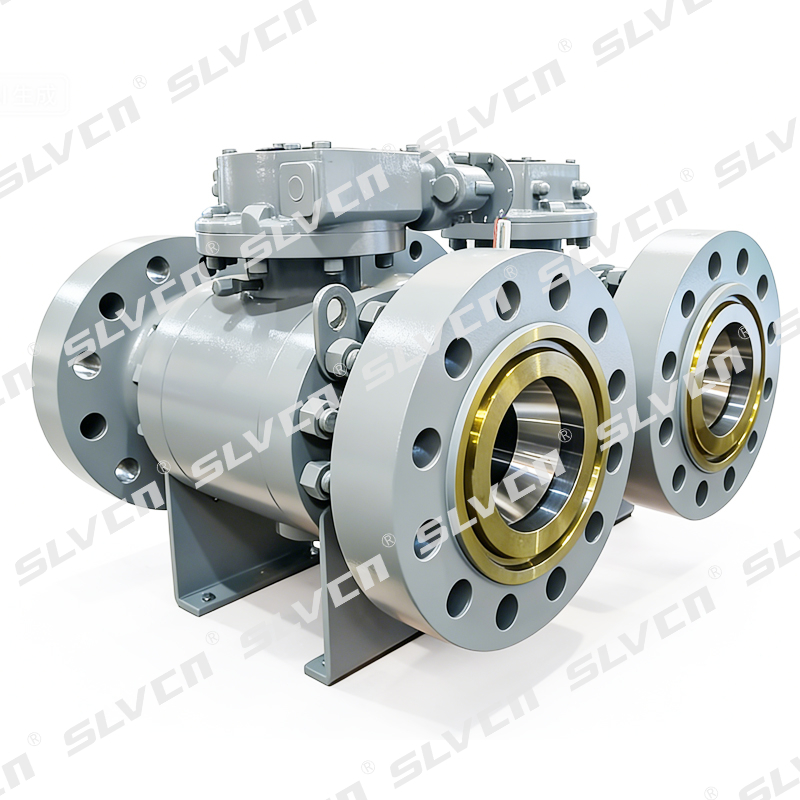 Forged Steel Metal Seated Trunnion-Mounted DBB Valve
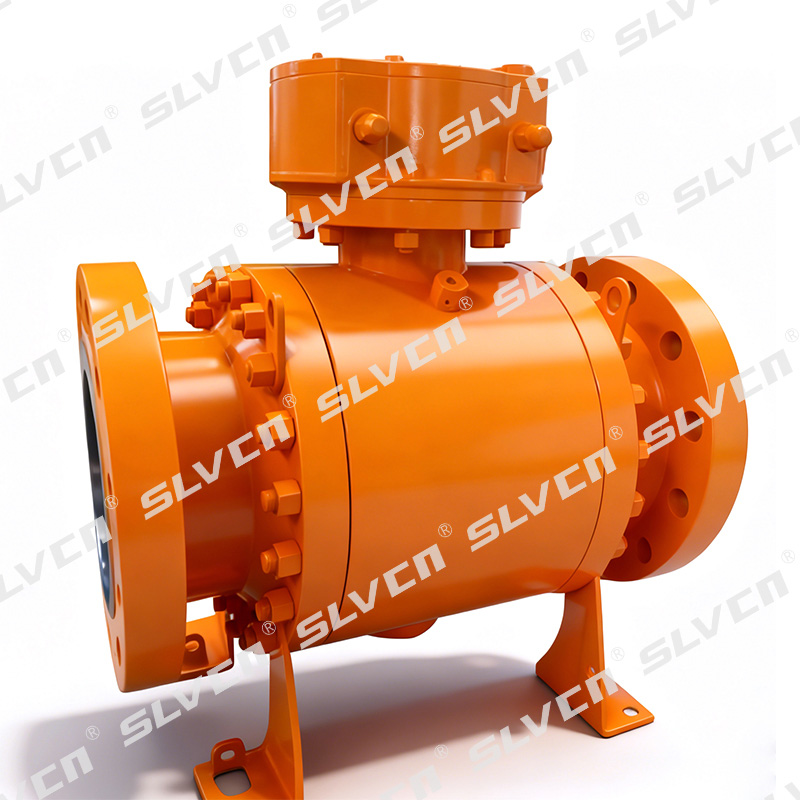 Class 2500 / 6000 PSI Forged DBB Trunnion Ball Valve
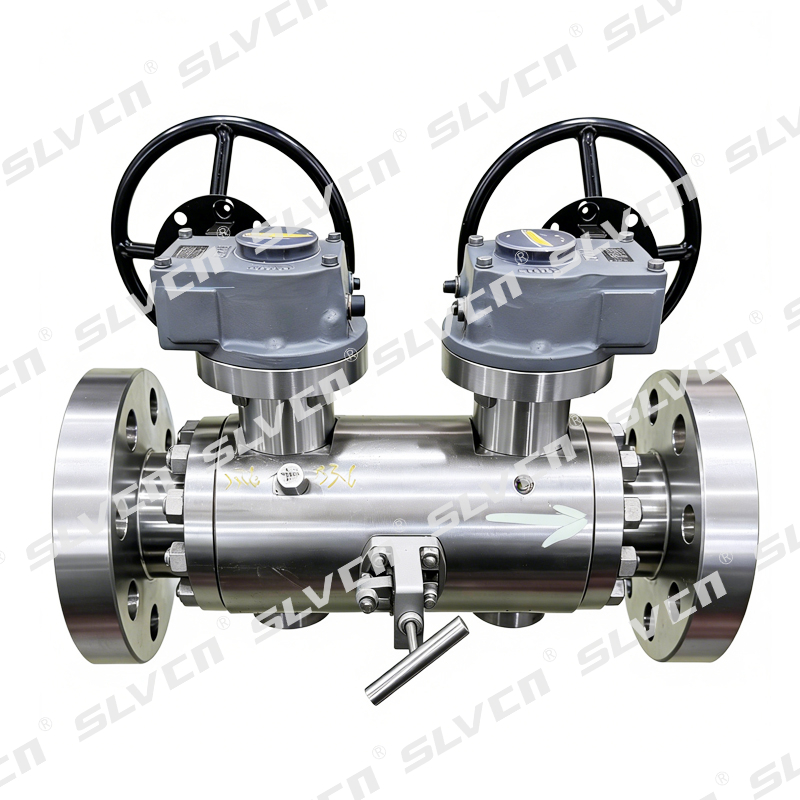 Forged Double Ball DBB Valve with Dual Gear Operation
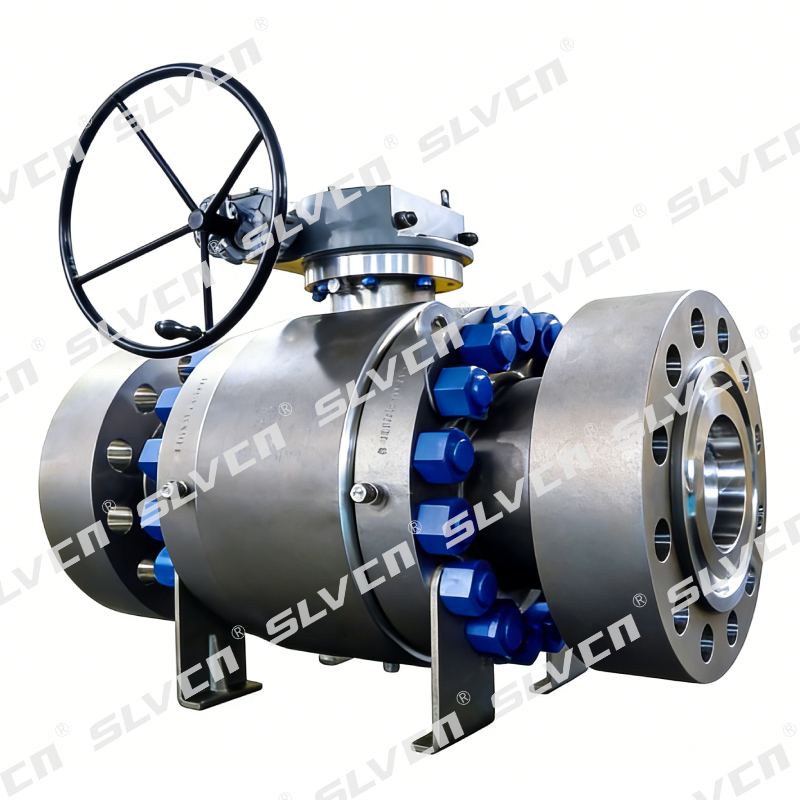 Severe Service Metal-Seated DBB Ball Valve
High-Integrity DBB Ball Valve for Critical Isolation
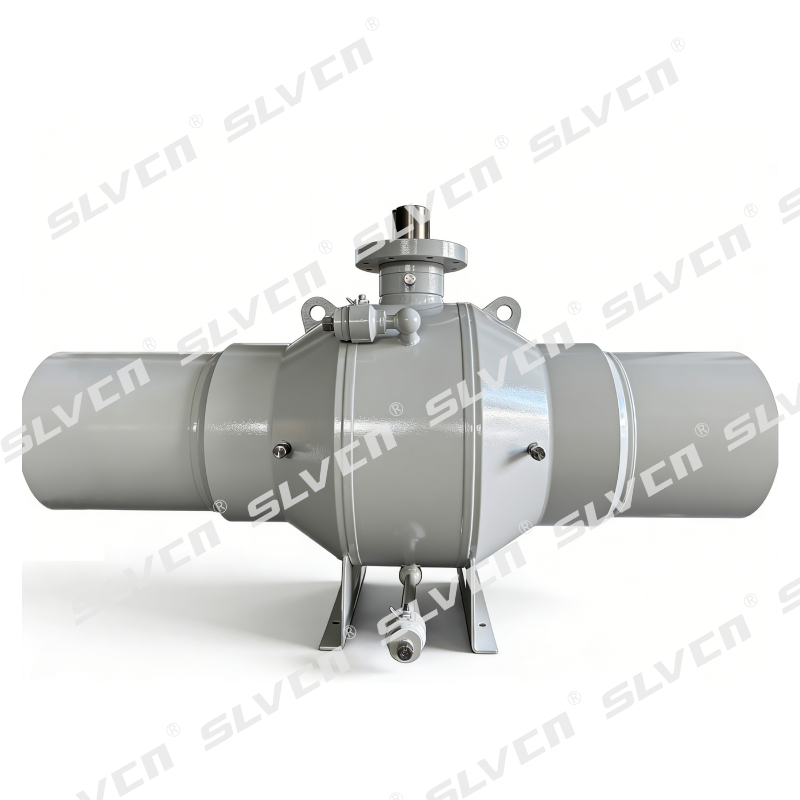 Class 600 Fully Welded Trunnion-Mounted DBB Ball Valve
Today, SLVCN serves customers in more than 100 countries and regions, supplying valves to EPC contractors, engineering companies, and end users across Europe, the Middle East, Southeast Asia, and the Americas. Backed by strong engineering expertise, advanced manufacturing, and rigorous quality control, SLVCN is committed to delivering safe, durable, and truly engineered valve solutions for the world’s most demanding industrial projects.



 18061659285

