


Leave Your Message
Liquid Oxygen (LOX) is the cornerstone of modern aerospace propulsion systems, serving as the primary oxidizer for rockets, satellite launch vehicles, and deep-space exploration systems. Stored and transported at an ultra-low cryogenic temperature of -183°C (-297°F), liquid oxygen presents extreme thermal and mechanical challenges to fluid control components. The rapid growth of commercial spaceflight, spearheaded by private launch service providers, has driven an unprecedented demand for highly reliable, fast-acting actuated ball valves capable of operating safely under these severe conditions.
In aerospace Ground Support Equipment (GSE) and launch pad fueling systems, valves must withstand rapid pressure transitions, high flow velocities, and critical thermal shock. The primary hazard in LOX service is the potential for materials to react with pure oxygen. Any contamination, friction-induced heat, or inappropriate material selection can trigger catastrophic ignition. Therefore, actuated ball valves used in aerospace LOX handling must meet stringent cleanliness standards, fire-safe criteria, and mechanical endurance metrics that far exceed standard industrial requirements.

To ensure zero-leakage performance and long-term reliability in liquid oxygen service, actuated ball valves must incorporate specialized design features that address cryogenic shrinkage, thermal isolation, and combustion risks.
An extended bonnet design places the stem packing and actuator well away from the cryogenic liquid. The gas column formed inside the extension insulates the packing gland, keeping it close to ambient temperature and preventing the actuator from freezing or locking up.
All wetted parts are manufactured from materials resistant to oxygen ignition, such as high-grade forged stainless steel (316/316L, CF8M) or Monel. Non-metallic seals are carefully selected from materials like PCTFE (Kel-F) or reinforced PTFE, which maintain elasticity at cryogenic temperatures.
As liquid oxygen trapped in the valve cavity warms up, it expands rapidly, creating dangerous overpressure. Our ball valves feature engineered pressure-relief paths (such as vented balls or self-relieving seats) to discharge excess pressure safely back upstream.
Valves undergo rigorous cleaning, degreasing, and particulate inspection in certified cleanrooms, complying with international standards like ASTM G93 and CGA G-4.1. This ensures the complete absence of hydrocarbons and organic residues that could cause combustion.
Jiangsu Shoulong Valve Co., Ltd. customizes and manufactures high-integrity actuated ball valves to meet the demanding requirements of aerospace launch facilities and cryogenic storage depots. Below are the core technical specifications designed to ensure reliable operation under extreme pressure and temperature cycles.
| Nominal Diameter | 1/2" to 36" (DN15 to DN900) |
| Pressure Class | ASME Class 150 to Class 2500 / 6000 PSI |
| Temperature Range | -196°C to +120°C (-320°F to +248°F) |
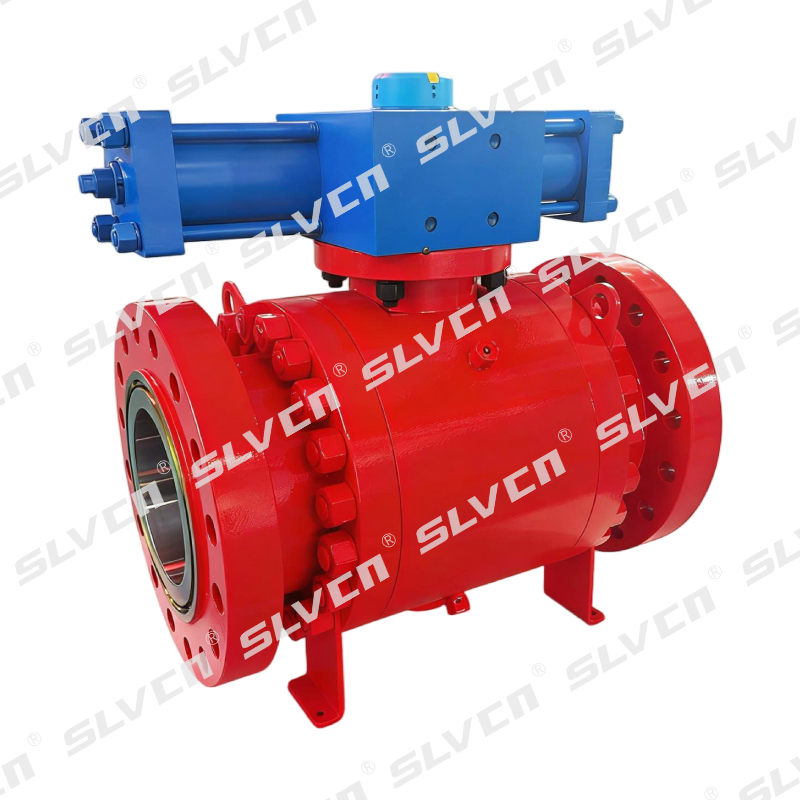
| Actuation Types | Pneumatic (Scotch Yoke / Rack & Pinion), Electric, Hydraulic |
| Sealing Performance | API 598, ISO 5208 Rate A (Zero Leakage) |

The global aerospace sector is undergoing a massive shift from government-led space programs to commercial, high-frequency launch models. This transition demands hardware that is not only highly reliable but also capable of rapid turnaround times and multiple reuse cycles. In Ground Support Equipment (GSE), actuated ball valves are crucial for automated propellant loading sequences. Traditional manual valves are being replaced by smart actuated systems that integrate positioners, limit switches, and diagnostics to monitor valve health in real time.
Furthermore, the push toward larger rockets and heavier payload capacities requires larger pipelines and higher flow rates. This has led to the development of large-diameter, high-pressure cryogenic ball valves. Unlike other valve types, ball valves provide an unobstructed, straight-through flow path, minimizing pressure drop and turbulences that could trigger vaporization in cryogenic lines. The integration of high-torque pneumatic actuators allows these valves to open or close within milliseconds in emergency shutdown (ESD) scenarios, protecting personnel, launch pads, and multi-million dollar rocket payloads.
Another major trend is the development of metal-to-metal seated cryogenic ball valves. While soft seats like PCTFE offer excellent bubble-tight shutoff, they can degrade over thousands of high-velocity thermal cycles. Advanced metal-seated designs with hard coatings (such as tungsten carbide or chromium carbide) provide the resilience needed for reusable launch installations, reducing maintenance overhead and downtime between flights.

With over 30 years of manufacturing experience, SLVCN is a professional designer and manufacturer of high-performance forged steel ball valves for critical industrial applications. We specialize in extreme working conditions including high pressure, high temperature, and cryogenic environments, providing safe and reliable flow control solutions for global industrial projects where operational reliability is non-negotiable.
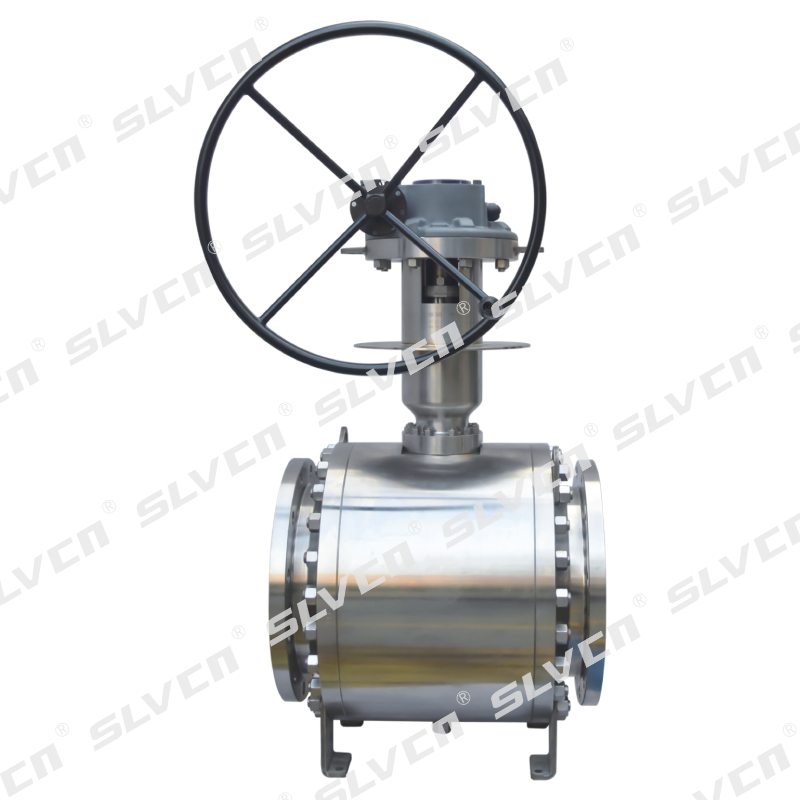
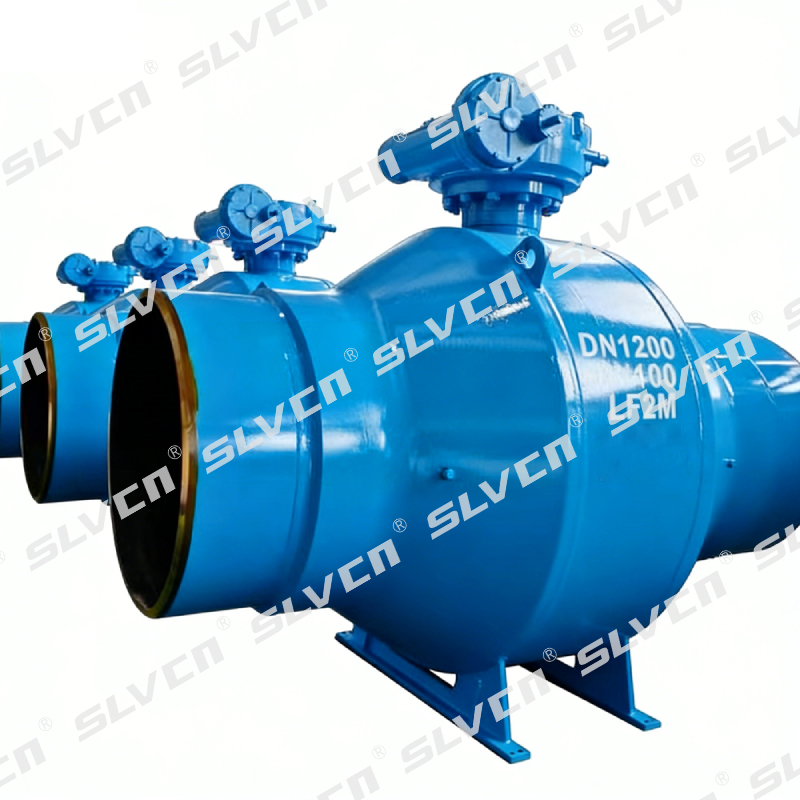
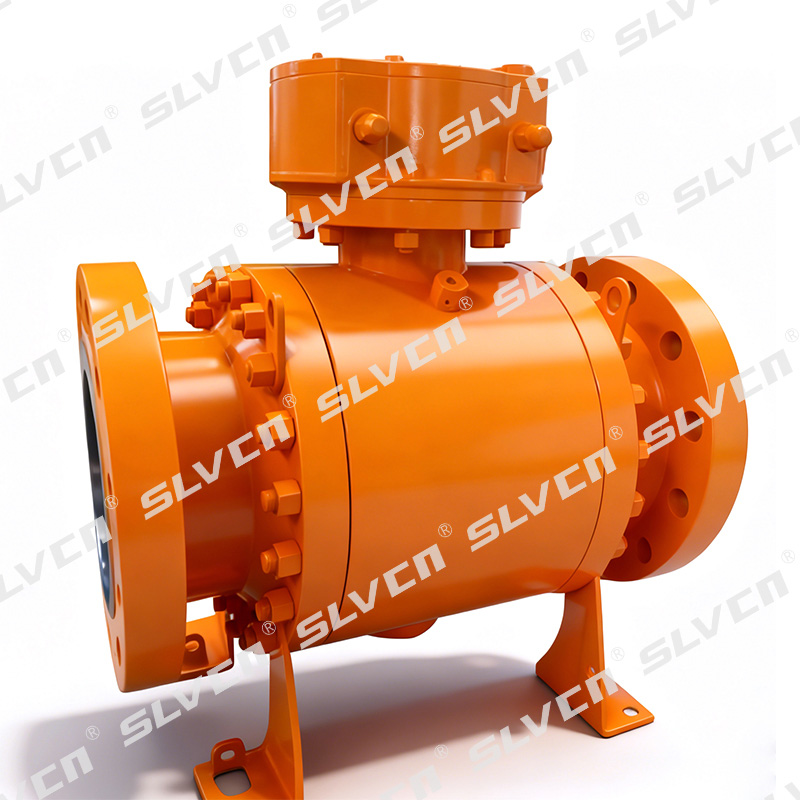
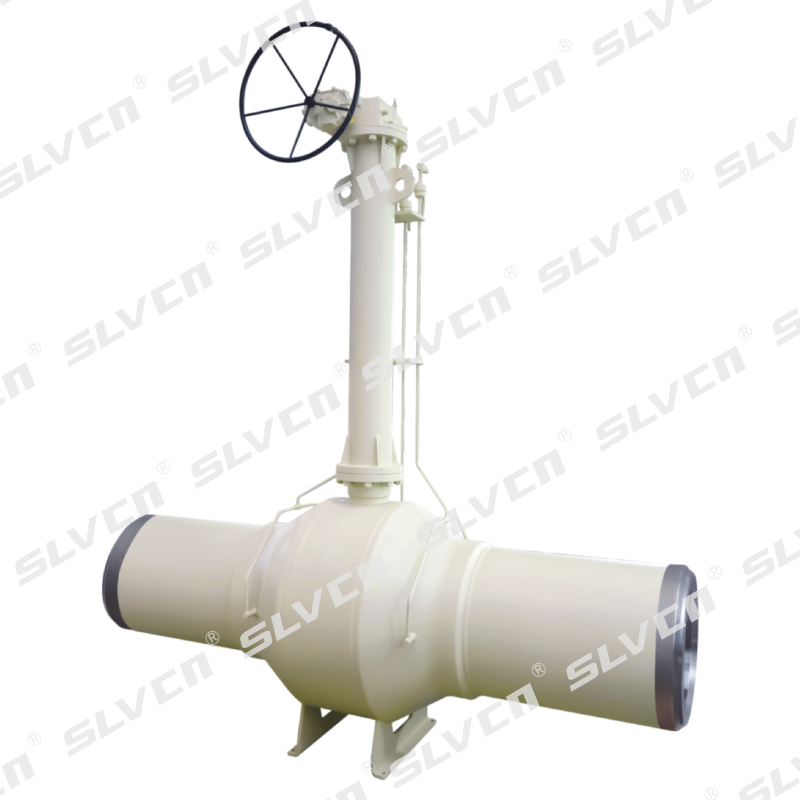
Our core product range covers forged trunnion-mounted and floating ball valves, top-entry and side-entry ball valves, fully welded ball valves, metal seated ball valves, cryogenic ball valves, high-pressure ball valves up to Class 2500 (PN420) and customized higher pressure ratings, as well as high-temperature service valves. Compared with conventional cast valves, SLVCN forged valves feature higher material density, superior mechanical strength, improved resistance to pressure fluctuations and thermal shock, and significantly longer service life under severe service conditions.
Designed for High Pressure, High Temperature, and Cryogenic Applications, SLVCN valves are widely used in long-distance oil & gas transmission pipelines, LNG storage and regasification terminals, offshore platforms and deepwater projects, power plants, refineries, compressor stations, and high-pressure chemical processing units. Whether handling flammable media, corrosive fluids, sour service media (H₂S), ultra-low temperatures, or extreme differential pressures, our valves ensure stable operation, bubble-tight shut-off, and maximum system safety in accordance with international sealing and performance standards.
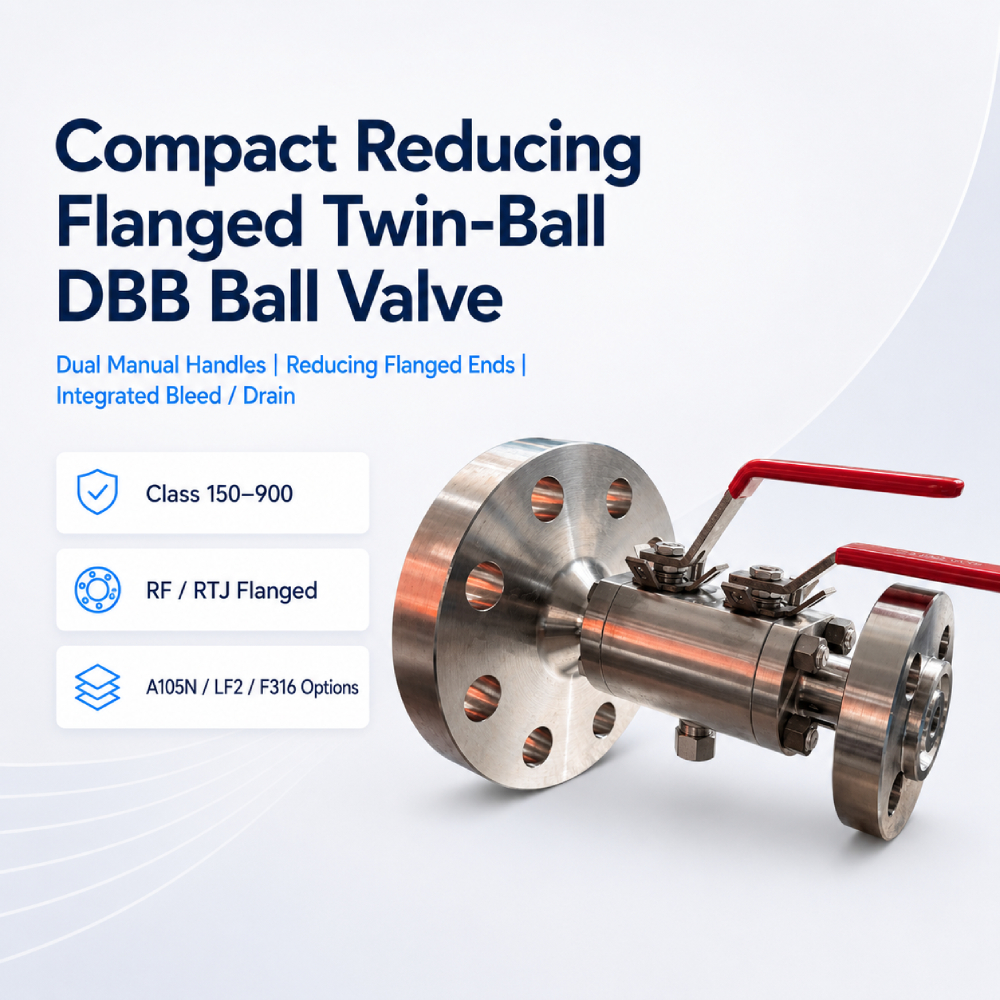
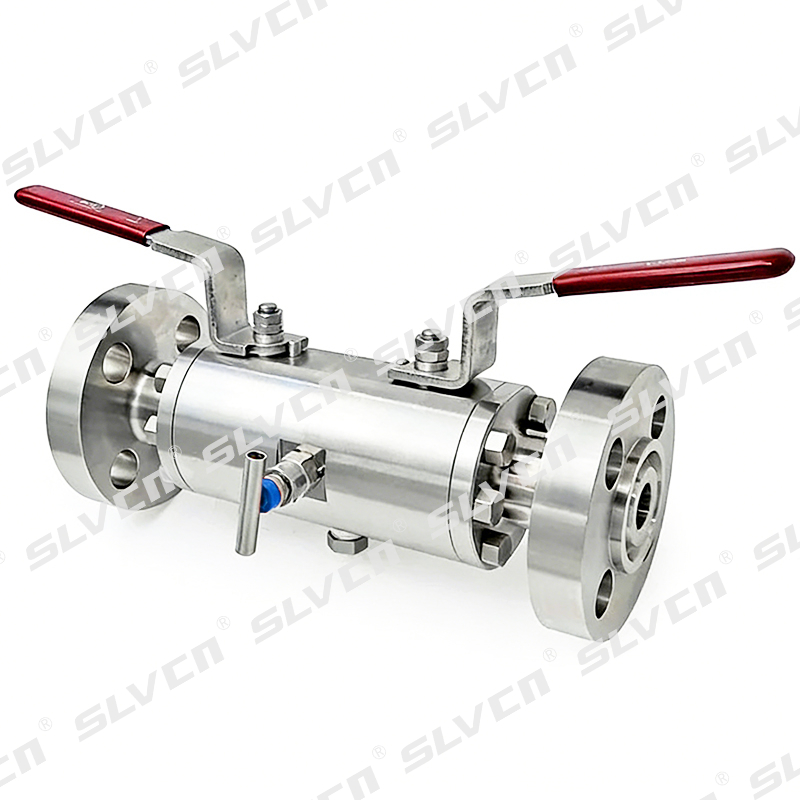
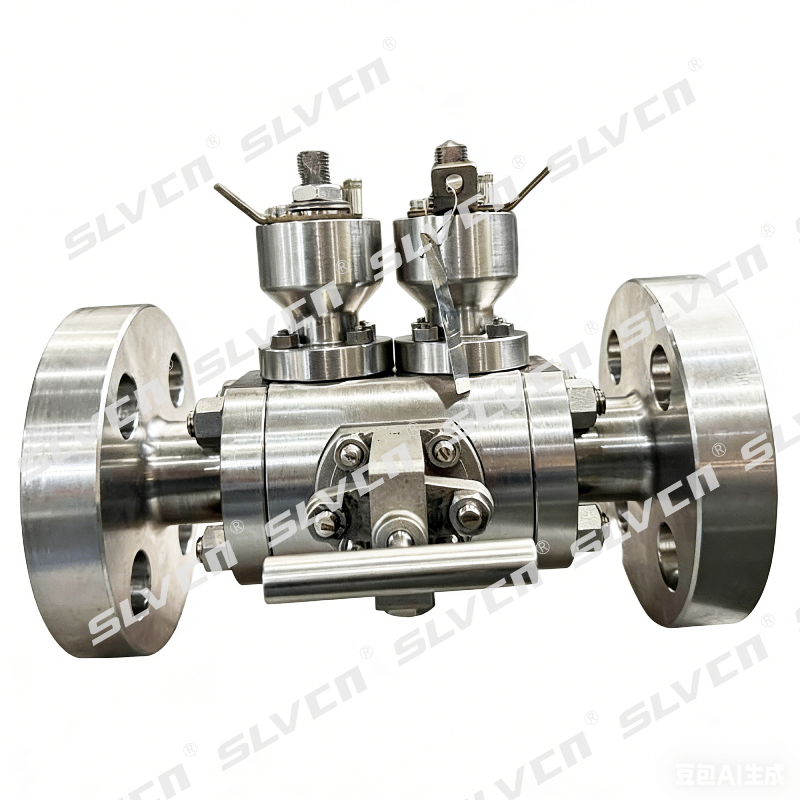
Safety and reliability are embedded in every design. Our forged ball valves are equipped with Double Block and Bleed (DBB) structures, anti-blowout stems, fire-safe designs in accordance with API 607 / API 6FA, anti-static devices, emergency sealing systems, and pressure-balanced seating structures suitable for high differential pressure operation. Valves can be designed with SPE or DPE seat configurations based on application requirements. For sour service environments, materials and sealing systems comply with NACE MR0175 / ISO 15156 requirements.
To ensure consistent quality, each valve undergoes a complete series of inspections and performance tests in accordance with API 6D, API 598, and ISO 5208, including shell test, seat leakage test (Rate A / zero visible leakage), fire-safe test, cryogenic test, operational torque test, dimensional inspection, and PMI material verification. SLVCN operates dedicated cryogenic testing facilities to validate valve performance at ultra-low temperatures down to −196°C.
SLVCN is certified to ISO 9001, CE, and API standards, and our products comply with API 6D, ASME B16.34, DIN, ANSI, and JIS specifications. We provide extensive customization capabilities covering sizes from 1/2” to 36”, full bore or reduced bore, special materials including A105, LF2, F11, F22, F51, Inconel, various soft and metal seat designs, and intelligent actuation with pneumatic, electric, and gear operators.
Today, SLVCN serves customers in more than 100 countries and regions, supplying valves to EPC contractors, engineering companies, and end users across Europe, the Middle East, Southeast Asia, and the Americas. Backed by strong engineering expertise, advanced manufacturing, and rigorous quality control, SLVCN is committed to delivering safe, durable, and truly engineered valve solutions for the world’s most demanding industrial projects.


 18061659285

